

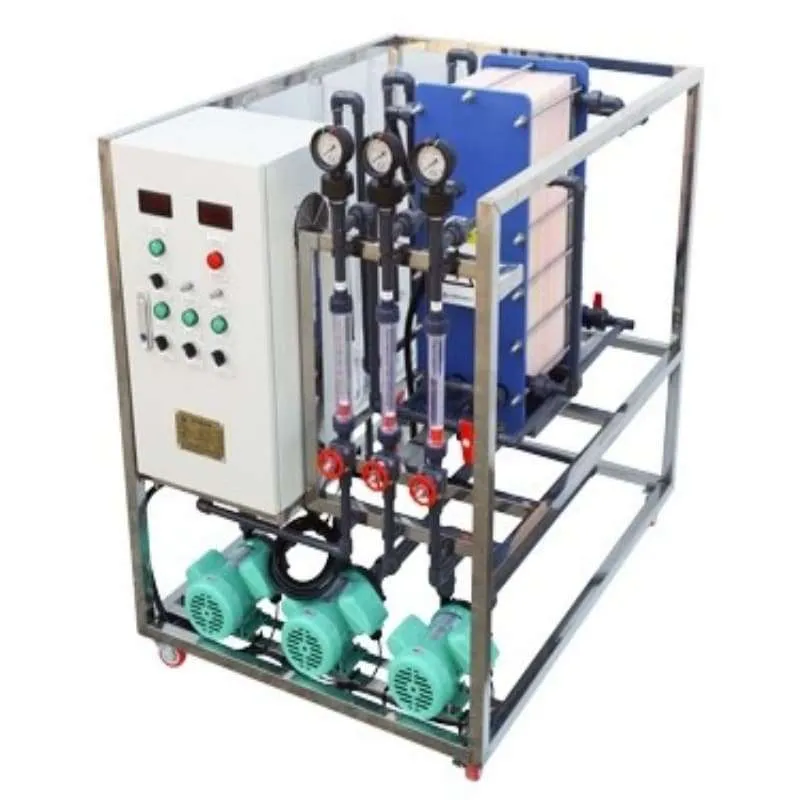
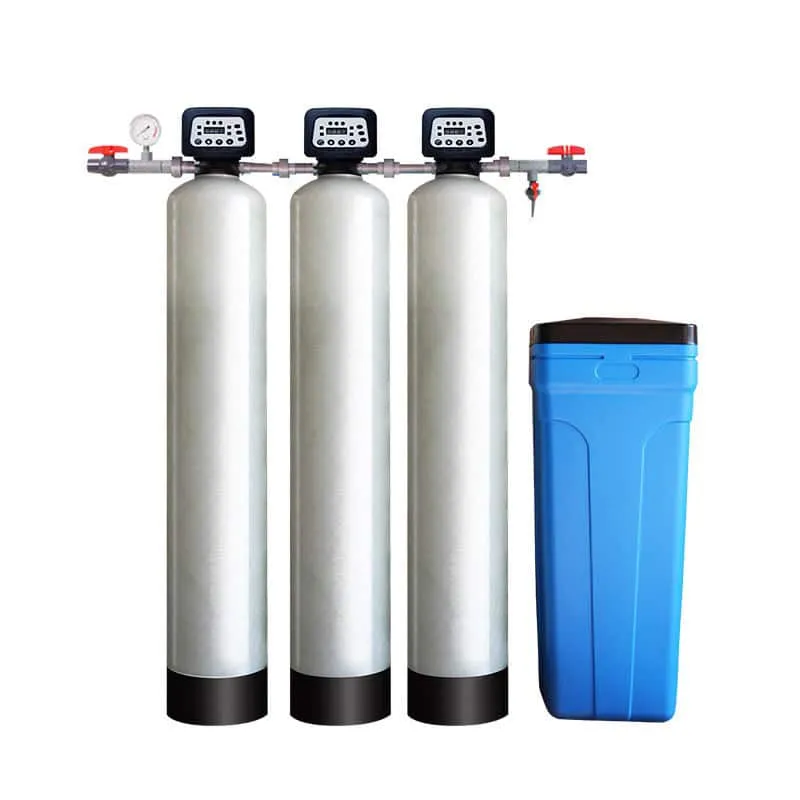
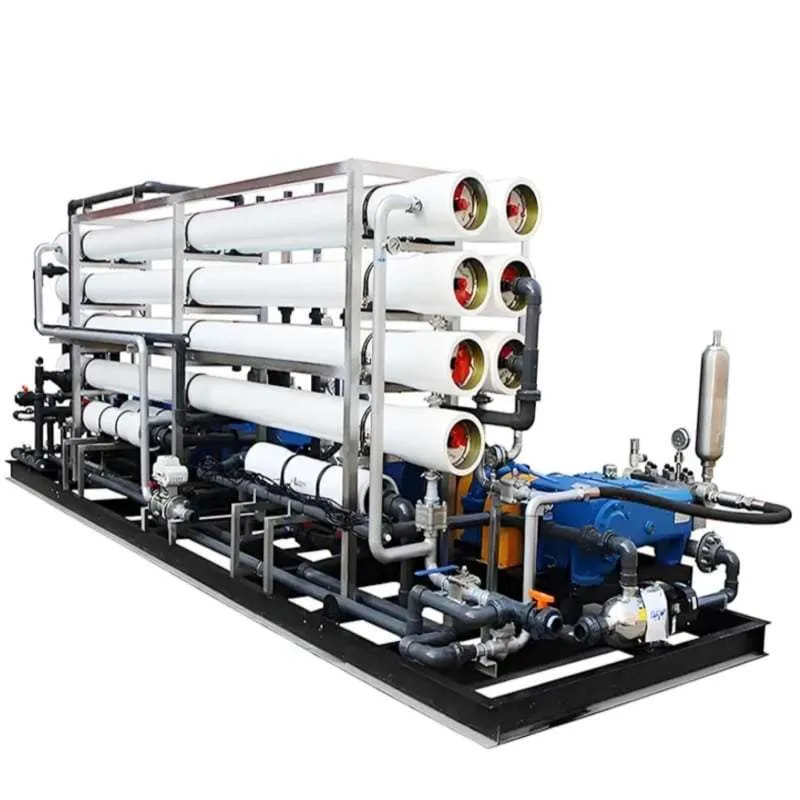
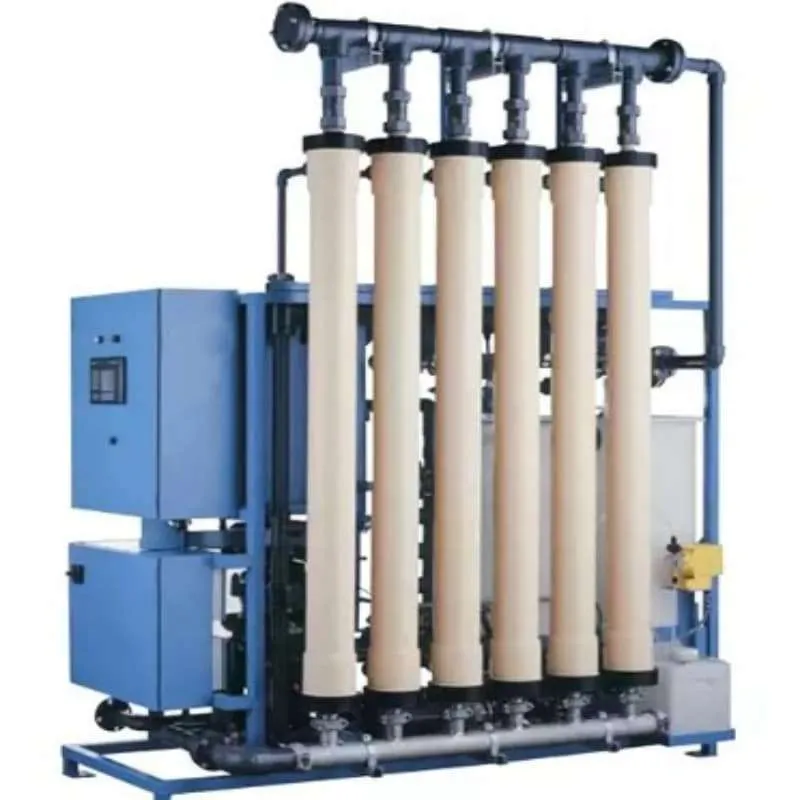
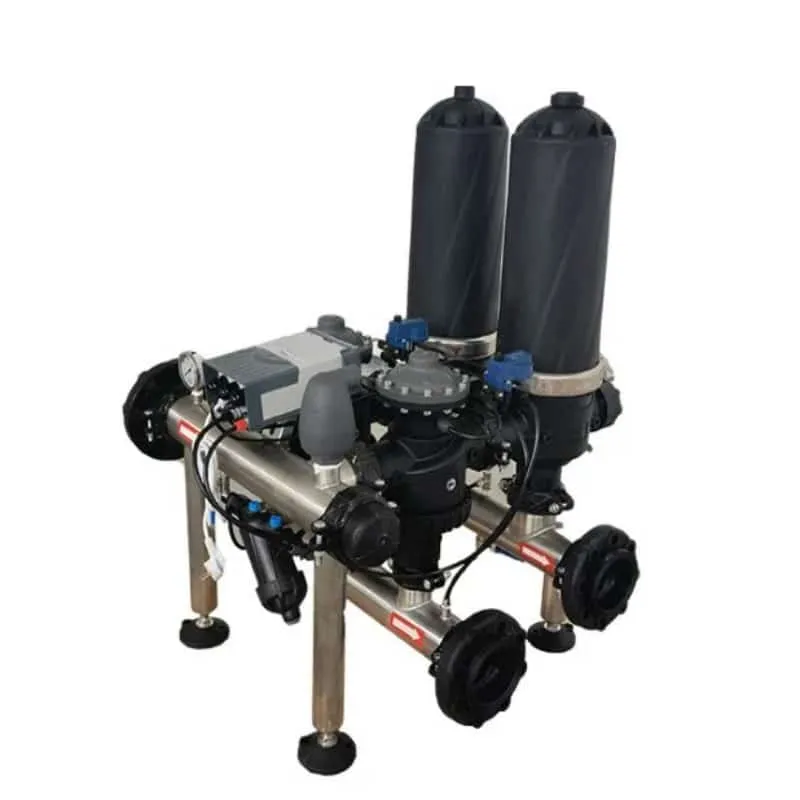
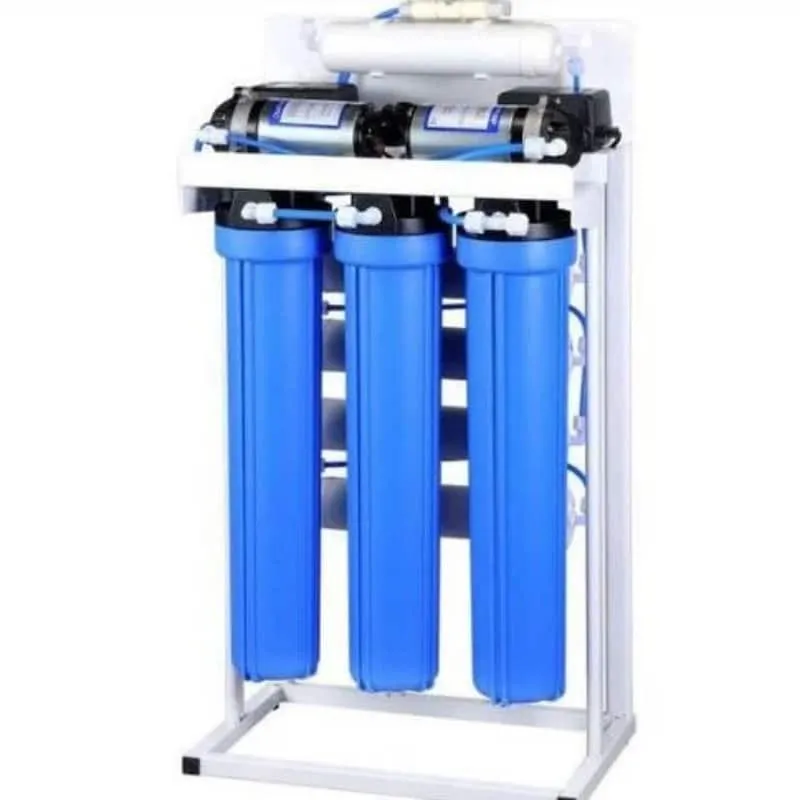



Demineralization water refers to the process of eliminating dissolved salts and minerals to produce high-purity water. This process plays a vital role in industries where water quality directly impacts performance and safety. For example, laboratories rely on it for cleaning equipment, while the electronics sector uses it to prevent defects in circuit boards. Additionally, the food and beverage industry depends on it to maintain product purity.
How Demineralization Water Works

Ion Exchange Process
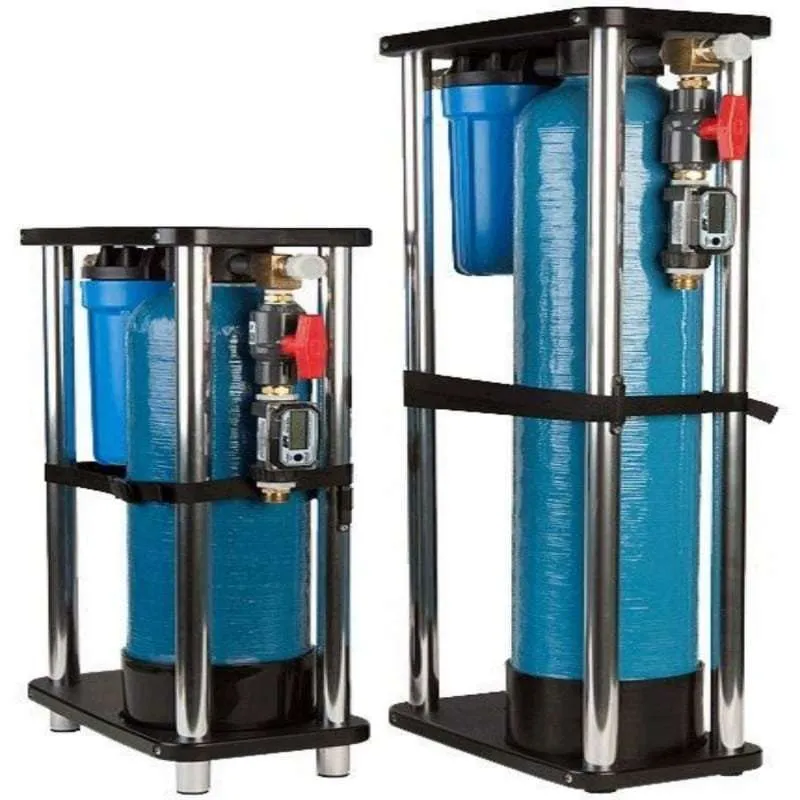
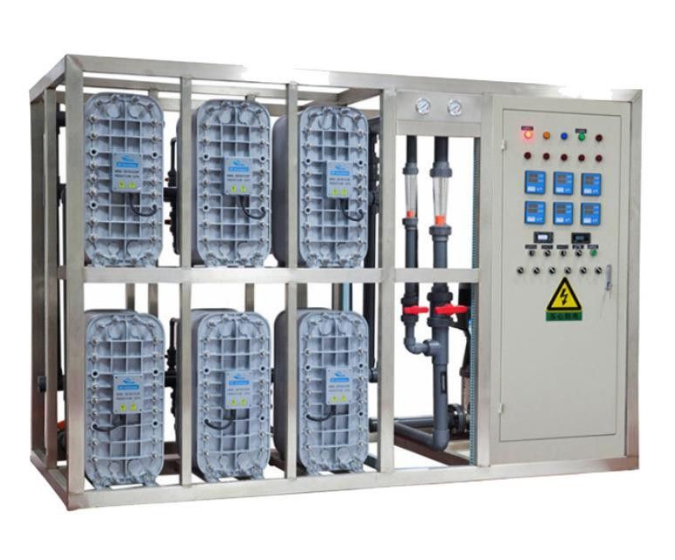
The ion exchange process is one of the most effective methods for producing demineralization water. It involves a series of steps to remove dissolved ions from water:
Pretreatment: Suspended solids, organic matter, and chlorine are removed through filtration or sedimentation. This step ensures the water is ready for ion exchange.
Ion Exchange: Water flows through cation and anion exchange resins. Cations like calcium and magnesium are replaced with hydrogen ions, while anions like chloride and sulfate are exchanged for hydroxyl ions.
Regeneration: The resins are restored to their original state by backwashing, applying a regenerant solution, and rinsing.
Rinse: Any remaining regenerant and exchanged ions are flushed out, leaving behind high-purity water.
This method is widely used in industries requiring consistent water quality, such as power plants and pharmaceuticals.
Reverse Osmosis Method
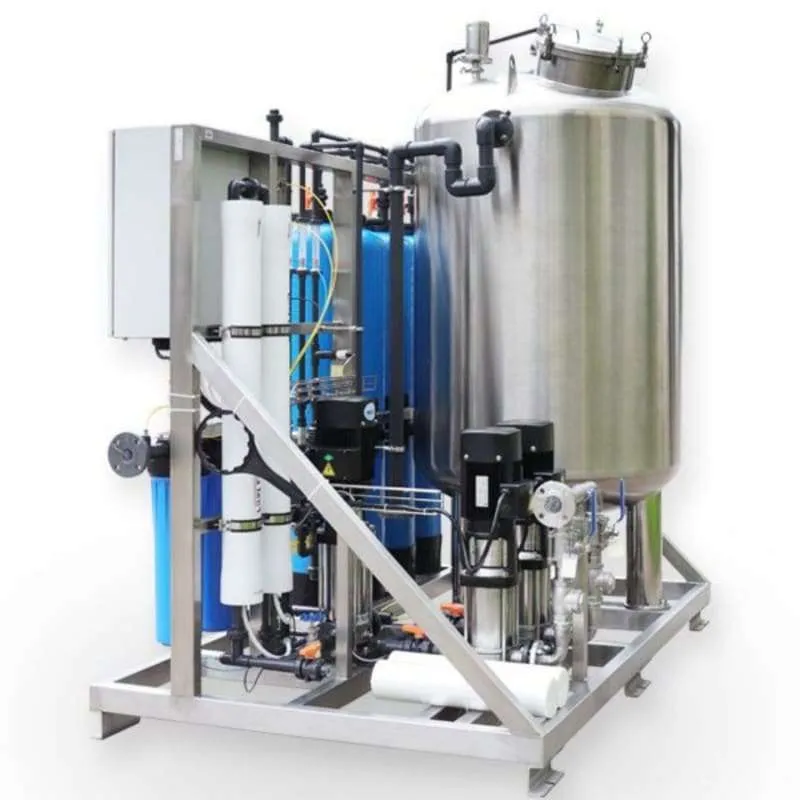
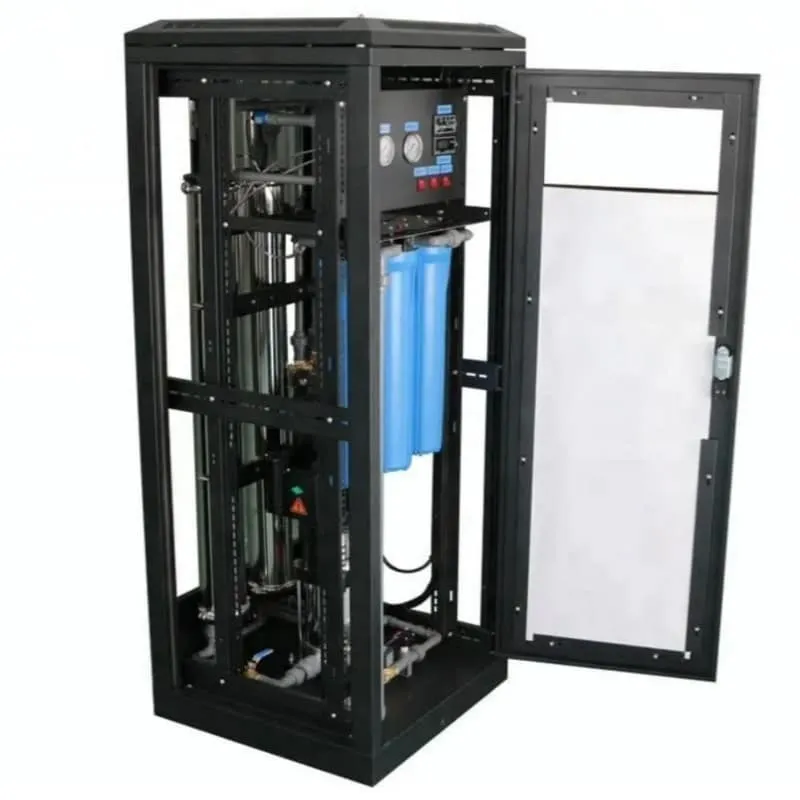
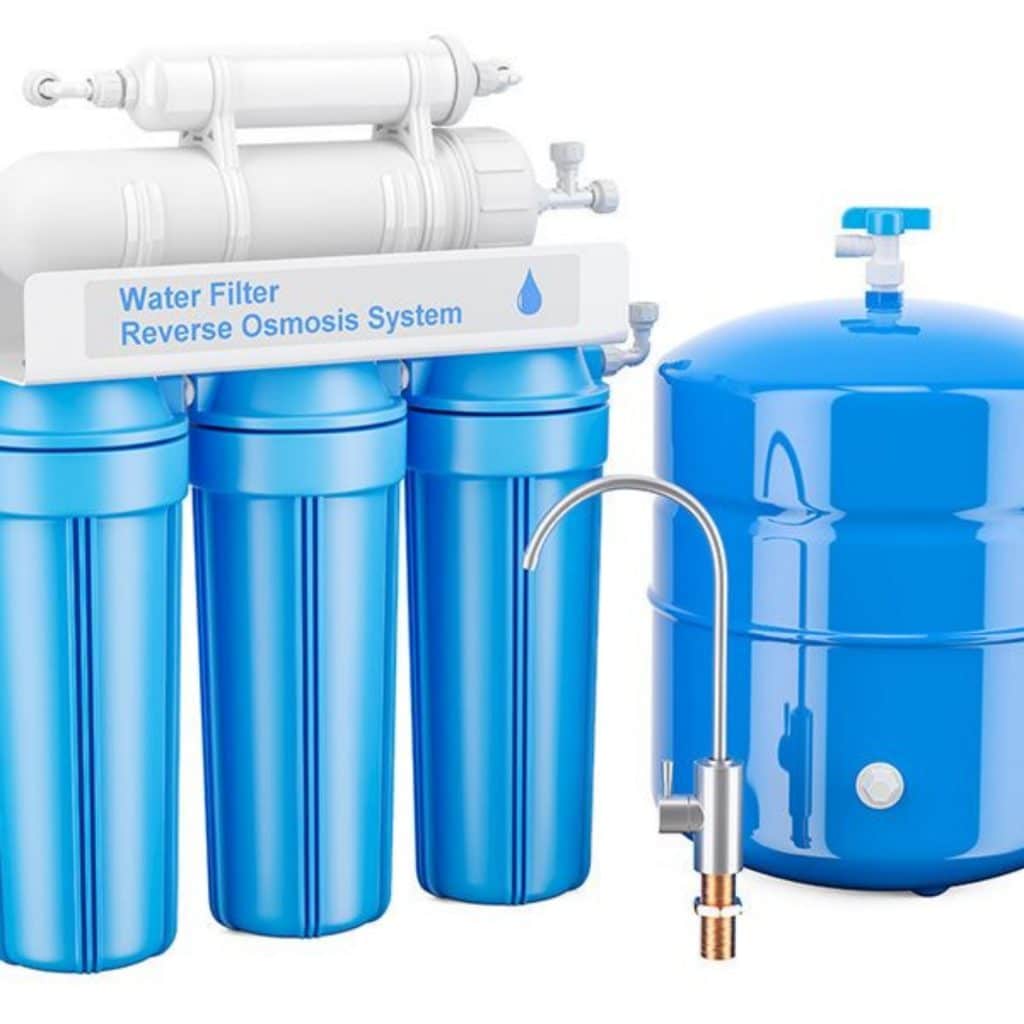
Reverse osmosis is another popular technique for creating demineralization water. It uses a semi-permeable membrane to separate water molecules from contaminants. Pressure is applied to force water through the membrane, allowing only pure water molecules to pass. This process effectively removes ions, dissolved salts, and other impurities.
The scientific principle behind reverse osmosis involves osmotic pressure. Water naturally moves from areas of low solute concentration to high solute concentration. By applying external pressure, you reverse this natural flow, ensuring contaminants are left behind. This method is highly efficient and suitable for large-scale applications like desalination and industrial water treatment.
Distillation Technique
Distillation is a traditional yet reliable method for achieving demineralization water. It involves heating water to its boiling point, converting it into steam. The steam rises, leaving behind impurities and dissolved salts. Once cooled, the steam condenses back into liquid form, resulting in purified water.
This technique is particularly useful in laboratories and medical facilities where water purity is critical. Although energy-intensive, distillation remains a trusted option for producing water free from contaminants.
Benefits of Demineralization Water

High Purity for Industrial and Medical Applications
You can rely on demineralization water to meet the stringent purity requirements of industrial and medical fields. In pharmaceutical production, it ensures that medications remain free from contaminants, safeguarding patient health. Electronics manufacturing benefits from its use by preventing mineral-related flaws in sensitive components. The cosmetic industry also depends on it to eliminate mineral pollutants, ensuring skincare products maintain their efficacy and safety.
In breweries, demineralized water plays a vital role in creating consistent flavors across batches. It also allows customization of unique taste profiles. Whether you’re producing medicines, electronics, or beverages, this high-purity water guarantees superior quality and reliability.
Prevention of Equipment Scaling and Corrosion
Scaling and corrosion can significantly reduce the lifespan of industrial equipment. Demineralization water prevents these issues by removing dissolved salts and minerals that cause buildup. For example, in power generation, it protects steam turbines from mineral scale accumulation, ensuring smooth operation. Cooling systems also benefit, as corrosion is minimized, extending their service life.
By using demineralized water, you reduce wear and tear on machinery. This not only enhances operational efficiency but also lowers the risk of unexpected breakdowns. The result is a more reliable and cost-effective production process.
Cost-Effectiveness in Long-Term Use
Although the initial setup for demineralization systems may seem costly, the long-term savings are substantial. You save on maintenance costs by reducing equipment damage caused by scaling and corrosion. Operational downtime decreases, allowing you to maintain productivity. Industries like cleaning and car washing also benefit, as demineralized water dries without leaving residues, eliminating the need for additional cleaning steps.
This water also supports sensitive formulations, ensuring product safety and efficacy. Whether you’re in manufacturing or healthcare, the financial advantages of using demineralized water make it a smart investment for the future.
Applications of Demineralization Water
Pharmaceuticals and Healthcare
In the pharmaceutical and healthcare sectors, demineralization water plays a pivotal role in maintaining the highest standards of purity. You will find it essential in pharmaceutical manufacturing, where it serves as a raw material, ingredient, and solvent. Its use ensures that medications meet stringent quality requirements, safeguarding patient health.
In medical environments, demineralized water prevents ions and minerals from interfering with sensitive processes. It is indispensable for laboratory tests, autoclaves, and dialysis machines, where even trace contaminants can compromise results or patient safety. Regulatory standards, such as those from the United States Pharmacopeia (USP), mandate its use to guarantee the purity required for drug production, cleaning, and sterilization processes.
Electronics and Semiconductor Manufacturing
The electronics and semiconductor industries rely heavily on demineralization water for their operations. Its absence of minerals ensures that scaling and corrosion do not compromise product quality. You will see it used in cooling systems, cleaning processes, and steam production, where high-purity water is critical.
In semiconductor manufacturing, the demand for ultra-pure water is non-negotiable. The purification process must deionize, sanitize, and filter water to remove contaminants. Cleaning semiconductor wafers requires water of exceptional purity, as even invisible impurities can disrupt the manufacturing process. By using demineralized water, you can meet the stringent quality standards necessary for producing flawless electronic components.
Automotive and Power Generation Industries
In the automotive and power generation industries, demineralization water enhances operational efficiency and reduces maintenance costs. By removing minerals that hinder heat transfer, it prevents corrosion and scaling in critical equipment like boilers and turbines. This extends the lifespan of machinery and ensures safe, efficient operations.
In power plants, demineralized water is indispensable for preventing mineral scale buildup in steam turbines and cooling systems. Its use minimizes downtime and maintenance, allowing you to maintain consistent productivity. Similarly, in the automotive sector, it supports processes like engine testing and cooling system maintenance, ensuring optimal performance and reliability.
Demineralization Water vs. Other Purification Methods

Comparison with Water Softening
You might wonder how demineralized water differs from softened water. While both processes improve water quality, their goals and outcomes vary significantly. Demineralization removes most or all dissolved minerals, achieving a higher purity level. In contrast, water softening targets only hardness minerals like calcium and magnesium, replacing them with sodium ions.
Feature | Demineralized Water | Softened Water |
|---|---|---|
Mineral Removal | Removes most or all minerals | Targets hardness minerals (Ca, Mg) |
Replacement Ions | None | Replaces with sodium |
Purity Level | Higher purity | Lower purity due to soluble salts |
If your application demands ultra-pure water, demineralization is the superior choice.
Comparison with Distilled Water
Distilled water and demineralized water serve different purposes. Distillation removes a broader range of contaminants, including bacteria and organic compounds, making it purer overall. However, it involves a more complex production process and higher energy consumption. Demineralized water focuses on eliminating specific ions and minerals, offering a cost-effective solution for many industrial needs.
For instance, laboratories often prefer distilled water for its unmatched purity, while industries like power generation rely on demineralized water to prevent scaling and corrosion.
Unique Advantages of Demineralization
Demineralized water offers several unique benefits across industries:
In the cosmetic industry, it prevents mineral pollutants from affecting product quality.
Car washes use it to avoid water spots, as it dries without leaving residues.
In pharmaceuticals, it ensures medications remain free of disruptive ions.
Electronics manufacturing benefits from its ability to prevent flaws in components.
Power plants rely on it to avoid mineral scale buildup in turbines.
Laboratories use it to ensure accurate test results.
It enhances the taste and shelf life of food and beverages.
These advantages make demineralized water an indispensable resource for diverse applications.
Demineralized water removes dissolved minerals, ensuring high purity for industrial and specialized applications. Its benefits include:
Preventing mineral scales in steam turbines for efficient power generation.
Reducing cross-contamination risks during cleaning and sterilization.
Maintaining product quality in pharmaceuticals, electronics, and food processing.
Industries like power plants, laboratories, and microelectronics have improved efficiency and reduced costs by adopting this solution. Explore its potential to enhance your operations.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian