




Project Background
The food and beverage industry relies heavily on high-quality water for production processes, including ingredient preparation, cleaning, and cooling. Ensuring water purity is essential to maintain product quality and comply with stringent health and safety standards. This case study examines a project undertaken by our company to provide advanced water treatment solutions for a leading beverage manufacturer.
Project Requirements
The beverage manufacturer required a comprehensive water treatment system capable of:
- Purifying water to meet WHO drinking water standards, removing impurities, microorganisms, and harmful chemicals.
- Supplying high-purity water for diluting and mixing beverage formulations, as well as for equipment cleaning, to prevent contaminants from affecting taste and quality.
- Ensuring continuous operation to meet high production demands.
- Providing real-time water quality monitoring to ensure compliance with health and safety standards.
Technical Details
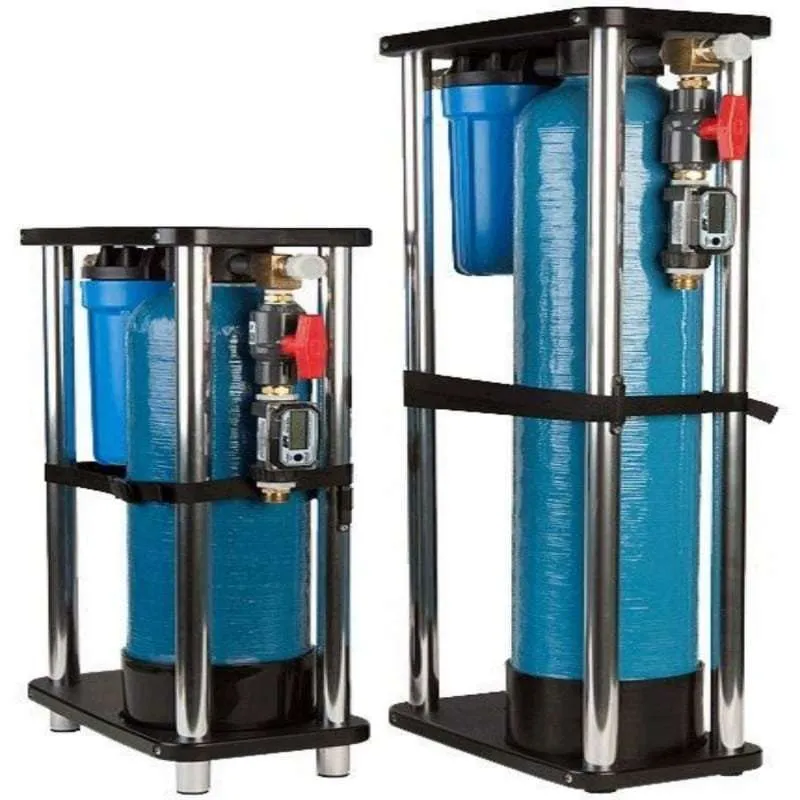
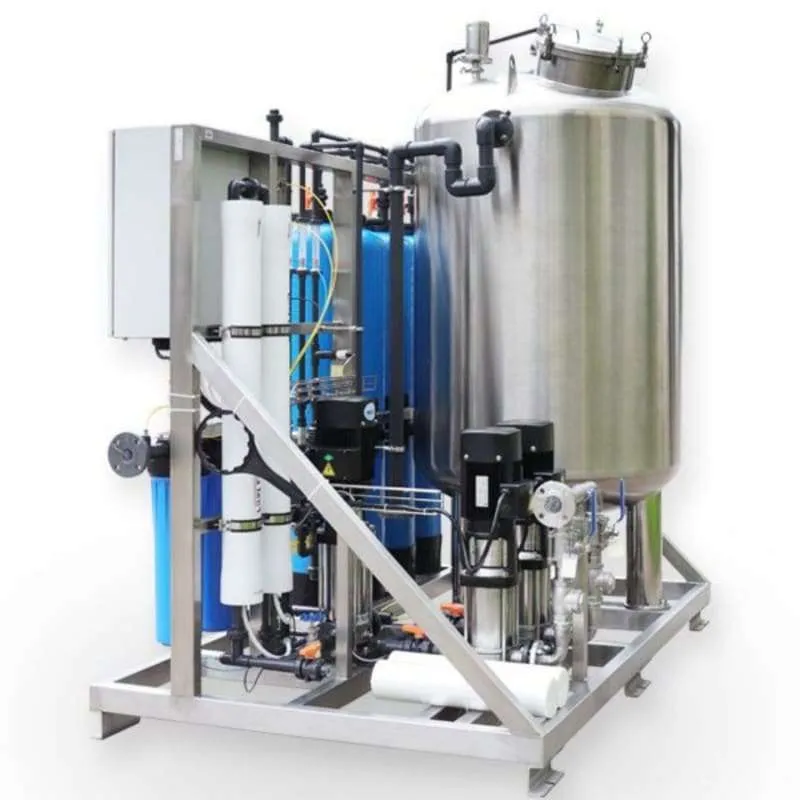
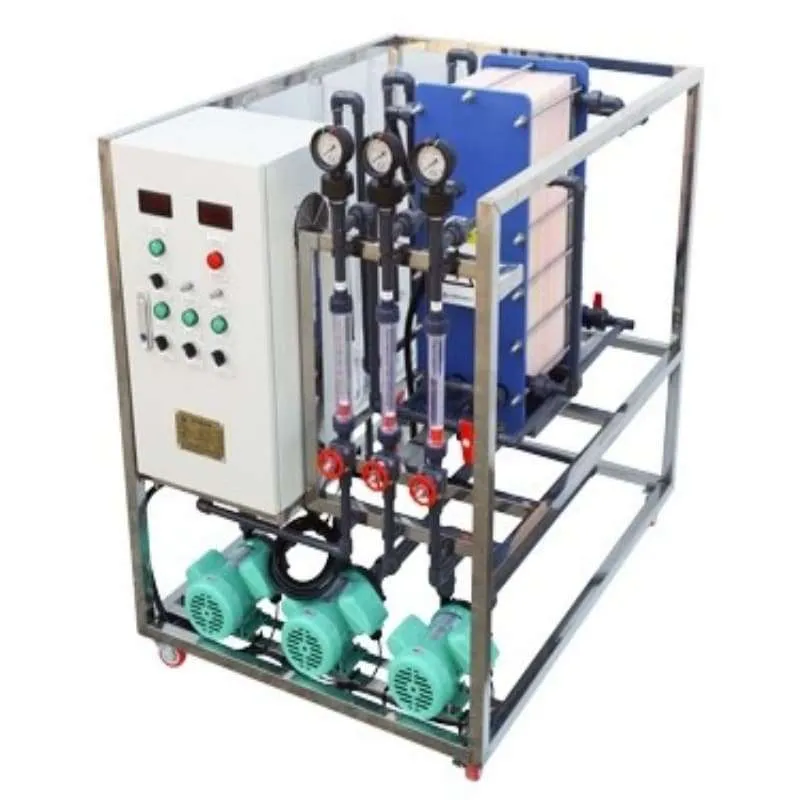
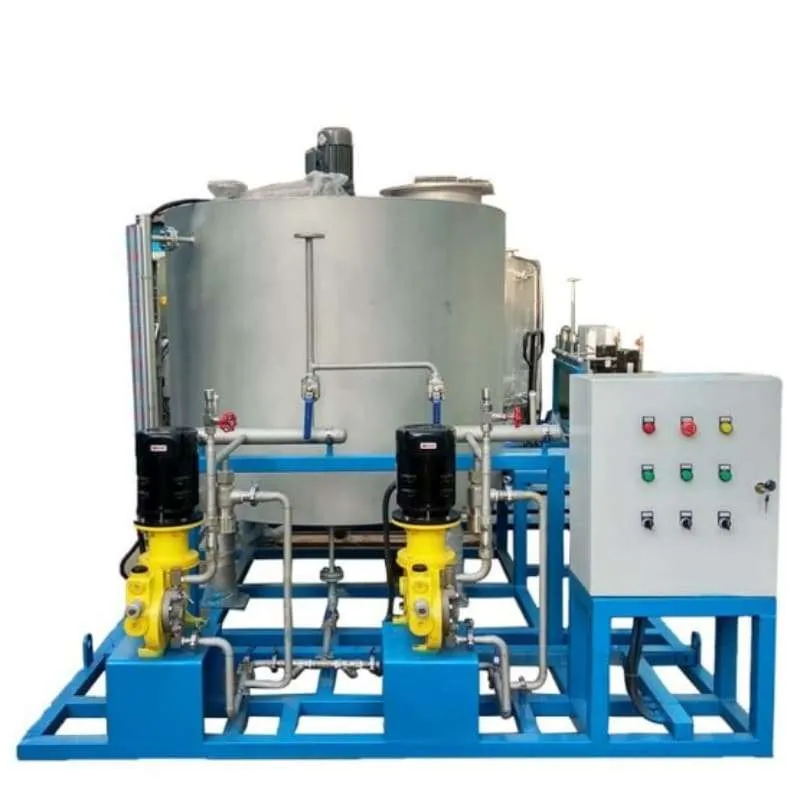
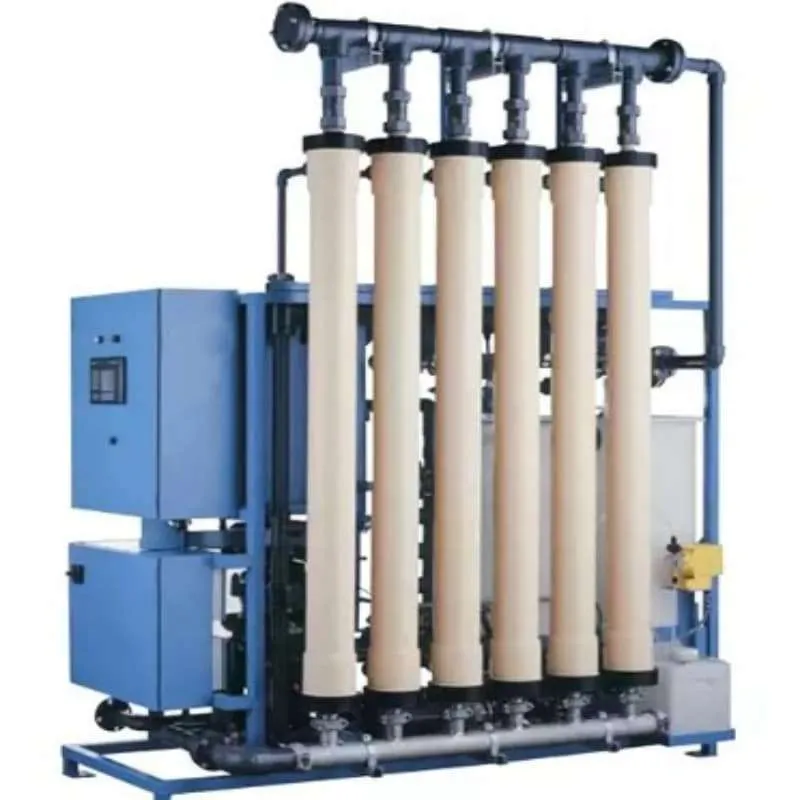
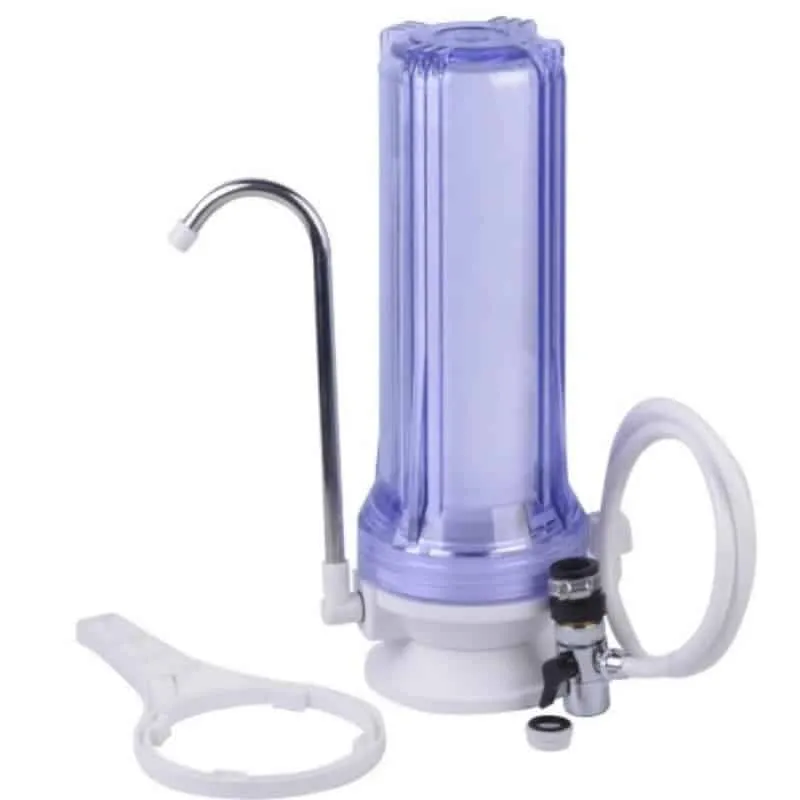
Our solution incorporated a multi-stage water treatment process, including:
- Pre-Treatment Stage:
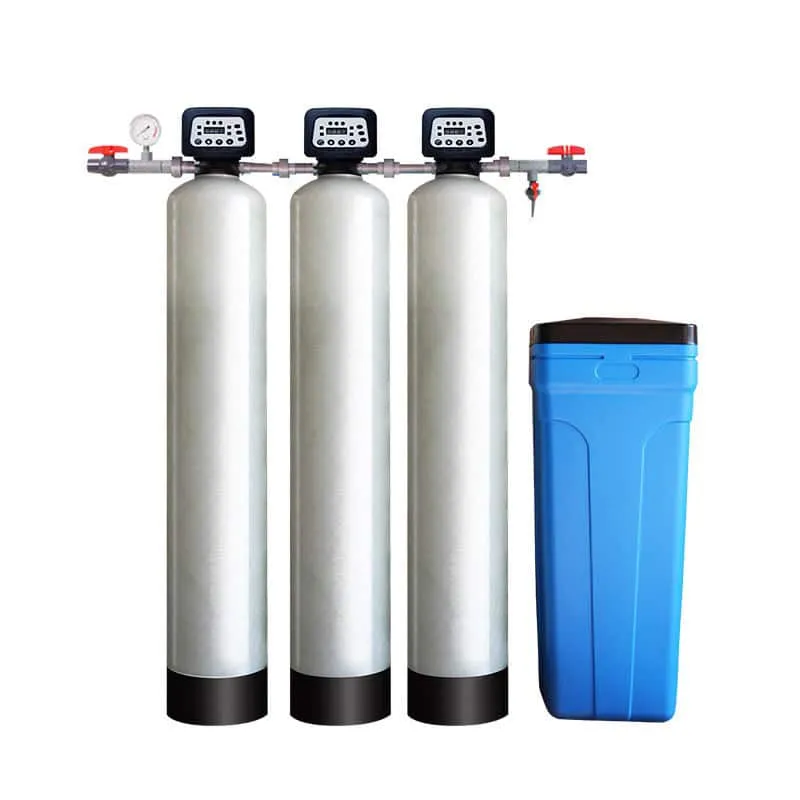
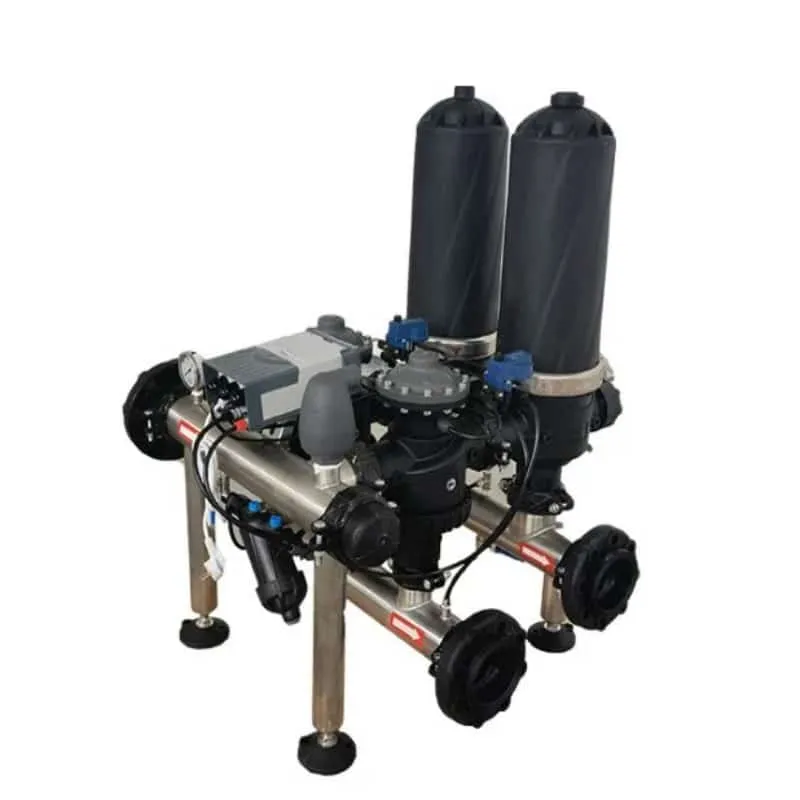
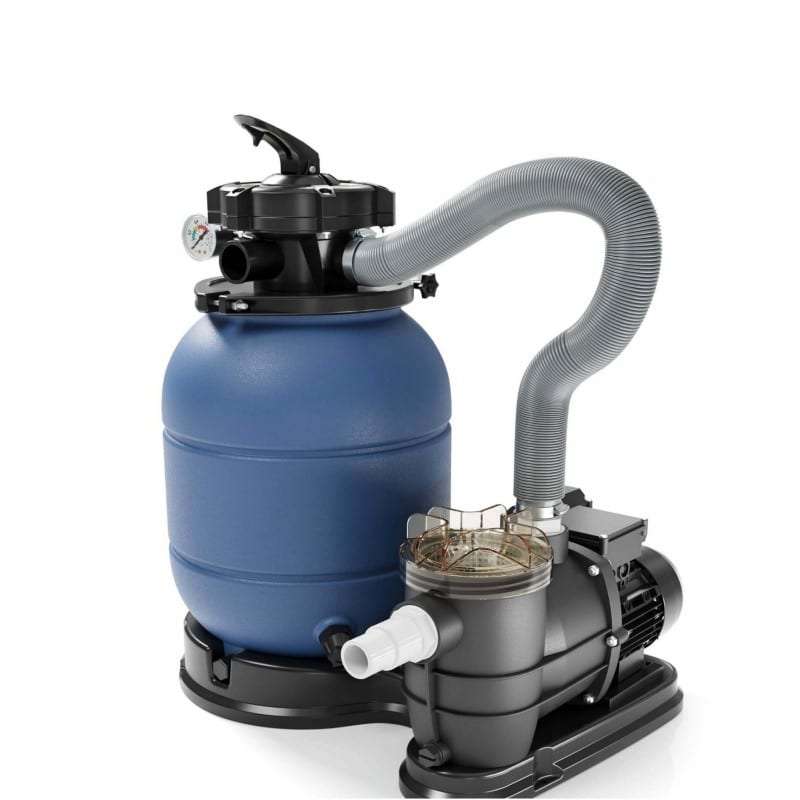
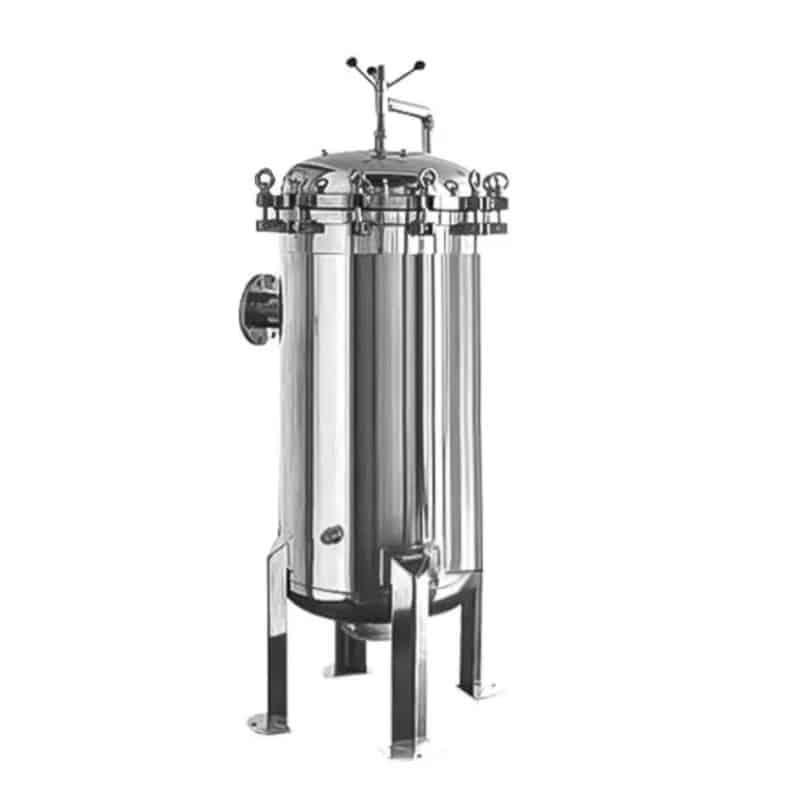
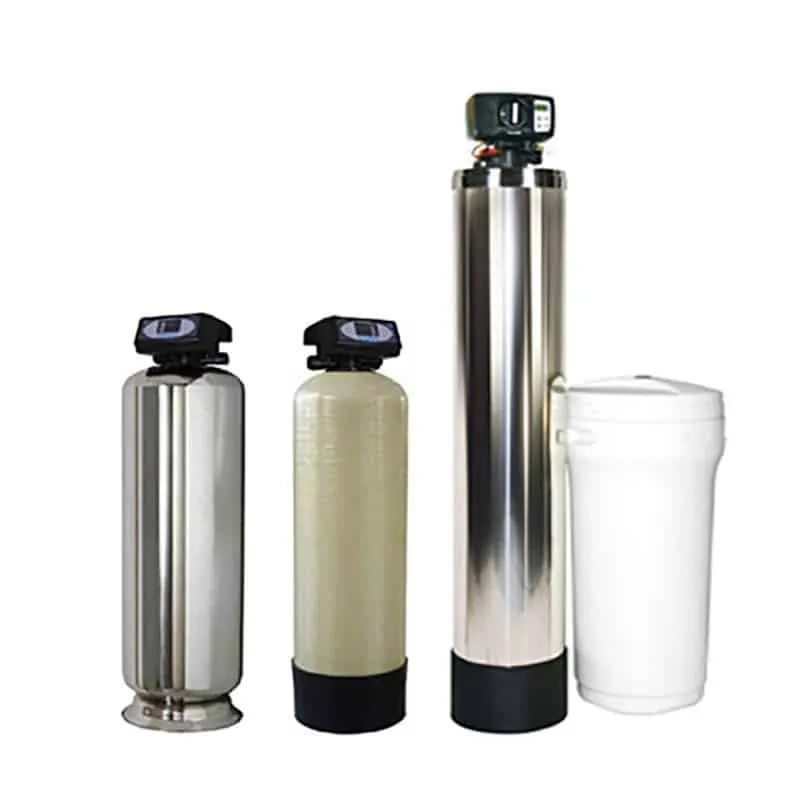
- Sand Filter: Removes large particles such as silt and suspended solids.
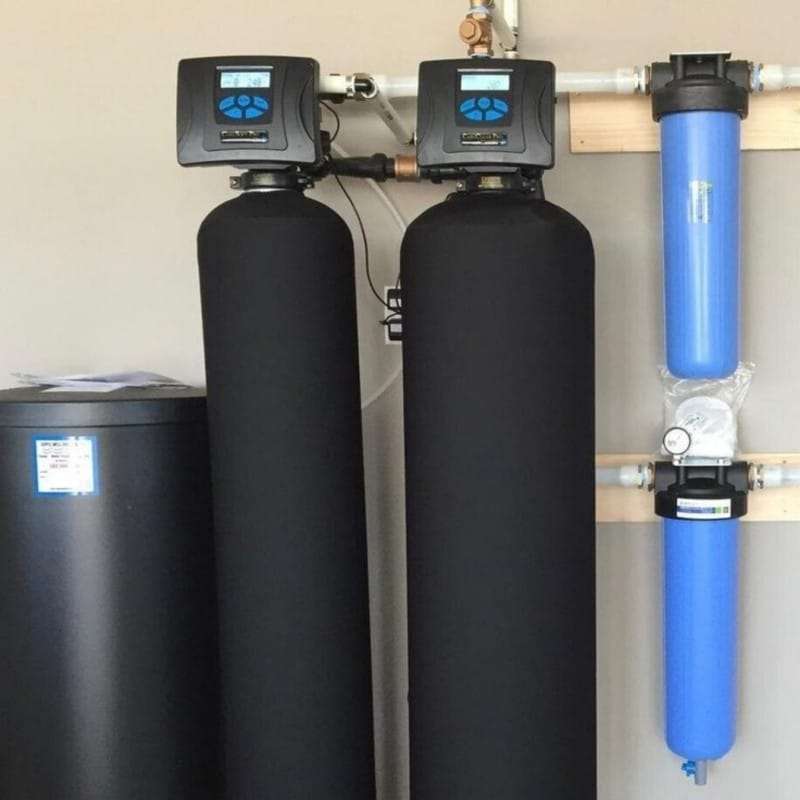
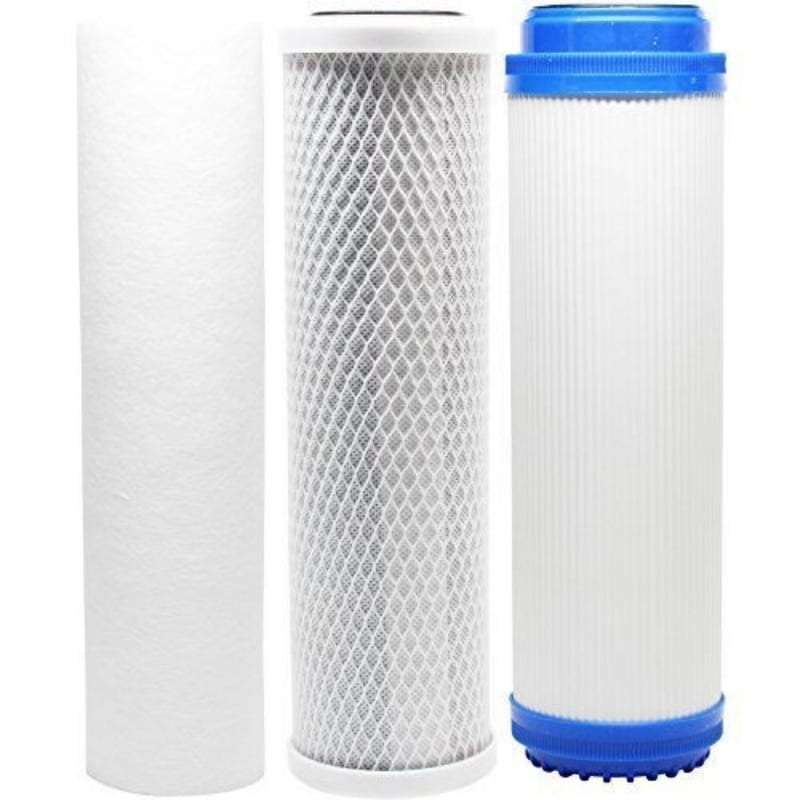
- Activated Carbon Filter: Adsorbs organic compounds, odors, and chlorine, enhancing sensory qualities.
- Advanced Treatment Stage:
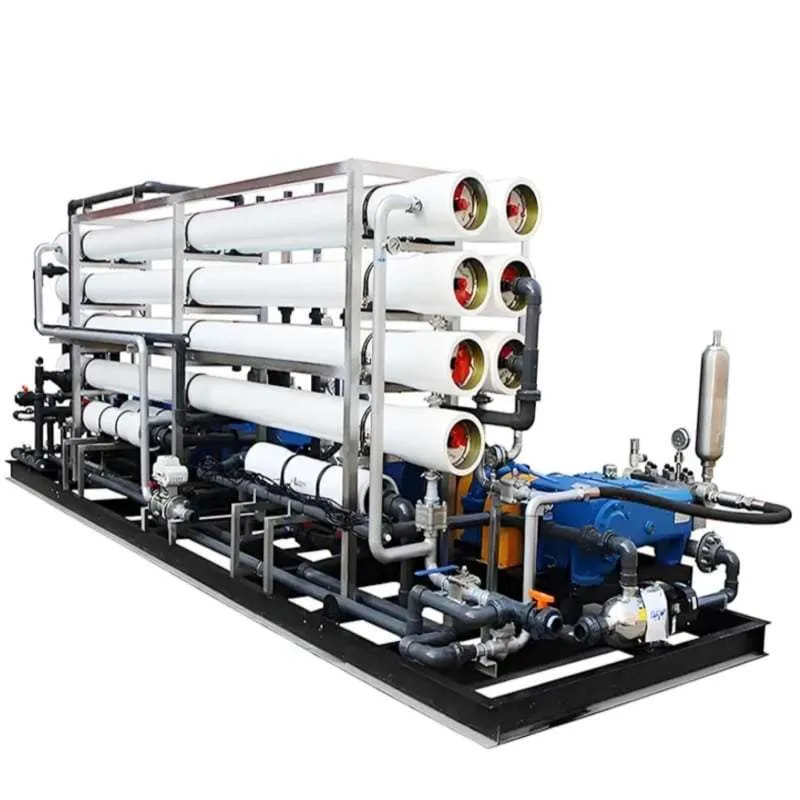
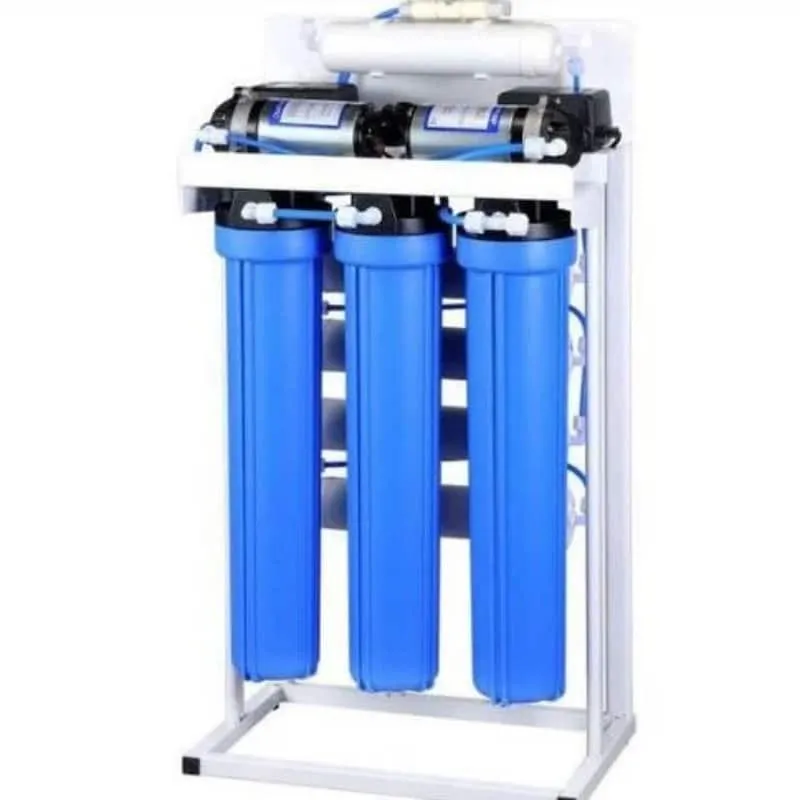
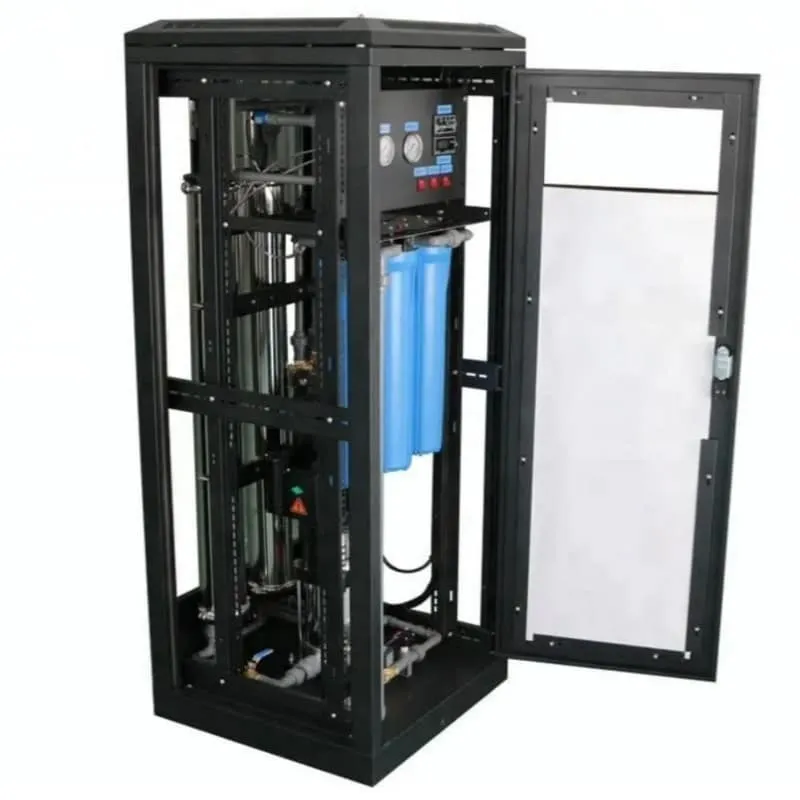
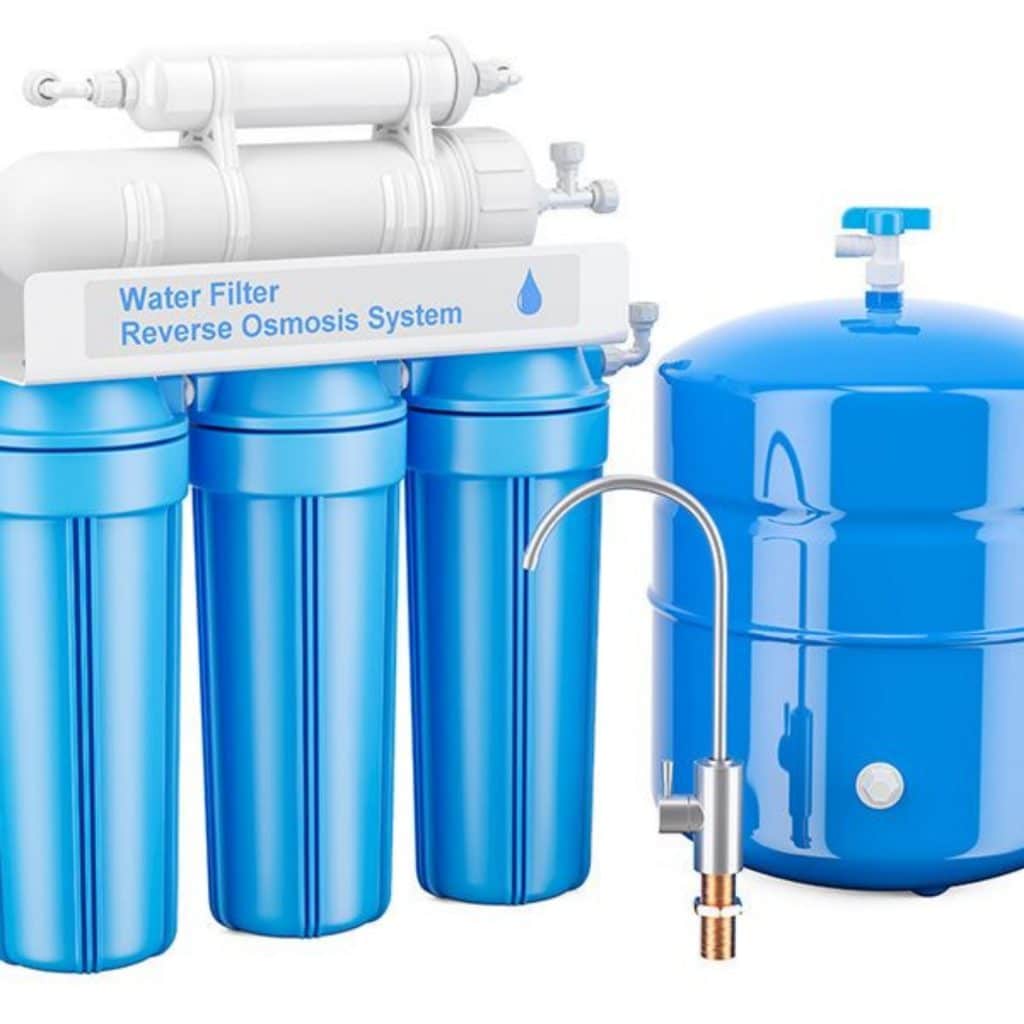
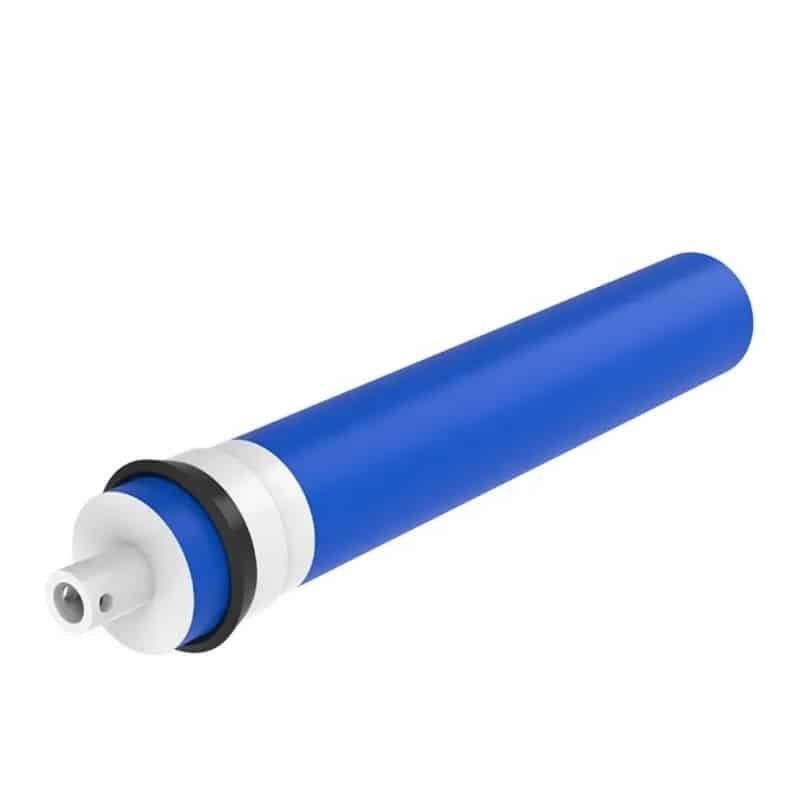
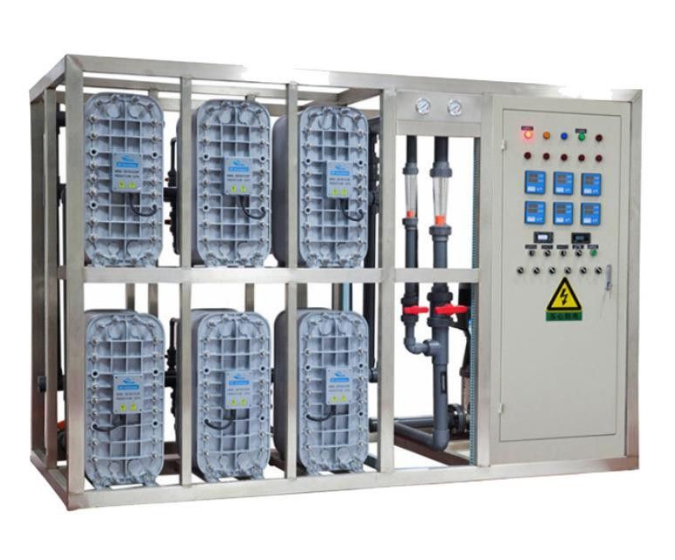
- Reverse Osmosis (RO) System: Utilizes high-pressure membrane technology to filter dissolved salts, heavy metals, and microorganisms, producing high-purity water.
- Ultraviolet (UV) Sterilization: Employs UV-C light to eliminate bacteria and viruses, ensuring water safety.
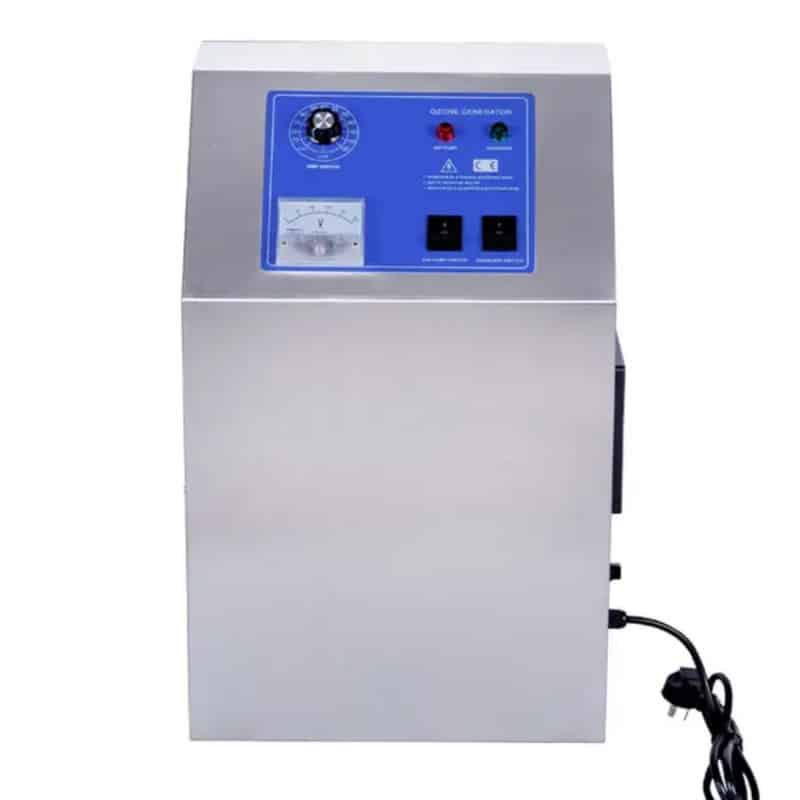
- Ozone Disinfection: Uses ozone’s strong oxidizing properties for secondary sterilization, preventing recontamination.
- Storage and Distribution Stage:
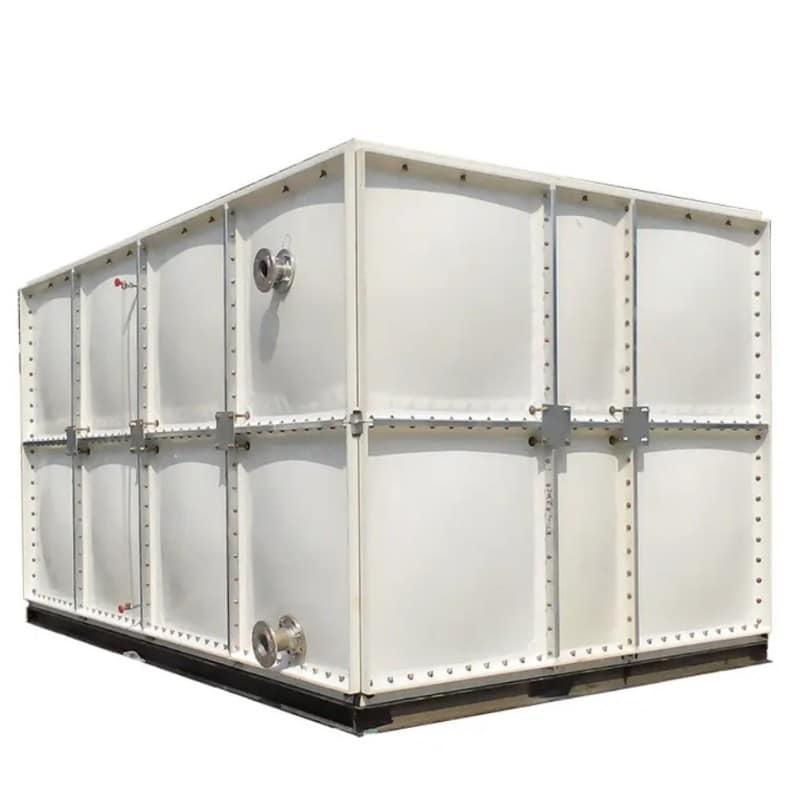
- Clean Water Storage Tank: Stores treated water in a sealed tank.
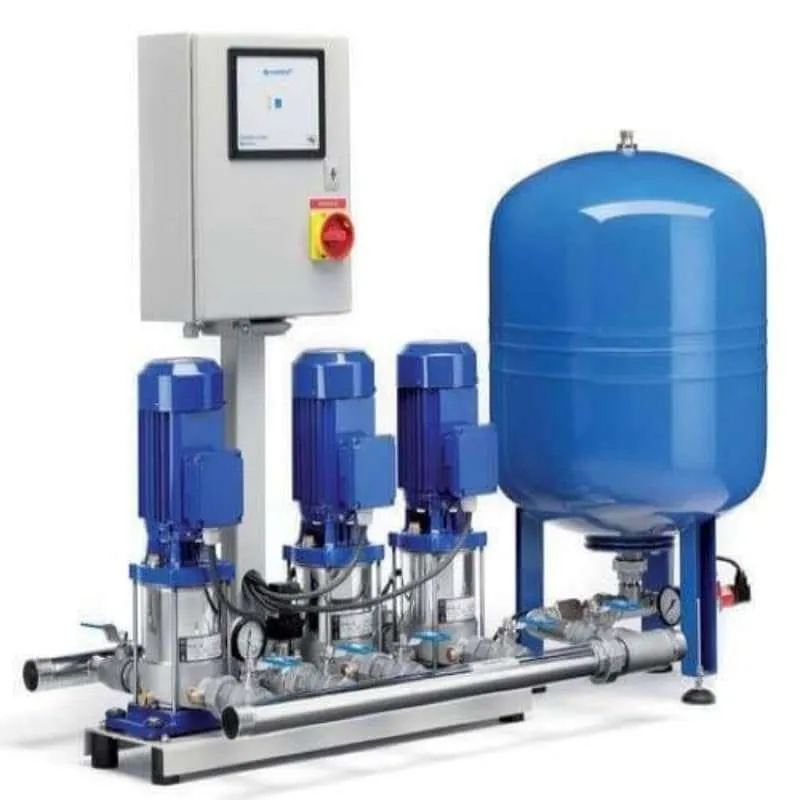
- Sterile Piping System: Distributes water to various production lines, maintaining sterility.
Project Parameters and Equipment Specifications
The following table outlines the key parameters and specifications of the water treatment system:
| Component | Specification |
|---|---|
| Sand Filter | Flow Rate: 50 m³/h; Filtration Precision: 5 microns; Material: Stainless Steel |
| Activated Carbon Filter | Flow Rate: 50 m³/h; Adsorption Capacity: 200 mg/g; Material: Activated Carbon |
| Reverse Osmosis System | Flow Rate: 40 m³/h; Recovery Rate: 75%; Membrane Type: Thin-Film Composite |
| UV Sterilizer | UV Dose: 40 mJ/cm²; Lamp Power: 100 W; Material: Quartz Glass |
| Ozone Generator | Ozone Output: 10 g/h; Power Consumption: 500 W; Material: Stainless Steel |
| Clean Water Storage Tank | Capacity: 100 m³; Material: Food-Grade Stainless Steel |
| Sterile Piping System | Diameter: DN100; Material: Food-Grade Stainless Steel; Sterilization Method: CIP |
Project Outcomes
Upon implementation, the water treatment system achieved the following results:
- Water Quality Compliance: The treated water consistently met WHO drinking water standards, ensuring product safety and quality.
- Operational Efficiency: The system operated continuously, meeting the manufacturer’s high production demands without interruptions.
- Real-Time Monitoring: Integrated online monitoring systems provided real-time data on water quality parameters, enabling proactive maintenance and ensuring compliance with health and safety standards.
- Environmental Sustainability: The system incorporated water recovery features, reducing wastewater discharge and promoting sustainable water use.
This project underscores the critical role of advanced water treatment solutions in the food and beverage industry, highlighting our company’s commitment to delivering high-quality, sustainable, and efficient water treatment systems tailored to our clients’ specific needs.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian