




Introduction
Semiconductor manufacturing is a highly intricate process that demands exceptional water quality and stringent management of wastewater. The industry relies on ultrapure water (UPW) for various stages, including wafer cleaning, etching, and rinsing. Simultaneously, it generates significant volumes of wastewater containing hazardous chemicals, necessitating effective treatment and reclamation systems.
Project Background
Our company was engaged by a leading semiconductor manufacturer to design and implement a comprehensive water treatment system for their new fabrication facility. The objective was to ensure a consistent supply of ultrapure water while efficiently treating and reclaiming wastewater to meet environmental regulations and support sustainable operations.
Project Requirements
The project encompassed the following key requirements:
- Ultrapure Water Supply: Establish a reliable and continuous supply of ultrapure water for semiconductor processing.
- Wastewater Treatment: Develop a system capable of treating diverse wastewater streams, including acidic, alkaline, and chemical-laden effluents.
- Water Reclamation: Implement a water reclamation process to recycle treated wastewater for non-critical applications, reducing overall water consumption.
- Compliance: Ensure all systems adhere to local environmental regulations and industry standards.
Technical Approach
Ultrapure Water Treatment System
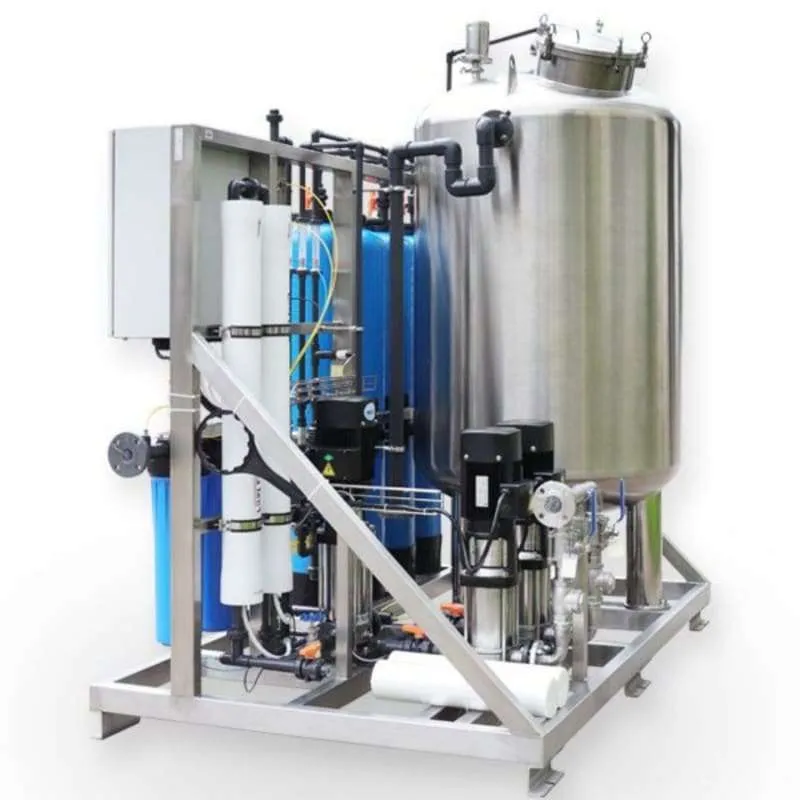
The ultrapure water system was designed with the following components:
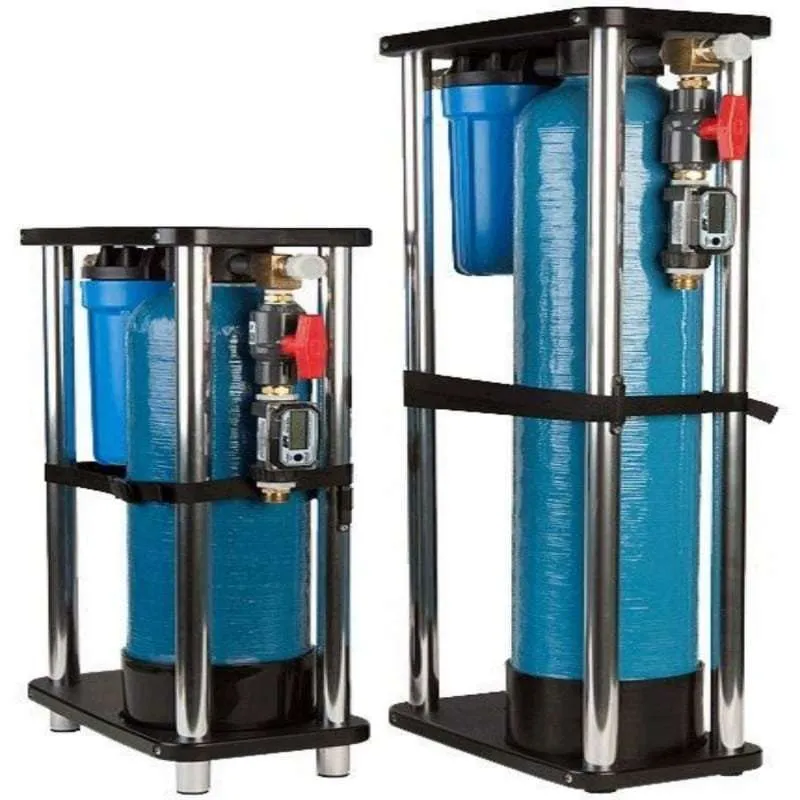
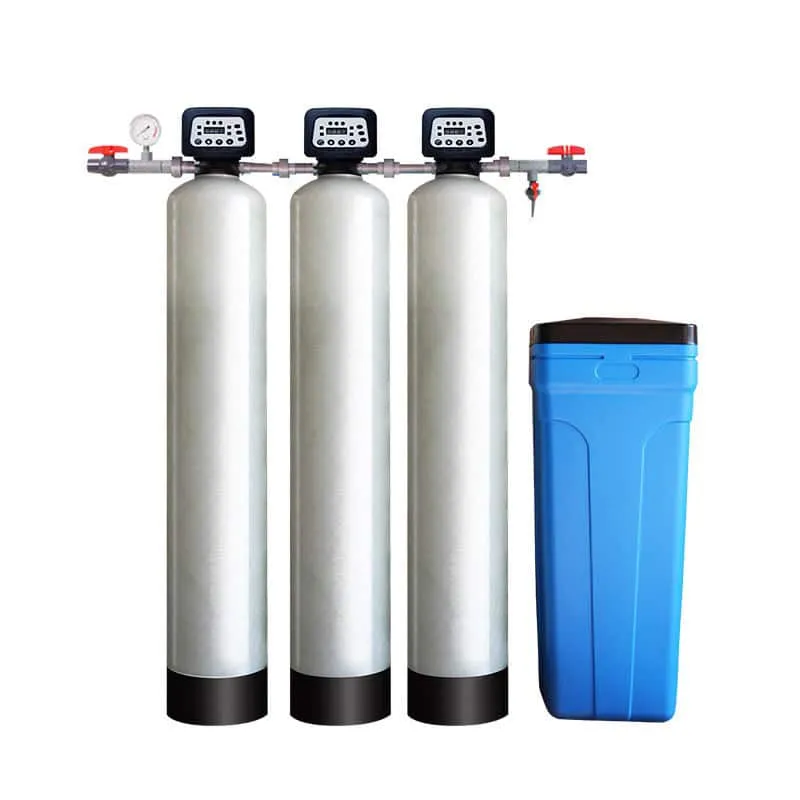
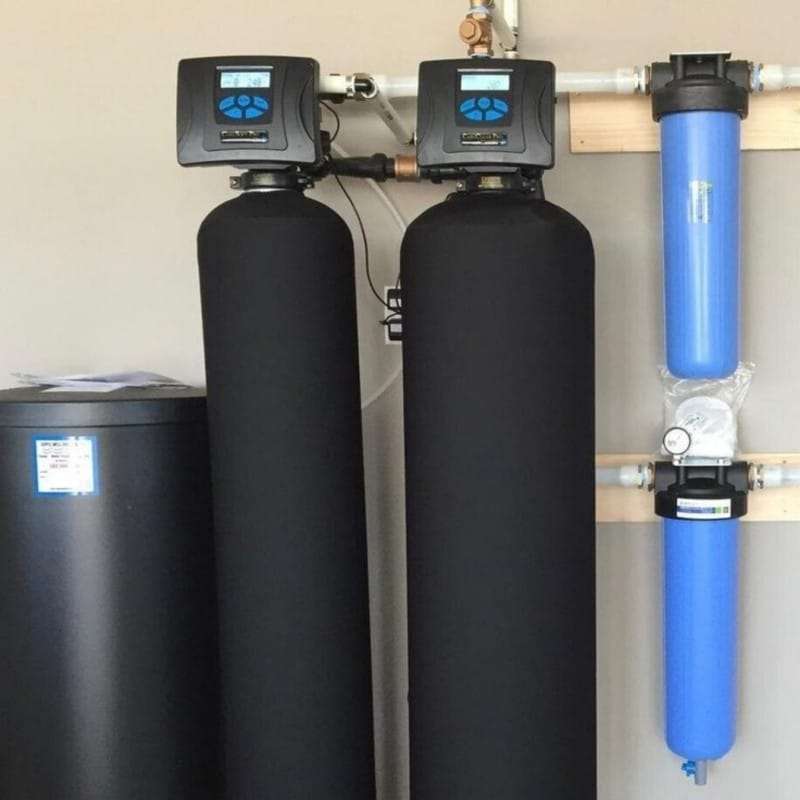
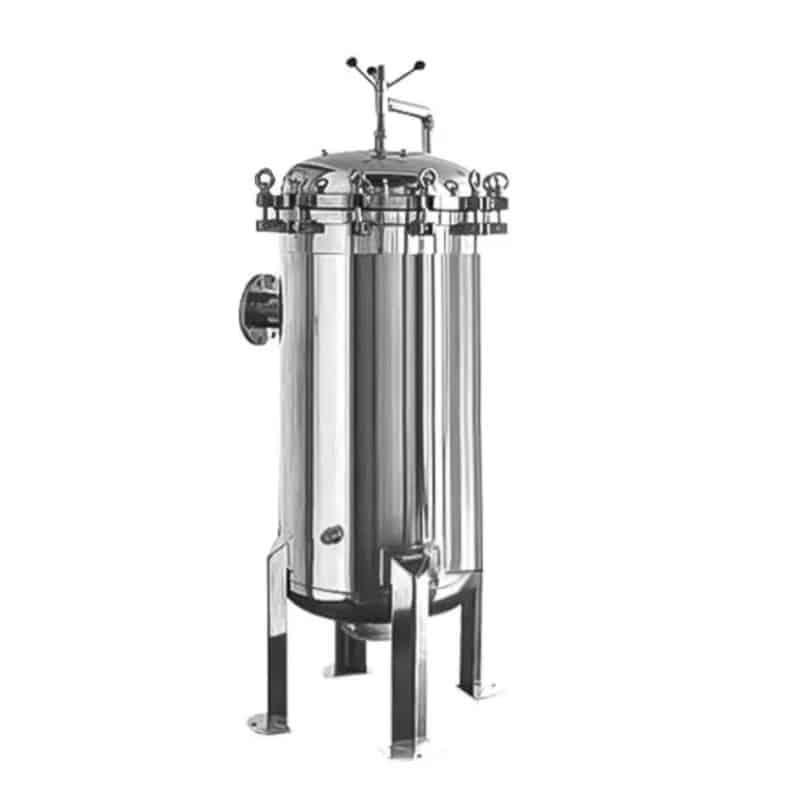
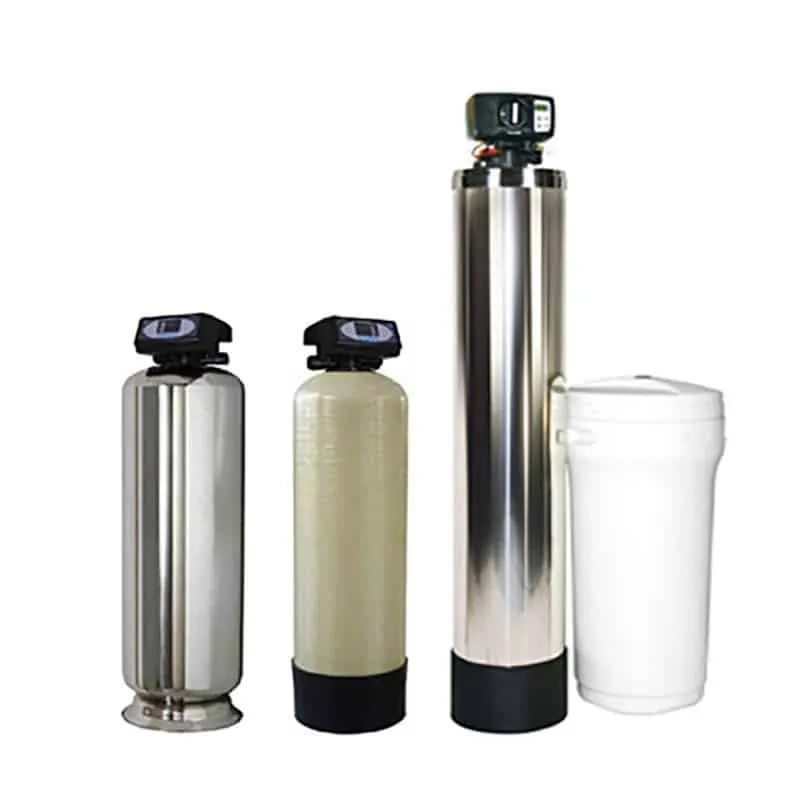
- Pretreatment: Multimedia filtration and activated carbon adsorption to remove suspended solids and organic contaminants.
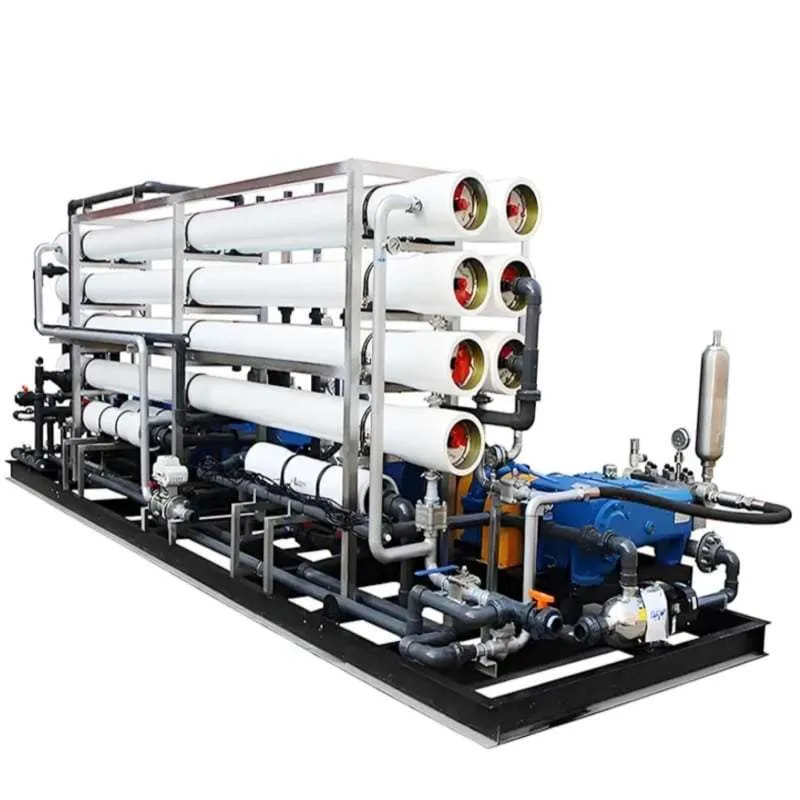
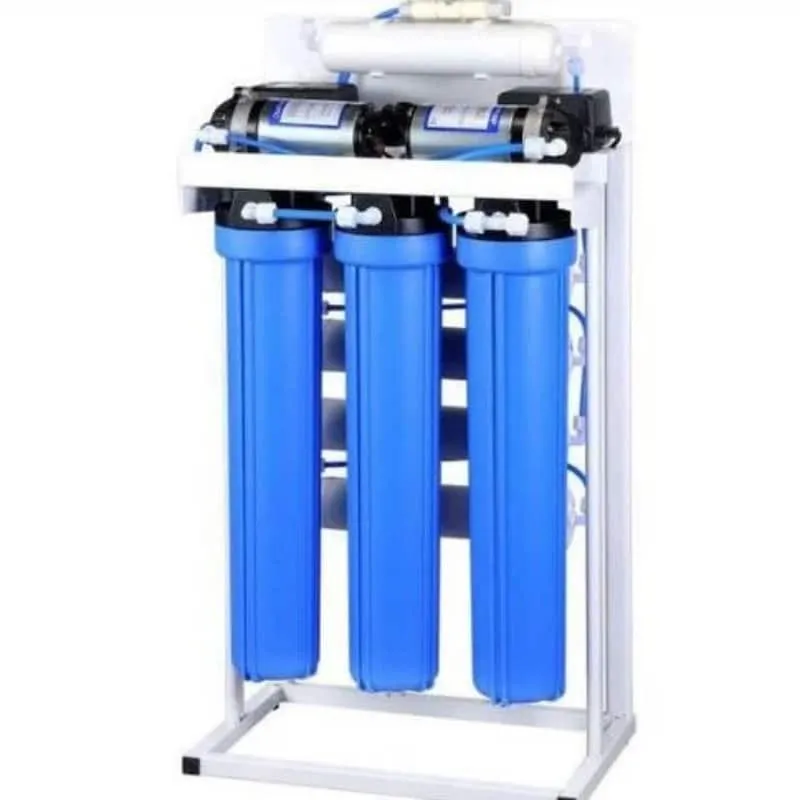
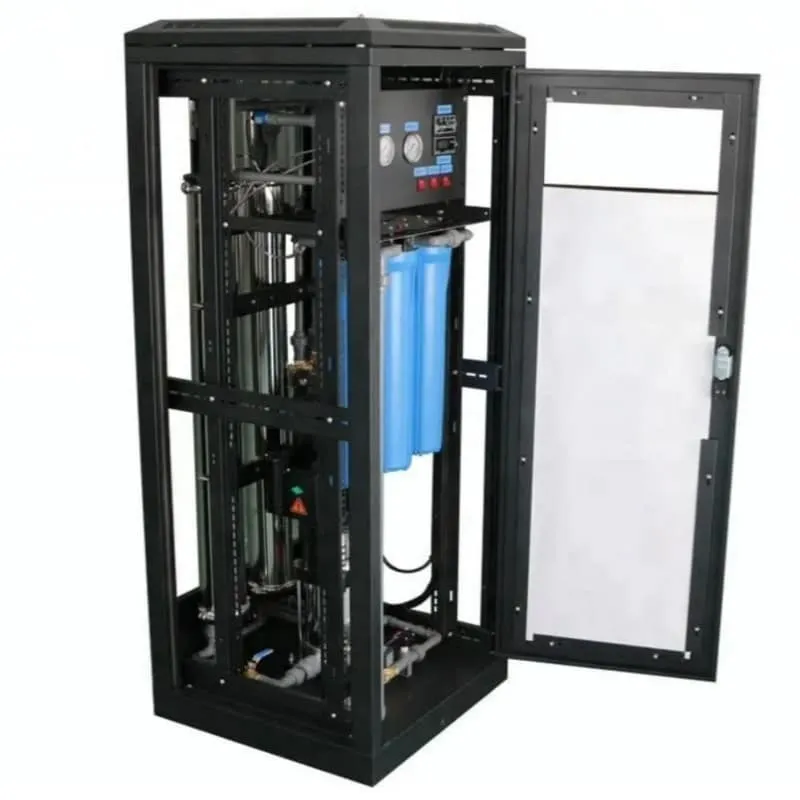
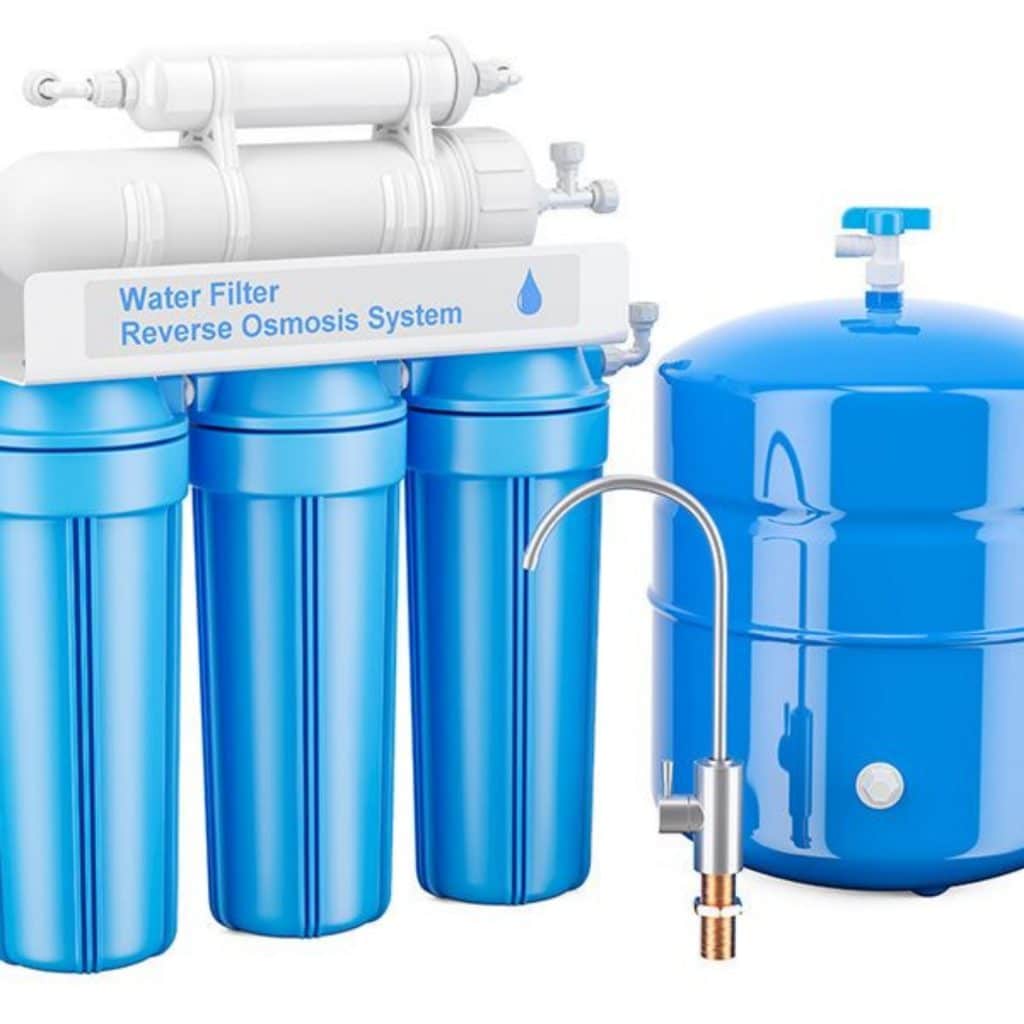
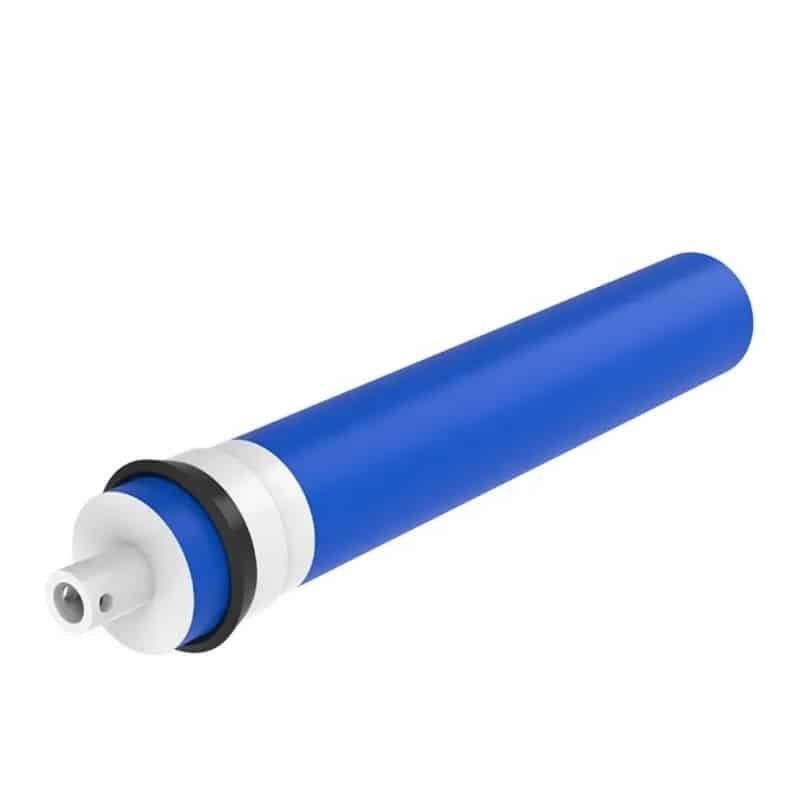
- Reverse Osmosis (RO): Two-pass RO units to desalinate and remove dissolved ions.
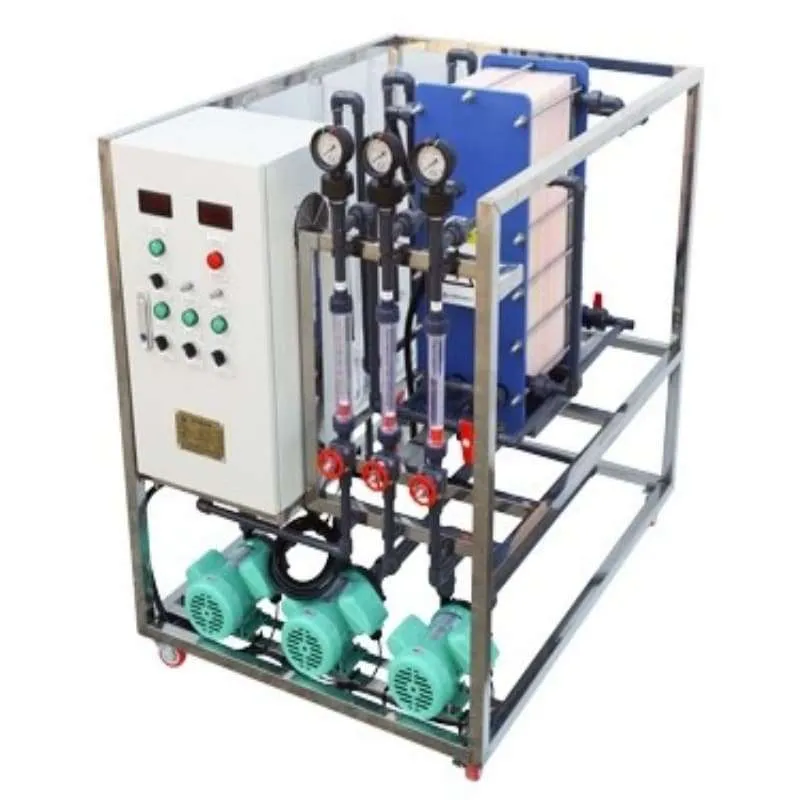
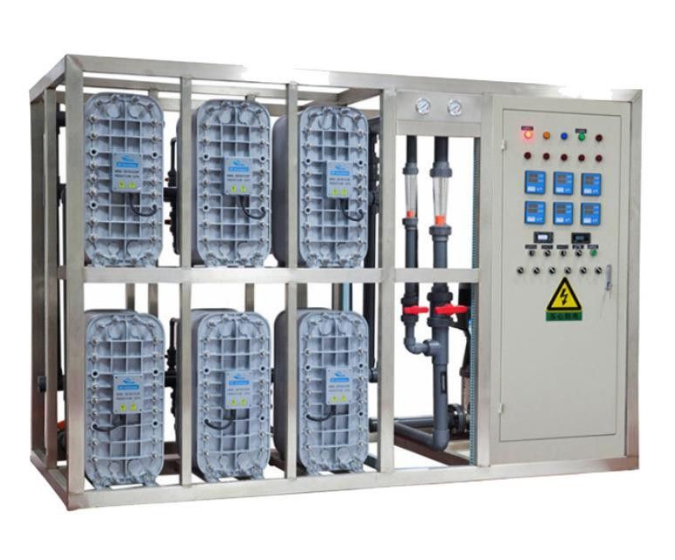
- Electrodeionization (EDI): Polishing stage to achieve ultrapure water quality by removing residual ions.
- Ultraviolet (UV) Disinfection: Final disinfection to eliminate microbial contaminants.
Wastewater Treatment and Reclamation
The wastewater treatment system was designed to handle various effluent streams:
- Acidic Wastewater: Neutralization tanks to adjust pH levels.
- Alkaline Wastewater: Neutralization tanks to adjust pH levels.
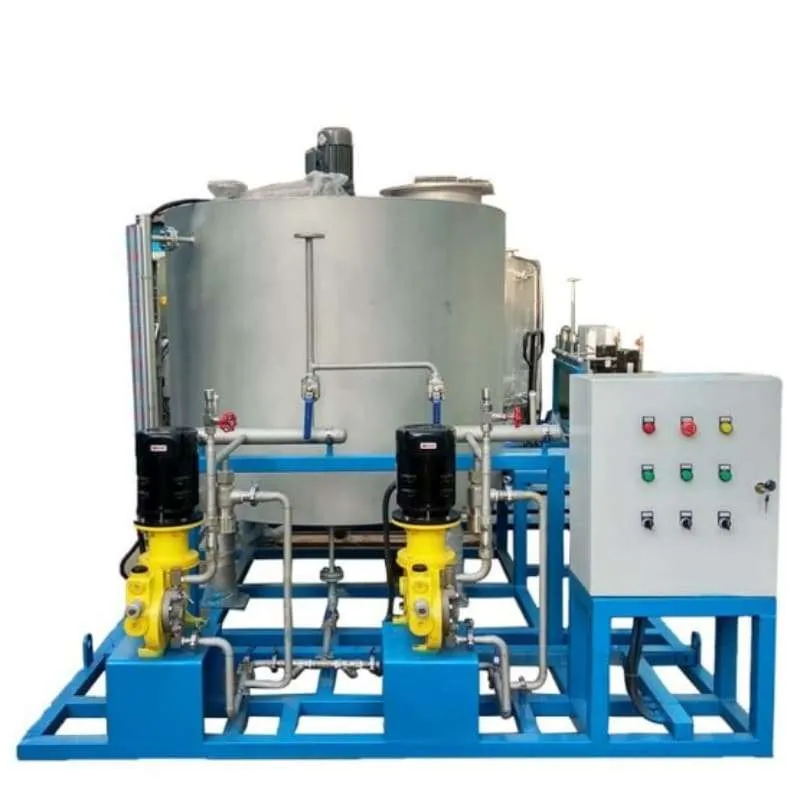
- Chemical Wastewater: Chemical precipitation and flocculation units to remove heavy metals and other contaminants.
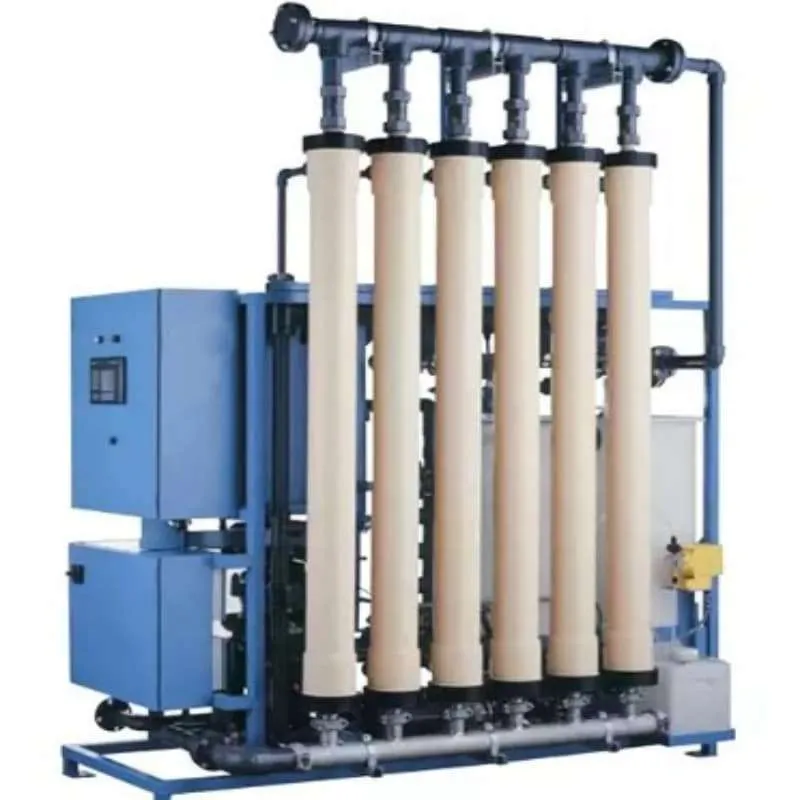
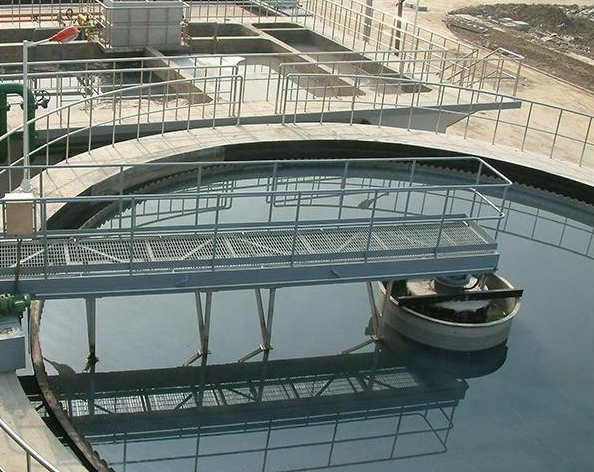
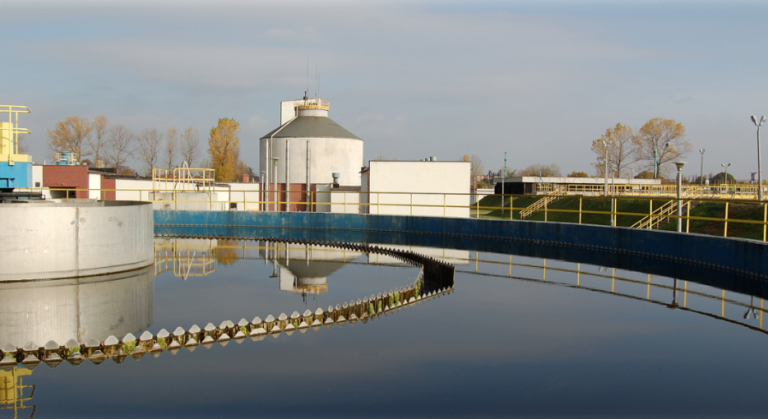
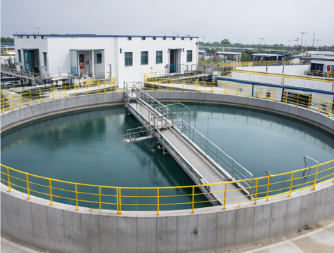
- Reclamation: Membrane bioreactors (MBR) followed by RO units to treat and reclaim wastewater for non-critical uses such as cooling and cleaning.
Equipment Specifications
The following table outlines the key equipment specifications for the water treatment and reclamation systems:
| Equipment Type | Specifications |
|---|---|
| Multimedia Filters | Flow Rate: 100 m³/h; Filtration Media: Anthracite, Sand, Gravel |
| Activated Carbon Filters | Flow Rate: 100 m³/h; Media: Granular Activated Carbon |
| Reverse Osmosis Units | Capacity: 50 m³/h; Membrane Type: Thin-Film Composite; Recovery Rate: 75% |
| Electrodeionization Units | Capacity: 50 m³/h; Voltage: 1.2 kV; Current Density: 20 A/m² |
| UV Disinfection Units | UV Dose: 40 mJ/cm²; Lamp Type: Low-Pressure Mercury Vapor |
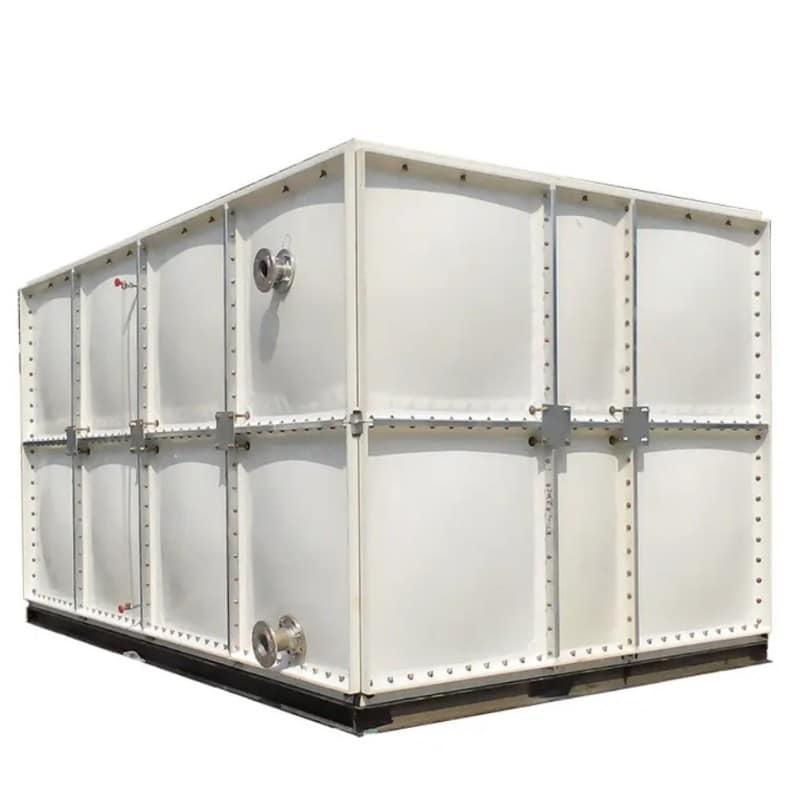
| Neutralization Tanks | Capacity: 10 m³; Material: FRP; pH Range: 2-12 |
| Chemical Precipitation Units | Capacity: 10 m³/h; Chemical Dosing: Alum, Lime; Flocculation Time: 30 min |
| Membrane Bioreactors | Capacity: 20 m³/h; Membrane Type: Hollow Fiber; Flux Rate: 20 LMH |
| RO Units for Reclamation | Capacity: 20 m³/h; Membrane Type: Thin-Film Composite; Recovery Rate: 80% |
Project Outcomes
The implementation of the water treatment and reclamation systems resulted in:
- Consistent Ultrapure Water Supply: The facility achieved a stable supply of ultrapure water, meeting the stringent requirements of semiconductor manufacturing processes.
- Effective Wastewater Treatment: All wastewater streams were treated to comply with environmental standards, minimizing the discharge of harmful substances.
- Water Reclamation Success: Approximately 40% of treated wastewater was successfully reclaimed for non-critical applications, significantly reducing the facility’s freshwater consumption.
- Regulatory Compliance: The systems ensured adherence to local environmental regulations, avoiding potential fines and supporting the company’s commitment to sustainability.
Conclusion
This case study demonstrates the critical role of advanced water treatment and reclamation systems in semiconductor manufacturing. By integrating state-of-the-art technologies and adhering to stringent environmental standards, our company successfully delivered a solution that met the client’s requirements for water quality, wastewater management, and sustainability.
For more information on our water treatment solutions for the semiconductor industry, please contact us.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian