

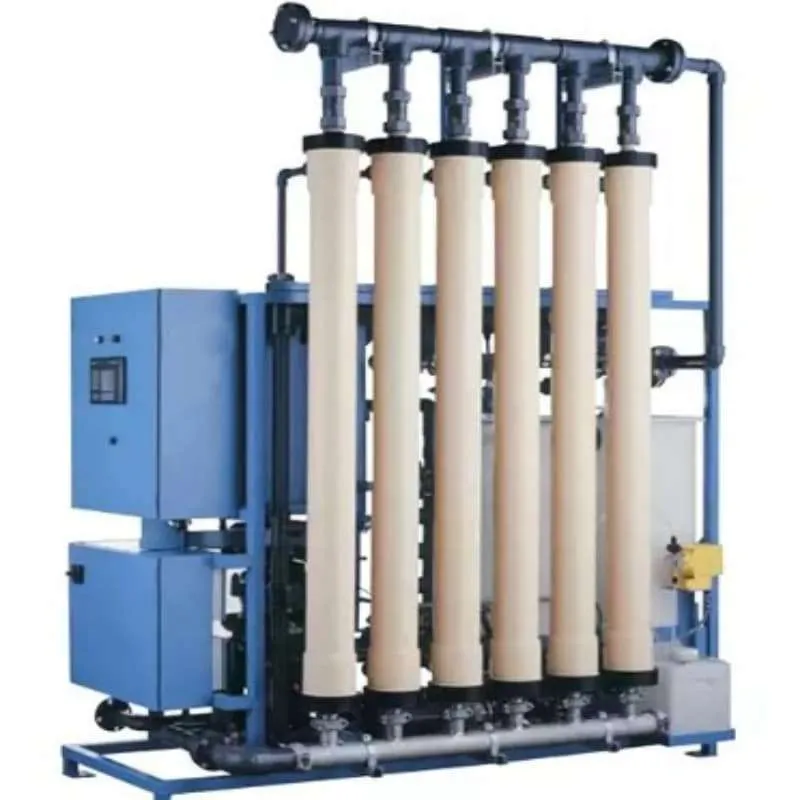
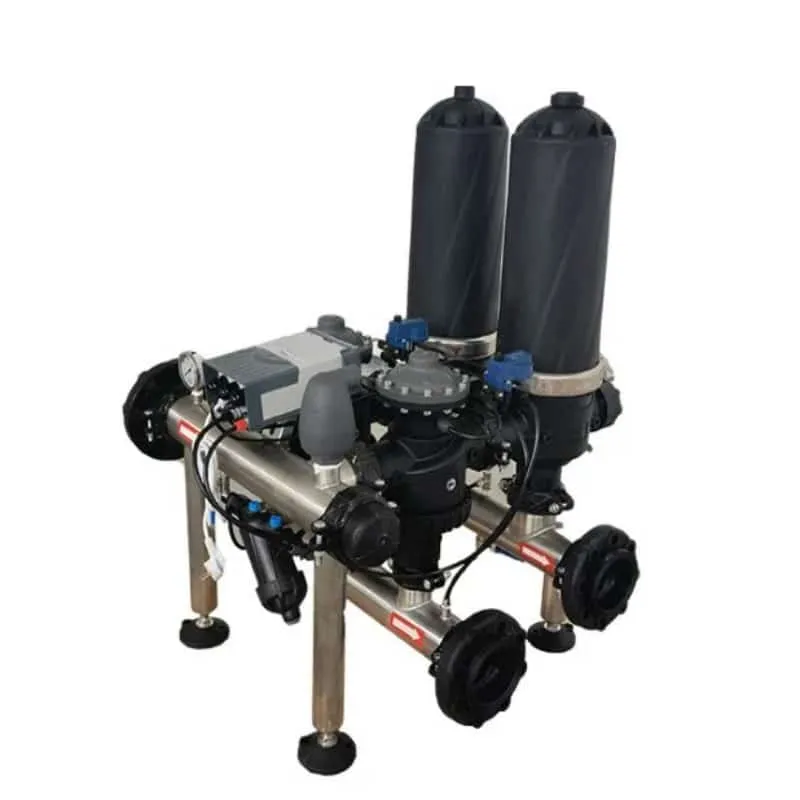
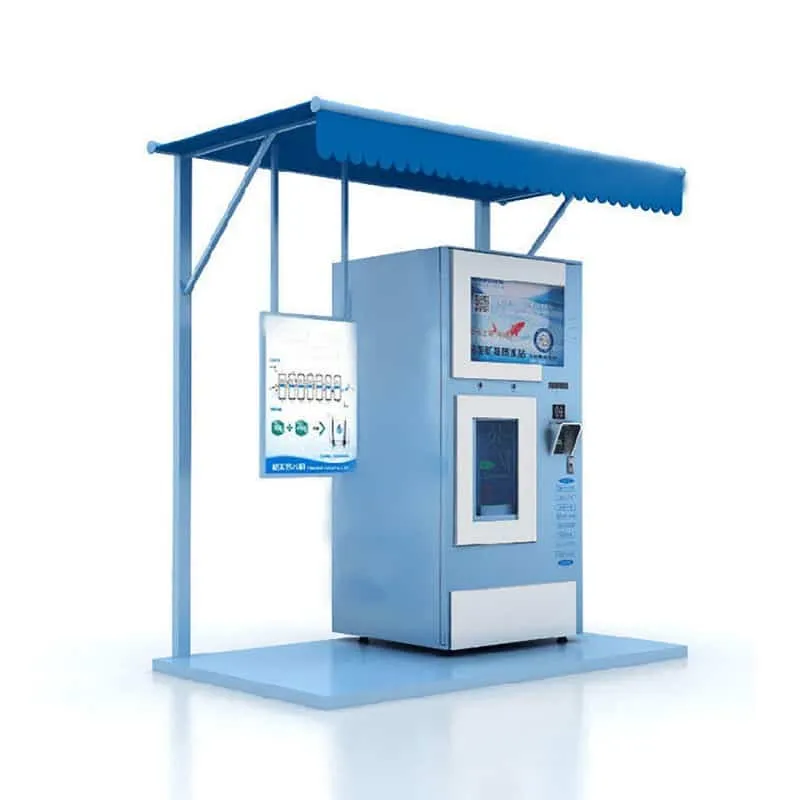
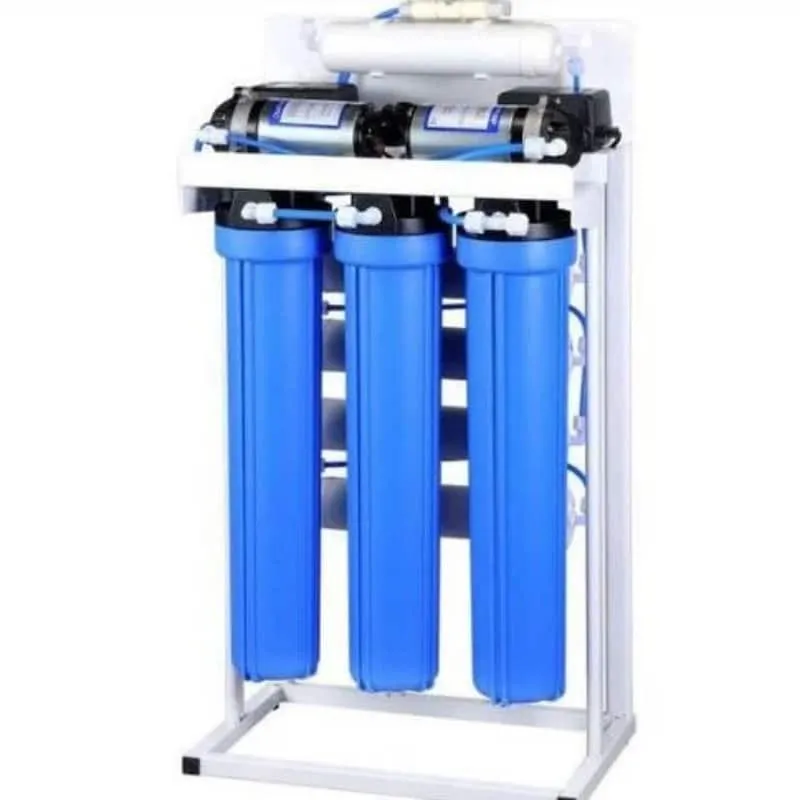
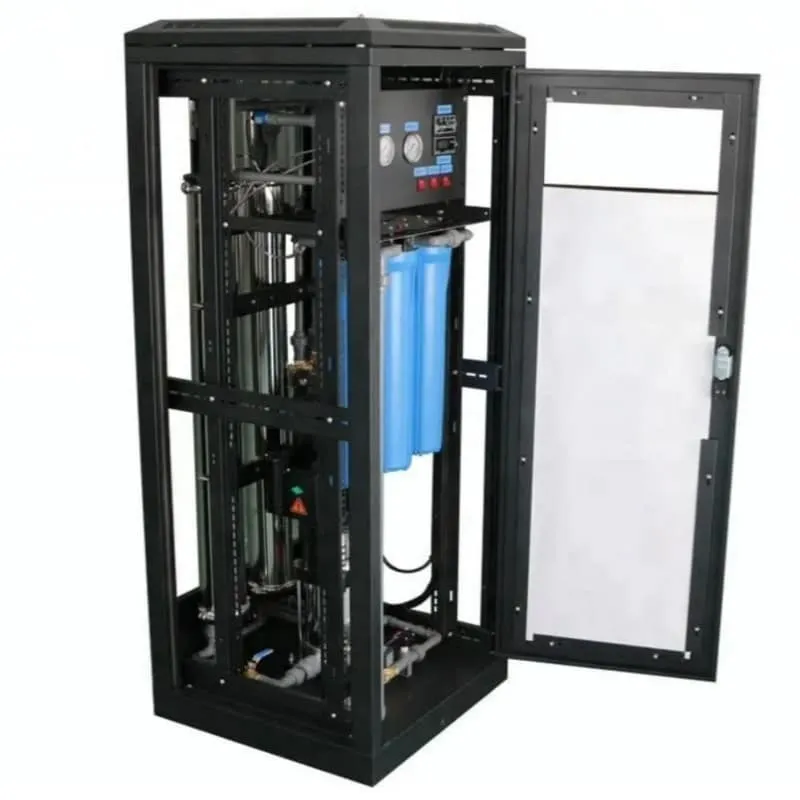
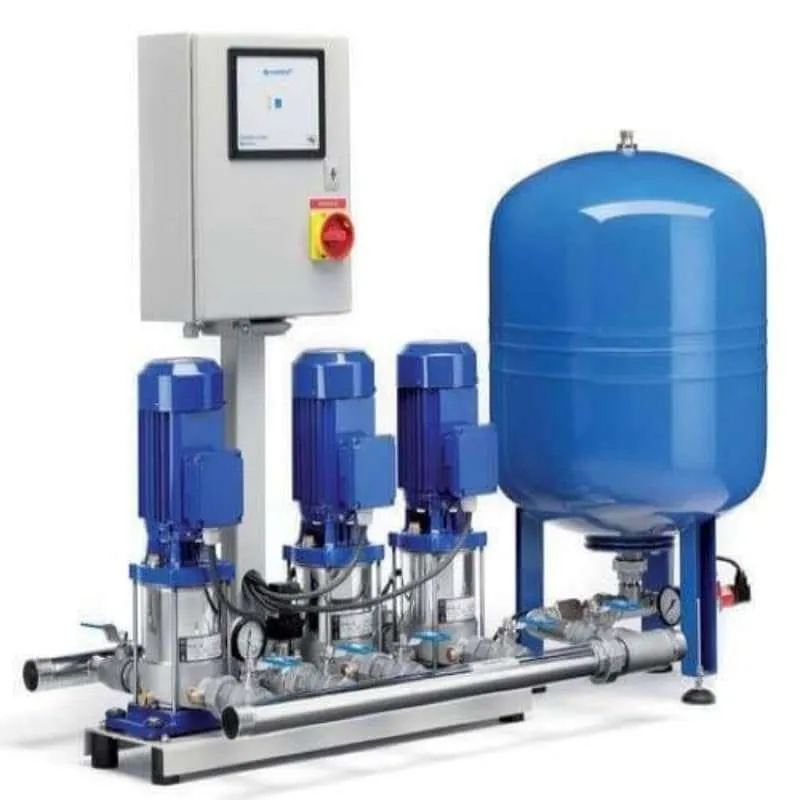

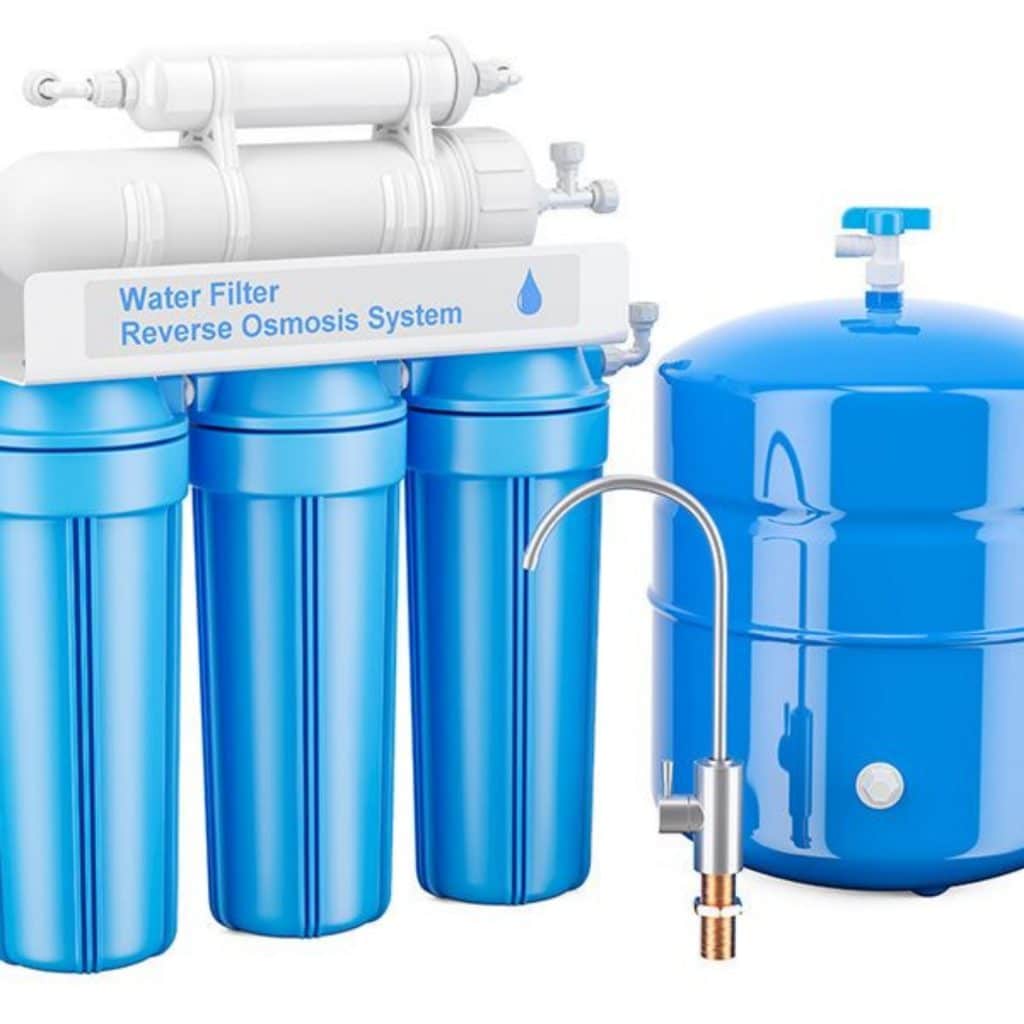


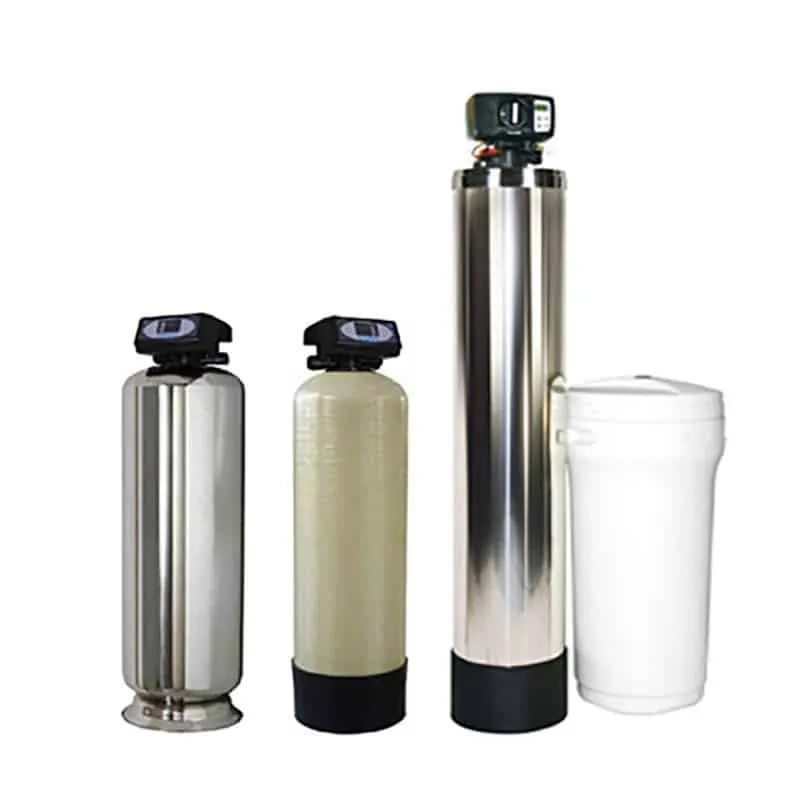
Industrial water treatment shapes your facility’s efficiency, safety, and operational costs. When you select a water treatment equipment supplier, you directly influence water quality and your ability to meet strict regulatory standards. You face diverse challenges, such as regulatory pressures, aging infrastructure, complex contaminants, high energy use, and rising operational costs. The right suppliers bring advanced technologies and expert support, helping you manage water resources, remain compliant, and build sustainable processes. Water impacts every aspect of your operation—from compliance to cost—so you need solutions designed for today’s industrial demands.
Key Takeaways
Selecting the right water treatment supplier impacts your facility’s efficiency and compliance with regulations.
Veolia, SUEZ, and Ecolab are leaders in providing advanced water treatment technologies tailored for various industries.
Invest in suppliers that offer customized solutions to address specific water challenges in your operations.
Consider the total cost of ownership, including installation and maintenance, when evaluating water treatment equipment.
Ensure your chosen supplier supports sustainability initiatives to reduce environmental impact and operational costs.
Look for suppliers with strong global support and a proven track record in your industry for reliable service.
Regular maintenance and monitoring of water treatment systems are crucial for compliance and operational efficiency.
Stay informed about evolving regulations to ensure your water treatment solutions meet all necessary standards.
Top Industrial Water Treatment Equipment Companies

Veolia
Overview
You encounter Veolia as one of the most recognized companies in the water treatment market. Veolia stands out among suppliers for its global reach and deep expertise in industrial water treatment equipment. The company supports a wide range of industries, including pharmaceuticals, automotive, energy, and food processing. Veolia’s commitment to sustainability and innovation positions it as a leader in the water treatment systems market. You benefit from their ability to address complex water and wastewater challenges, ensuring compliance and operational efficiency.
Main Products
Veolia offers a comprehensive portfolio of water treatment equipment and solutions. You can access:
Advanced filtration systems for process water treatment and purification.
Reverse osmosis membranes designed for high-performance industrial applications.
Wastewater treatment plants engineered for large-scale operations.
Boiler feed water treatment systems that optimize energy use and protect equipment.
Digital water management platforms for real-time monitoring and control.
Core water treatment equipment tailored for specific industrial needs.
Industrial Strengths
Veolia’s strengths lie in its ability to deliver customized solutions for diverse industrial sectors. You gain access to:
Advanced water treatment technologies for the pharmaceutical sector, ensuring regulatory compliance.
Solutions that enhance operational efficiency and support sustainability initiatives.
Expertise in managing product quality, safety, and variability in wastewater.
Sustainable water and wastewater treatment systems for the automotive industry, improving operational efficiency and profitability.
Technologies that maintain water quality and ensure compliance with stringent environmental standards.
Veolia’s mastery of the water cycle allows you to maximize profitability and sustainability in your industrial operations.
SUEZ
Overview
SUEZ ranks among the top water treatment equipment suppliers worldwide. You rely on SUEZ for innovative water treatment solutions and a strong global presence. The company serves over 50,000 industrial and municipal clients in more than 100 countries. SUEZ’s focus on sustainability and advanced water treatment technologies makes it a preferred choice for multinational manufacturers seeking reliable water quality solutions.
Main Products
SUEZ provides a broad range of water treatment equipment and systems, including:
Membranes for filtration and reverse osmosis applications.
Wastewater treatment systems designed for industrial and municipal use.
Boiler feed water treatment solutions that protect critical infrastructure.
Digital water management tools for predictive analytics and process optimization.
Water treatment plants engineered for efficiency and compliance.
Industrial Strengths
SUEZ leads the industry with its commitment to sustainable water treatment solutions. You benefit from:
Innovative ‘waste-to-value’ technologies that transform wastewater by-products into energy and materials.
Tailored solutions for specific water and wastewater challenges, promoting efficiency and sustainability.
Comprehensive chemical and equipment solutions for process water treatment.
Predictive analytics that enhance productivity and reduce operational costs.
Metric | Value |
|---|---|
Employees Worldwide | 90,000 |
Countries of Operation | Over 100 |
Industrial and Municipal Clients | Over 50,000 |
Employees in Water Technologies | Over 10,000 |
SUEZ’s global presence ensures you receive consistent support, improved water quality, and efficient waste management systems wherever your operations are located.
Ecolab
Overview
Ecolab stands out as a trusted partner in the industrial water treatment systems market. You turn to Ecolab for sustainable water treatment equipment and solutions that drive operational excellence. The company’s expertise spans food and beverage, energy, manufacturing, and healthcare sectors. Ecolab’s approach to water stewardship and net-positive water impact sets it apart from other companies and manufacturers.
Main Products
Ecolab delivers a wide array of water treatment equipment, including:
Membranes for advanced filtration and purification.
Boiler feed water treatment systems that improve efficiency and reduce downtime.
Wastewater treatment systems for industrial and municipal clients.
Water treatment plants designed for large-scale operations.
Digital water management platforms that optimize water use and monitor water quality.
Industrial Strengths
Ecolab’s strengths center on sustainability and collaboration. You benefit from:
Water stewardship strategies that aim for a net-positive water impact.
Solutions that enhance water-use efficiency and support local watershed protection.
Collaboration with stakeholders to address shared water challenges.
Sustainable water strategies that yield significant returns on investment.
Experience in water management that supports both your operations and those of your partners.
Ecolab’s three-pathway strategy—efficiency, reuse, and protection—helps you achieve your sustainability goals while maintaining high water quality standards.
Xylem
Overview
You find Xylem among the most innovative companies in the industrial water treatment equipment market. Xylem focuses on solving complex water challenges for industrial clients worldwide. The company delivers advanced water treatment solutions that address both water scarcity and quality. You benefit from their expertise in designing systems for water reuse, purification, and wastewater treatment systems. Xylem’s commitment to sustainability and technology leadership makes it a preferred partner for industries seeking reliable water treatment equipment.
Main Products
Xylem offers a comprehensive range of water treatment equipment for industrial applications. You can select from:
Advanced filtration systems for process water and wastewater.
Membranes for reverse osmosis, nanofiltration, and ultrafiltration.
Boiler feed water treatment systems that protect your assets and optimize energy use.
Disinfection technologies, including ultraviolet and ozone systems.
Digital monitoring platforms for real-time water quality management.
Xylem’s portfolio covers every stage of the water cycle, from intake to discharge. You gain access to robust solutions that ensure compliance and operational efficiency.
Industrial Strengths
You experience Xylem’s strengths through its focus on technological advancement and energy efficiency. The company leads with innovative processes that eliminate the need for membranes in some applications, reducing high salinity brine discharge and saving energy. Xylem also introduced the world’s first sequential Advanced Oxidation Process (AOP) system for large populations, which enhances contaminant removal.
Advancement Description | Link |
|---|---|
Innovative processes without membranes to prevent high salinity brine discharge and save energy. | |
Implementation of the world’s first sequential Advanced Oxidation Process (AOP) system for large populations, enhancing contaminant removal. |
You can cut operating costs by 25% and reduce energy use by 25% with Xylem’s water treatment equipment. The company’s performance metrics show a strong commitment to value, even as it continues to innovate.
Metric | Xylem’s Performance | Industry Median (Water Supply) |
|---|---|---|
Gross Margin | 38.78% | 61.8% |
Adjusted Operating Margin | 18.9% | 26.8% |
Net Profit Margin | 10.7% | 17.9% |
Xylem’s focus on energy savings and advanced water treatment solutions helps you meet your industrial water goals while supporting sustainability.
Aquatech
Overview
You recognize Aquatech as a leader in industrial water treatment equipment and water treatment solutions. Aquatech specializes in advanced technologies for water purification, desalination, and zero liquid discharge. The company serves a diverse range of industries, including food and beverage, manufacturing, and critical minerals recovery. Aquatech’s commitment to innovation and energy efficiency sets it apart from other suppliers.
Main Products
Aquatech provides a robust selection of water treatment equipment for industrial use:
RecovOAR® Reverse Osmosis systems for high-efficiency water recovery.
HERO® systems that deliver over 95% water recovery with minimal chemical use.
Hybrid ZLD (Zero Liquid Discharge) systems that combine membrane and thermal technologies.
Boiler feed water treatment systems designed for reliability and cost savings.
Advanced membranes for challenging water sources and industrial processes.
You can rely on Aquatech’s solutions to address complex water and wastewater challenges while optimizing operational costs.
Industrial Strengths
Aquatech stands out for its energy-efficient water treatment equipment and innovative solutions. You benefit from technologies that reduce energy demand by up to 60%, such as RecovOAR® Reverse Osmosis. The HERO® system achieves high water recovery rates and minimizes chemical use, which lowers your operational costs. Hybrid ZLD systems integrate membrane and thermal processes, making them ideal for treating high-TDS wastewater.
RecovOAR® Reverse Osmosis reduces energy demand by up to 60%.
HERO® system achieves over 95% recovery with minimal chemicals.
Hybrid ZLD Systems optimize energy use for high-TDS wastewater.
Aquatech’s expertise spans multiple industries:
Industry | Description |
|---|---|
Food & Beverage | Reliable solutions to manage process water for dairies, wineries, breweries, and food processing. |
Manufacturing | Customized solutions to transform water usage, reduce consumption, and comply with regulations. |
Critical Minerals Recovery | Innovative approaches to ensure water security and support essential minerals recovery. |
Aquatech’s focus on energy efficiency and high-performance water treatment equipment helps you achieve sustainability and compliance in your industrial operations.
Evoqua
Overview
You turn to Evoqua for reliable and advanced water treatment equipment in industrial environments. Evoqua has built a reputation for delivering turnkey water treatment solutions and wastewater treatment systems for a wide range of industries. The company’s expertise covers biological, chemical, and physical water treatment processes. Evoqua’s commitment to innovation and service excellence makes it a trusted partner for industrial water management.
Main Products
Evoqua’s product portfolio includes:
OMNIFLO® SBR systems with Jet Tech technology for biological wastewater treatment.
OMNIPAC SBR systems with pre-engineered tank designs.
Boiler feed water treatment systems that ensure equipment longevity and process reliability.
Membrane bioreactors (MBRs) for high-quality effluent production.
Advanced membranes, sand filters, and activated carbon filters for comprehensive water purification.
You can select Evoqua’s water treatment equipment to address both routine and complex water challenges in your facility.
Industrial Strengths
Evoqua demonstrates its strengths through successful large-scale projects and advanced technology. You benefit from their experience in expanding biological wastewater treatment plants, such as the Seacrest, Florida project, which doubled capacity to 4.0 million gallons per day using OMNIFLO® SBR systems. Evoqua also delivered turnkey solutions for growing communities in Texas, featuring OMNIPAC SBR systems with multiple treatment basins.
Expansion of Seacrest, Florida plant: Increased capacity from 2.0 to 4.0 MGD with advanced biological treatment.
Turnkey wastewater treatment solution for Texas: Pre-engineered circular tank design with multiple SBR basins.
Evoqua’s technology addresses a wide range of industrial water contaminants:
Treatment Type | Description |
|---|---|
Biological Treatment | Utilizes microorganisms to decompose organic matter in wastewater. |
Chemical Treatment | Adds chemicals to neutralize or precipitate contaminants. |
Filtration | Removes suspended solids from wastewater. |
Disinfection | Destroys pathogenic microorganisms. |
Membrane Bioreactors (MBRs) | Combines biological treatment with membrane filtration for high-quality effluents. |
Moving Bed Biofilm Reactor | Uses biofilm-coated carriers for effective wastewater treatment. |
Chemical Precipitation | Forms insoluble particles for removal through sedimentation or filtration. |
Oxidation | Breaks down complex organic pollutants using advanced oxidative processes. |
Sand Filters | Treats surface waters and wastewater efficiently. |
Activated Carbon Filters | Removes organic compounds and residual disinfectants. |
Chlorination | Disinfects water by adding chlorine. |
Ultraviolet (UV) Disinfection | Inactivates pathogens without chemicals, supporting environmental goals. |
Evoqua’s comprehensive water treatment equipment and solutions help you meet strict regulatory standards and ensure reliable industrial water management.
Pall Corporation
Overview
You encounter Pall Corporation as a global leader in water treatment equipment, especially in the industrial sector. Pall consistently ranks among the top three companies in the industrial water filtration segment. Alongside Entegris and Cobetter, Pall dominates about 60% of the global market share. You benefit from Pall’s deep expertise in filtration technology, which is especially prominent in the semiconductor and advanced manufacturing markets. This company stands out among suppliers for its commitment to innovation and reliability in water purification.
Main Products
Pall offers a comprehensive range of water treatment equipment designed for industrial applications. You can choose from:
Advanced filtration systems for process water and wastewater treatment systems.
High-performance membranes for critical separation and purification tasks.
Boiler feed water treatment solutions that protect your assets and optimize plant efficiency.
Long-life hydraulic and lubrication filters that extend equipment life.
Specialized filtration products for the semiconductor, pharmaceutical, and food and beverage industries.
These products help you maintain water quality, reduce contaminants, and ensure consistent performance across your operations.
Industrial Strengths
You gain significant advantages when you select Pall for your industrial water treatment needs:
Effective monitoring, separation, and filtration improve your end-product quality.
Pall’s systems extend equipment life and reduce the need for frequent replacements.
You experience less costly downtime, which enhances your overall process reliability.
High-performance filtration systems maximize process efficiency and business performance.
Long-life hydraulic and lubrication filters reduce maintenance downtime and operating costs.
Pall Corporation’s leadership in industrial water treatment equipment ensures you achieve reliable, efficient, and high-quality water management for your facility.
Dow
Overview
Dow stands as a powerhouse among industrial water treatment equipment companies. You rely on Dow for innovative solutions that address complex water challenges in manufacturing, energy, and municipal sectors. Dow’s global presence and commitment to research and development make it a preferred partner for industries seeking advanced water purification and wastewater treatment systems.
Main Products
Dow’s portfolio features some of the most advanced water treatment equipment available today. The following table highlights key products and their applications:
Product Name | Description | Application |
|---|---|---|
FILMTEC reverse osmosis (RO) and nanofiltration (NF) elements | Advanced technologies for water separation | Industrial, municipal, commercial, and consumer water applications |
Designed for pressurized water reactor (PWR) nuclear power plants | Nuclear power sector | |
TEQUATIC™ PLUS F-50 Fine Particle Filter | Innovative filtration solution that maximizes uptime and minimizes maintenance | Various industrial applications |
IntegraFlo Ultrafiltration Modules | Efficient module design that reduces overall system costs | Water treatment plants |
You can also access:
Boiler feed water treatment solutions that ensure system longevity.
Membranes for high-efficiency separation and purification.
Water treatment equipment tailored for both large-scale and specialized industrial needs.
Industrial Strengths
Dow’s strengths lie in its relentless pursuit of innovation and efficiency. You benefit from:
FILMTEC RO and NF elements that deliver superior water separation for diverse industrial applications.
DOWEX™ MONOSPHERE™ 1400PC Cation Resin, which supports the demanding requirements of nuclear power plants.
TEQUATIC™ PLUS F-50 Fine Particle Filter, recognized for its ability to maximize uptime and minimize maintenance.
IntegraFlo Ultrafiltration Modules that help you reduce system costs and improve plant efficiency.
Continuous product development that keeps you ahead in water treatment technology.
Dow’s advanced water treatment equipment and solutions empower you to meet stringent regulatory standards and achieve operational excellence.
Pentair
Overview
Pentair emerges as a trusted name in industrial water treatment equipment. You turn to Pentair for modular solutions that adapt to your facility’s unique requirements. Pentair’s advanced membrane technologies help you reduce your water footprint and optimize resource use. The company’s focus on sustainability and efficiency makes it a top choice for industries facing water scarcity and regulatory pressures.
Main Products
Pentair provides a robust lineup of water treatment equipment for industrial clients:
Modular water treatment systems that scale with your operations.
Advanced membranes for precise separation and purification.
Boiler feed water treatment solutions that protect critical infrastructure.
Water recycling and reuse systems that support sustainability goals.
Specialized equipment for contaminant removal and product water preparation.
These solutions help you address a wide range of water challenges, from initial intake to final discharge.
Industrial Strengths
You benefit from Pentair’s commitment to tailored solutions and global support:
Pentair’s modular water treatment equipment adapts to your site’s specific needs, ensuring efficient contaminant removal and water recycling.
The company’s advanced membrane technologies help you optimize resource use and reduce your environmental impact.
Pentair’s professional network of partners supports you worldwide, with resources available 24/7.
You can access live and recorded training sessions on pump knowledge, as well as an online library for further learning.
Pentair helps you find the right distributor and keeps your company information up to date.
Pentair’s focus on modularity, sustainability, and global service ensures you receive reliable, efficient, and future-ready water treatment solutions for your industrial facility.
Hella Water
Overview
You discover Hella Water as a leading force among industrial water treatment equipment suppliers. With over two decades of experience, you see Hella Water deliver innovative solutions that address the most demanding water challenges. The company’s mission centers on providing clean, safe water for communities and industries worldwide. You benefit from their commitment to sustainability, efficiency, and advanced technology. Hella Water stands out among companies for its ability to transform raw water sources into high-quality water that meets or exceeds national hygiene standards. You can rely on their expertise for both large-scale industrial projects and specialized applications.
Main Products
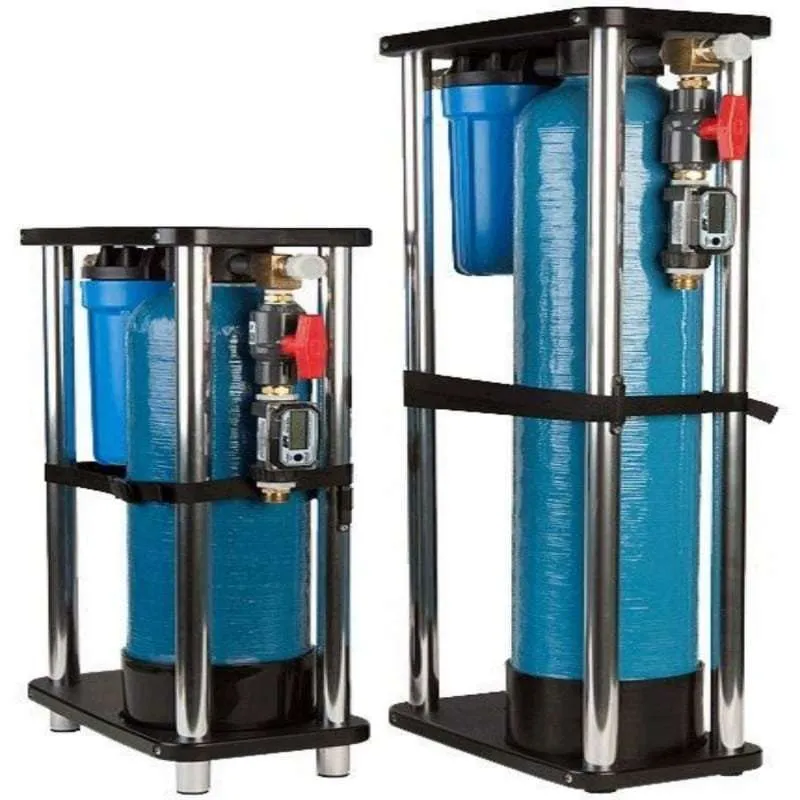
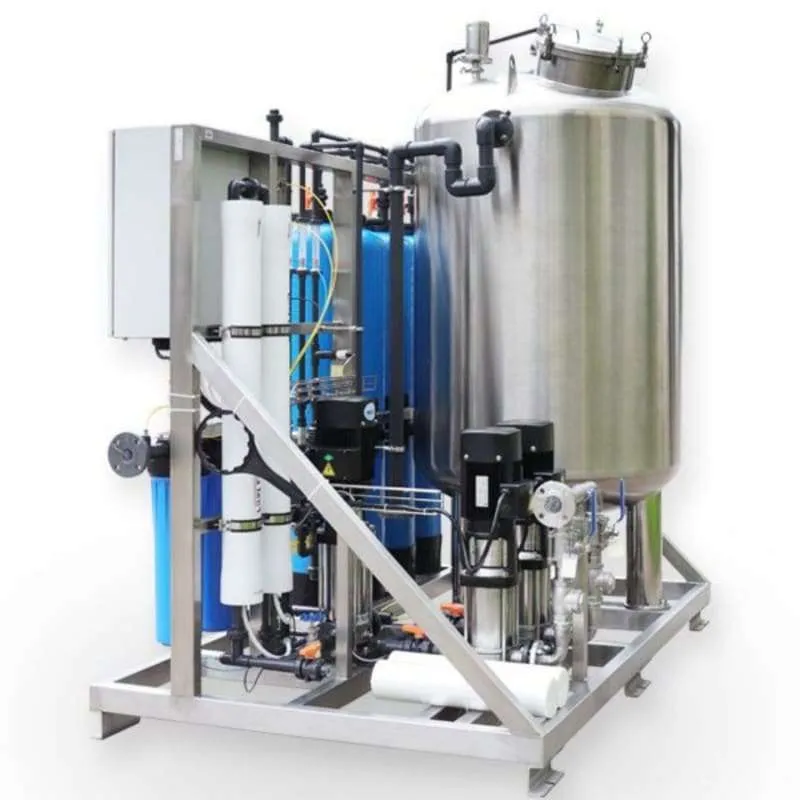
Hella Water offers a comprehensive range of water treatment equipment designed for industrial use. You can select from advanced systems that cover every stage of the water cycle. The product lineup includes:
Desalination systems that convert saline water into potable water for industrial processes.
Reverse osmosis systems that remove over 99% of ions, bacteria, viruses, and particles, ensuring high-level purification.
Nanofiltration and ultrafiltration units that target specific contaminants and improve water quality.
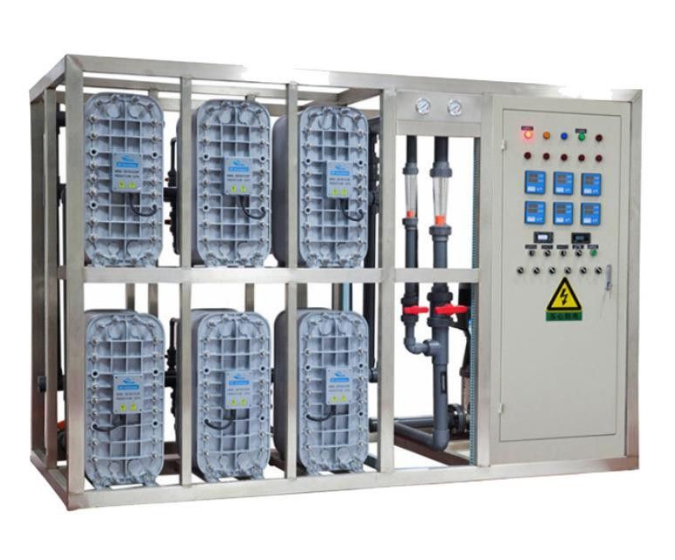
Electrodeionization systems for ultrapure water production in sensitive industrial environments.
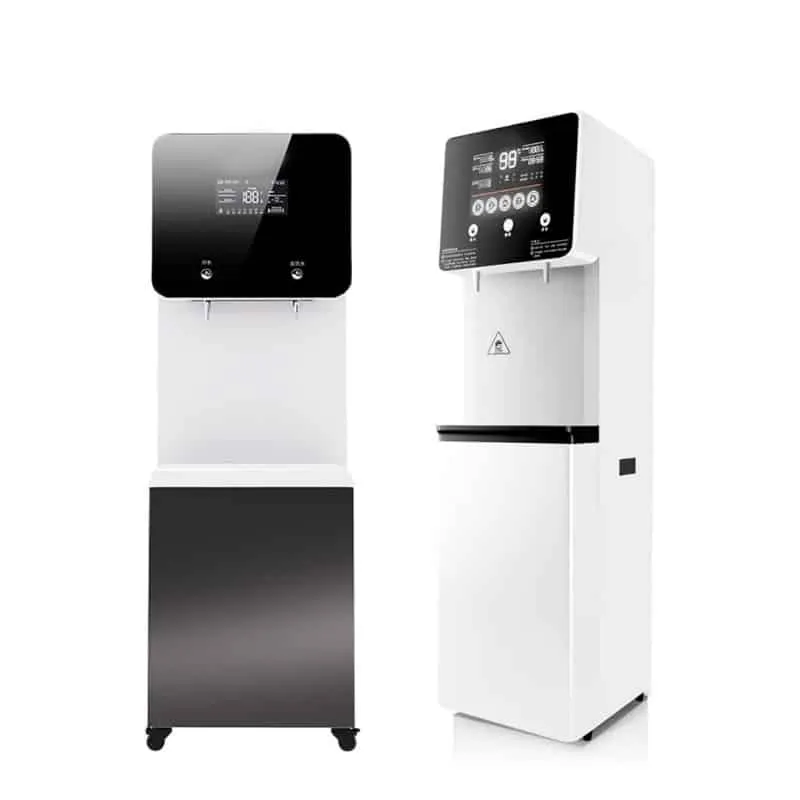
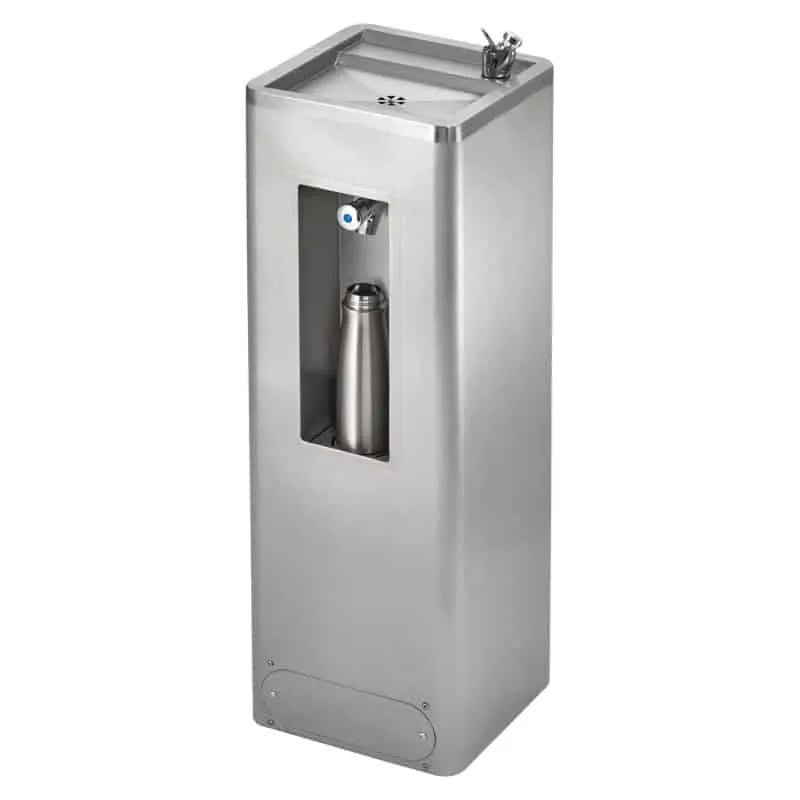
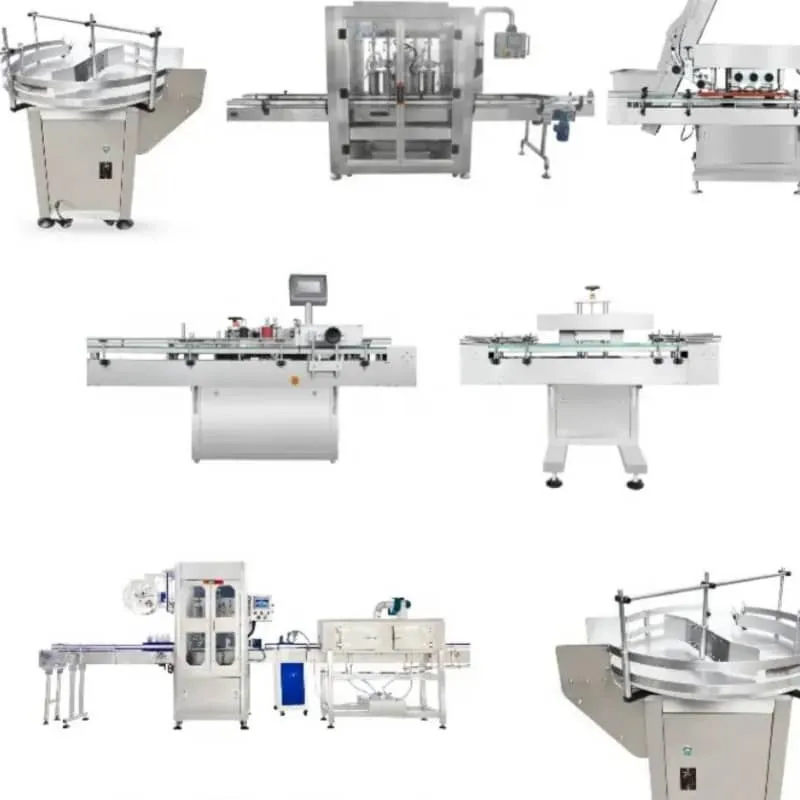
Supporting equipment such as filling machines, water vending machines, and commercial water purifiers for flexible deployment.
You also gain access to specialized wastewater treatment systems that help you manage industrial discharge and protect the environment. Hella Water’s solutions extend to boiler feed water treatment, ensuring your equipment operates efficiently and reliably.
Industrial Strengths
You experience Hella Water’s strengths through its focus on customized solutions and advanced technology. The company engineers each system for efficiency, reliability, and ease of maintenance. You can address a wide range of industrial water challenges, from removing impurities in process water to treating complex wastewater streams.
Hella Water integrates multiple treatment stages to deliver optimal results. The following table highlights the core technology components and their functions:
Technology Component | Function Description |
|---|---|
Raw water system | Level control system to adjust stop and start, single-way valve to prevent re-flux. |
Quartz sand filter | Removes turbidity, suspended matter, organic matter, colloid, etc. |
Activated carbon filter | Eliminates free chloride, organics, harmful matter, bad smell/color, etc. |
Resin softening filter | Removes calcium and magnesium ions to reduce hardness. |
Dosing system | Automatically adjusts chemical dosing according to water quality parameters. |
PP filter | Prevents deposition of large particles into the RO membrane. |
High pressure pump | Provides high pressure to pump water into the reverse osmosis system. |
Capable of removing over 99% of ions, bacteria, viruses, and particles. | |
Backwash system | Cleaning system to prolong the service life of the RO membrane. |
Sterilization system | Uses UV light and Ozone generator to kill organics like bacteria and viruses. |
Chemicals system | Customized adjustment system to purify different raw water types. |
You benefit from Hella Water’s ability to tailor solutions for industries such as food and beverage, pharmaceuticals, agriculture, and power generation. The company’s water treatment equipment supports both process water and boiler feed water treatment, helping you maintain operational efficiency and regulatory compliance. You also find value in their robust membranes and filtration technologies, which ensure consistent water quality and reduce downtime.
Hella Water’s dedication to quality assurance and cost-effective investments means you receive reliable performance and long-term value. You join a movement toward sustainable water management when you choose Hella Water. Their expertise in purification and wastewater treatment systems positions you for success in today’s competitive industrial landscape.
Experience the difference with Hella Water—where advanced water treatment equipment and innovative solutions secure your industrial future.
Comparing Industrial Water Treatment Companies

Specialties & Differentiators
When you compare the top suppliers of water treatment equipment, you notice that each company brings unique strengths to the industrial market. Some companies focus on advanced filtration, while others lead in digital monitoring or chemical dosing. For example, Veolia stands out with its skid-mounted reverse osmosis systems and membrane bioreactors. SUEZ offers specialty filtration cartridges and decarbonation equipment. Xylem delivers high-efficiency pumps and smart controls, which help you manage water resources more effectively. Evoqua provides strong aftermarket service and lifecycle support, making it a reliable partner for ongoing operations. Pentair specializes in modular filtration systems, and Ecolab excels in chemical dosing and water reuse solutions. Hella Water differentiates itself with integrated solutions that combine desalination, ultrafiltration, and electrodeionization, giving you flexibility for both process and potable water needs.
Here is a quick comparison of product innovations:
Company | Product Innovations |
|---|---|
Veolia | Skid-mounted RO, membrane bioreactors, ultrafiltration, filtration media, disinfection, chemical dosing |
SUEZ | Membrane tech, ion exchange, RO/NF, decarbonation, specialty cartridges |
Xylem | High-efficiency pumps, mixing, UV disinfection, packaged plants, digital controls |
Evoqua | MBRs, RO, filtration media, chemical feed, corrosion control, lifecycle support |
Pentair | Filtration systems, RO, cartridge/media filters, pumps |
Ecolab | Chemical dosing, membrane systems, cleaning, monitoring for water quality and reuse |
You can select a supplier based on the specific water challenges you face in your industrial facility.
Technology & Innovation
You want water treatment equipment that keeps pace with changing regulations and industrial demands. Leading companies invest heavily in research and development. Veolia and SUEZ push the boundaries with new membrane and filtration technologies. Xylem integrates digital monitoring and smart controls, which allow you to optimize water use and reduce downtime. Evoqua’s membrane bioreactors and corrosion control solutions help you maintain high water quality in complex environments. Hella Water’s systems combine multiple purification stages, including reverse osmosis and advanced sterilization, to deliver reliable results for both process and potable water. These innovations ensure you always have access to clean water, whether you need it for manufacturing, cooling, or wastewater treatment systems.
Service & Global Reach
Global service coverage matters when you operate across multiple regions. You need a supplier who can support your water treatment equipment wherever your industrial sites are located. Veolia Water Technologies serves clients in over 60 countries, with major customers like ArcelorMittal and BASF. SUEZ Water Technologies operates worldwide and partners with companies such as Nestlé and Shell. Xylem provides global support and works with clients like Unilever and Dow. Hella Water delivers solutions to a wide range of sectors, ensuring you receive expert service and support no matter your location.
Company | Global Coverage | Notable Customers | |
|---|---|---|---|
Veolia Water Technologies | 60+ countries | 4.50 billion | ArcelorMittal, BASF, SABIC |
SUEZ Water Technologies | Worldwide | 3.80 billion | Nestlé, Shell, Sinopec |
Xylem Inc. | Global | 2.60 billion | Georgia-Pacific, Unilever, Dow |
You gain peace of mind when you choose a supplier with proven global reach and a strong track record in industrial water solutions.
Choosing an Industrial Water Treatment System Supplier

Technical Capabilities
When you evaluate suppliers for water treatment equipment, you need to focus on their technical capabilities. The right supplier brings advanced technologies to your industrial operation. You want systems that use reverse osmosis, nanofiltration, and other modern solutions to improve water quality. Customization is also important. Each industrial site has unique water challenges, so your supplier should offer tailored solutions that fit your needs. Sustainability matters as well. Choose a partner who uses environmentally friendly technologies to reduce water consumption and lower your environmental impact. Telemetry and remote monitoring give you real-time insights into your water treatment equipment. This helps you manage performance and spot issues before they become problems. Compliance is another key factor. Your supplier must ensure that all water treatment equipment meets current regulatory standards for industrial use.
Here is a summary of the technical capabilities you should look for:
Capability | Description |
|---|---|
Advanced Technologies | Utilizes cutting-edge solutions like reverse osmosis and filtration to optimize water quality. |
Customization | Offers tailored solutions to meet specific needs of various industries, enhancing system performance. |
Sustainability | Focuses on environmentally friendly technologies that reduce water consumption and environmental impact. |
Telemetry | Provides remote monitoring and management capabilities for real-time insights into system performance. |
Compliance | Ensures adherence to evolving regulatory standards and environmental demands. |
Tip: Always ask suppliers about their experience with your specific industrial sector and the technologies they use in their water treatment equipment.
Product Fit
You need water treatment equipment that matches your industrial process requirements. Start by reviewing your water source and the quality you need for your operation. Some industries require ultrapure water, while others need robust systems for treating wastewater. The best suppliers offer a wide range of products, from desalination units to advanced filtration and reverse osmosis systems. Make sure the equipment can handle your water volume and the contaminants present in your process. You should also consider the flexibility of the system. Can it adapt to changes in your water supply or production needs? A good product fit means fewer disruptions and better performance for your industrial facility.
Assess your water source and quality requirements.
Match equipment capacity to your industrial process.
Look for flexibility and scalability in the system design.
Support & Service
Reliable support and service are essential when you invest in water treatment equipment for industrial use. You want a supplier who offers comprehensive training, technical support, and maintenance services. Fast response times reduce downtime and keep your operation running smoothly. Many leading suppliers provide remote monitoring and diagnostics, so you can address issues quickly. Choose a partner with a proven track record in after-sales service. This ensures your water treatment equipment continues to perform at its best throughout its lifecycle.
Note: Strong support and service from your supplier protect your investment and help you maintain compliance with industrial water regulations.
Cost & Value
You need to balance cost and value when selecting water treatment equipment for your industrial facility. The right investment delivers reliable performance, long-term savings, and lower operational risks. You should not focus only on the initial purchase price. Instead, consider the total cost of ownership, which includes installation, maintenance, energy use, and system lifespan.
Several factors influence the cost of industrial water treatment equipment. You must evaluate your flow rate requirements, the chemistry and quality of your influent stream, and the target level of quality for treated water. The materials used in construction also play a significant role in overall expenses. Here is a summary of the main cost drivers:
Cost Factor | Description |
|---|---|
Flow Rate Requirements | Determines how fast a given volume of water needs to be processed, affecting overall costs. |
Chemistry and Quality of Influent Stream | The quality of the incoming water influences the complexity and cost of treatment. |
Target Level of Quality for Treated Water | Higher quality requirements typically lead to increased costs. |
Required Construction Materials | The choice of materials can significantly impact the cost of the system. |
You should compare suppliers based on the value they deliver, not just the price tag. Some companies offer advanced features, such as energy-efficient pumps or automated monitoring, that reduce long-term costs. Others provide robust after-sales support, which helps you avoid unexpected downtime. When you assess value, look for solutions that improve water quality, enhance process reliability, and support your sustainability goals.
Tip: Request a detailed cost breakdown from each supplier. This helps you understand where your money goes and allows you to make informed decisions for your industrial operation.
Compliance
You must ensure your water treatment equipment meets all relevant compliance standards. Industrial facilities face strict regulations that govern water use, discharge, and environmental impact. Non-compliance can lead to fines, shutdowns, or reputational damage.
Major markets enforce different rules, but some standards appear worldwide. In the United States, the Clean Water Act (CWA) regulates pollutants and requires permits for wastewater discharge. The Safe Drinking Water Act (SDWA) protects public water supplies, which affects industries near these sources. In the European Union, the Water Framework Directive (WFD) promotes sustainable water use and mandates permits for discharge. Many companies also follow ISO 14001, an international standard for environmental management systems. National standards and permits vary, so you need to monitor water quality and secure the right approvals.
Regulation/Standard | Description |
|---|---|
Clean Water Act (CWA) | Framework for regulating pollutants in U.S. waters, requiring permits for wastewater discharge. |
Water Framework Directive (WFD) | Governs water protection in the EU, promoting sustainable water use and requiring permits for wastewater discharge. |
Safe Drinking Water Act (SDWA) | Protects public drinking water supplies, impacting industries discharging near these sources. |
ISO 14001 | International standard for environmental management systems, enhancing compliance with regulatory requirements. |
National Standards and Permits | Vary by country, requiring monitoring of water quality and obtaining permits for water-related activities. |
You should ask each supplier how their water treatment equipment supports compliance with these standards. Leading suppliers design systems that help you monitor water quality, automate reporting, and adapt to changing regulations. This ensures your industrial facility stays ahead of compliance challenges and operates without interruption.
Note: Regularly review your compliance requirements, especially if you expand operations or change your water treatment processes.
Industrial Water Treatment System Applications
Power Generation
You play a critical role in power generation when you manage water resources effectively. Power plants depend on water for cooling, steam production, and emissions control. You must use advanced water treatment equipment to ensure reliable operation and regulatory compliance. In this sector, you often face challenges such as scaling, corrosion, and the removal of dissolved solids. You need robust solutions to treat boiler feed water and cooling tower water.
You can select from a range of industrial water treatment equipment, including reverse osmosis systems, demineralizers, and filtration units. These systems help you maintain equipment efficiency and extend asset life. You also reduce downtime and operational costs. Many power plants now use zero liquid discharge systems to minimize environmental impact. You must monitor water quality continuously to meet strict standards.
Application Area | Key Water Treatment Equipment | Purpose |
|---|---|---|
Boiler Feed Water | Demineralizers, RO, Filtration | Prevent scaling and corrosion |
Cooling Towers | Filtration, Chemical Dosing | Control biofouling and deposits |
Wastewater Discharge | ZLD Systems, Advanced Filtration | Meet environmental regulations |
Tip: Regular maintenance of your water treatment equipment ensures consistent performance and compliance in power generation.
Food & Beverage
You must prioritize water quality in the food and beverage industry. Water acts as an ingredient, a cleaning agent, and a processing aid. You cannot compromise on safety or taste. Industrial water treatment equipment helps you remove contaminants, control microbial growth, and meet hygiene standards. You use filtration, reverse osmosis, and ultraviolet disinfection to produce high-purity water for your processes.
You also rely on water treatment equipment to manage wastewater from production lines. This protects the environment and supports your sustainability goals. You can choose modular systems that adapt to changing production volumes. Many facilities now recycle process water to reduce costs and conserve resources.
Use filtration and RO for ingredient water.
Apply UV and ozone for disinfection.
Treat wastewater before discharge or reuse.
You ensure product quality and regulatory compliance when you invest in advanced industrial water treatment equipment.
Chemical Manufacturing
You face complex water challenges in chemical manufacturing. Water serves as a solvent, a reactant, and a cooling medium. You must control impurities to protect your processes and products. Industrial water treatment equipment removes suspended solids, dissolved ions, and organic contaminants. You often use multi-stage systems that combine filtration, ion exchange, and reverse osmosis.
You also need to treat process wastewater before discharge. Strict regulations require you to monitor and control pollutants. You can implement advanced oxidation and membrane technologies to meet these demands. Many chemical plants now recover and reuse water to lower costs and reduce environmental impact.
Water Use Area | Typical Water Treatment Equipment | Benefit |
|---|---|---|
Process Water | Filtration, RO, Ion Exchange | High-purity water for reactions |
Cooling Systems | Filtration, Chemical Dosing | Prevent scaling and fouling |
Wastewater Treatment | Advanced Oxidation, Membrane Systems | Regulatory compliance |
Note: You improve operational efficiency and product quality when you select the right industrial water treatment equipment for chemical manufacturing.
Mining & Heavy Industry
You face unique challenges in mining and heavy industry when it comes to managing water. Mining operations require large volumes of water for mineral extraction, dust suppression, and equipment cooling. Heavy industry relies on water for cooling, cleaning, and processing raw materials. You must use advanced water treatment equipment to ensure reliable supply and safe discharge.
Water treatment equipment helps you remove suspended solids, heavy metals, and chemical contaminants from process water. You need robust systems that can handle high loads and variable water quality. Industrial sites often operate in remote locations, so you depend on equipment that is easy to maintain and can withstand harsh conditions.
You must address strict environmental regulations. Discharging untreated water can harm local ecosystems and result in fines. You use water treatment equipment to meet compliance standards and protect your reputation. Many industrial facilities now recycle water to reduce costs and minimize environmental impact.
Here are common applications for water treatment equipment in mining and heavy industry:
Treating process water for mineral separation and ore washing.
Managing wastewater from tailings ponds and slurry pipelines.
Removing heavy metals and toxic chemicals before discharge.
Recycling water for dust control and equipment cooling.
Treating stormwater runoff to prevent pollution.
Tip: You improve operational efficiency and reduce downtime when you invest in reliable water treatment equipment for your industrial site.
You select from a range of technologies to meet your needs. Reverse osmosis systems remove dissolved salts and metals. Ultrafiltration units capture fine particles and colloids. Chemical dosing systems neutralize acids and adjust pH levels. You also use sedimentation tanks and clarifiers to separate solids from water.
The following table summarizes key water treatment equipment and their functions in mining and heavy industry:
Equipment Type | Function | Industrial Application |
|---|---|---|
Reverse Osmosis | Removes dissolved salts and metals | Process water, wastewater |
Ultrafiltration | Captures fine particles and colloids | Ore washing, recycling |
Chemical Dosing | Neutralizes acids, adjusts pH | Wastewater, process water |
Sedimentation Tanks | Separates solids from water | Tailings, stormwater |
Clarifiers | Removes suspended solids | Slurry, process water |
You must monitor water quality continuously. Automated sensors and remote monitoring systems help you track performance and detect issues early. You rely on suppliers who offer technical support and training for your staff.
You achieve sustainability goals by recycling water and reducing fresh water intake. Advanced water treatment equipment allows you to reuse water in your industrial processes, lowering costs and supporting environmental stewardship.
Note: You protect your business and the environment when you choose the right water treatment equipment for mining and heavy industry.
You ensure project success when you match supplier strengths to your industrial water needs. Careful evaluation of each provider helps you secure the right water treatment equipment for your facility. Reach out to suppliers or request proposals to move your project forward. The water treatment industry continues to expand, with global demand for water solutions projected to reach $90.02 billion by 2030. You can expect ongoing innovation as water quality and sustainability remain top priorities.

FAQ
What is a water treatment system?
A water treatment system removes contaminants from water to make it suitable for industrial, commercial, or residential use. You can use a water treatment system to ensure safe water for processes, equipment, or consumption.
Why do industrial facilities need a water treatment system?
You need a water treatment system to protect equipment, meet regulatory standards, and ensure product quality. A water treatment system also helps you reduce operational costs and minimize environmental impact.
How do you choose the right water treatment system for your facility?
You should assess your water source, contaminants, and required water quality. Consult with experts to match a water treatment system to your process needs. Consider system capacity, maintenance, and compliance requirements.
What technologies are common in a water treatment system?
You often find reverse osmosis, ultrafiltration, nanofiltration, and electrodeionization in a water treatment system. These technologies help you remove particles, ions, and microorganisms from water.
How often should you maintain a water treatment system?
You should follow the manufacturer’s guidelines for maintenance. Regular checks and cleaning keep your water treatment system efficient. Schedule inspections to prevent downtime and extend system life.
Can a water treatment system help with water reuse?
Yes, you can use a water treatment system to recycle and reuse water in your facility. This reduces fresh water consumption and supports sustainability goals.
What industries benefit most from a water treatment system?
Industries such as power generation, food and beverage, chemical manufacturing, and mining rely on a water treatment system. You improve process reliability and meet strict regulations with the right system.
How does a water treatment system support regulatory compliance?
A water treatment system helps you meet local and international water quality standards. Automated monitoring and reporting features make compliance easier for your facility.
Tip: Always document your water treatment system maintenance and upgrades for audit purposes.
Feature | Benefit for Your Facility |
|---|---|
Automated Controls | Simplifies water treatment system operation |
Remote Monitoring | Tracks water treatment system performance |
Modular Design | Expands your water treatment system easily |
You can request a custom water treatment system for unique industrial needs.
Ask suppliers about energy-saving features in your water treatment system.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian