




Project Background
The textile and dyeing industry is a significant contributor to global water consumption and pollution. Manufacturing textiles can consume up to 200 tons of fresh water per ton of dyed fabric, resulting in substantial wastewater production. According to the World Bank, dyeing and garment treatment account for approximately 17-20% of all industrial water pollution.
Project Requirements
The primary objectives of this water treatment project are:
- Efficient Removal of Dyes and Chemicals: Eliminate residual dyes and chemicals from wastewater to meet environmental discharge standards.
- Water Reuse: Enable the recycling of treated water for use in various stages of textile processing.
- Compliance with Environmental Regulations: Ensure adherence to local and international environmental standards.
Technical Aspects
Project Parameters
- Wastewater Characteristics:
- High Chemical Oxygen Demand (COD) and Biological Oxygen Demand (BOD).
- Presence of complex organic compounds and residual dyes.
- Alkaline pH levels.
- Treatment Capacity:
- Designed to process 500 cubic meters of wastewater per day.
Equipment Specifications
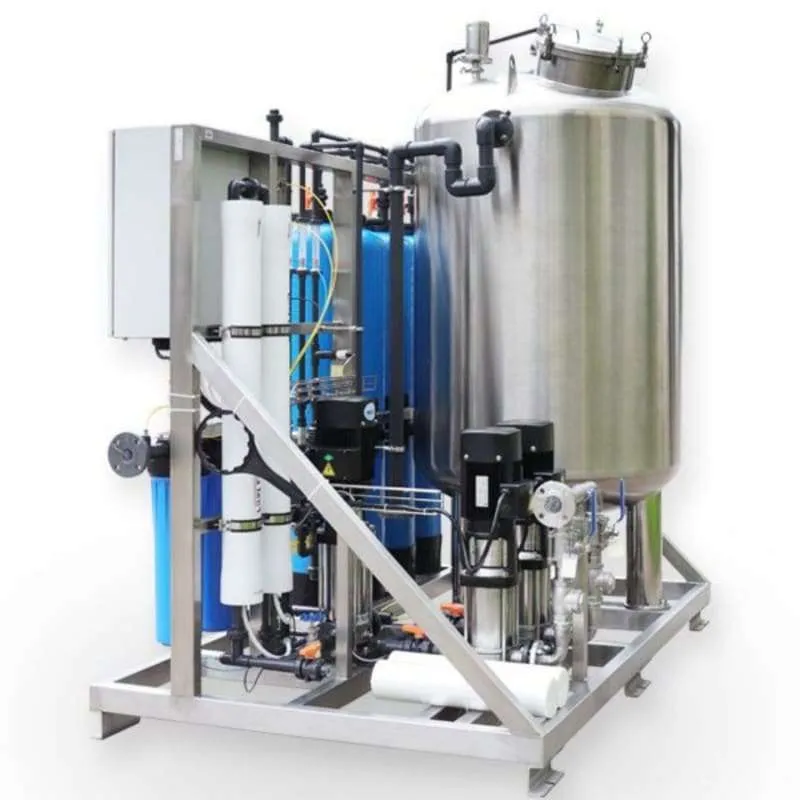
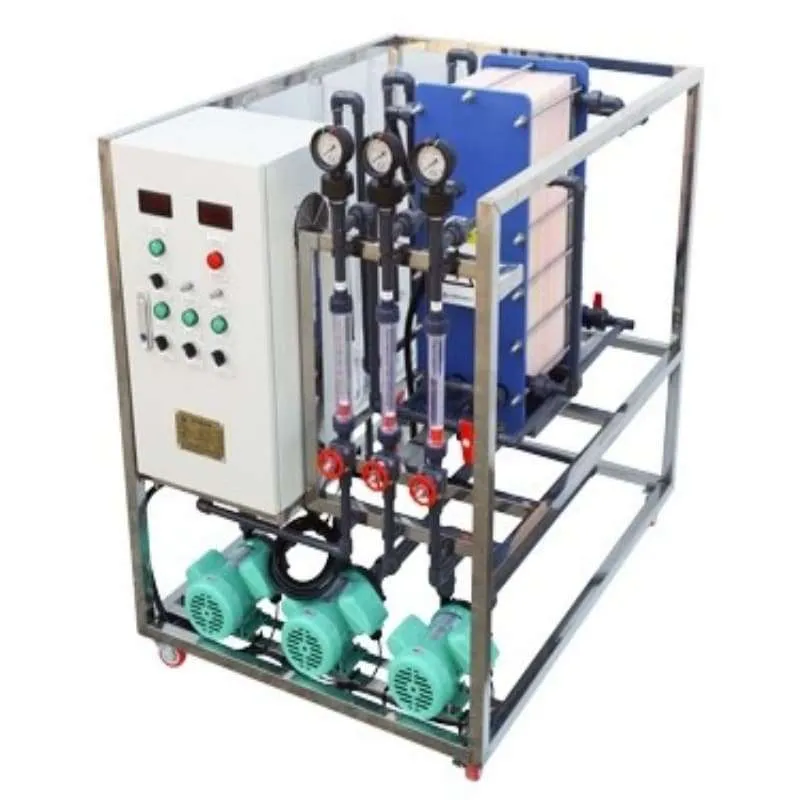
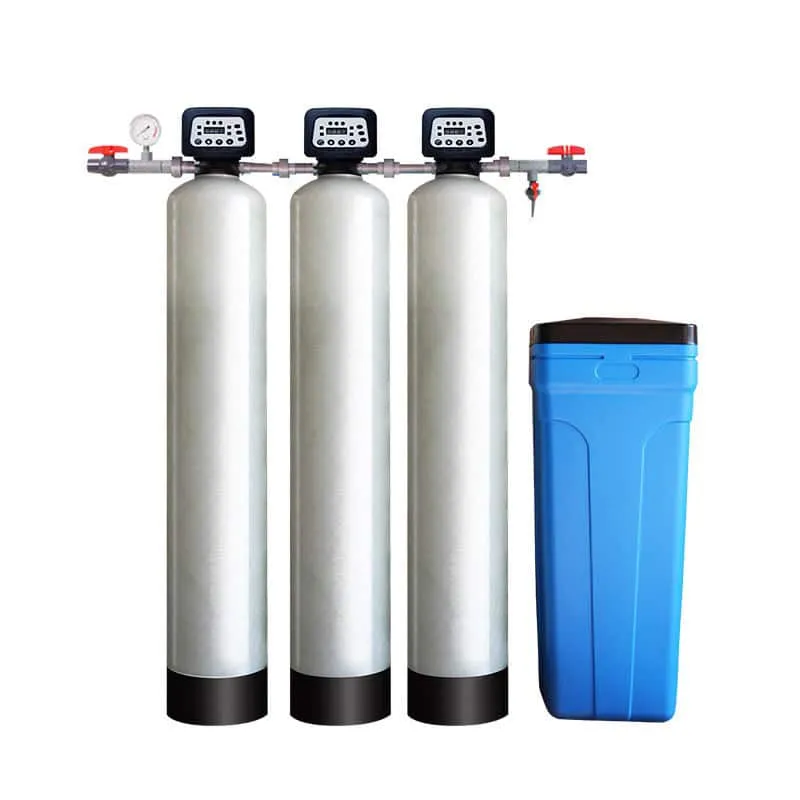
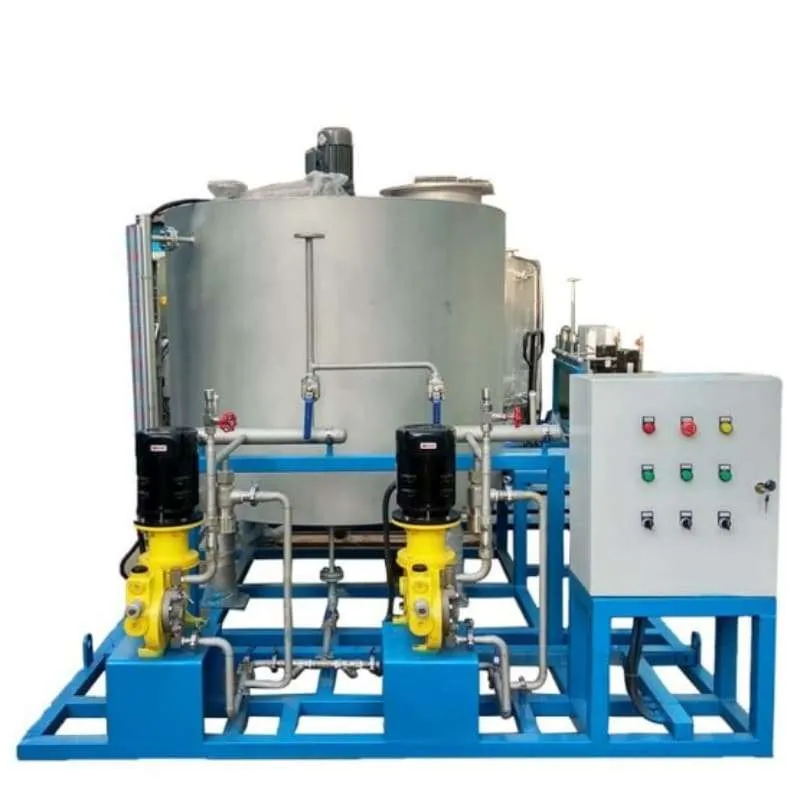
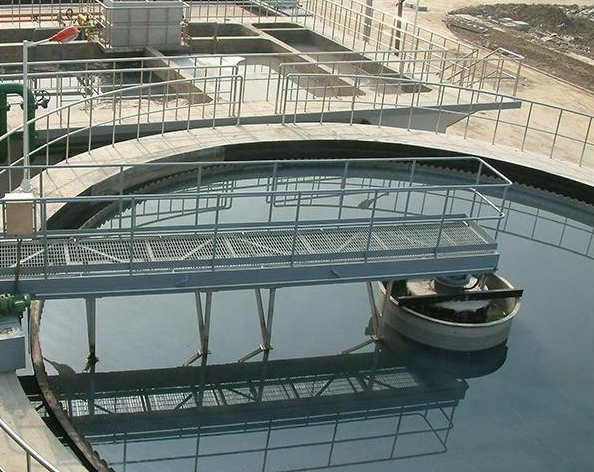
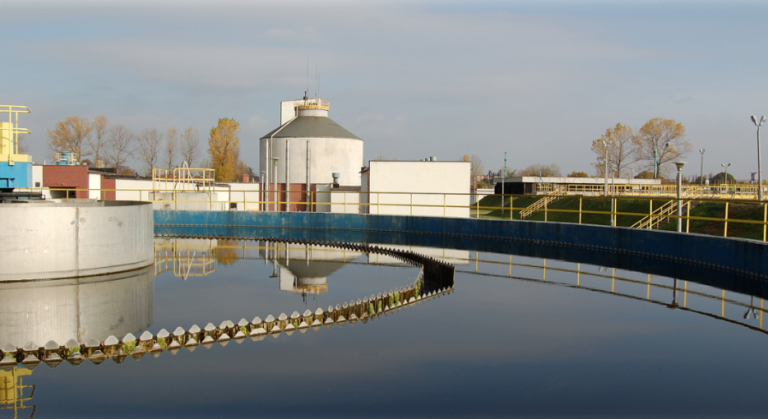
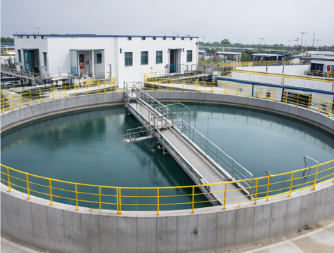
The treatment system comprises several key components:
Anaerobic Reactor
Utilizes anaerobic microorganisms to degrade complex organic compounds, reducing COD levels.
Aerobic Bioreactor
Employs aerobic bacteria to further decompose organic matter, lowering BOD levels.
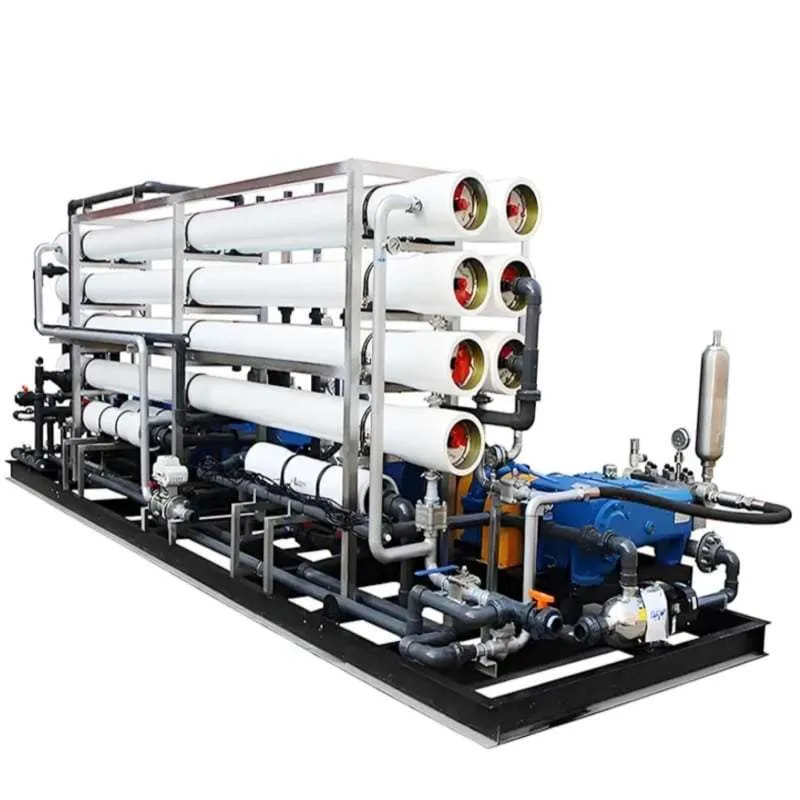
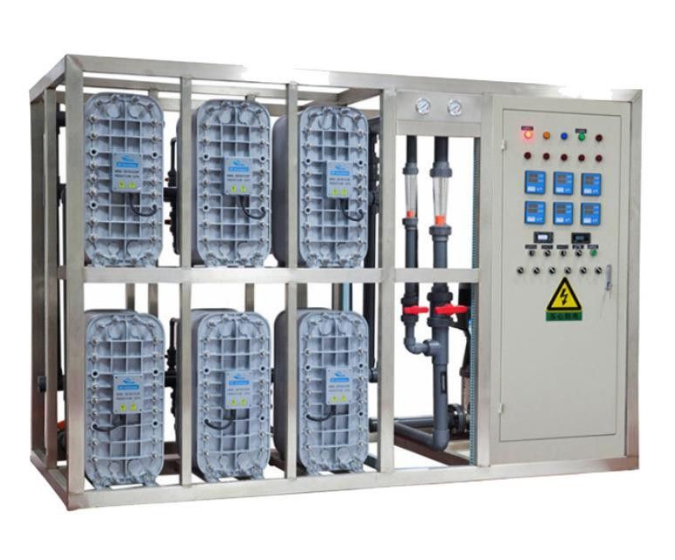
Membrane Filtration Unit
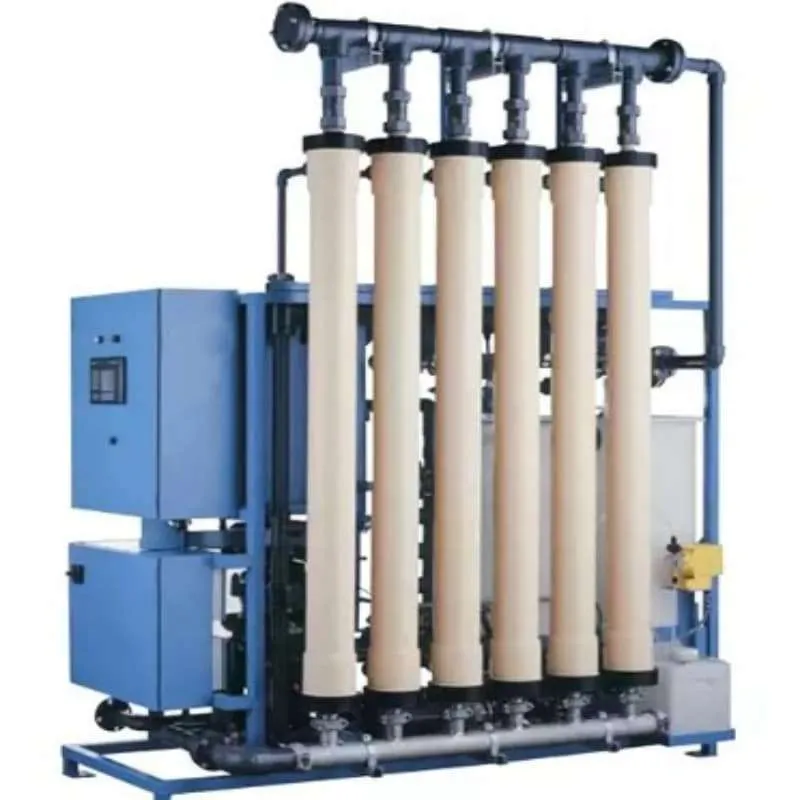
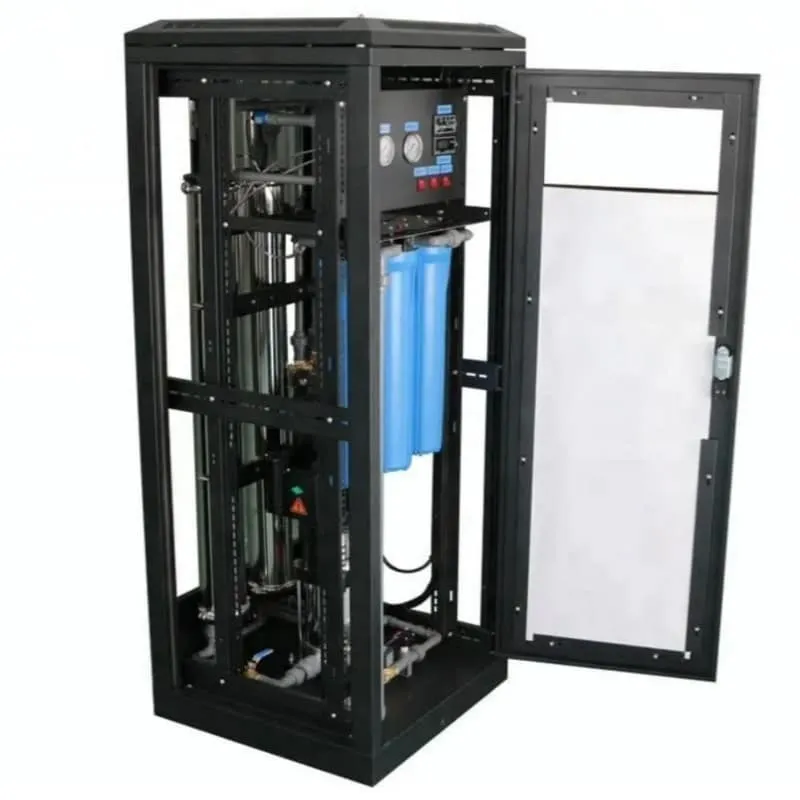
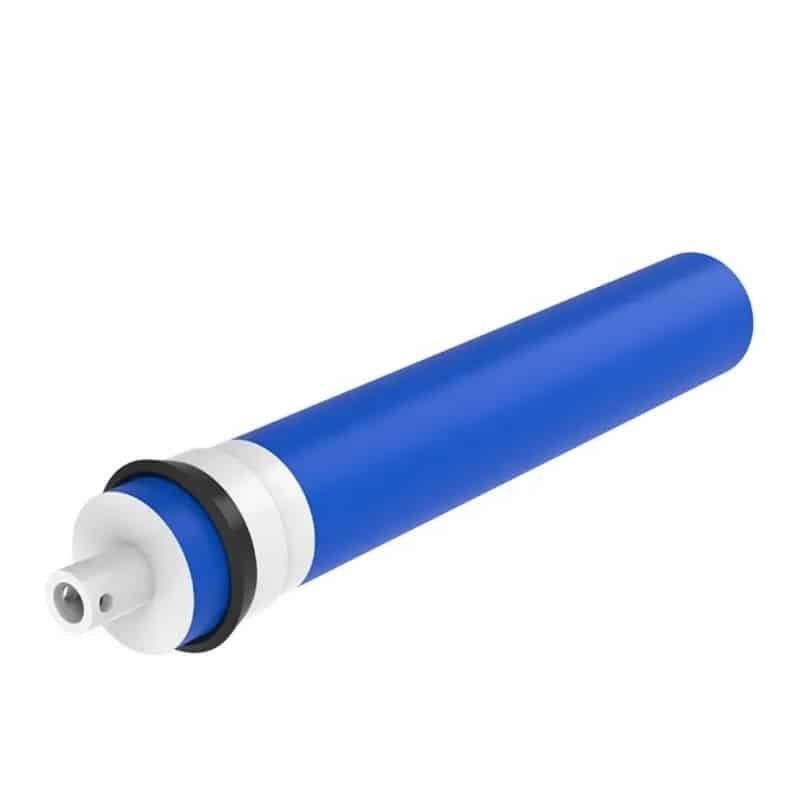
Employs ultrafiltration and reverse osmosis membranes to remove remaining contaminants and enable water reuse.
Sludge Dewatering System
Concentrates and dewaters sludge for safe disposal or potential use as a byproduct.
Project Outcomes
Upon implementation, the water treatment system achieved the following results:
- Dye Removal Efficiency: Achieved a dye removal rate exceeding 95%, ensuring compliance with discharge standards.
- Water Reuse: Enabled the recycling of treated water, reducing fresh water consumption by 40%.
- Environmental Compliance: Met all local and international environmental regulations, contributing to sustainable industrial practices.
This case study demonstrates the effectiveness of advanced water treatment technologies in addressing the challenges faced by the textile and dyeing industry, promoting environmental sustainability and operational efficiency.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian