




1. Case Basic Information

1.1 Project Overview
| Item | Details |
|---|---|
| Project Name | Steam generator and pre-filter water treatment module |
| Project Unit (Customer Name) | Samara Ley Kazakhstan LLP |
| Project Location | Axelfield |
| Project Core Goal | Purify oilfield polluted water to meet the water inlet requirements of steam generators, and provide stable high-quality steam for subsequent production |
| Cooperation Mode | Equipment supply, installation guidance, commissioning, transportation, loading and unloading, and DDP cargo service |
| Warranty Period | 5 years (consumables not included) |
1.2 Basic Water Quality Data
1.2.1 Inlet Water Quality (Key Indicators)
| No | Detection Indicators | Unit | Design Standard Value | Measured Value |
|---|---|---|---|---|
| 1.1 | Turbidity | мг/дм³ (mg/L) | 1.5 | 107.2246±15.0114 |
| 1.2 | Chroma | Spend | 20 | 42.7801±8.5561 |
| 1.3 | Odor (20℃/60℃) | point | 2, 2 | 5, 5 |
| 1.4 | Unpleasant smell | point | 2 | 5 |
| 2.1 | Permanganate (Organic matter index) | мгO₂/дм³ | 5 | 20.72±2.07 |
| 2.3 | Total hardness | мг-экв/дм³ | 7 | 24.5±2.5 |
| 2.6 | Total dissolved solids (TDS) | мг/дм³ (mg/L) | 1000 | 40729.0±814.6 |
| 2.7 | Petroleum pollutants | мг/дм³ (mg/L) | 0.1 | 202.386±50.596 |
| 3.1 | Chloride (Cl⁻) | мг/дм³ (mg/L) | 350 | 37152.0±743.0 |
| 3.3 | Total iron (Fe) | мг/дм³ (mg/L) | 0.3 | 4.0429±0.7277 |
| 3.15 | Sodium + Potassium (Na⁺+K⁺) | мг/дм³ (mg/L) | 200 | 24121.34±1929.71 |
1.2.2 Outlet Water Quality Standard (Steam Generator Requirement)
| Water Quality Indicator | Standard for Steam Generators (Operating at Pressures up to 1.4 MPa) | Standard for Steam Generators (Operating at Pressures up to 9.0 MPa) |
|---|---|---|
| Organoleptic indicators | Strictly comply with drinking water standards SanPiN 2.1.3684-21 | Strictly comply with drinking water standards SanPiN 2.1.3684-21 |
| Odor, points | ≤2 | ≤2 |
| Flavor, points | ≤2 | ≤2 |
| Color, degrees | ≤20 | ≤20 |
| EMF turbidity (formazine turbidity units) or mg/dm³ | ≤2.6 | ≤2.6 |
| Kaolin turbidity, mg/dm³ | ≤1.5 | ≤1.5 |
| Suspended substances, mg/dm³ | ≤5.0 | ≤5.0 |
| Permanganate oxidation, mg O₂/dm³ | ≤5.0 | ≤5.0 |
| Total hardness, mcg-eq/dm³ | ≤20 | ≤20 |
| Silicic acid (in terms of SiO₂), mg/dm³ | ≤10.0 | ≤10.0 |
| Font transparency, cm (no less) | 40 | – |
| Content of iron compounds (in terms of Fe), µg/L | 300/not standardized | 50/100 |
| Content of copper compounds (in terms of Cu), µg/L | Not standardized | 10/not standardized |
| Total hardness, mcg-eq/L | 15/20 | 5/10 |
| Dissolved oxygen content, µg/L | 30/50 | 20/30 |
| pH value (at t=25℃) | 8.5÷10.5 | – |
| Content of petroleum products, mg/L | 3 | 0.5 |
| Free carbon dioxide content, µg/L | Not allowed | – |
| Dry residue, mg/L | 1000 | – |
| Chlorides, mg/L | 350 | – |
| Sulfates, mg/L | 500 | – |
1.3 Key Equipment Scale
| System | Key Parameters |
|---|---|
| Water Treatment System | Inlet water capacity: 75 m³/H; Outlet water capacity: 20 m³/H; Meet the boiler water inflow requirements |
| Steam Generator System | 2 sets of steam generators; Maximum outlet steam pressure: 15 MPa; Maximum steam temperature: 360℃; Equipped with 1 set of remote control console for dual steam generators |
2. Project Core Pain Points and Requirements

2.1 Severe Oilfield Polluted Water Contamination
The inlet water of the project has extremely poor quality, with multiple indicators far exceeding the standard. For example, the turbidity is as high as 107.2246±15.0114 mg/L (1.5 mg/L as the standard), petroleum pollutants reach 202.386±50.596 mg/L (0.1 mg/L as the standard), and total dissolved solids (TDS) are 40729.0±814.6 mg/L (1000 mg/L as the standard). Such polluted water cannot be directly used for steam generators, and if not properly treated, it will cause serious corrosion and scaling of the boiler, affecting the service life and safety of the equipment.
2.2 High Demand for Water Quality Stability of Steam Generators
Steam generators have strict requirements on water quality. Taking the steam generator operating at a pressure of up to 9.0 MPa as an example, the content of petroleum products in the inlet water must be ≤0.5 mg/L, the total hardness ≤10 mcg-eq/L, and the dissolved oxygen content 20-30 µg/L. The traditional water treatment process is difficult to stably control multiple indicators within the standard range, which may lead to unstable steam output and even safety accidents.
2.3 High Cost of Traditional Water Treatment
In the traditional treatment of oilfield polluted water, there are problems such as high dosage of chemicals, large amount of residue, and high operation cost. For example, similar to the situation of Zhongyuan Oilfield mentioned in the China Petrochemical News Network report, the traditional process has high agent cost and large residue output, which not only increases the operation cost but also brings great pressure to environmental protection.
2.4 Need for Efficient Integration of Water Treatment and Steam Generation
The project requires that the treated water can be directly supplied to the steam generator, and the entire system needs to be highly integrated and automated to reduce manual operation and management costs. At the same time, the system should have good scalability and adaptability to cope with possible changes in the quality and quantity of oilfield polluted water.
3. Hella Water Customized Solutions

3.1 Overall Process Design of Water Treatment and Steam Generation
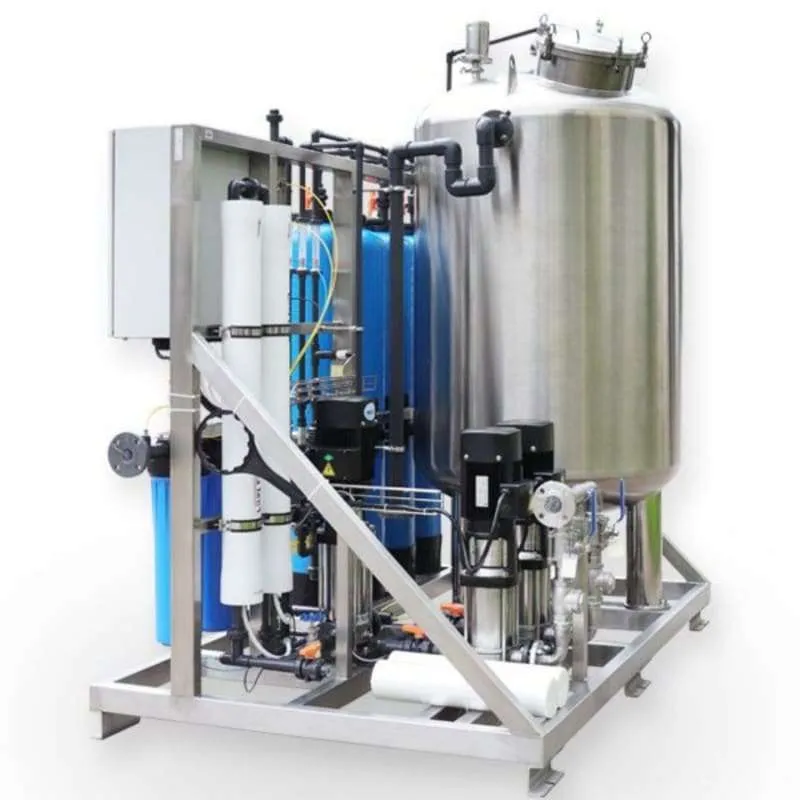
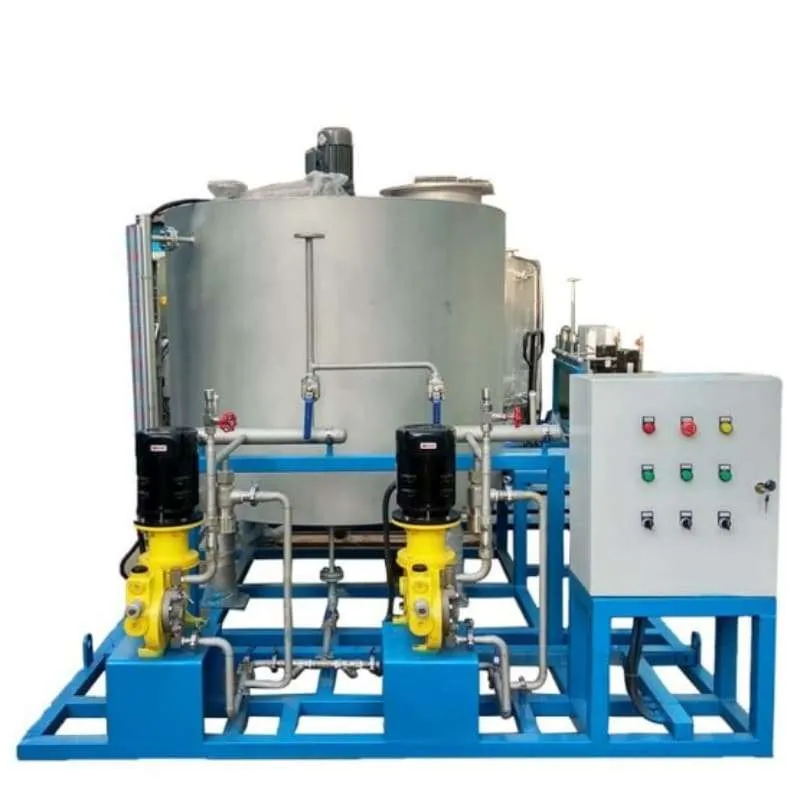
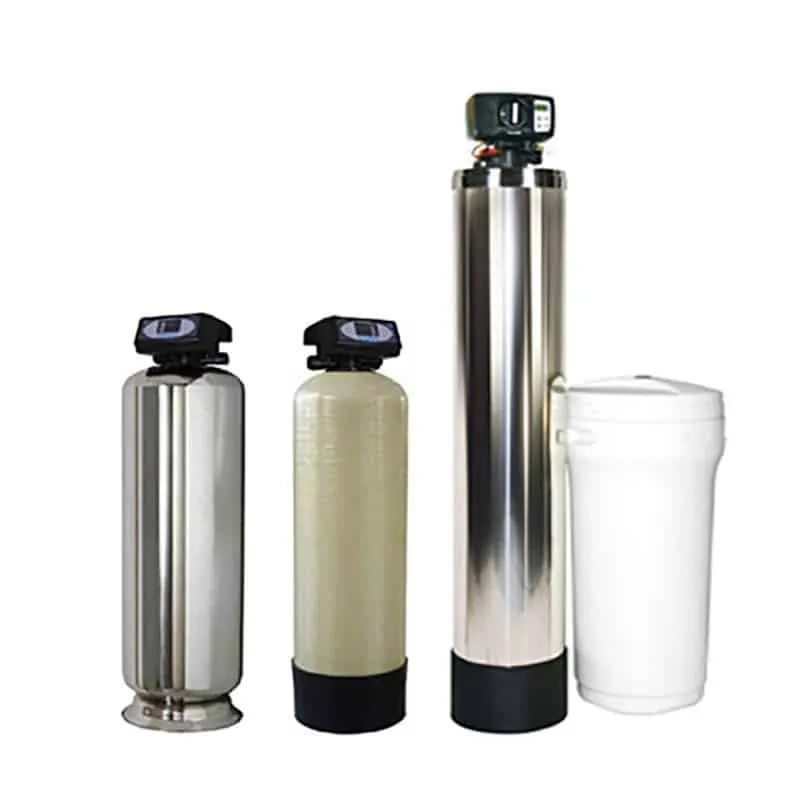
The solution adopts a multi-stage combined process to realize the deep purification of oilfield polluted water and the efficient operation of steam generators. The specific process flow is as follows:Polluted water → Conditioning pool (existing) → Oil isolation tank → Dissolved Air Flotation Machine (with dosing device) → Flocculation tank (with dosing device) → Press filter → Ceramic membrane area → Quartz sand/activated carbon filter (2 sets) → Ultrafiltration module → Desalination reverse osmosis (with dosing device) → Reverse osmosis machine → Boiler water inlet → Steam generator → Steam.
3.2 Key Module Design and Parameters
3.2.1 Oil Isolation System
| Parameter | Details |
|---|---|
| Equipment Model | 75 m³/h oil-water separator |
| Design Flow | 75 m³/h |
| Influent Oil Content | 200 mg/L |
| Target Outlet Oil Content | ≤20 mg/L |
| Hydraulic Retention Time (HRT) | 1 h |
| Separation Tank Size | L×W×D=4 m×2.4 m×2.4 m |
| Surface Load Rate | 1.0 m³/(m²·h) |
| Oil Skimmer Speed | 0.8 m/min |
| Key Technology | Inclined plate sedimentation (inclined plate specifications: spacing 60 mm, inclination 45°, PP material) + oleophilic stainless steel wire mesh agglomeration (aperture 10 mm, thickness 300 mm) |
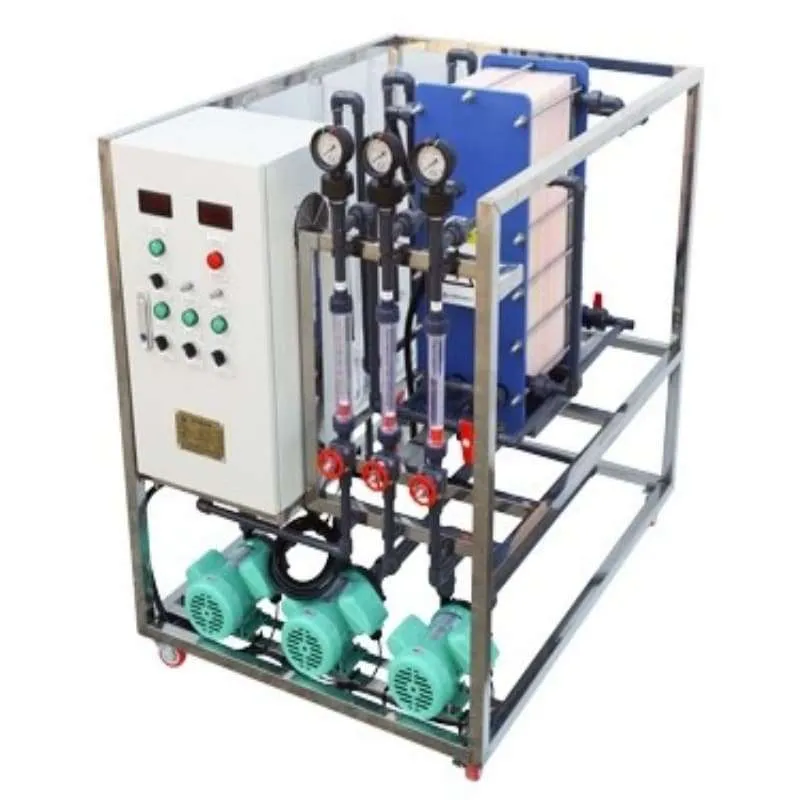
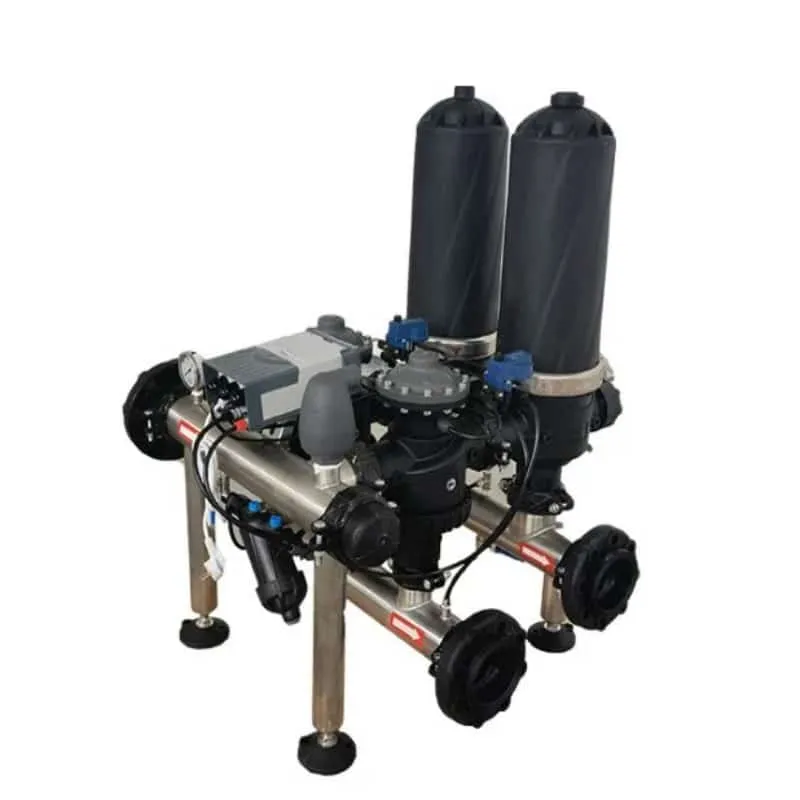
3.2.2 Dissolved Air Flotation System (Related Product Link)
| Equipment | Specifications | Quantity | Power |
|---|---|---|---|
| 75 m³/h Dissolved Air Flotation Machine | Overall size: 12 m×2.3 m×2.3 m; Internal carbon steel anti-corrosion (full penetration welding on both internal and external surfaces, followed by kerosene leak detection test); Anti-corrosion with three layers of fiberglass cloth and five layers of resin coating | 1 set | – |
| Dissolved Air Tank | Model: ZTRQ-75; Material: Carbon Steel | 1 set | – |
| Reflux Pump | Model: ZTRQ-75 | 1 pc | 8 kW |
| Air Compressor | Model: ZTRQ-75 | 1 pc | 2.8 kW |
| Scraper | Type: Chain | 1 pc | 0.75 kW |
| Releaser | Model: TJ Releaser; Material: PVC | 1 set | – |
| Stirring Device | Model: ZTRQ-75 | 2 pcs | 1.8 kW each |
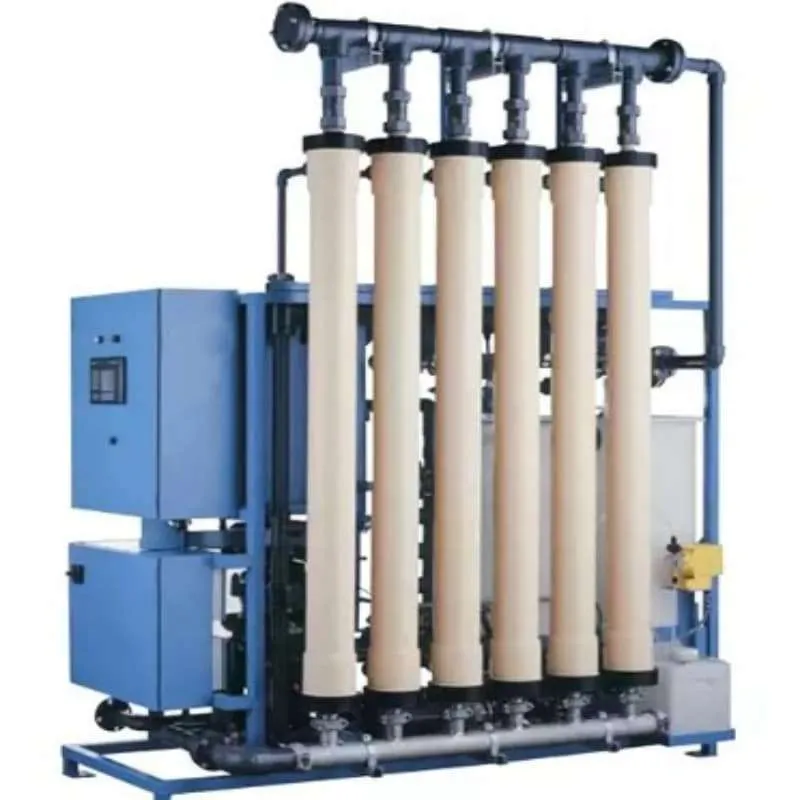
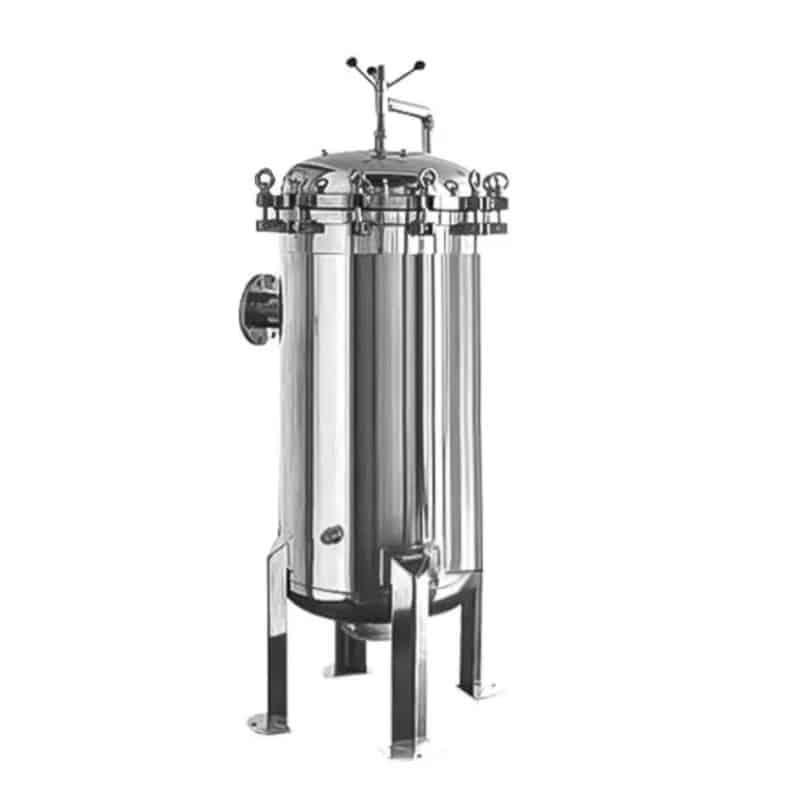
3.2.3 Ultrafiltration System (Related Product Link)
| Parameter | Details | |
|---|---|---|
| Equipment Model | 60 T Ultrafiltration Device | |
| Design Flow | 60 m³/h | |
| Ultrafiltration Membrane | Quantity: 22 pcs; Material: PVDF; Specification: Ф225 | |
| Precision Filter | Specification: 40″ 40; Material: Stainless steel; Type: Quick-release | 1 pc |
| Control System | PLC control + touchscreen; Support manual/automatic operation | |
| Frame Material | Stainless steel |
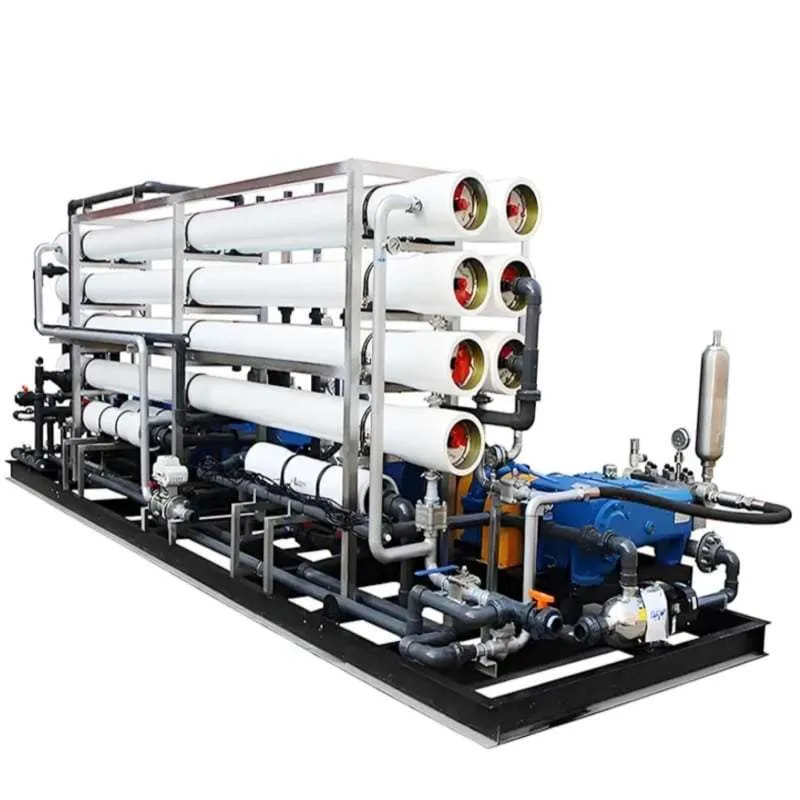
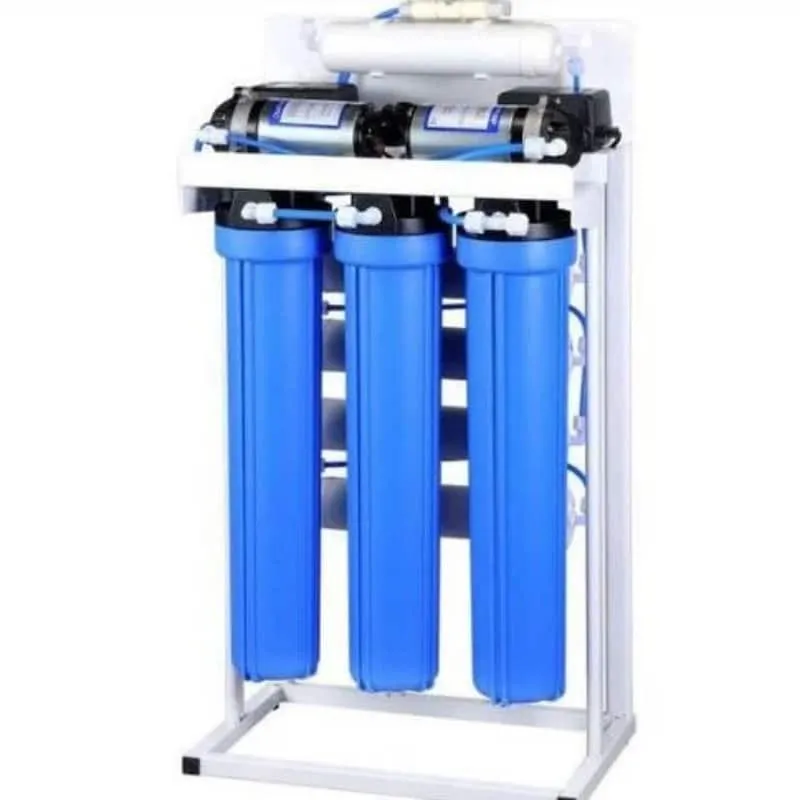
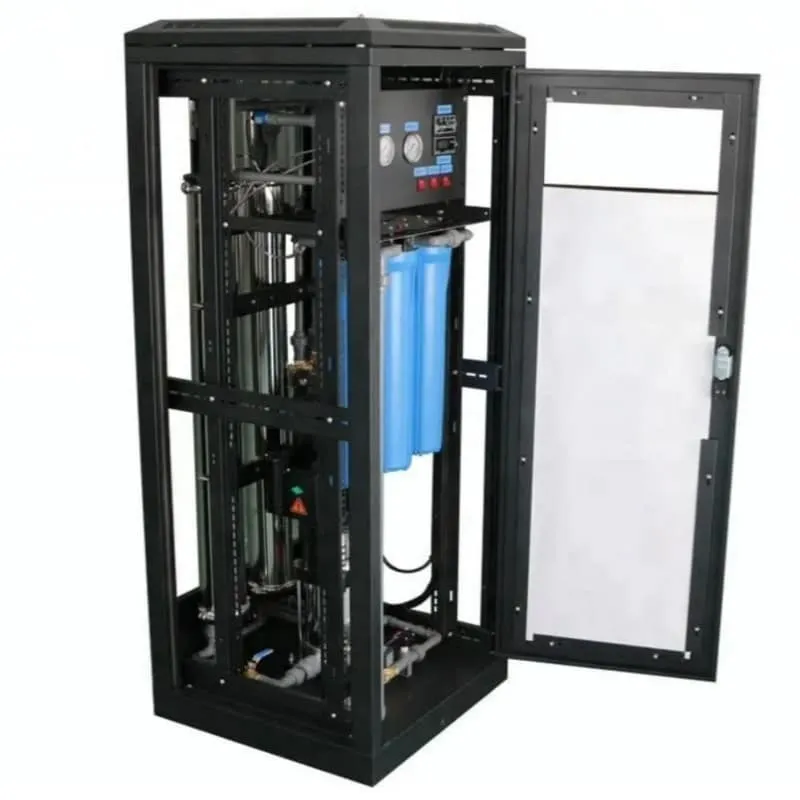
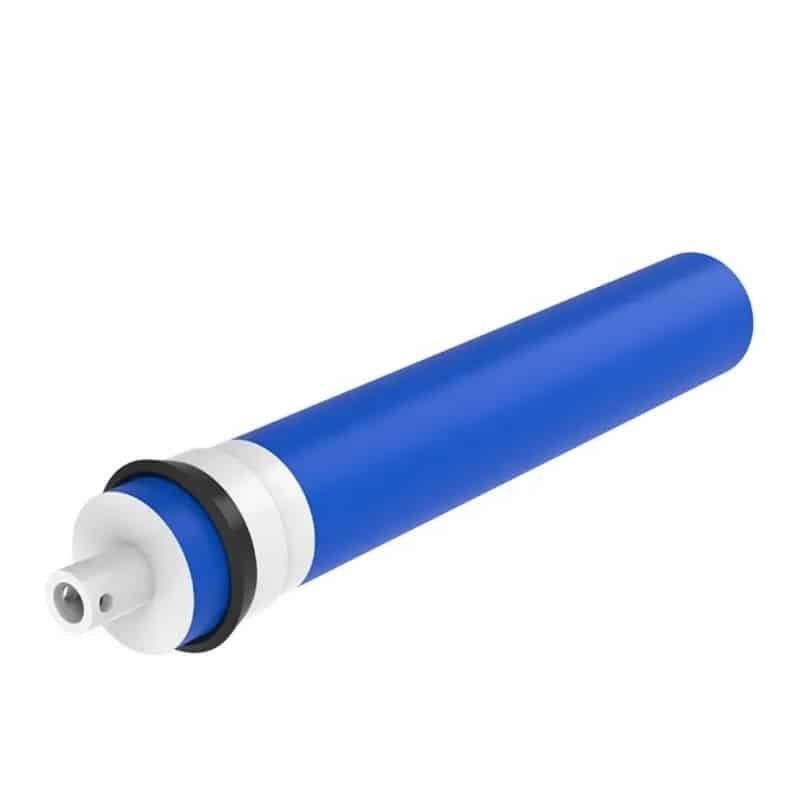
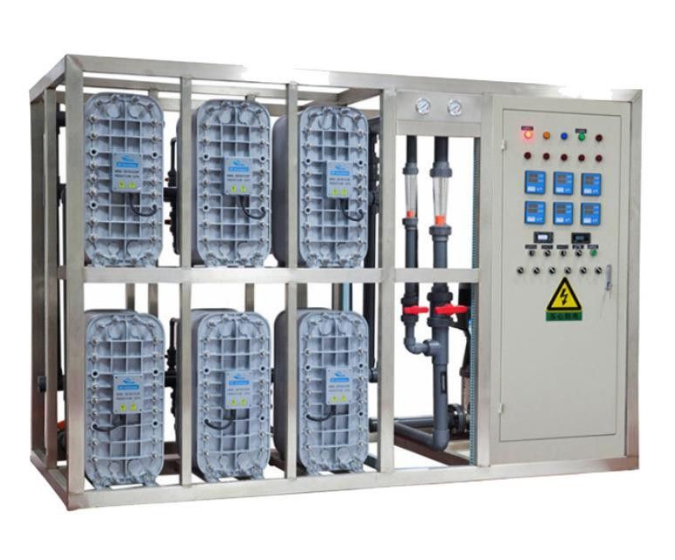
3.2.4 Reverse Osmosis Desalination System (Related Product Link)
| System | Parameters |
|---|---|
| First-stage Desalination Reverse Osmosis (25 m³/h) | – Design flow: 25 m³/h- High-pressure pump: Flow 50 m³, Head 580 m, Power 30+55 kW, Material 2205- RO membrane: Quantity 45 pcs, Model SW8040HR-400- Membrane shell: Quantity 9 pcs, Model F80-1000psi-6- Cleaning system: 2000 L PE cleaning box; Cleaning pump: Flow 36 m³, Head 23 m, Power 4 kW, Material 304 |
| Second-stage Reverse Osmosis (20 m³/h) | – Design flow: 20 m³/h- High-pressure pump: Material 304 stainless steel; Lift 120 m, Flow 20 m³, Power 11 kW- Pressure vessels: Quantity 5 pcs, Model US8040-4, Material Fiberglass- Membrane elements: Quantity 20 pcs, Type Composite polyamide, Specification 8040 |
3.2.5 Steam Generator System
| Parameter | Details |
|---|---|
| Equipment Model | WNS8-17-Y (Q) steam boiler |
| Quantity | 2 sets |
| Rated Evaporation Capacity | 8 t/h |
| Rated Steam Pressure | 17 MPa |
| Rated Steam Temperature | 350℃ |
| Feed Water Temperature | 20℃ |
| Economizer Outlet Water Temperature | 56.005℃ (gas fuel); 54.857℃ (oil fuel) |
| Design Exhaust Temperature | 91.774℃ (gas fuel); 92.846℃ (oil fuel) |
| Design Fuel | Natural gas, heavy oil |
| Design Boiler Thermal Efficiency | 94.6% (natural gas); 94.8% (heavy oil) |
| Supporting Equipment | 1 set of gas pressure regulator (inlet pressure 4 bar, outlet pressure 0.45 bar); 1 set of dual steam generator remote control console; 250 meters of sectional gas pipeline; 250 meters of sectional insulated water supply pipeline; 1 set of spare parts (ZII); 2 units of modular rooms for steam generators |
3.3 Automatic Control and Intelligent Management
The entire system is equipped with a centralized control system, including PLC control, touchscreen operation, and frequency converters. It can realize real-time monitoring of parameters such as water flow, pressure, temperature, and water quality (conductivity, ORP, etc.), and automatically adjust the operation status of equipment (such as dosing amount, pump speed, etc.). For example, the reverse osmosis system is equipped with 2 conductivity meters (EC410) and 1 ORP meter (±300 mvA) to monitor the water quality in real time; the steam generator is equipped with high and low water level alarms, low water level interlock protection, and steam overpressure alarm and interlock protection to ensure the safe and stable operation of the system.
4. Project Effect Verification
4.1 Water Quality Purification Effect
After the treatment of the customized system by Hella Water, the key indicators of the outlet water fully meet the inlet water requirements of the steam generator. Taking the steam generator operating at a pressure of up to 9.0 MPa as an example, the verification results of key indicators are as follows:
| Key Indicator | Post-treatment Value | Standard Requirement | Compliance Status |
|---|---|---|---|
| Petroleum pollutants | ≤0.5 mg/L | ≤0.5 mg/L | Compliant |
| Turbidity | ≤2.6 mg/dm³ | ≤2.6 mg/dm³ | Compliant |
| Total hardness | ≤10 mcg-eq/L | ≤10 mcg-eq/L | Compliant |
| Dissolved oxygen | 20-30 µg/L | 20-30 µg/L | Compliant |
| Chlorides | ≤350 mg/L | ≤350 mg/L | Compliant |
4.2 Economic Benefit Analysis
4.2.1 Cost Saving of Water Treatment
Refer to the Harbin News Network report (Haerbin News Network) that the cost of self-made demineralized water is less than 10 yuan/ton, while the cost of purchasing demineralized water is more than 1700 yuan/ton. Assuming that the project consumes 2000 tons of treated water per year, the annual cost saving is about 3.4 million yuan (calculated as (1700-10) yuan/ton × 2000 tons).
4.2.2 Energy Saving of Steam Generator
Refer to the Xinhua News report (Jiangsu: Waste Heat Converted into Kinetic Energy, Steam Promotes Efficient Energy Utilization) that the new steam storage technology can reduce the energy consumption of steam production by about 44%. The WNS8-17-Y (Q) steam boiler in this project has a thermal efficiency of up to 94.8% (oil fuel), which is higher than the average thermal efficiency of traditional boilers (about 85%). It is estimated that the annual energy consumption can be reduced by about 10%, and the annual energy cost can be saved by hundreds of thousands of yuan (specifically depending on the local fuel price and steam usage).
4.3 Environmental Protection Effect
- Zero Discharge of Wastewater: The system treats oilfield polluted water into reclaimed water that meets the standard, which is completely used for the steam generator, realizing the recycling of wastewater and no discharge of wastewater.
- Reduction of Solid Waste: The press filter in the system can reduce the water content of sludge to 78%-83%, reducing the amount of solid waste by more than 30% compared with the traditional process (referring to the effect of Zhongyuan Oilfield’s new technology), and reducing the pressure of solid waste treatment.
- Reduction of Carbon Emissions: The high thermal efficiency of the steam generator and the recycling of wastewater reduce the consumption of fossil fuels and fresh water resources, and the annual carbon emission reduction is about 127,000 tons (referring to the carbon emission reduction effect of Tianwan Nuclear Power Plant’s steam supply project in the Xinhua News report).
5. Case Corresponding Product Quotation Description
5.1 Quotation Summary
| Project Category | Product/Service | Specification | Quantity | Unit Price (USD) | Total Price (USD) | Remarks |
|---|---|---|---|---|---|---|
| Water Treatment System | Water treatment complete set | Inlet water: 75 m³/H; Outlet water: 20 m³/H; Meet boiler water inflow requirements | 1 set | – | – | Including oil isolation tank, dissolved air flotation machine, flocculation tank, press filter, ceramic membrane, ultrafiltration, reverse osmosis, etc. |
| Steam Generator System | WNS8-17-Y (Q) steam boiler | Rated evaporation capacity: 8 t/h; Rated steam pressure: 17 MPa; Rated steam temperature: 350℃ | 2 sets | 324,800 | 649,600 | – |
| Gas pressure regulating cabinet | Model: RX0.4/1500C | 1 set | 18,900 | 18,900 | – | |
| Gas pipelines | Flange elbow DN125 | 250 pcs | 16 | 4,000 | – | |
| Insulated water supply pipes | Cable with flange DN80 heating elbow | 500 pcs | 25 | 12,500 | – | |
| Spare parts and consumables | Spare parts within two years | 2 batches | 2,800 | 5,600 | – | |
| Skid-mounted room with isolation | Size: 12 m×2.6 m×2.3 m | 2 sets | 18,000 | 36,000 | – | |
| Auxiliary Projects | Guidance installation, commissioning, transportation, loading and unloading | Boiler room and water treatment equipment | 1 item | – | – | Included in the total price |
| Cargo DDP service | – | 1 item | – | – | Included in the total price | |
| Total | – | – | – | – | 726,600 | – |
5.2 Key Equipment Quotation Details
5.2.1 Water Treatment System Core Equipment Quotation
| Equipment Name | Specification | Quantity | Estimated Unit Price (USD) | Estimated Total Price (USD) |
|---|---|---|---|---|
| Oil isolation tank | Size: 4 m×2.4 m×2.4 m; Weight: 3 Ton | 1 set | 15,000 | 15,000 |
| Dissolved air flotation device | Size: 12 m×2.4 m×2.4 m; Weight: 6 Ton | 1 set | 45,000 | 45,000 |
| Coagulation and flocculation tank | Size: 22 m×2.4 m×2.4 m; Weight: 6 Ton | 1 set | 30,000 | 30,000 |
| Filter press machine | Size: 3.6 m×0.9 m×1.8 m; Weight: 1 Ton | 1 set | 20,000 | 20,000 |
| Ceramic membrane area | Size: 2 m×2.4 m×2.4 m; Weight: 1 Ton | 1 set | 50,000 | 50,000 |
| Ultrafiltration module | Size: 3 m×1 m×2.3 m; Weight: 5 Ton; Design flow: 60 m³/h | 1 set | 80,000 | 80,000 |
| First-stage desalination reverse osmosis module | Size: 5 m×1.2 m×2.4 m; Weight: 8 Ton; Design flow: 25 m³/h | 1 set | 120,000 | 120,000 |
| Second-stage reverse osmosis module | Size: 4 m×1 m×2.3 m; Weight: 3 Ton; Design flow: 20 m³/h | 1 set | 100,000 | 100,000 |
Note: The above unit prices are estimated based on market conditions, and the actual prices shall be subject to the formal contract.
6. Frequently Asked Questions (FAQ)
6.1 Technical Questions
Q1: What is the service life of the core components (such as ultrafiltration membrane and reverse osmosis membrane) in the water treatment system?
A1: The service life of ultrafiltration membranes is generally 3-5 years, and the service life of reverse osmosis membranes is generally 2-3 years. The specific service life is affected by factors such as inlet water quality, operation and maintenance level, and cleaning frequency. Hella Water will provide regular maintenance guidance and remind customers to replace consumables in a timely manner. At the same time, the project provides 2 batches of spare parts within two years to ensure the continuous operation of the system.
Q2: How to ensure the stability of the steam generator’s steam output?
A2: The steam generator system of this project adopts multiple measures to ensure stable steam output:
- The water treatment system stably provides high-quality inlet water, which meets the water quality requirements of the steam generator and avoids corrosion and scaling of the boiler, ensuring the stable heat transfer efficiency of the boiler.
- The steam generator is equipped with a dual remote control console, which can monitor and adjust the operation parameters (such as fuel supply, water supply, pressure, etc.) of the two steam generators in real time.
- The system is equipped with high and low water level alarms, low water level interlock protection, and steam overpressure alarm and interlock protection. When abnormal conditions occur, the system will automatically take protective measures to avoid affecting the steam output.
- The steam generator uses a corrugated furnace, which enhances the agitation of flue gas, increases the radiant heat transfer area, and reduces the rigidity of the furnace, effectively mitigating expansion stress and ensuring the stable operation of the boiler.
Q3: Can the system adapt to the changes in the quality and quantity of oilfield polluted water?
A3: Yes. The water treatment system of this project has strong adaptability:
- The pre-treatment process (oil isolation, dissolved air flotation, flocculation) adopts a flexible dosing control system. According to the changes in inlet water quality (such as oil content, turbidity), the dosing amount can be automatically adjusted to ensure the treatment effect.
- The ultrafiltration and reverse osmosis systems are equipped with frequency converters, which can adjust the operating speed of the pump according to the changes in inlet water quantity, ensuring the stable operation of the system and avoiding energy waste.
- Hella Water will provide regular water quality testing services for customers. If the inlet water quality changes significantly, the process parameters can be optimized or auxiliary treatment equipment can be added to ensure the system’s treatment effect.
6.2 Economic and Maintenance Questions
Q1: What is the annual operation and maintenance cost of the system?
A1: The annual operation and maintenance cost of the system mainly includes the cost of consumables (such as ultrafiltration membranes, reverse osmosis membranes, filter elements, chemicals), energy cost (electricity, fuel), and labor cost. The specific cost is estimated as follows:
- Consumables cost: About 50,000-80,000 USD/year (including 1-2 batches of filter elements, 1 batch of chemicals, and partial spare parts).
- Energy cost: The total installed power of the water treatment system is about 100 kW, and the annual electricity cost is about 30,000-50,000 USD (calculated based on 8,000 operating hours/year and 0.05 USD/kWh). The fuel cost of the steam generator depends on the steam usage. Taking the annual steam usage of 50,000 tons as an example, the natural gas cost is about 500,000-800,000 USD/year (calculated based on 10-16 USD/Nm³ of natural gas and 10 Nm³ of natural gas per ton of steam).
- Labor cost: The system adopts an automatic control system, and 2-3 operators can complete the daily operation and maintenance work. The annual labor cost is about 50,000-80,000 USD (depending on the local labor price).The total annual operation and maintenance cost is about 630,000-930,000 USD, and the specific cost is affected by factors such as local energy prices, labor prices, and system operation load.
Q2: What after-sales services does Hella Water provide during the warranty period?
A2: During the 5-year warranty period (excluding consumables), Hella Water provides the following after-sales services:
- Free repair or replacement of faulty equipment and components (excluding consumables such as filters, membranes, and chemicals) caused by quality problems.
- Regular on-site inspection services (at least 2 times a year) to check the operation status of the system, optimize operation parameters, and provide maintenance guidance.
- 24-hour online technical support. When customers encounter technical problems, they can contact Hella Water’s technical support team at any time, and the team will provide solutions within 4 hours.
- Free training services. Before the system is put into operation, Hella Water will provide 2-3 training sessions for the customer’s operation and maintenance personnel, covering system operation, parameter adjustment, fault diagnosis, and daily maintenance.
Q3: How to reduce the operation cost of the system?
A3: Customers can reduce the system’s operation cost through the following methods:
- Strengthen daily operation and maintenance: Regularly clean the filter, ultrafiltration membrane, and reverse osmosis membrane to extend the service life of consumables and reduce the replacement frequency of consumables.
- Optimize energy use: Use waste heat resources (such as industrial wastewater, waste gas waste heat) to preheat the inlet water of the steam generator. Refer to the Yantai Daily report (Watt’s Steam Engine to Green Low-Carbon: The “Black Technology” of Steam Generators Promotes Industrial Transformation), the waste heat can be used to 制取 high-quality saturated steam, reducing the fuel consumption of the steam generator.
- Improve the recycling rate of wastewater: Collect the condensed water of the steam generator and reuse it as the inlet water of the water treatment system, reducing the consumption of raw water and the treatment load of the water treatment system.
- Use intelligent management: Use the system’s automatic control and monitoring functions to optimize the operation parameters (such as dosing amount, pump speed) and avoid energy waste caused by improper operation.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian