




Project Background
In the pharmaceutical industry, water is a critical raw material used extensively in manufacturing processes, equipment cleaning, and as an ingredient in medicines. Ensuring the purity and quality of water is paramount to meet stringent regulatory standards and maintain product integrity.
Project Requirements
The project aimed to design and implement a water treatment system that meets the following requirements:
- Purity Standards: Achieve water quality in compliance with Good Manufacturing Practices (GMP) for pharmaceutical use.
- Capacity: Provide a consistent supply of purified water to support uninterrupted production.
- Sustainability: Incorporate energy-efficient and environmentally friendly technologies.
Technical Details
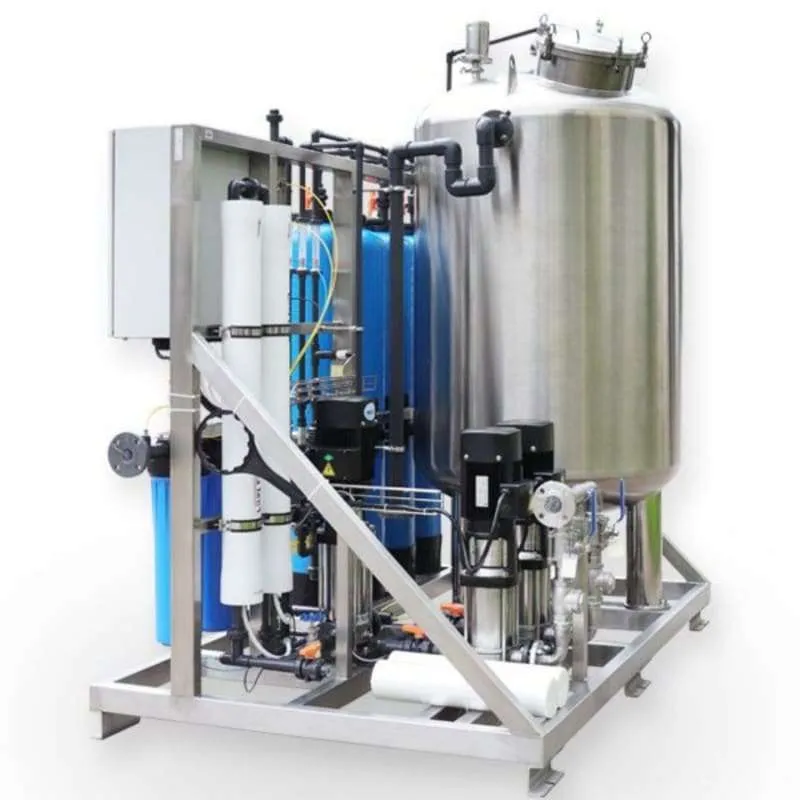
The water treatment system was designed with the following parameters:
- Raw Water Quality: Municipal water with Total Organic Carbon (TOC) levels of 2 mg/L and Total Dissolved Solids (TDS) of 500 mg/L.
- Required Water Quality: Purified Water (PW) with TOC levels not exceeding 0.5 mg/L and endotoxin levels below 0.25 EU/mL.
Equipment Specifications:
| Equipment Type | Specifications |
|---|---|
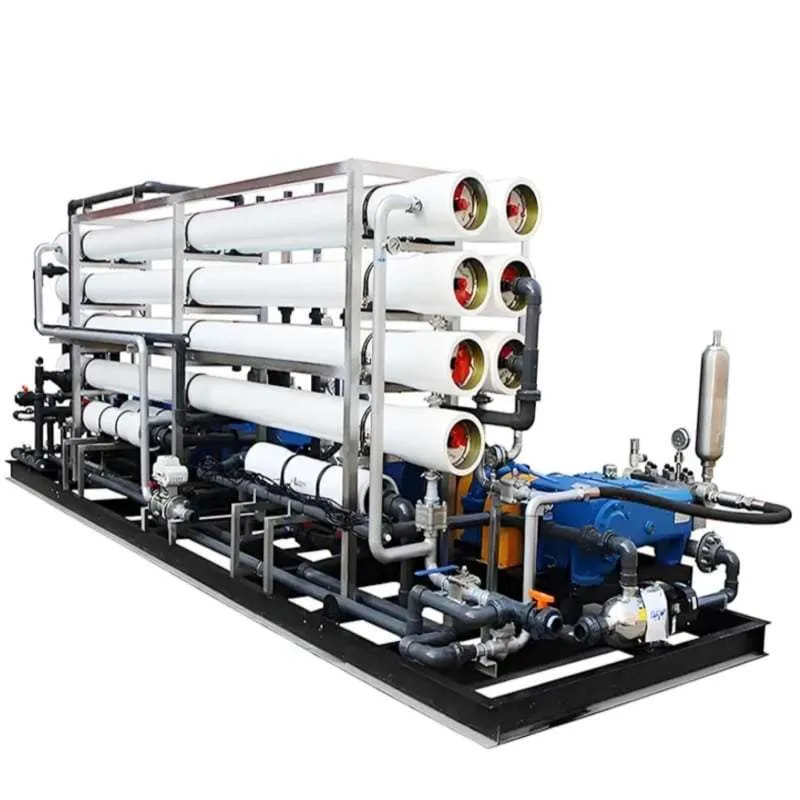
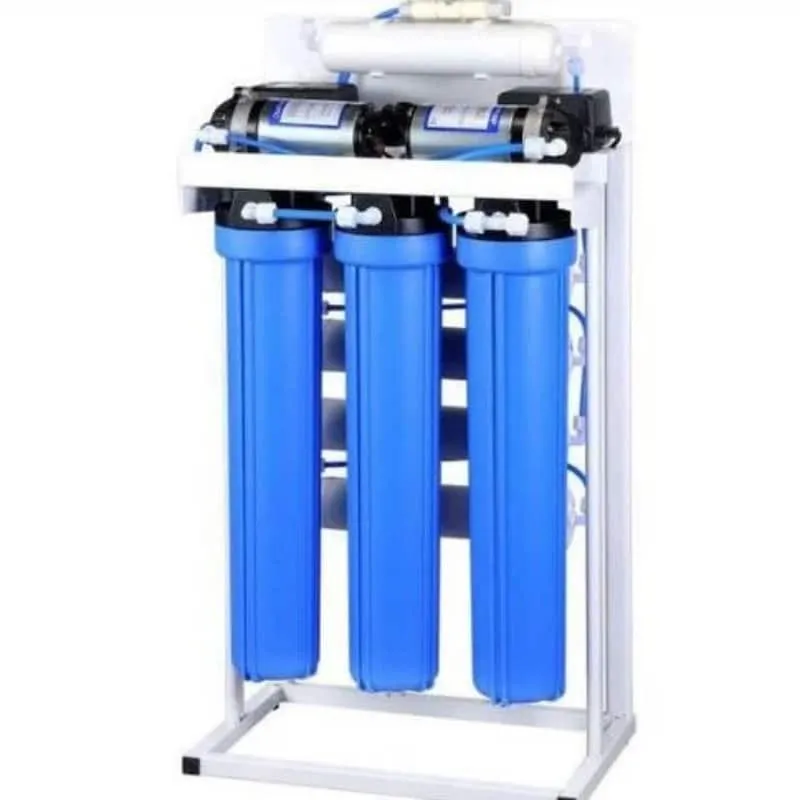
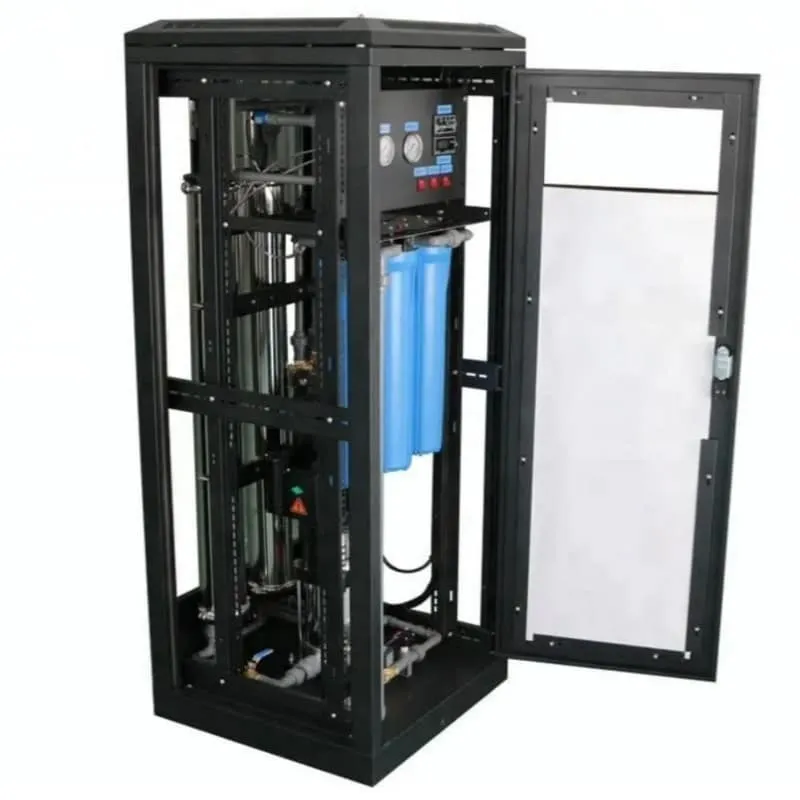
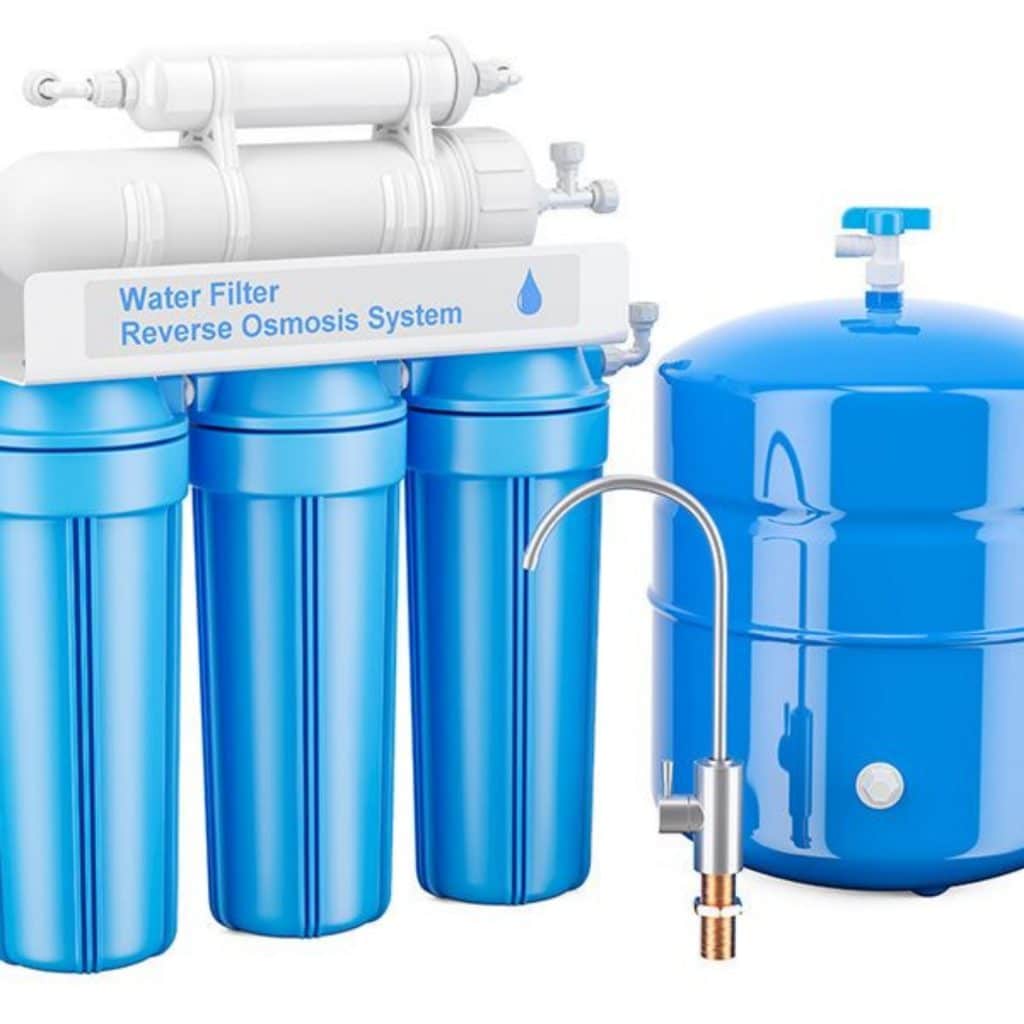
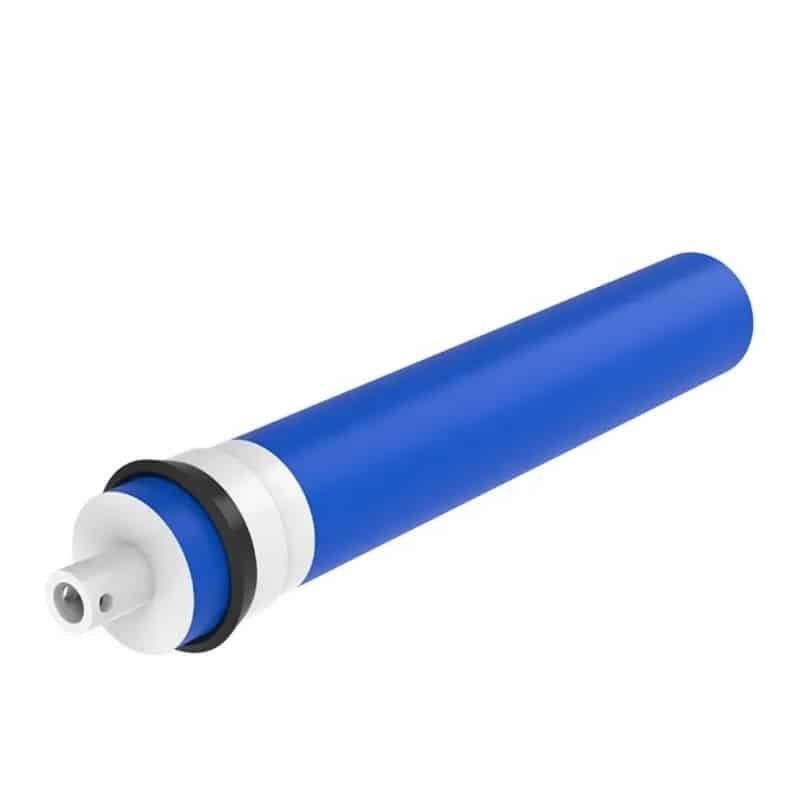
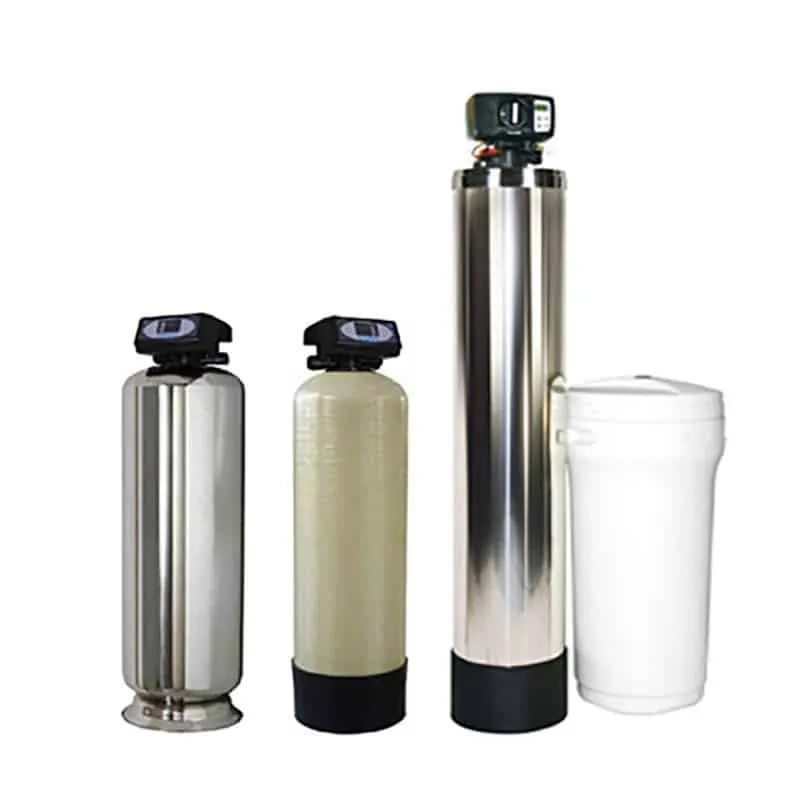
| Reverse Osmosis (RO) | Membrane type: Thin-film composite; Recovery rate: 75%; Rejection rate: 99%+ |
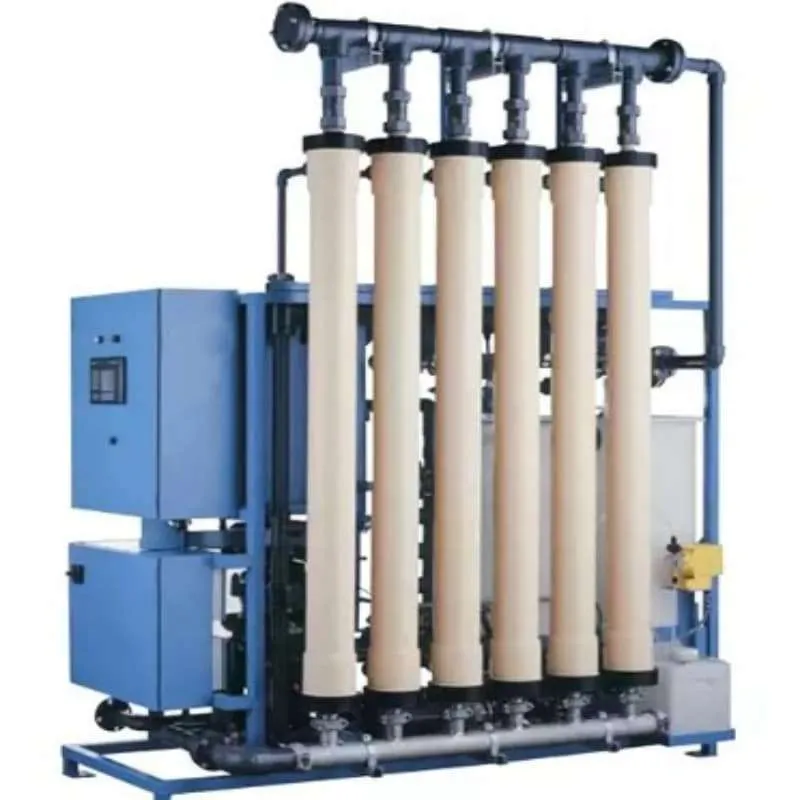
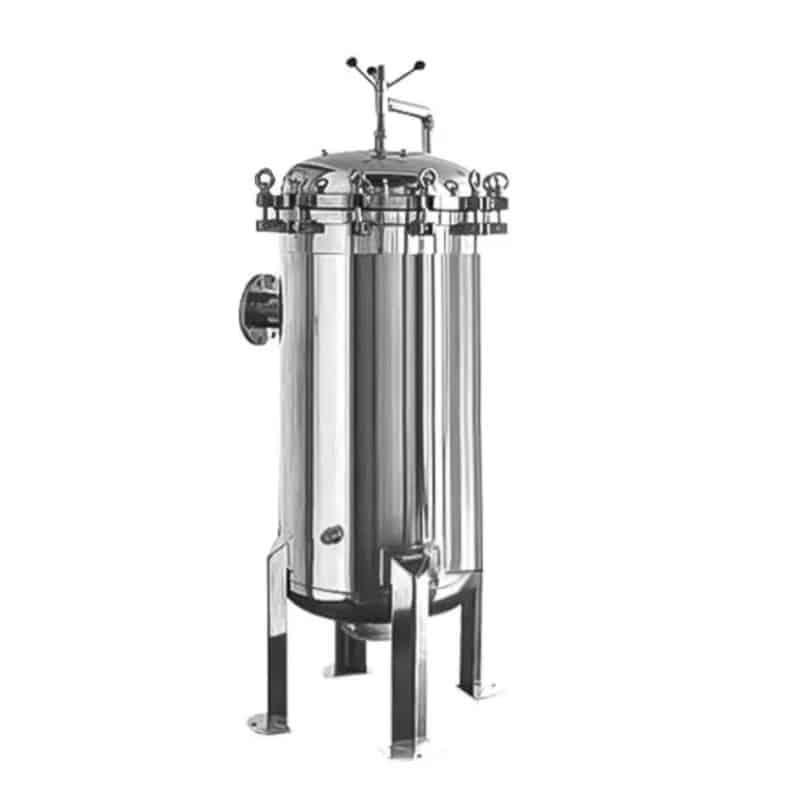
| Ultrafiltration (UF) | Membrane pore size: 0.01 µm; Flux rate: 50 L/m²·h |
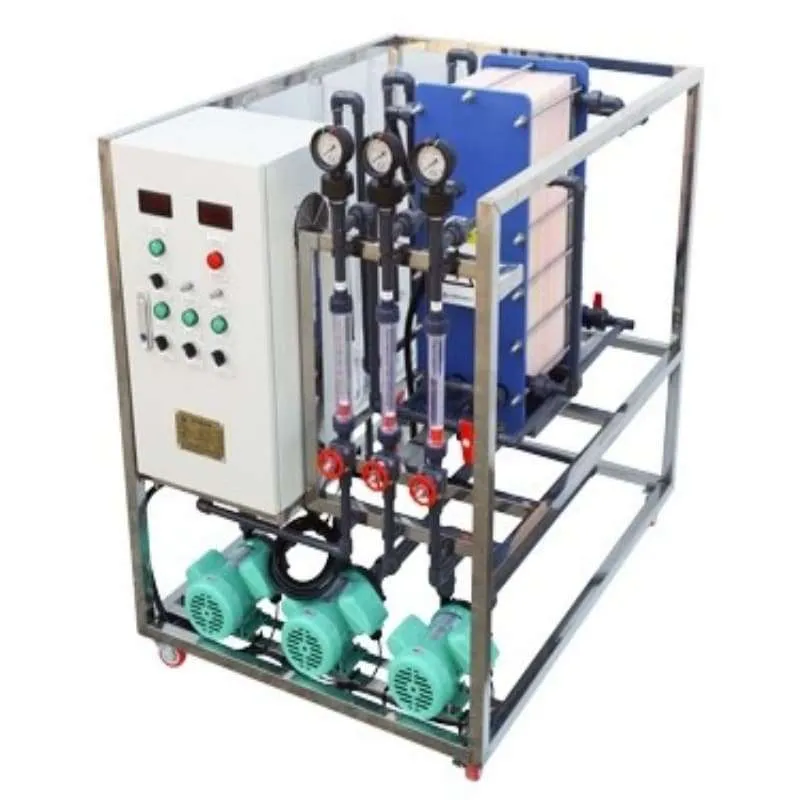
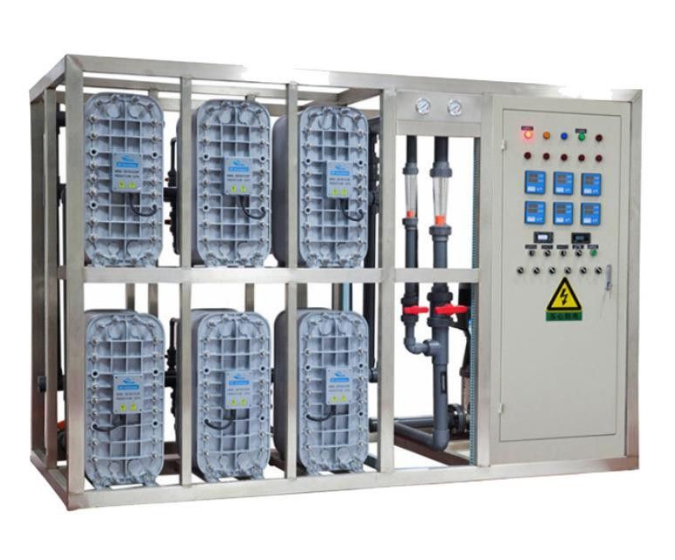
| Electrodeionization (EDI) | Capacity: 10 m³/h; Resistivity: 18.2 MΩ·cm at 25°C; Endotoxin removal: >99% |
| UV Sterilizer | UV dose: 40 mJ/cm²; Lamp type: Low-pressure mercury vapor |
Project Outcomes
The implementation of the water treatment system resulted in:
- Compliance: Achieved water quality standards as per GMP guidelines.
- Operational Efficiency: Reduced water consumption by 30% through recycling and reuse.
- Cost Savings: Lowered operational costs by 20% due to energy-efficient equipment and reduced chemical usage.
This case study underscores the importance of advanced water treatment technologies in the pharmaceutical industry to ensure product quality, regulatory compliance, and operational efficiency.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian