




Project Background
In the mining industry, water is essential for various operations, including mineral processing, dust suppression, and equipment cooling. However, mining activities often lead to water contamination, necessitating effective treatment solutions to ensure environmental compliance and operational efficiency.
Project Requirements
The primary objectives for a mining water treatment project include:
- Contaminant Removal: Eliminating heavy metals, suspended solids, and other pollutants from mining wastewater.
- Water Reuse: Facilitating the recycling of treated water for mining processes to reduce freshwater consumption.
- Regulatory Compliance: Meeting environmental standards set by local and international authorities.
- Operational Efficiency: Implementing cost-effective and reliable treatment systems to minimize downtime and maintenance.
Technical Aspects
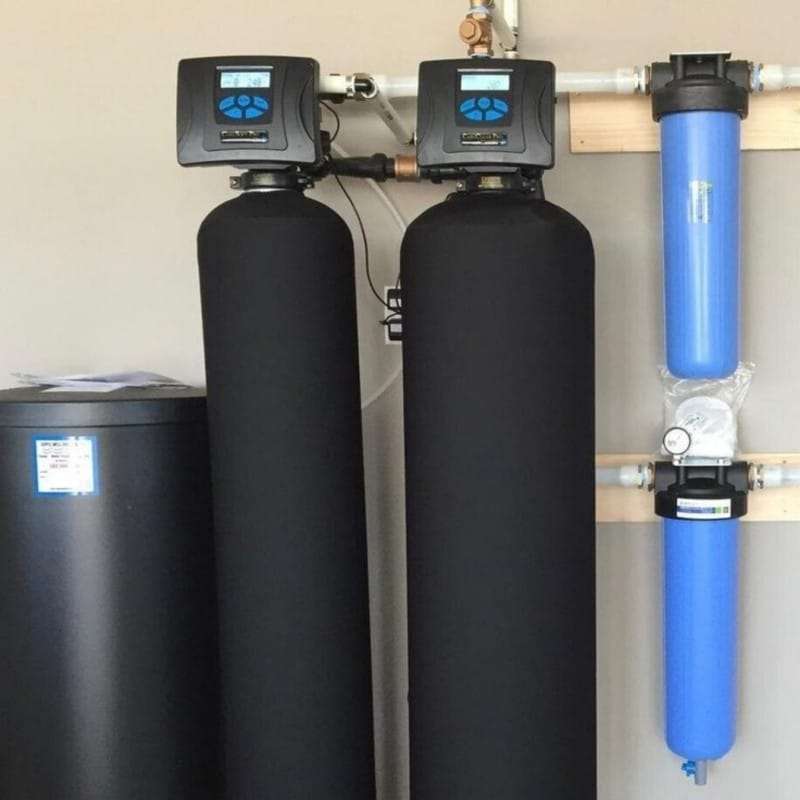
A comprehensive water treatment system for mining operations typically involves several key components:
- Pre-Treatment: Processes such as coagulation, flocculation, and sedimentation to remove large particles.
- Primary Treatment: Techniques like flotation and filtration to eliminate suspended solids.
- Secondary Treatment: Biological methods, including activated sludge processes, to degrade organic contaminants.
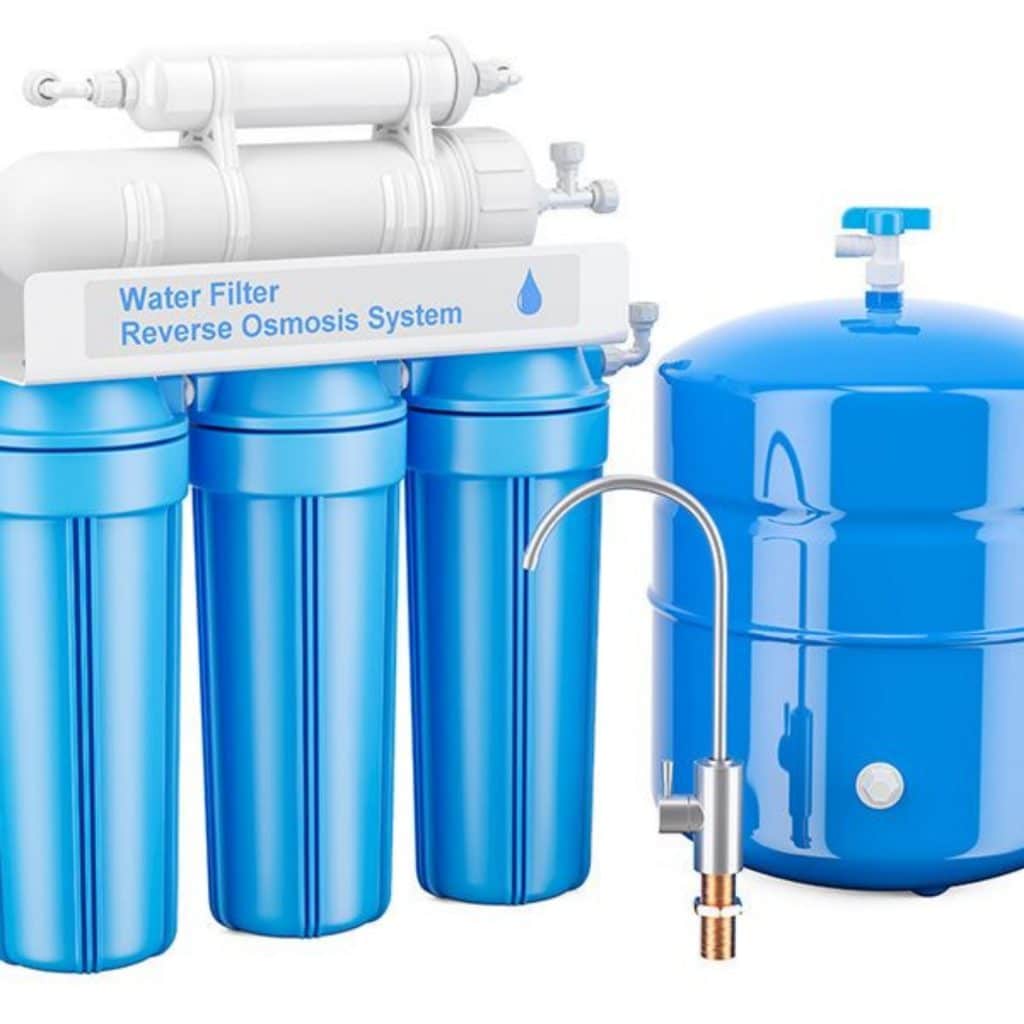
- Tertiary Treatment: Advanced processes such as reverse osmosis or ion exchange to remove dissolved metals and achieve high-quality effluent.
Project Parameters
The specific parameters for a mining water treatment project depend on the nature of the mining operation and the quality of the influent water. Key parameters include:
- Flow Rate: The volume of water to be treated per unit of time.
- Contaminant Concentration: Levels of specific pollutants, such as heavy metals or suspended solids.
- pH Level: Acidity or alkalinity of the water, which affects treatment processes.
- Temperature: Influences the efficiency of certain treatment methods.
Equipment Specifications
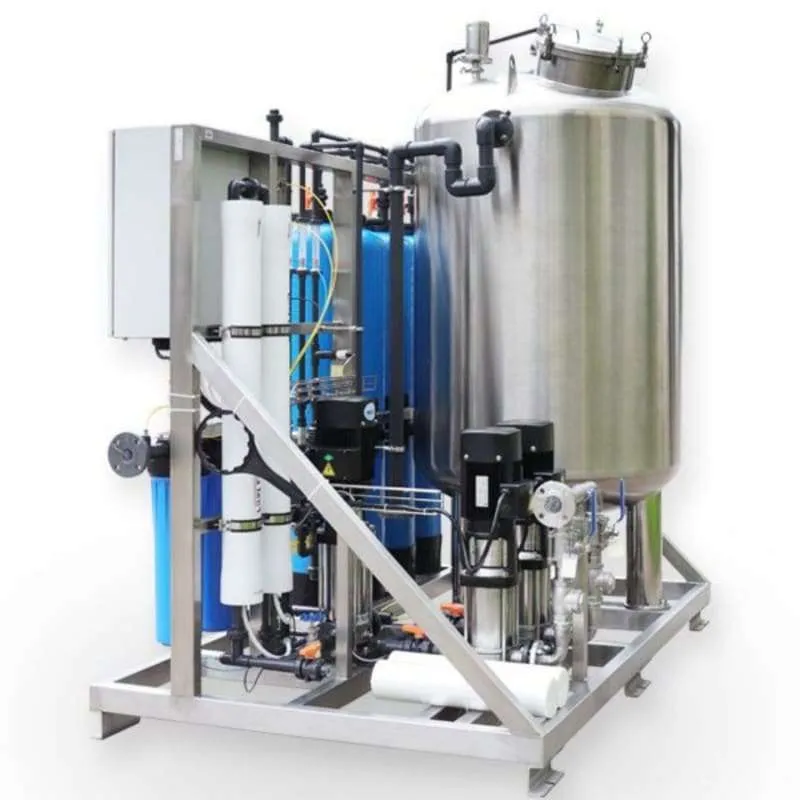
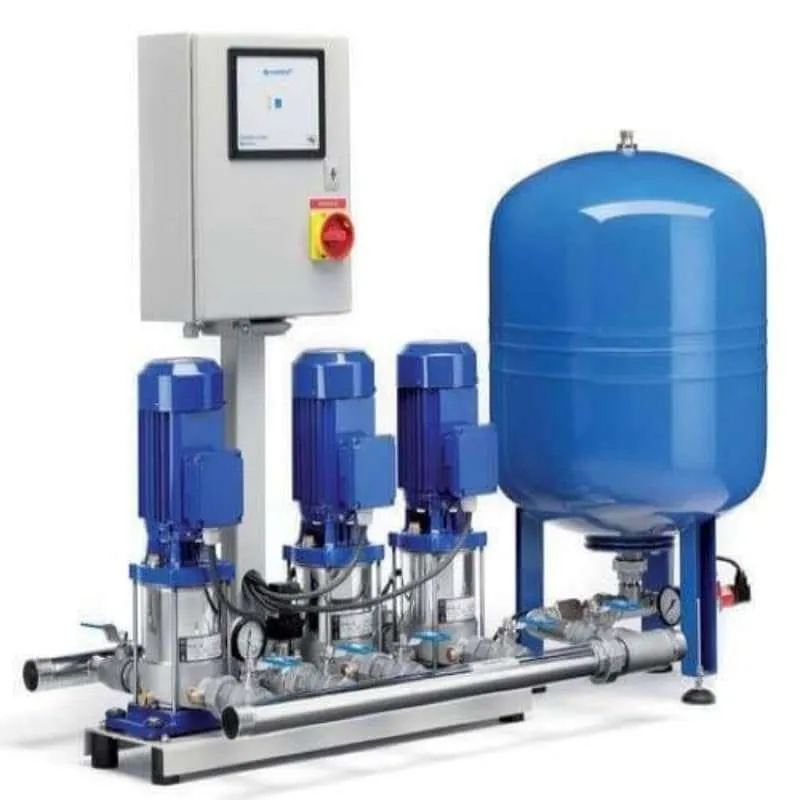
The selection of equipment is crucial for the success of the water treatment system. Commonly used equipment includes:
- Coagulation and Flocculation Units: Designed to mix chemicals with water to form flocs.
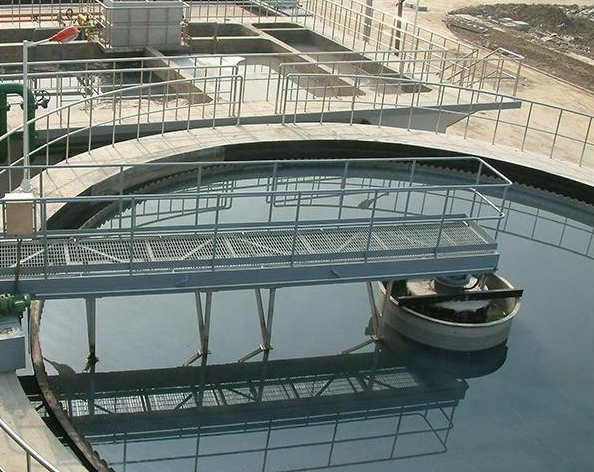
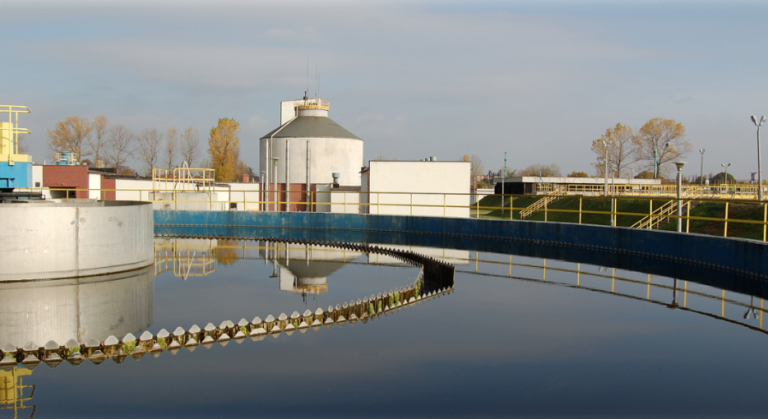
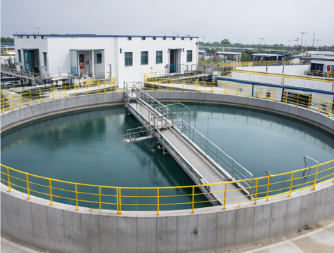
- Sedimentation Tanks: Allow flocs to settle out of the water.
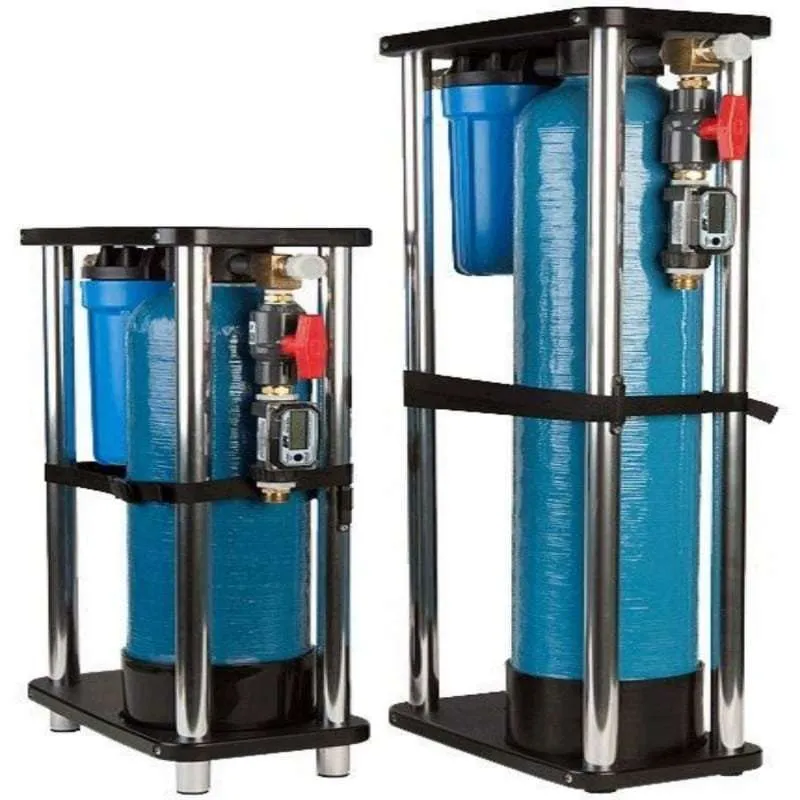
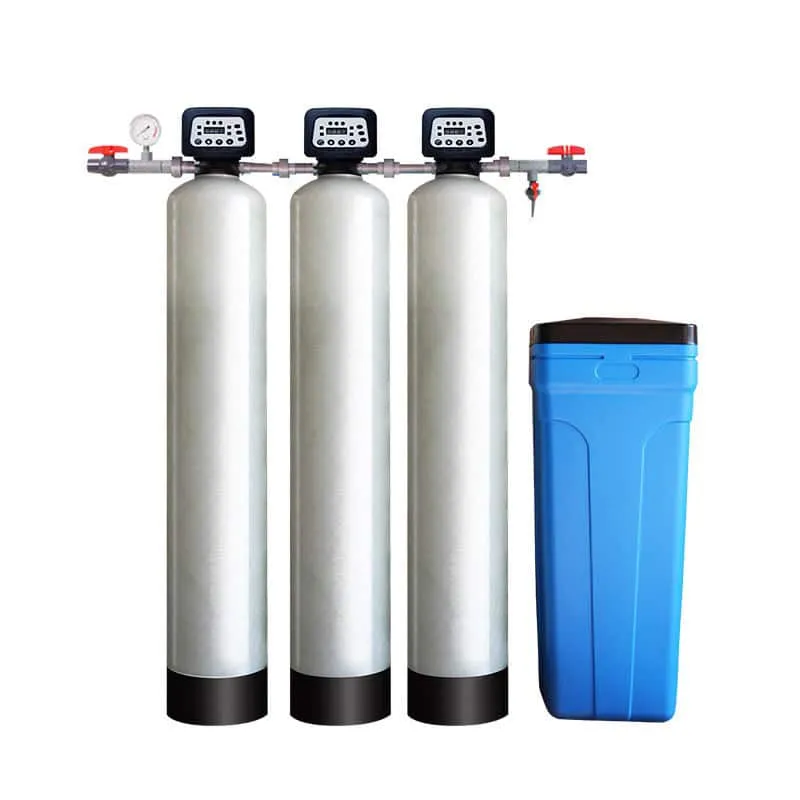
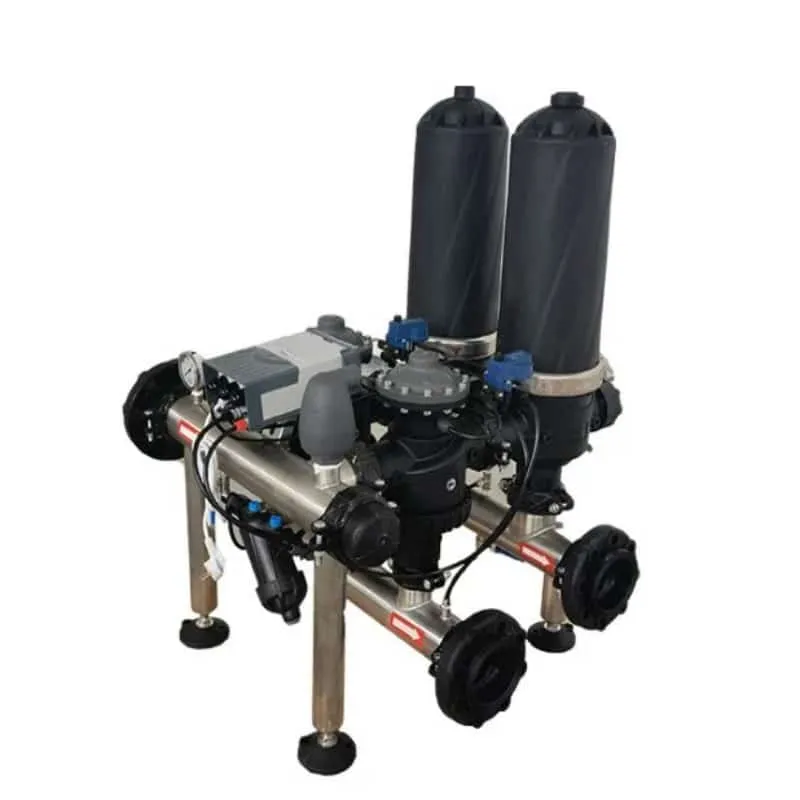
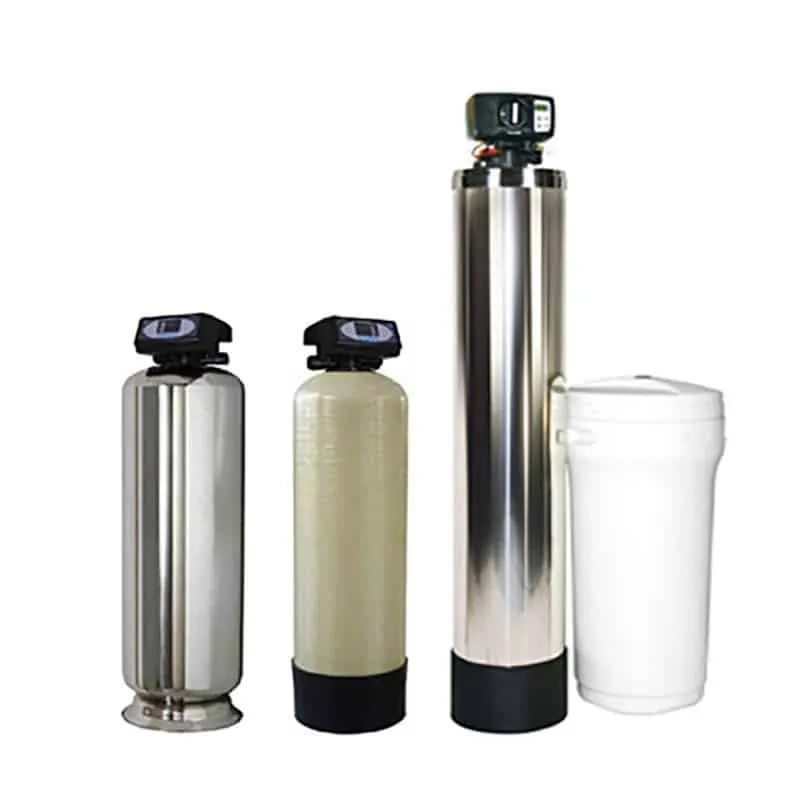
- Filtration Systems: Utilize media filters to remove remaining suspended solids.
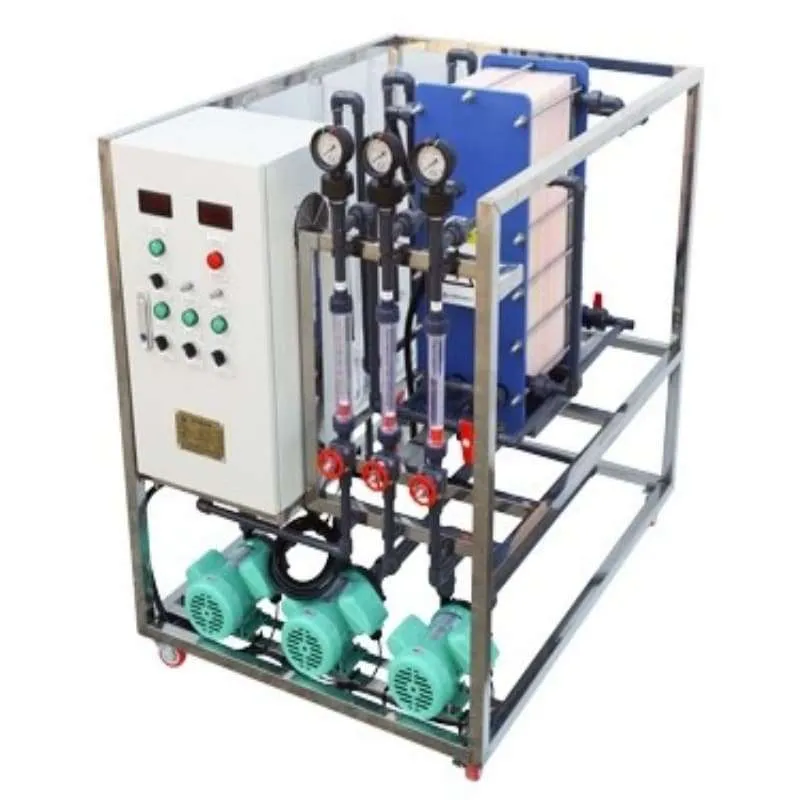
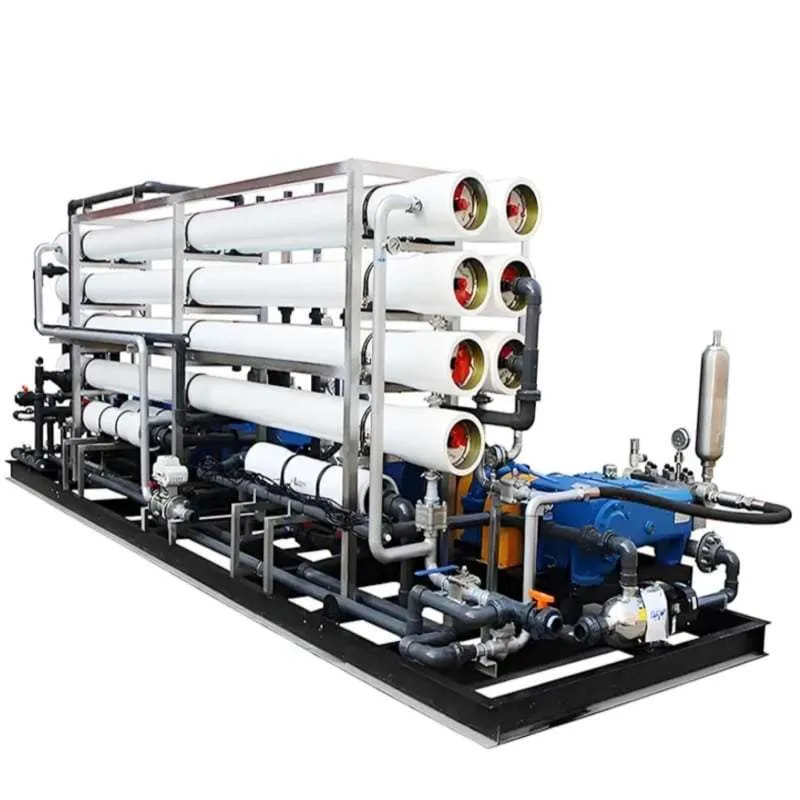
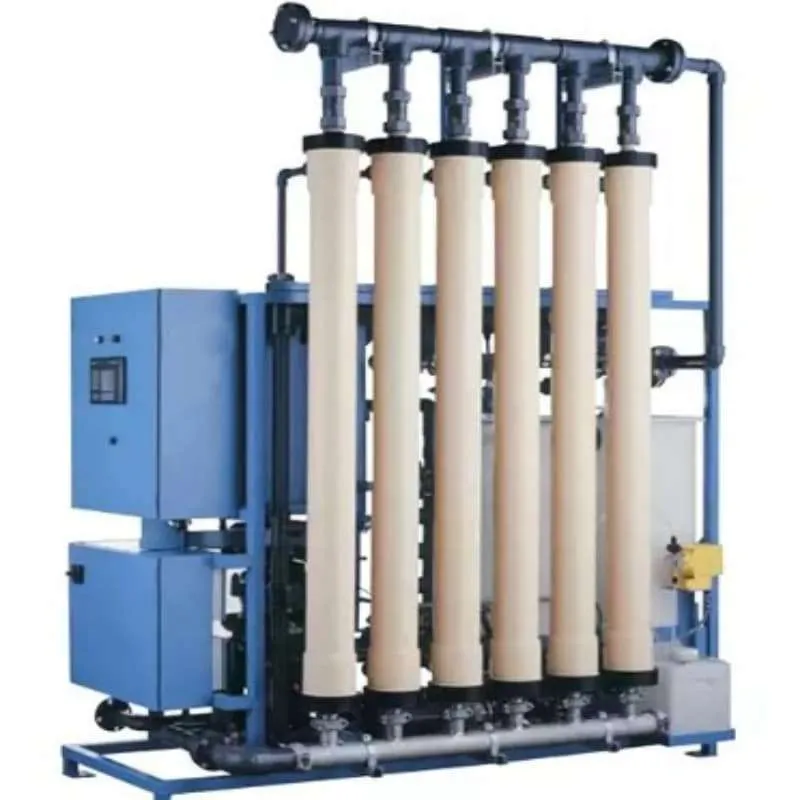
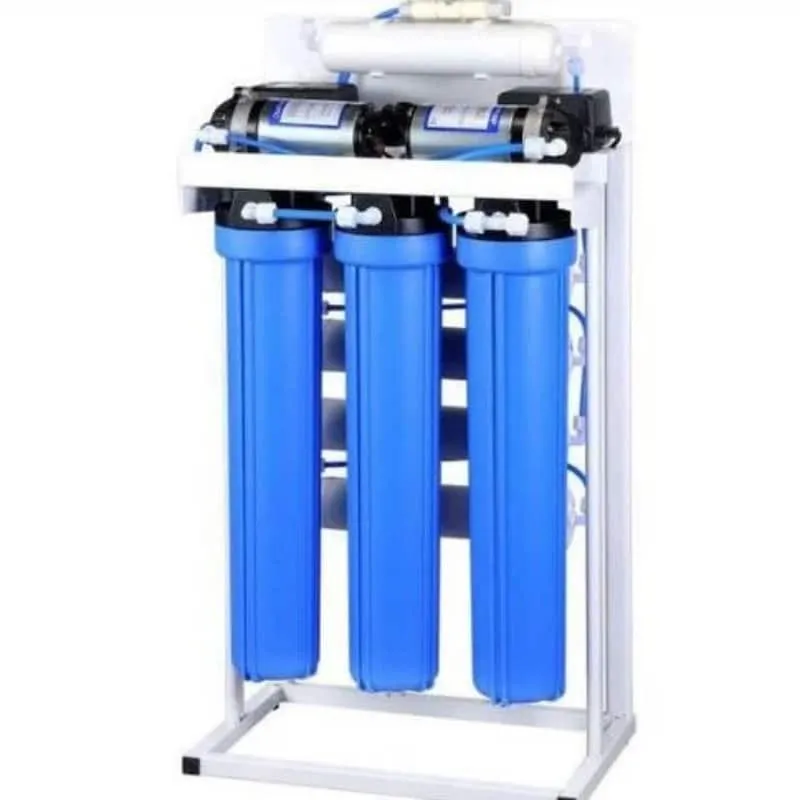
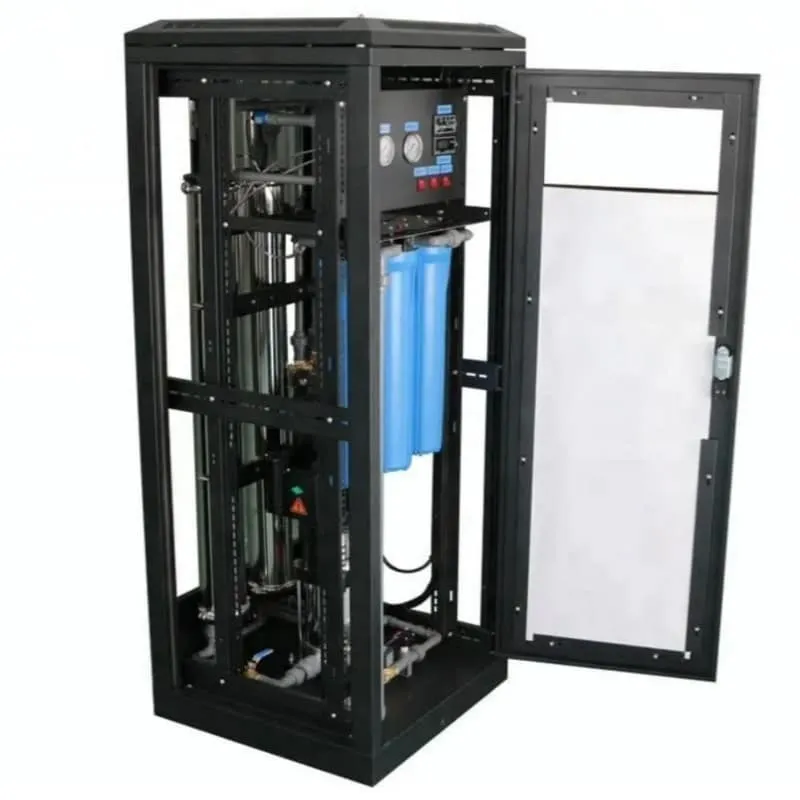
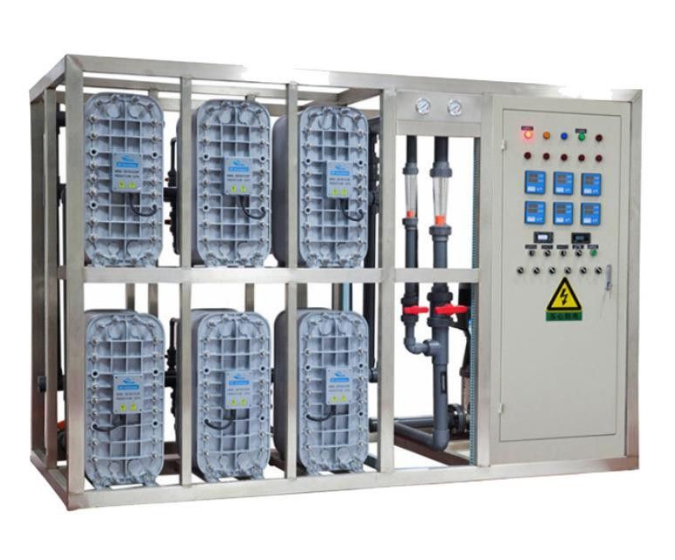
- Membrane Systems: Employ reverse osmosis or nanofiltration to remove dissolved contaminants.
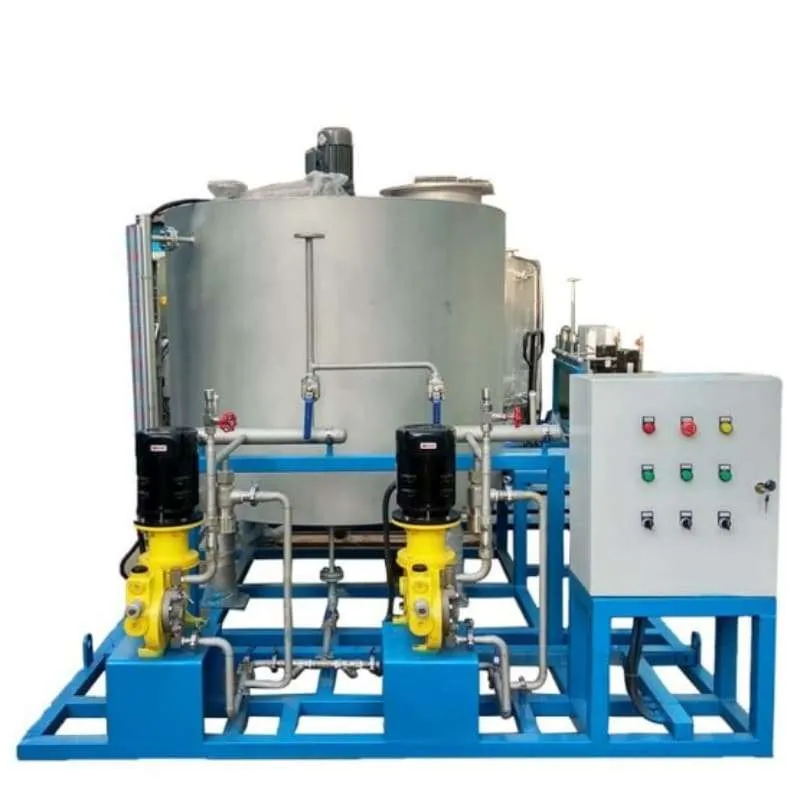
- Chemical Dosing Systems: Add necessary chemicals for coagulation, pH adjustment, or disinfection.
Sample Equipment Specifications Table
| Equipment Type | Model/Specification | Capacity | Features |
|---|---|---|---|
| Coagulation Tank | CT-500 | 500 m³/h | Stainless steel construction |
| Flocculation Unit | FU-300 | 300 m³/h | Adjustable mixing speed |
| Sedimentation Tank | ST-1000 | 1000 m² | High-efficiency sludge removal |
| Sand Filter | SF-200 | 200 m³/h | Multi-layer filtration media |
| Reverse Osmosis Unit | RO-1000 | 1000 m³/day | High rejection rate for heavy metals |
| Chemical Dosing System | CDS-50 | 50 L/h | Automated dosing control |
Project Outcomes
Upon successful implementation of the water treatment system, the mining operation achieved:
- Enhanced Water Quality: Effluent met stringent environmental standards, ensuring safe discharge or potential reuse.
- Cost Savings: Reduced freshwater consumption and minimized penalties for non-compliance.
- Operational Continuity: Improved process reliability and reduced downtime associated with water-related issues.
- Environmental Stewardship: Demonstrated commitment to sustainable mining practices and corporate responsibility.
By integrating advanced water treatment technologies, mining operations can effectively manage water resources, mitigate environmental impacts, and enhance overall operational efficiency.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian