

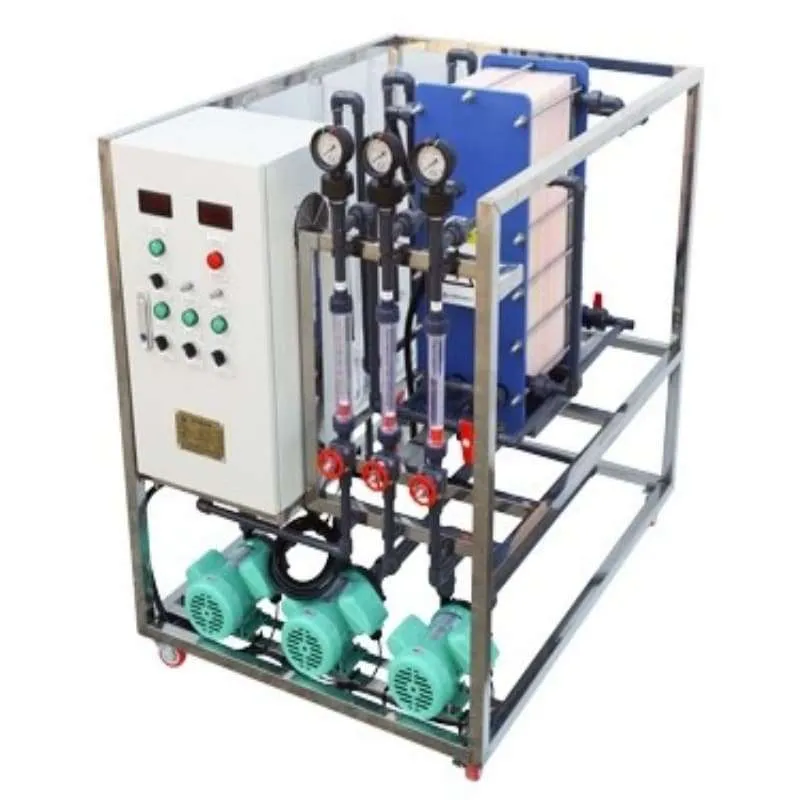
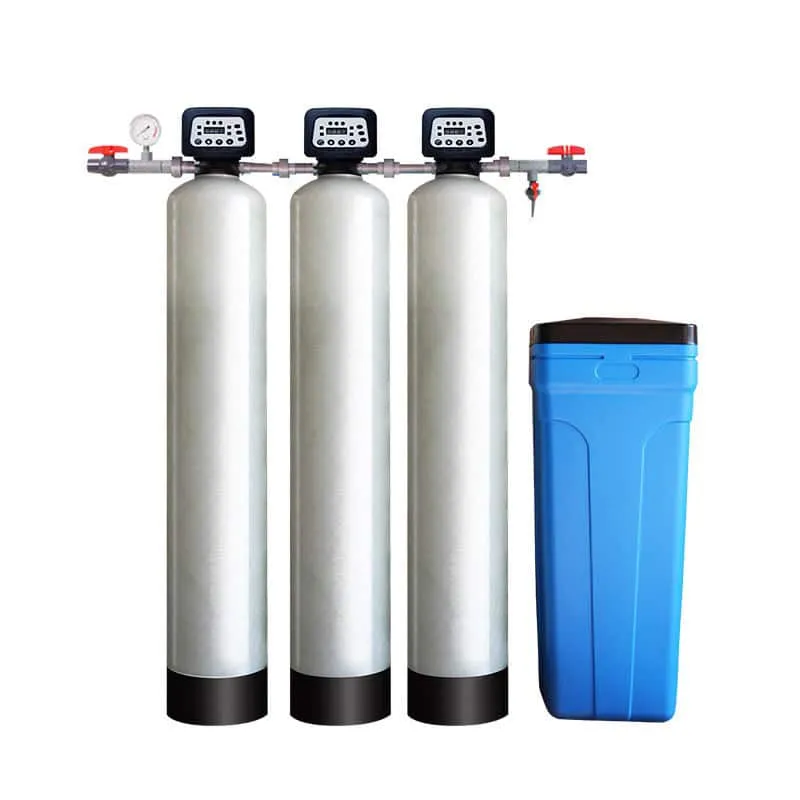
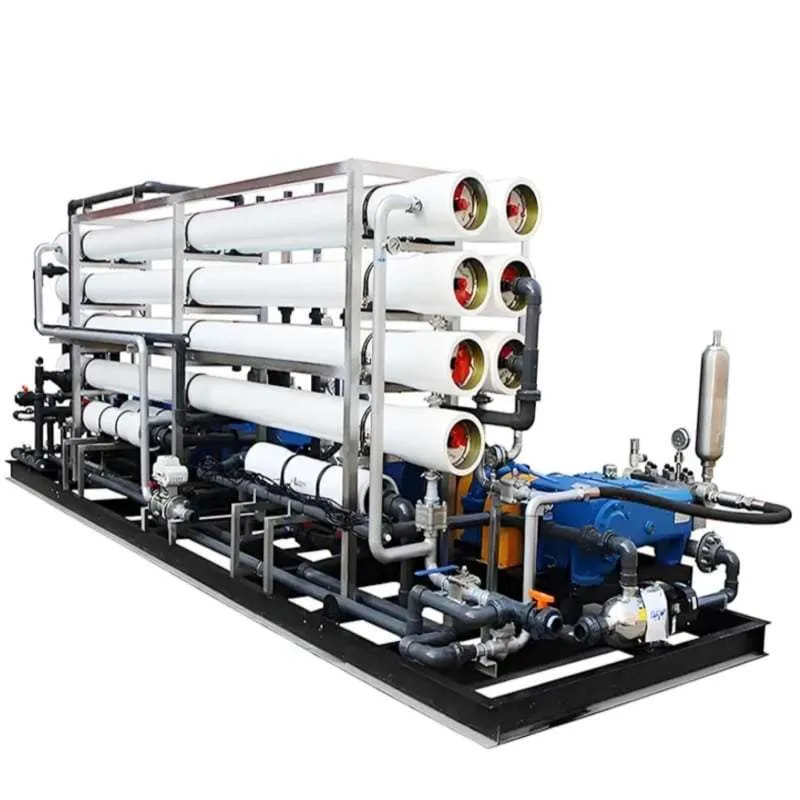
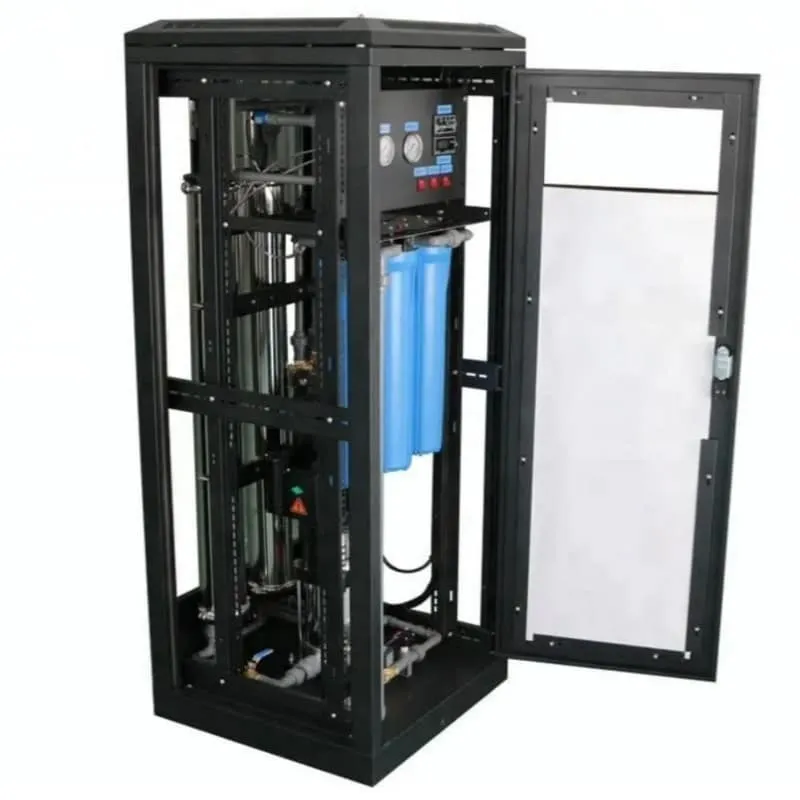

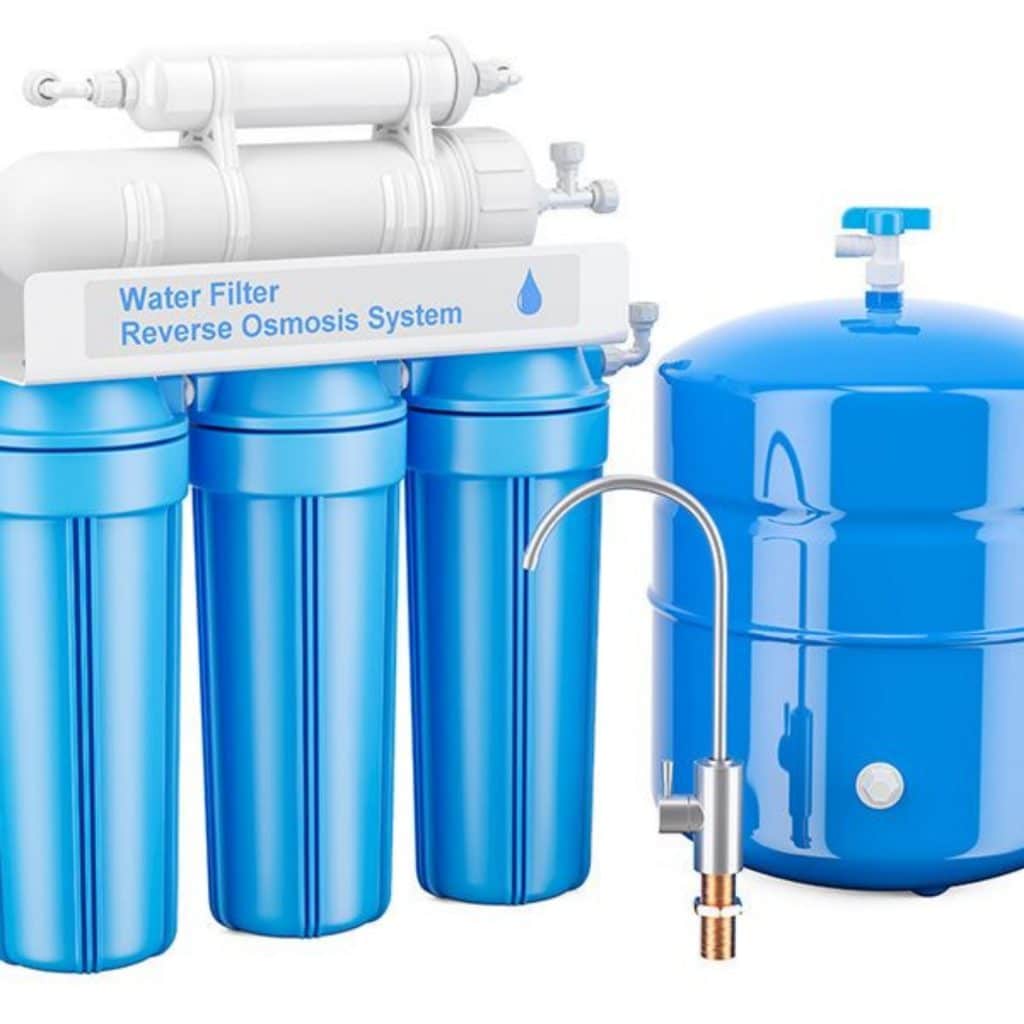


You need high-purity water for making semiconductors. Small particles or chemicals can hurt microchips. You have to follow tough water rules to stop problems. These rules keep your products safe and protect your good name. Knowing the details and daily problems helps you work well. Think about how being green and new ideas can change clean water use later.
Key Takeaways
High-purity water is very important for making semiconductors. It stops problems from happening in microchips. – There are strict rules for water quality, like resistivity and total organic carbon levels. These rules keep the water clean and protect the products. – People check the water often to stop contamination. This helps keep production running well. – Recycling water in fabs can save resources and lower costs. But it needs special treatment methods. – Using new water treatment technology can make things work better. It also helps meet future purity rules.
High-Purity Water Requirements

Definition and Purity Levels
High-purity water is needed to make semiconductors. This water must be very clean. Even tiny bits of dirt or chemicals can cause trouble. In your factory, you use ultrapure water for almost every job. You use it to clean wafers and rinse tools. Ultrapure water goes through many steps to get rid of minerals, particles, bacteria, and organic stuff. You check its quality by looking at a few important things.
Here is a table that shows the usual standards for ultrapure water in semiconductor manufacturing:
Parameter | Specification |
|---|---|
Resistivity | 18.2 MΩ·cm at 25°C |
Total Organic Carbon (TOC) | < 1 ppb |
Particle Count | < 1 particle/mL (> 0.05 µm) |
Bacteria Levels | < 0.1 CFU/mL |
Dissolved Oxygen | < 5 ppb |
Silica | < 0.5 ppb |
You often see these rules in industry guides like SEMI F63 and ASTM. For example, SEMI F63 says ultrapure water should have 18.2 MΩ·cm resistivity. This is the highest value for water at room temperature. It means there are almost no ions left in the water. You also keep TOC below 1 part per billion to stop organic pollution. The particle count must be very low, with less than one particle per milliliter above 0.05 microns. These numbers show how strict the rules are for high-purity water in your work.
Why Purity Matters
Ultrapure water helps keep your products safe from defects. Even a small bit of dirt can cause big problems. If particles or chemicals touch a wafer, they can make surface defects. These defects lower the yield and may ruin whole batches. Organic stuff can block light during photolithography, which makes bad patterns and broken chips. Some impurities react with chemicals used in making chips, causing more problems.
You must watch water quality at every step, from making it to using it. If you use the wrong pipes or tanks, new dirt can get in. High-purity plastics like fluoropolymers help stop this. You also need to check water quality all the time. If the quality drops, wafers can get dirty, cleaning may not work, or equipment can break.
Water quality management costs a lot in semiconductor manufacturing because you need so much ultrapure water to make chips. Good water management can help lower costs from water shortages and rules, which affects the total cost of making chips.
If you do not keep ultrapure water standards, you pay more. Bad water can waste resources, slow down work, and cause more failures. Your reputation can also get hurt if customers get bad chips. That is why stopping contamination is so important in your factory. By following strict ultrapure water rules, you protect your products, your machines, and your business.
Ultrapure Water Quality Standards

Key Parameters and Limits
You need to watch ultrapure water quality in your factory. Ultrapure water must have very few impurities. These rules help keep wafers safe from damage. You check a few important things to see if your water is good.
Here is a table that lists the main things you check, where you check them, and how you test them:
Parameter | Measured (POD/POC) | Test Method |
|---|---|---|
TOC | Online | Conductivity/CO2 |
Total Silica | Lab | ICP-MS or GFAAS |
Particle Count | Lab | SEM – capture filter at various pore sizes |
You need high resistivity, usually above 18 MΩ·cm. This means your water has almost no ions. TOC must be very low, under 1 part per billion. Silica should be less than 10 ppb for the best water. There should be fewer than 1 particle per milliliter if the particle is bigger than 0.2 microns. Bacteria and endotoxins should be almost zero.

The chart shows that ultrapure water for semiconductors has much stricter rules than other water. These rules help you stop expensive problems.
Industry Standards (SEMI F63, ASTM)
You follow industry rules to make sure your ultrapure water is good enough. SEMI F63 and ASTM D5127 are the main guides for ultrapure water. SEMI F63 changes every two years to match new chip technology. ASTM D5127 gives the highest grades for ultrapure water. It says resistivity should be 18.2 MΩ·cm, TOC below 1 ppb, and almost no bacteria or particles.
Here is a table that compares the two main rules:
Standard | Key Requirements |
|---|---|
SEMI F63 | Updated every two years to align with the International Roadmap for Devices and Systems (IRDS). |
ASTM D5127 | Most stringent grades target resistivity of 18.2 MΩ·cm, TOC below 1 ppb, total bacteria below 1 CFU/L, and particle counts at 20 nm and smaller. |
You need to keep up with these rules because they change as chips get smaller. Your factory uses special water systems to meet these tough rules. By following these rules, you keep your process safe and your products very good.
Ultrapure Water Production
Treatment Processes
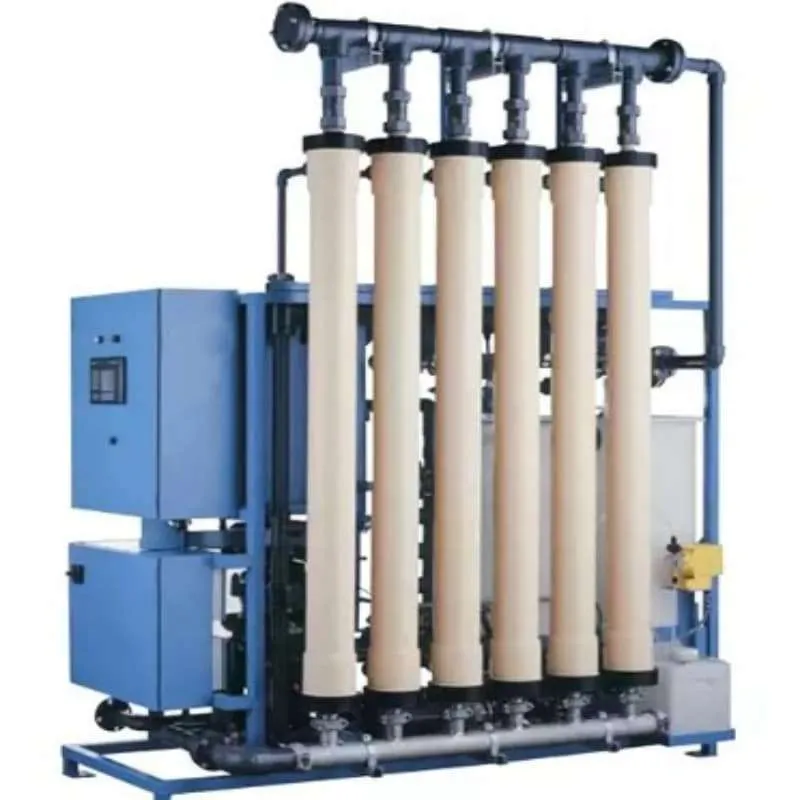
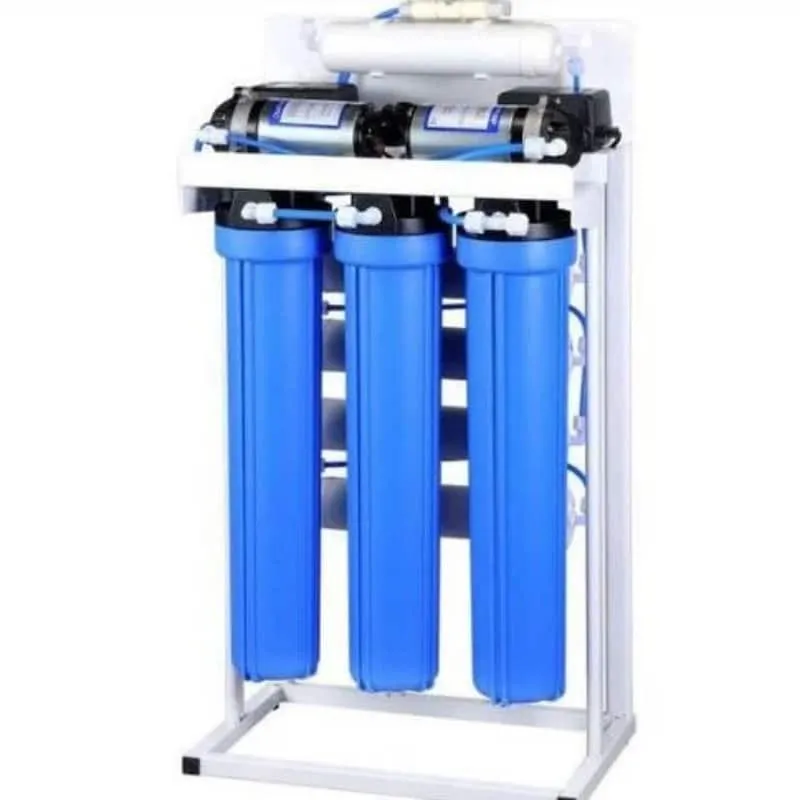
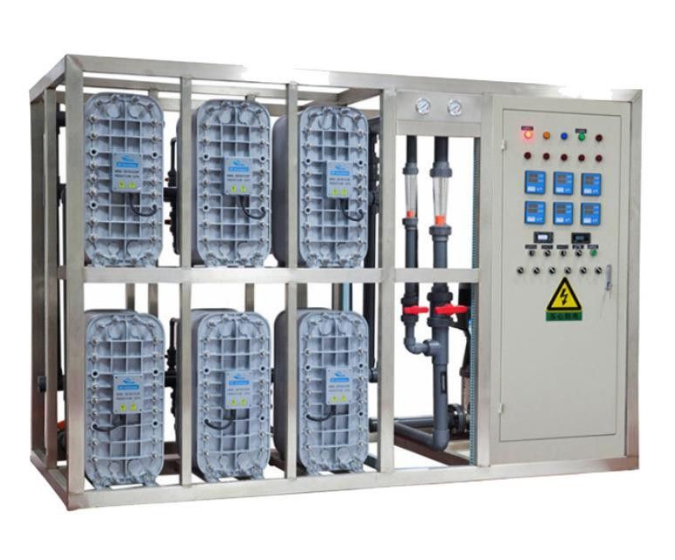
You need ultrapure water for every step when making semiconductors. The water system uses many treatment steps to make water very pure. First, filtration takes out big pieces and dirt. Then, reverse osmosis removes almost all dissolved solids, bacteria, and organic carbon. This step lowers total dissolved solids from 500 ppm to about 5 ppm. After that, ion exchange or electrodeionization takes out almost all ions and silica. This gives water resistivity up to 18 MΩ·cm. Ultraviolet lamps break down organic contaminants. Ultrafiltration gets rid of the last small particles and germs.
Treatment Step | Removal Efficiency |
|---|---|
Reverse Osmosis (RO) | 90–99% of dissolved solids, bacteria, and organic carbon |
Ion Exchange / EDI | Almost all remaining ions, silica, and weakly ionized species, producing DI water with resistivity of 15–18 MΩ·cm |
These steps are needed for careful jobs like chemical mechanical planarization and wafer cleaning. As chips get smaller, you need better water systems. This makes ultrapure water production cost more and become harder to manage.
System Components and Monitoring
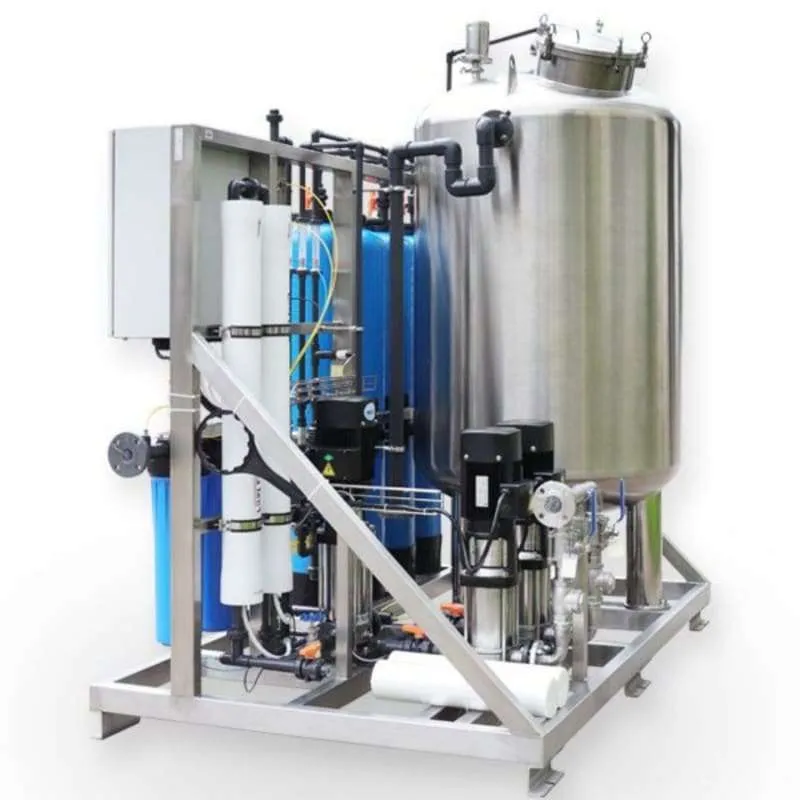
Ultrapure water systems use many parts to keep water clean. Reverse osmosis membranes do the first cleaning. Electrodeionization modules take out ions. UV lamps destroy organic material. Ultrafiltration membranes catch the last particles. Inline resistivity meters and TOC analyzers check water quality right away. Particle counters find even tiny bits.
Component/Method | Description |
|---|---|
Reverse osmosis membranes | Essential for initial purification of water. |
Electrodeionization modules | Further purifies water by removing ions. |
UV lamps | Used for disinfection and to eliminate organic contaminants. |
Ultrafiltration membranes | Removes larger particles and microorganisms. |
Inline resistivity meters | Provides real-time monitoring of water resistivity. |
TOC analyzers | Measures total organic carbon levels in the water. |
Particle counters | Counts particles to ensure water quality meets specifications. |
PLC-based control systems | Automates monitoring and alerts for deviations in pressure, flow, and quality. |
You watch flow, pressure, conductivity, and resistivity at each step. Advanced sensors check temperature and particle levels. These checks help stop problems during chemical mechanical planarization and other important steps. Real-time monitoring keeps ultrapure water within strict rules and protects your products.
Water Use and Recycling in Fabs
Consumption per Wafer and Fab
Making semiconductors uses a lot of ultrapure water. Each wafer needs thousands of liters for cleaning. One 200-mm wafer can use over 2,000 gallons of water. Big fabs can process 40,000 wafers every month. They use about 4.8 million gallons of water each day. Most fabs use between 5 and 10 million gallons daily. This is more water than 33,000 homes use in one day.
Facility Type | Monthly Wafer Processing | Daily Water Consumption (gallons) |
|---|---|---|
Large Fab | 40,000 | 4.8 million |
Typical Fab | 50,000 | 5 to 10 million |
Single Wafer | 1 wafer (200-mm) | Over 2,000 |
You have to watch water use to save money. You also need to follow environmental rules. As chips get smaller, you need even more ultrapure water. This helps stop contamination.
Recycling and Sustainability
Recycling water in fabs is very hard. Some top companies, like TSMC, recycle 87% of their water. Many fabs recycle about 42% of their water. You use special ways to recycle water, such as:
Reverse osmosis
Hollow fiber ultra-filtration
Sand filtration
You must keep ultrapure water very clean after recycling. This makes recycling tricky and expensive. In 2023, TSMC used reclaimed water for 12% of its needs. This helped them reach their goal. But, they still used 25.2% more water per unit that year. This shows it is tough to balance making chips and saving water.
“To help you understand, parts per quadrillion is like having just one molecule of impurity in a whole Olympic swimming pool.” – Prakash Govindan, co-founder and COO of Gradiant
You need to keep making recycling better. Good water management helps you follow rules and protect nature. You help make chip factories more green.
Challenges and Solutions
Operational and Technical Issues
Running ultrapure water systems is tough. You need to keep water clean all the time. You must take out particles, bacteria, and chemicals. These things can hurt wafers. Wet etching needs water with almost no impurities. If you miss even a tiny contaminant, you get defects. This lowers how many good chips you make.
You use physical, chemical, and biological ways to treat wastewater. Old treatment methods often do not meet strict rules. You must spend money on new research to make these methods better. Making ultrapure water costs much more than making drinking water. You pay up to 350 times more for each gallon. Big chip factories use about 10 million gallons every day. Handling this much water is hard and affects the environment.
You also have to follow rules that want zero liquid discharge. These rules help you use less energy by up to 20%. Companies like TSMC reuse millions of metric tons of water each year. They use reclaimed water technology to cut waste and help nature.
You need to keep water very pure and also be green. This means you must upgrade water systems and recycle more water. You must do this without hurting product quality.
Innovations and Future Trends
New technologies help make ultrapure water systems work better. High-efficiency reverse osmosis helps save more water. Multi-stage filtration takes out tiny particles down to 0.1 microns. Continuous electrodeionization removes ions without using chemicals. UV disinfection and ozone treatment kill germs and make water safer.
Innovation Type | Description |
|---|---|
High-efficiency reverse osmosis | Helps save water and makes systems work better. |
Water recycling and reuse | Made for chip factories to save resources. |
Energy-efficient designs | Lowers the impact of cleaning water on the environment. |
Multi-stage filtration | Takes out tiny particles for high purity. |
High-flux and rejection membranes | Makes more water and uses less energy. |
Continuous Electrodeionization (CEDI) | Removes ions without needing chemicals. |
UV disinfection | Kills germs without chemicals. |
Ozone treatment | Cleans water and kills germs with strong oxidation. |
In the future, water purity standards will get even higher. More than 75% of new chip technologies will need ultrapure water. Factories want to recycle over 90% of their water. Smart water management systems will help check water and save more. Modular water systems will help factories grow. Advanced filtration will make systems work over 30% better. More companies will try to use less fresh water to be more green.
You must keep making water systems better to meet new rules and help the environment. New ideas help you stay ahead and make good products.
You need high-purity water to keep wafers safe. Tough water rules help stop defects and make more good chips. Even tiny bits of dirt can make chips work worse. Special cleaning systems and checks keep water clean. Companies spend money on recycling and new tools. Soon, water systems will get smarter and even cleaner.
Ultra pure water stops wafers from getting dirty.
Small impurities can lower how well chips work.
FAQ
What is ultrapure water used for in semiconductor manufacturing?
Ultrapure water is used to wash wafers and tools. This water takes away dirt and chemicals. Clean water helps make sure products work well and last long.
How do you test ultrapure water quality?
You use sensors and lab tests to check water. You look at resistivity, total organic carbon, and particle count. These checks help you follow strict rules and stop contamination.
Why does semiconductor manufacturing need so much water?
You need a lot of water for every step. Washing, rinsing, and cooling all use ultrapure water. Using lots of water helps stop defects and keeps things running smoothly.
Can you recycle water in a semiconductor fab?
You can recycle water with special treatment systems. Recycling saves resources and helps the environment. Many fabs reuse water to cut costs and make less waste.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian