




Project Background
The chemical industry is a cornerstone of global manufacturing, producing a vast array of products essential to modern life. However, this sector is also a significant consumer of water resources and a major generator of wastewater. Effective water treatment is crucial to meet environmental regulations, reduce operational costs, and promote sustainability.
Project Requirements
Our client, a leading chemical manufacturing facility, sought to upgrade its water treatment systems to achieve the following objectives:
- Compliance: Ensure adherence to stringent environmental discharge standards.
- Efficiency: Enhance water reuse capabilities to minimize freshwater consumption.
- Cost Reduction: Lower operational expenses associated with water treatment processes.
Project Technical Details
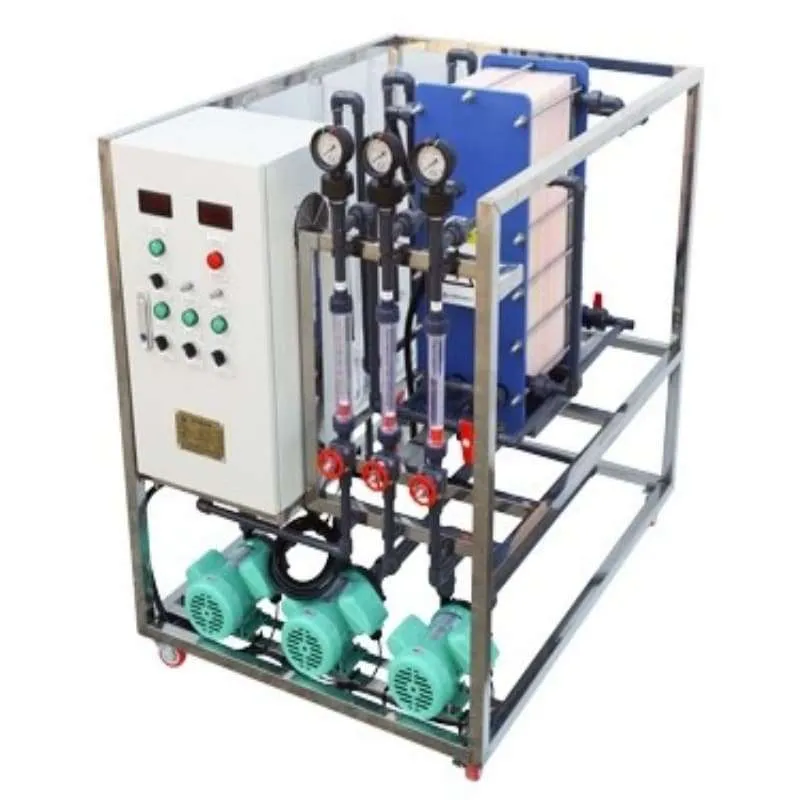
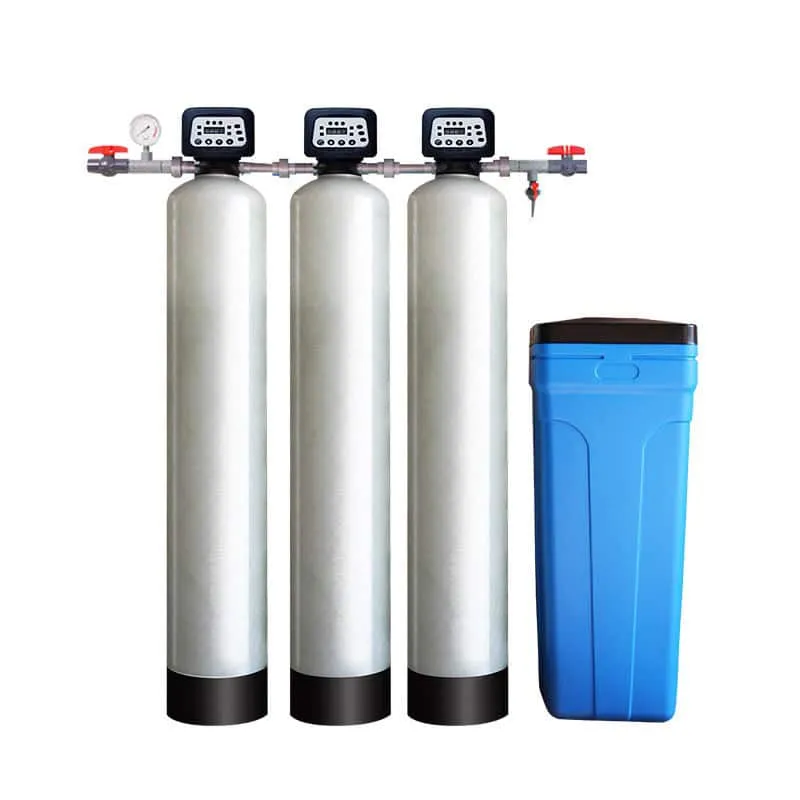
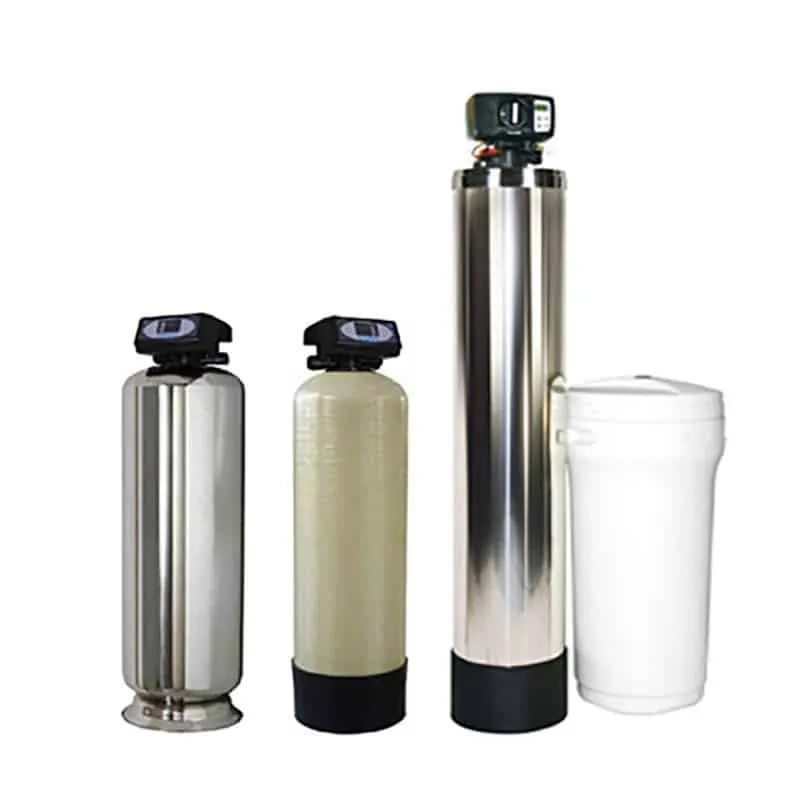
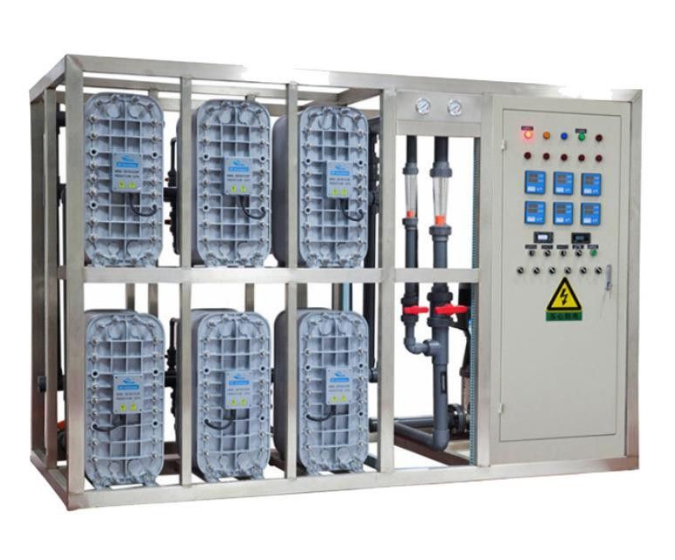
To meet these requirements, we designed a comprehensive water treatment solution incorporating advanced technologies.
Project Parameters:
| Parameter | Specification |
|---|---|
| Source Water Quality | High Total Dissolved Solids (TDS) and Chemical Oxygen Demand (COD) levels |
| Treatment Capacity | 5,000 cubic meters per day |
| Discharge Standards | Compliance with local environmental regulations |
| Water Reuse Target | 80% of treated water for industrial processes |
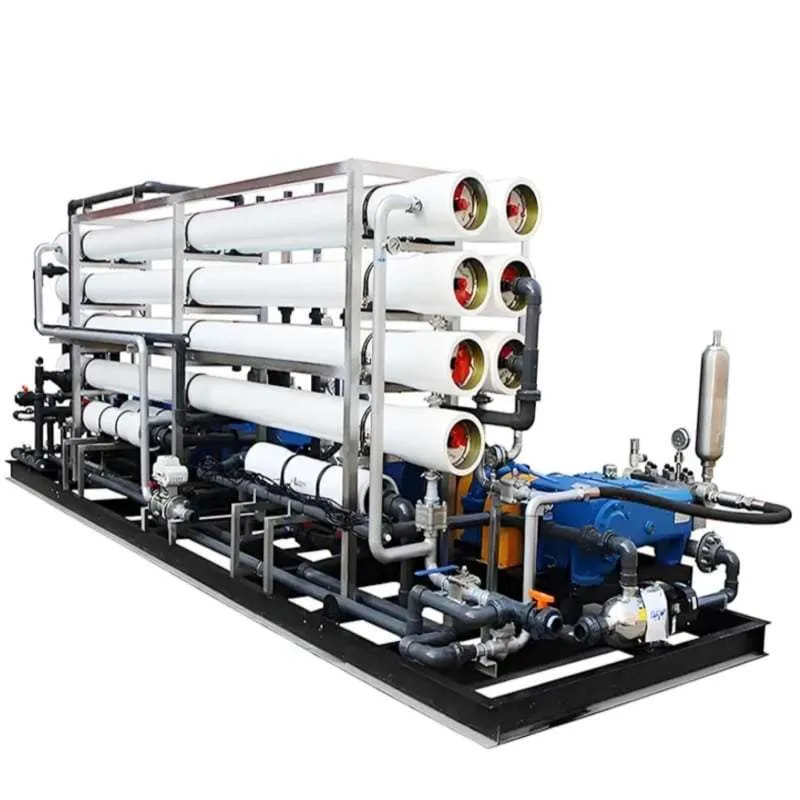
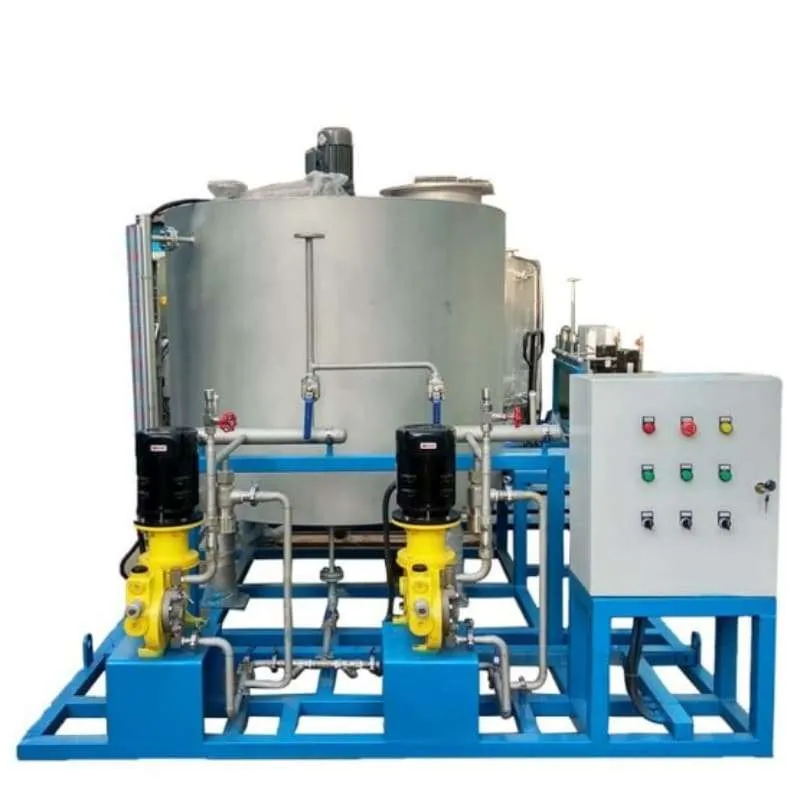
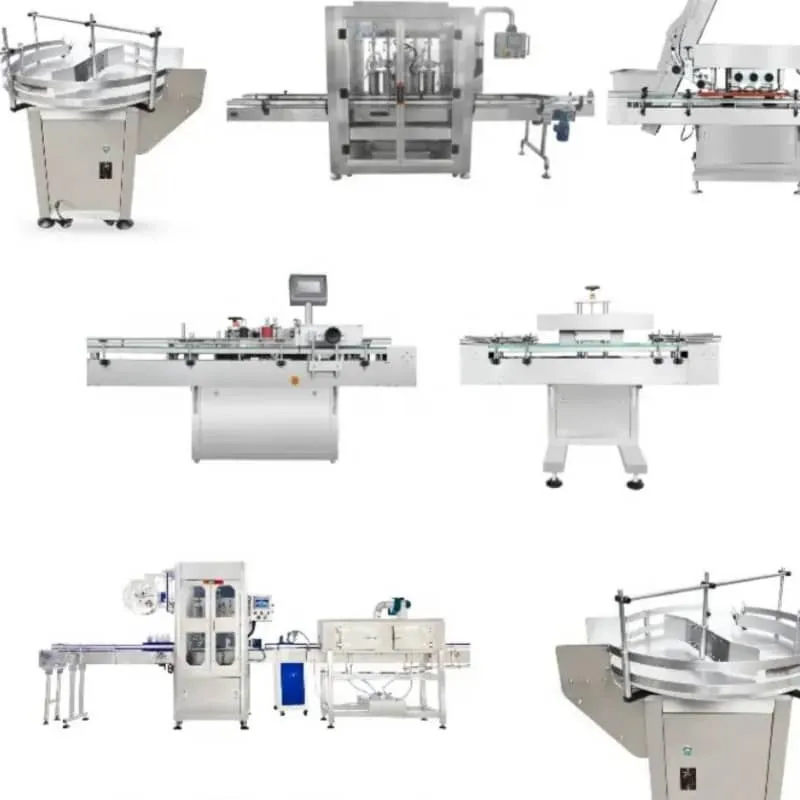
Equipment Specifications:
| Equipment | Specification |
|---|---|
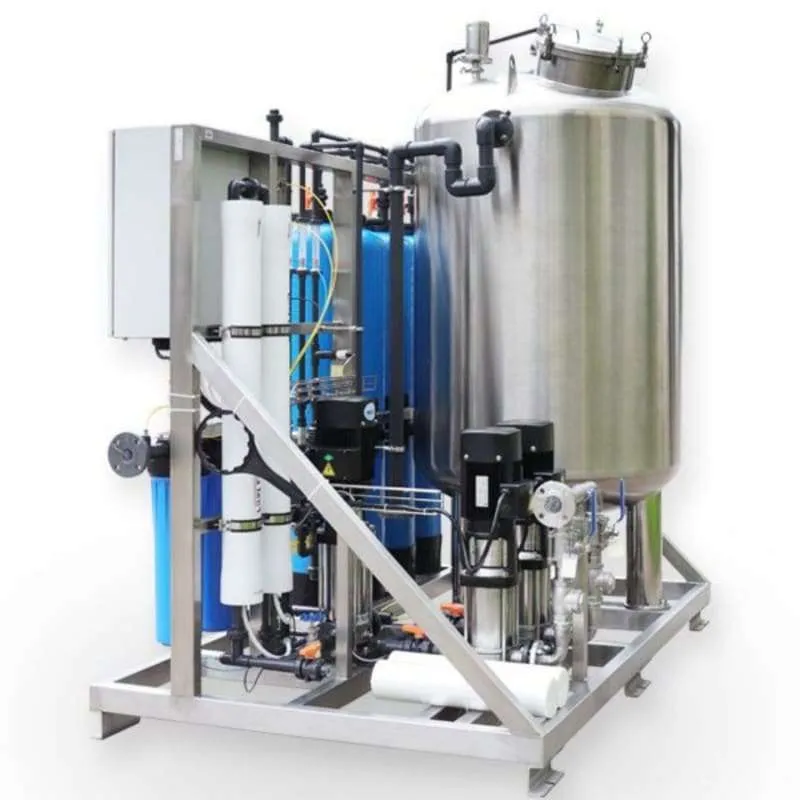
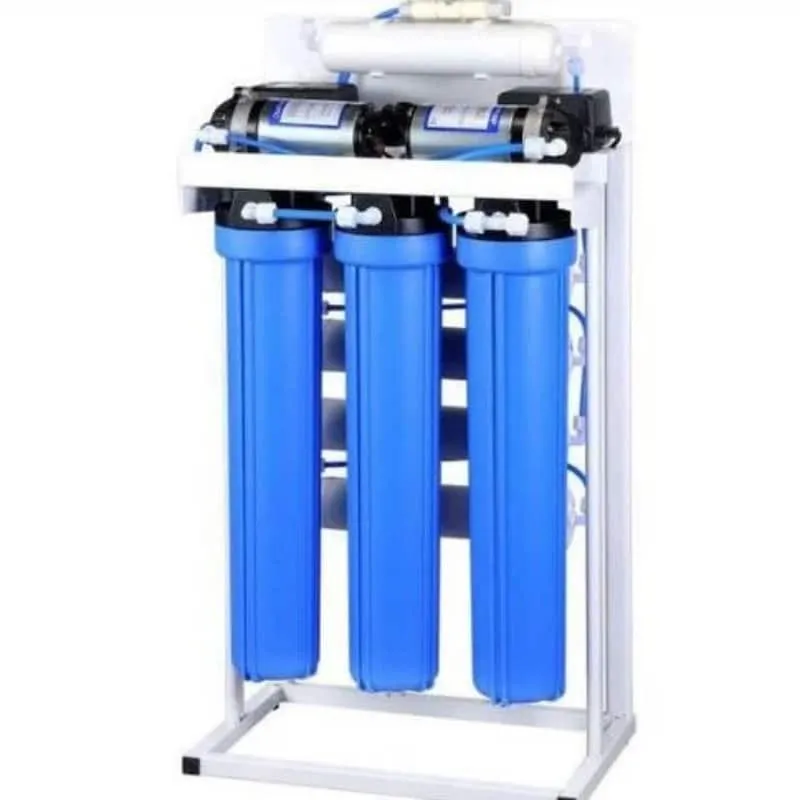
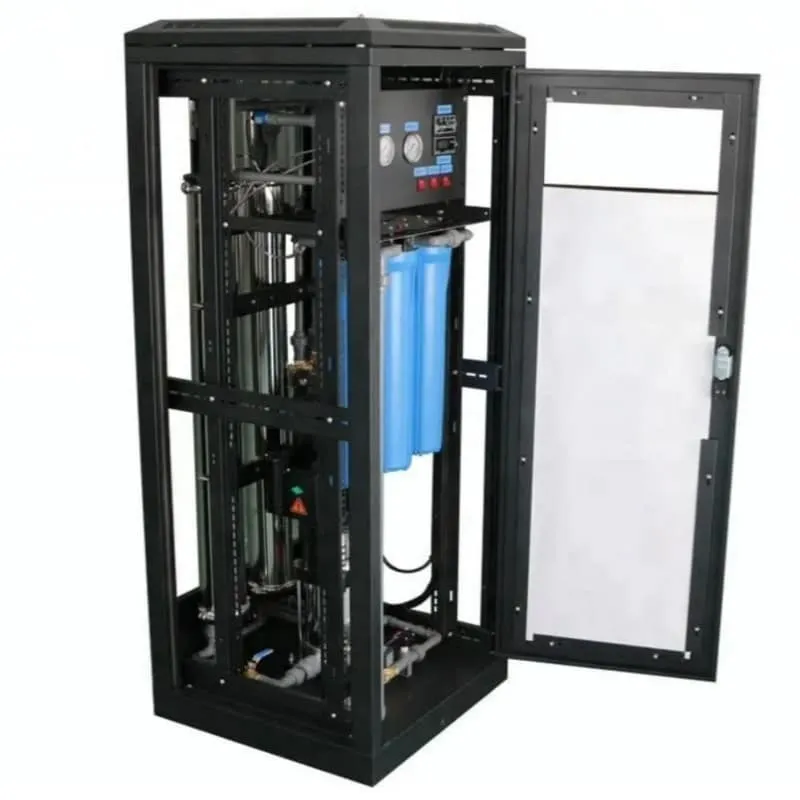
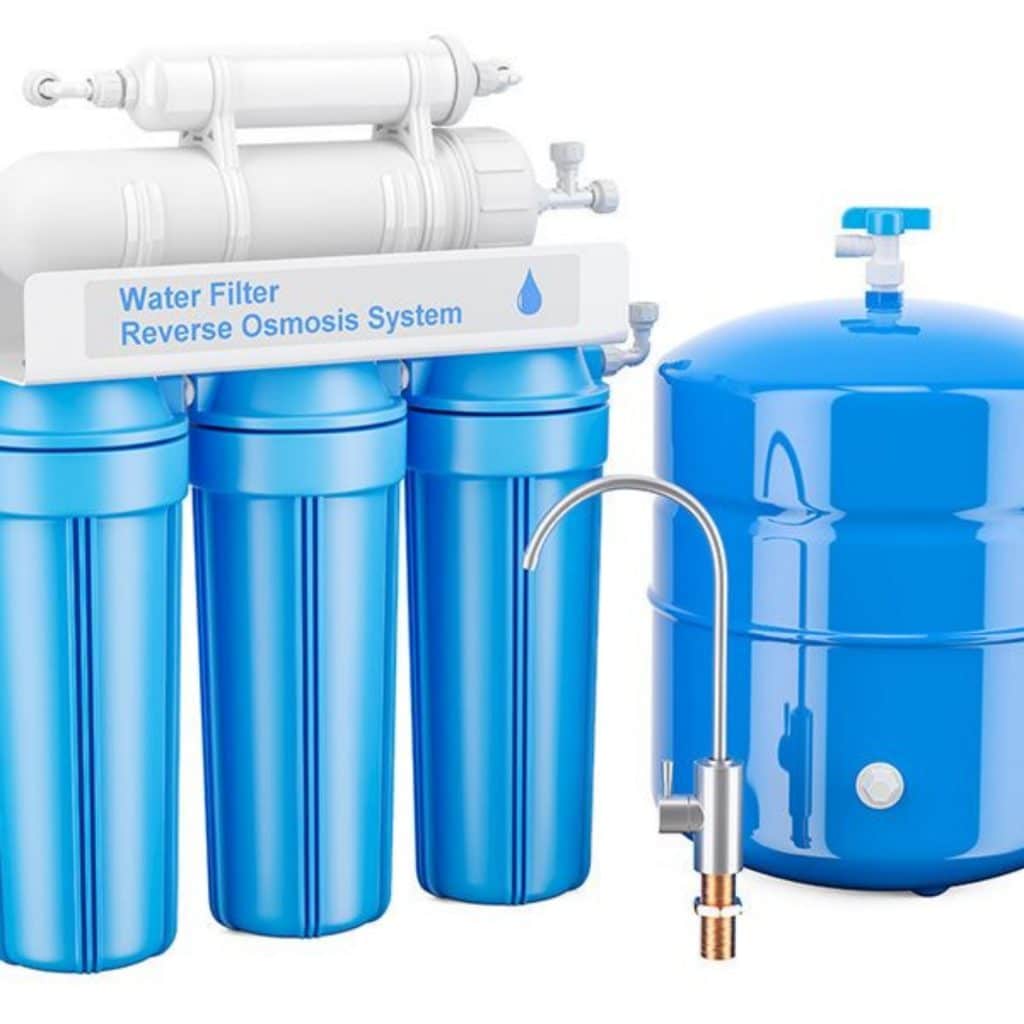
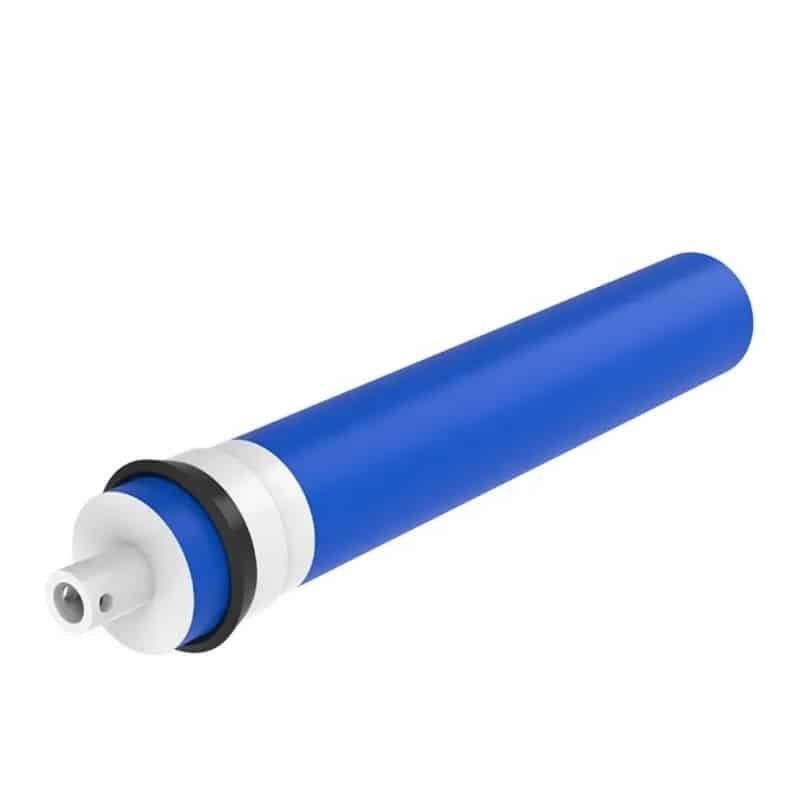
| Reverse Osmosis (RO) System | High-rejection membranes capable of removing 99% of dissolved salts |
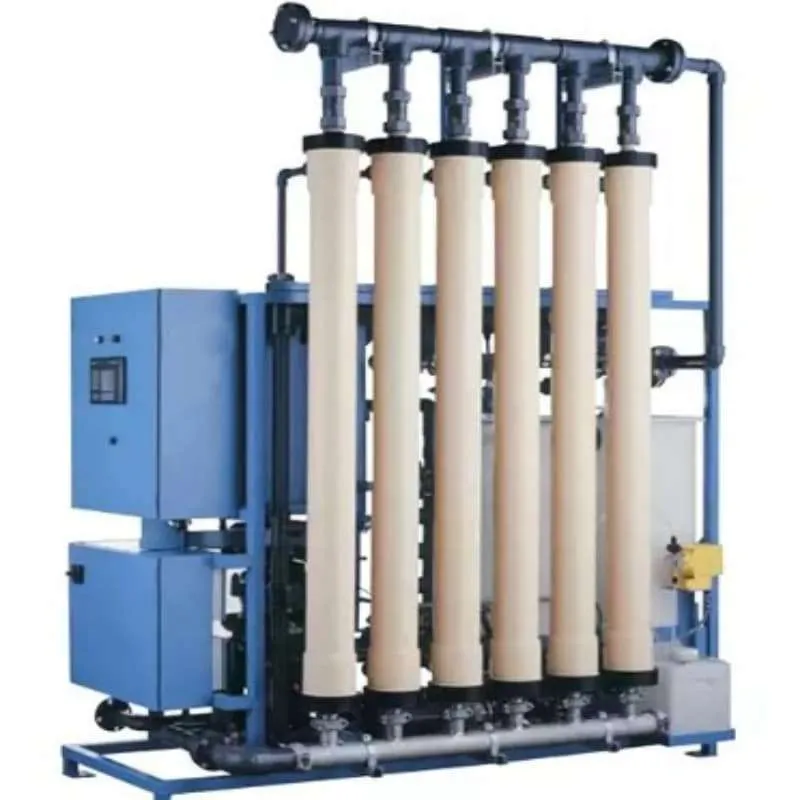
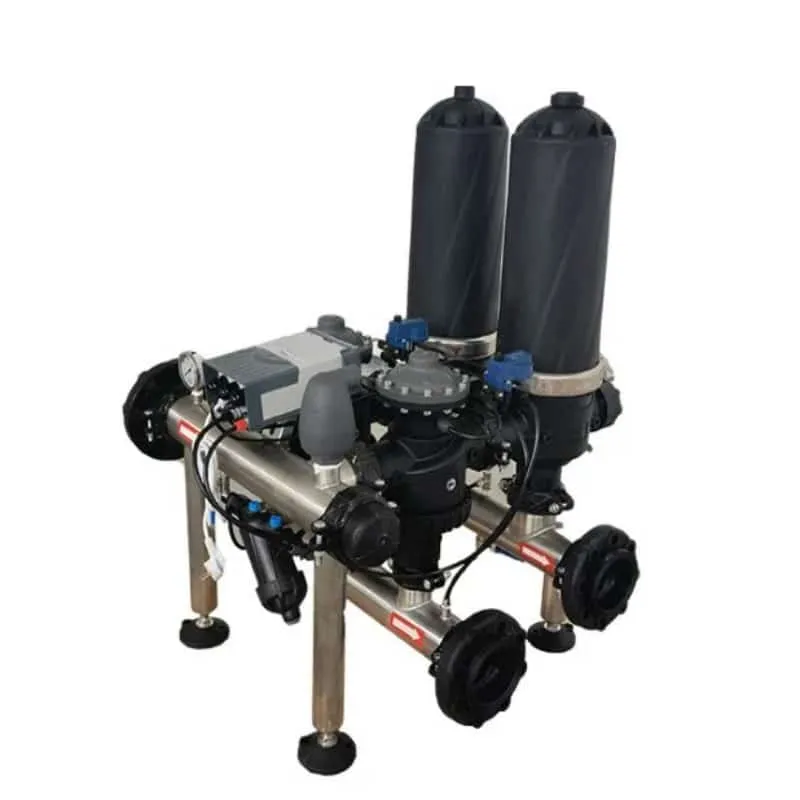
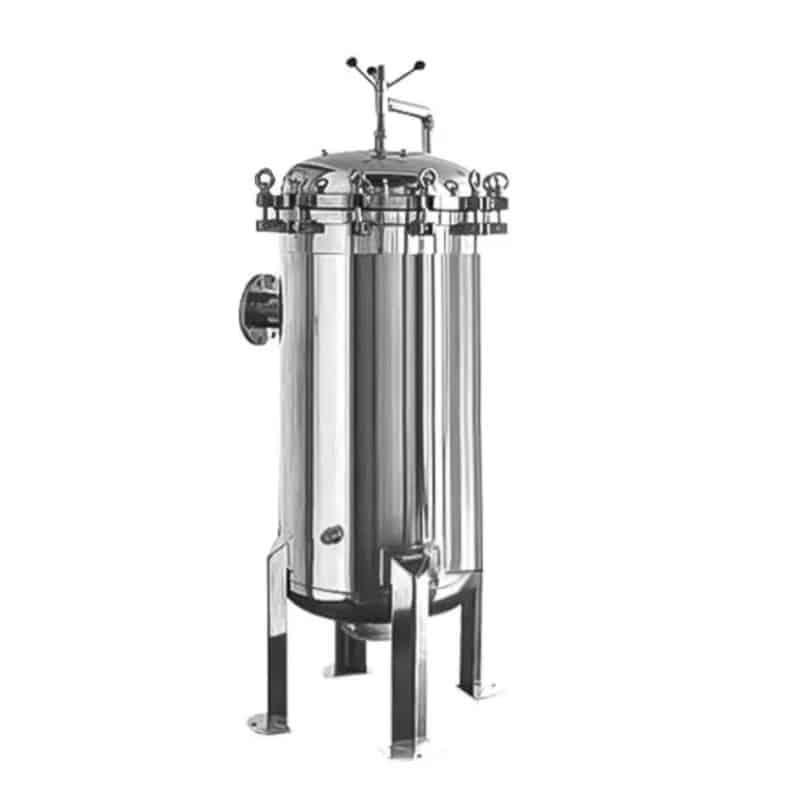
| Ultrafiltration (UF) Units | 0.01-micron pore size for effective removal of suspended solids |
| Chemical Dosing Units | Automated dosing for coagulants and flocculants |
| Sludge Dewatering System | Centrifuge with 85% dewatering efficiency |
| Control System | SCADA-based system for real-time monitoring and control |
Project Outcomes
Upon implementation, the upgraded water treatment system achieved:
- Regulatory Compliance: Effluent quality consistently met environmental discharge standards.
- Water Reuse: Successfully recycled 80% of treated water for industrial use, significantly reducing freshwater intake.
- Cost Savings: Operational costs decreased by 30% due to reduced chemical usage and energy consumption.
This project underscores the critical role of advanced water treatment solutions in enhancing sustainability and operational efficiency within the chemical industry.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian