

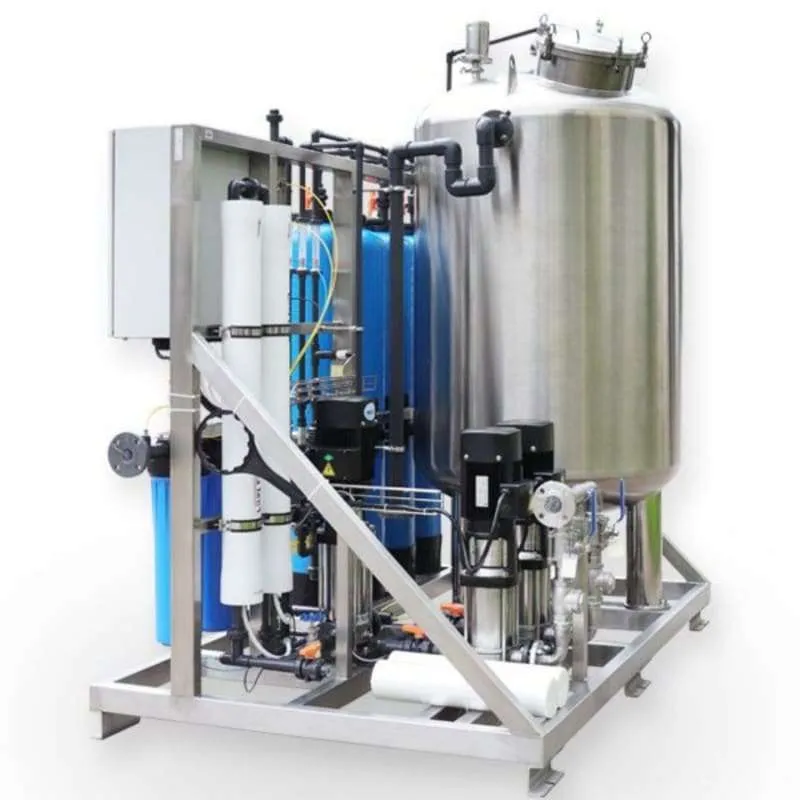

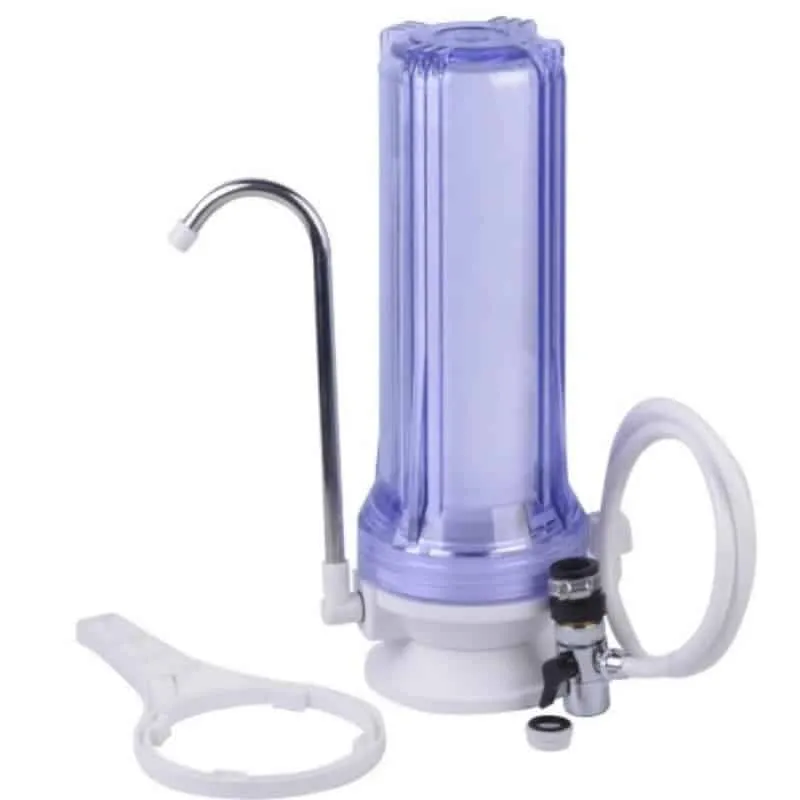

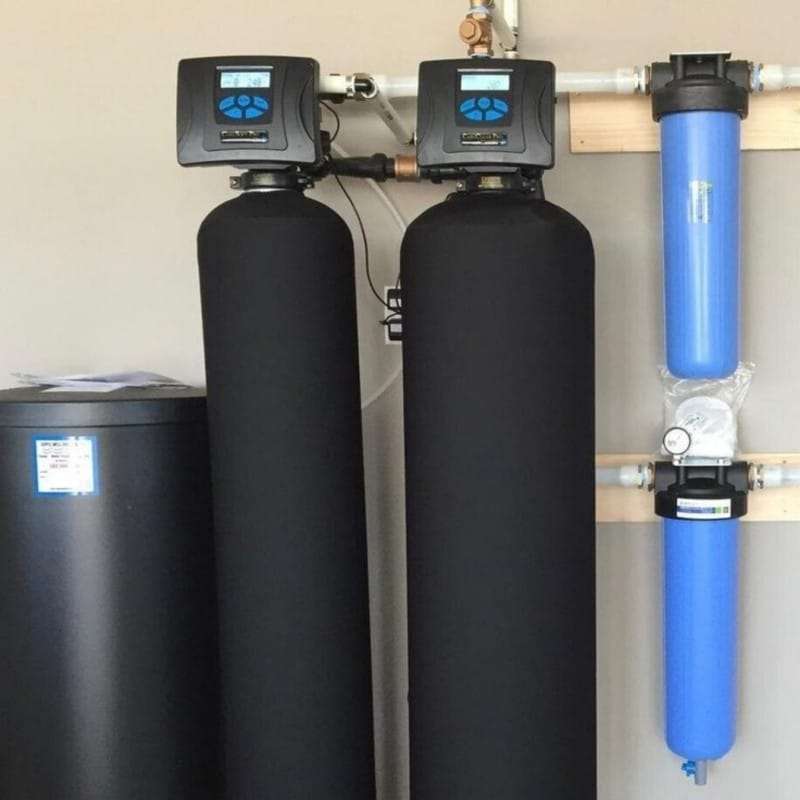

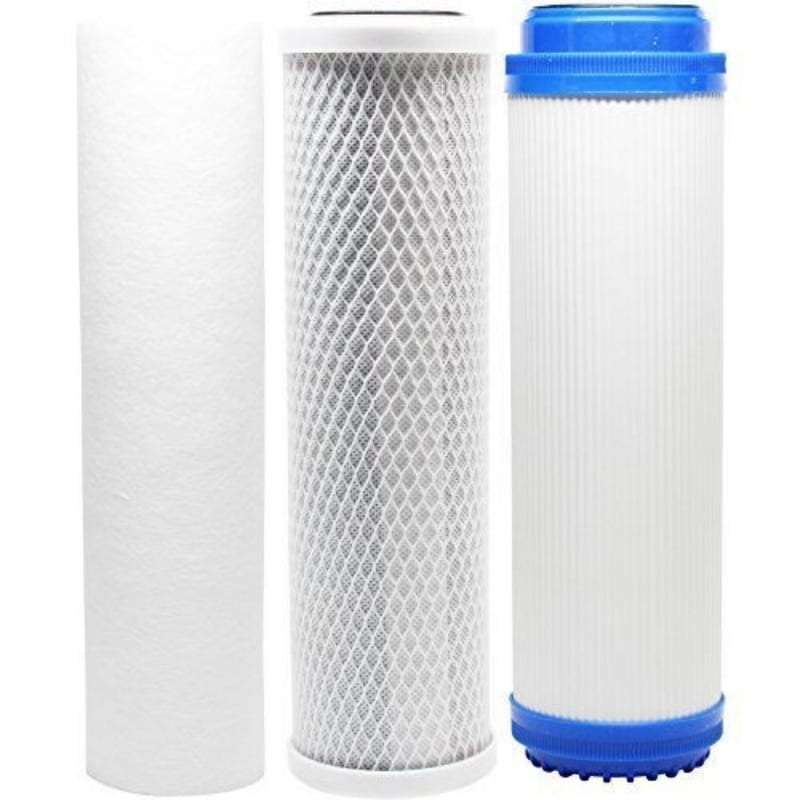
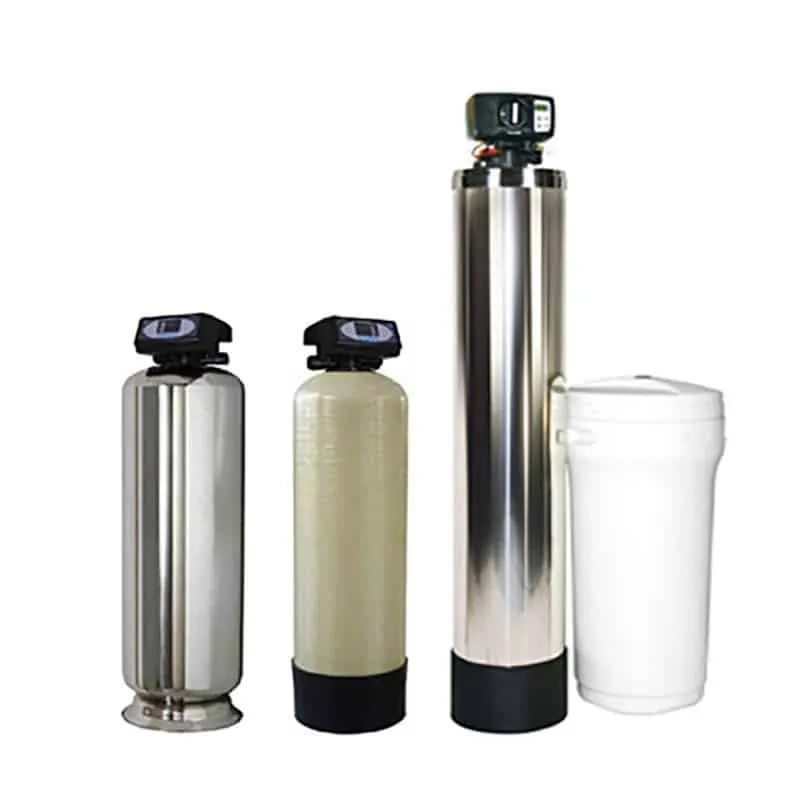
You boost Power Plants performance using two water processes. External cleaning removes raw minerals, floating dirt, and ions. It acts before water enters your system. Internal chemical treatment conditions water inside the boiler loop. This stops heat scale buildup, oxygen rust, and carryover.
Full boiler water treatment protects your important Power Plants equipment. Clean water stops heat-blocking scale from building up. This keeps heat moving well and saves energy. Pure steam turns your turbine smoothly. It will not leave minerals on delicate turbine blades. Good water chemistry prevents bad tube breaks. This keeps Power Plants running safely for a long time.
Key Takeaways
Good water cleaning removes bad minerals.
This stops scale, rust, and costly damage.
Outside filters use special parts to clean water.
They clean raw water before the boiler.
Inside chemicals change pH and remove oxygen.
This protects hot boiler pipes from rust.
Live tracking systems check water purity constantly.
This keeps the plant safe and efficient.
Critical Contaminants in Boiler Feedwater

Raw water carries harmful dirt. Dirt destroys your power machines. You must find these bad items. They stop your plant operations. Good water treatment protects valuable equipment. It keeps power production steady.
Hardness Minerals and Scale Formation
High heat changes calcium and magnesium. Heat turns these minerals into deposits. Four simple steps show scaling:
Decreased Solubility: Hot water drops mineral solubility fast. This forces ions out.
Chemical Conversion: Heat removes carbon dioxide gas. Bicarbonates become carbonates quickly.
Crystallization and Surface Attachment: Minerals turn into solid crystals. They stick to hot metal.
Alkaline Acceleration: High pH creates more carbonate. This speeds up solid deposits.
Fast evaporation leaves behind salty deposits. These layers form hard thermal scale. You need complete scale freedom. Scale traps heat and breaks tubes.
Dissolved Oxygen and Metal Pitting
Dissolved oxygen attacks boiler feedwater systems. Oxygen touches steel and iron parts. Chemical reactions start deep inside. Local activity creates small metal holes. These holes quickly become bad pits.
Chemistry shows this simple process clearly:
Anodic Reaction: Iron turns to ferrous ions. It loses two electrons.
Cathodic Reaction: Oxygen consumes water and electrons. It makes hydroxide ions.
Overall Process: Iron mixes with oxygen. It creates ferrous hydroxide.
Oxygen builds oxide scabs over holes. This cap hides bad metal damage. Pitting continues under the scab layer. Chemical treatments cannot fix hidden spots. Active sites get red oxide caps. Dark black iron forms inside. You must remove all oxygen. Do this before steam loops start.
Silica Volatilization and Volatile Carryover
Silica brings danger at high heat. At 400 psig, silica vaporizes. It goes straight into steam. Over 41 bar, silica dissolves. It turns into steam gas fast.
Silica gas travels with steam currents. It moves into the turbine. Steam cools on turbine blades. Silica turns back to solid. It leaves glassy, hard deposits. Deposits ruin smooth blade aerodynamics. They drop efficiency and shake machines.
Total Dissolved Solids and Chloride Attacks
Total dissolved solids ruin steam purity. Salts create heavy water foam. Steam carries salty liquid droplets out. Droplets leave solids on superheater tubes.
Chloride ions cause stress corrosion cracking. Chlorides break steel oxide films fast. Thermal stress creates deep cracks. You must control all chemical levels. This stops bad chloride attacks. It prevents sudden equipment loss.
External Boiler Feed Water Treatment Systems

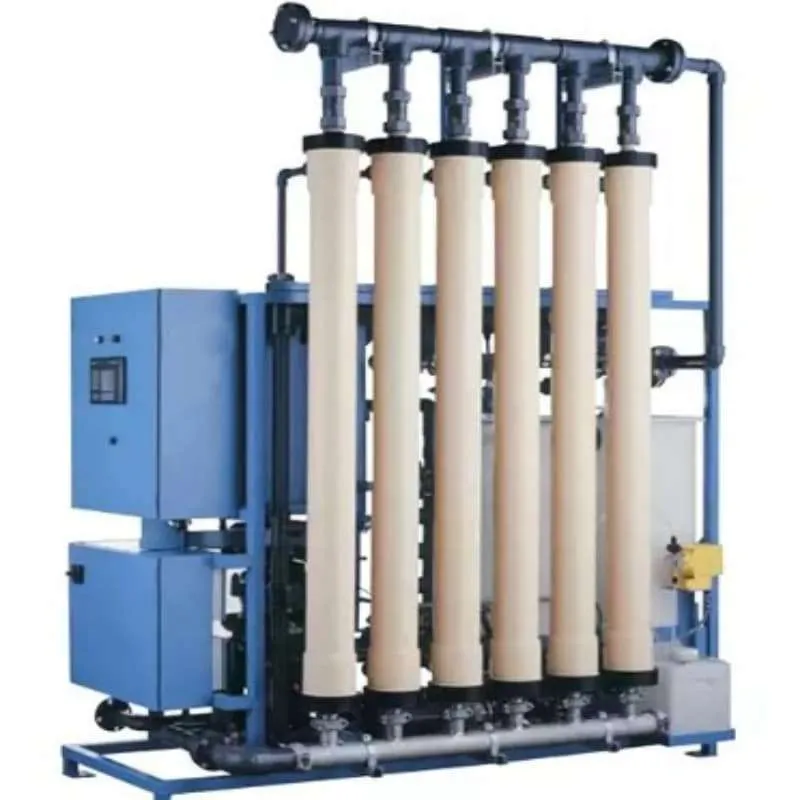
Clean raw water first. Do this before it enters power machines. External boiler feed water treatment removes bad solids. It cleans out salts and silica. This protects steam generation systems from scale. It stops rust and broken machines.
Clarification, Filtration, and Lime Softening
Dirty water enters your plant. Clear big particles out first. Use a media filtration system. Settling tanks catch heavy mud. Multi-media filters trap dirt.
Next, use lime softening. Cold or hot lime works well. This lowers minerals and silica. Lime cleans water using two steps:
Carbonate Hardness Reduction: Hydrated lime meets carbon dioxide. It reacts with calcium bicarbonates. It touches magnesium bicarbonates too. This converts soluble minerals into solids. Calcium carbonate forms quickly. Magnesium hydroxide drops out fast. Solids leave the water.
Silica Reduction: Magnesium hydroxide attracts silica. It sticks to the surface. Add extra magnesium oxide if needed. Do this for low-magnesium water.
Clean water moves forward now. It enters advanced membrane systems.
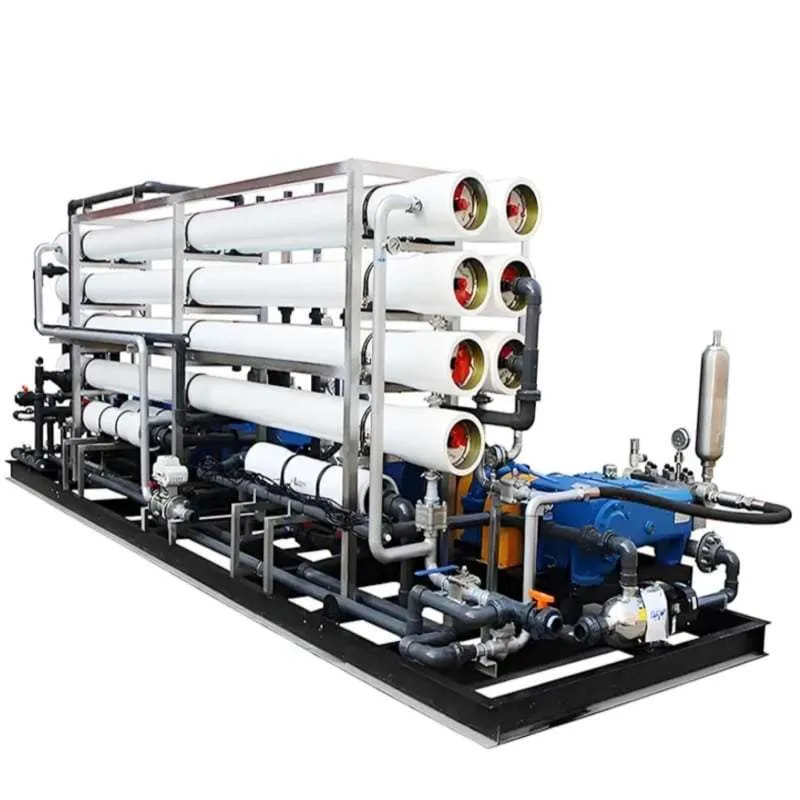
Reverse Osmosis and VSEP Membranes
First filters clean dirty water. Next, push water through membranes. High pressure moves the liquid. Reverse osmosis removes bad salts. It cleans out organics and silica. Standard membranes fail with solids. Heavy foulants ruin them fast.
Use Vibratory Shear Enhanced Processing instead. It handles oils and solids. This table compares both systems:
Feature / Parameter | Standard RO Membranes | Vibratory Shear Enhanced Processing (VSEP) |
|---|---|---|
Mechanism / Action | Uses standard crossflow. Layers build up fast. Surfaces foul quickly. | Uses fast vibration (50–60 Hz). Vibrating decks make shear. This removes the boundary layer. |
Fouling Resistance | Hard solids foul it easily. Oils and organics hurt it. | Stops solids and organics. Oils cannot stick. Surfactants slide away. |
Pretreatment Needs | Needs multi-stage filters. Requires chemical care. Needs heavy oversight. | Needs simple setup. Uses basic screening only. |
Flux & Membrane Life | Water flow drops down. Needs frequent cleaning. Membranes break fast. | Keeps water flow steady. Membranes last much longer. |
Target Feed Streams | Cleans easy water streams. Needs pre-treated water. | Cleans tough dirty water. Works on brines. Cleans PFAS and wastewater. |
Good membranes protect downstream units. They stop bad mineral overloads.
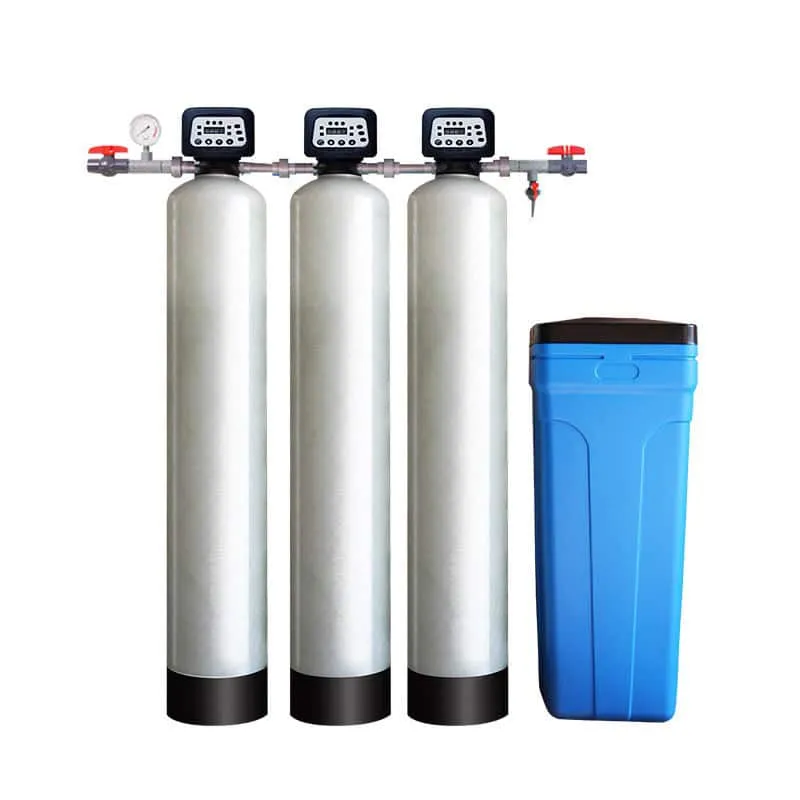
Ion Exchange Softening and Demineralization
Membranes clean out dissolved ions. High-pressure boilers need pure water. Resins do deep demineralisation. They trade bad ions for hydrogen. They swap ions for hydroxide. Cation resins trade sodium and calcium. They swap magnesium for hydrogen. Anion resins trade chloride and sulfate. They swap silica for hydroxide.
Mixed-bed demineralizers lower conductivity levels. They reach 0.1 microsiemens or lower. Synthetic resins mix in one tank. Water flows through the mixture. Cation resins swap ions for hydrogen. Anion resins swap ions for hydroxide. Resins sit very close together. Leaking ions get trapped fast. Nearby resins catch escaped ions. Water becomes very pure. This step sends clean water to tanks.
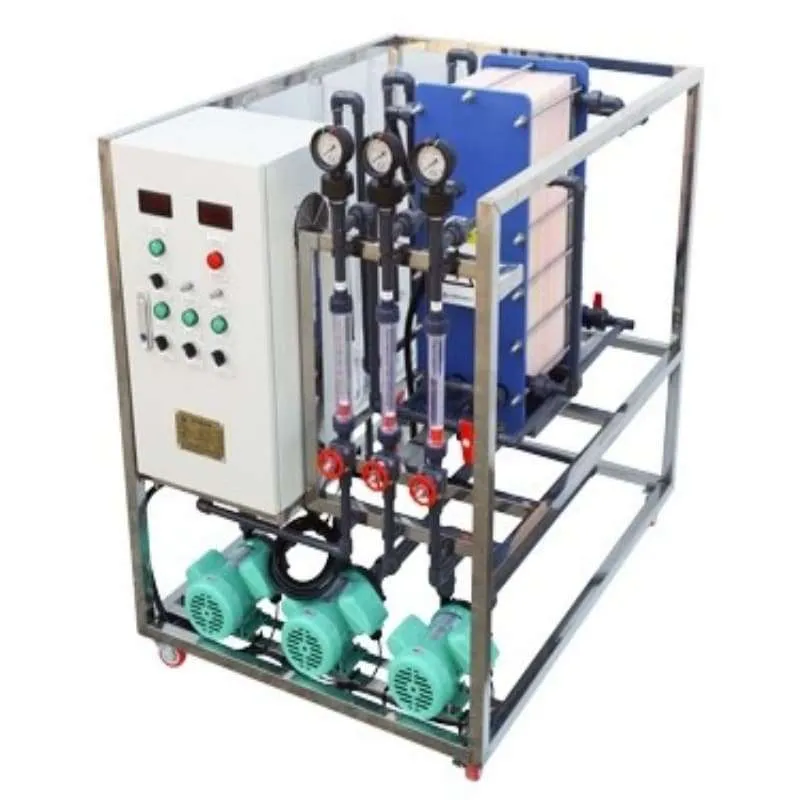
Electrodeionization and Polishers
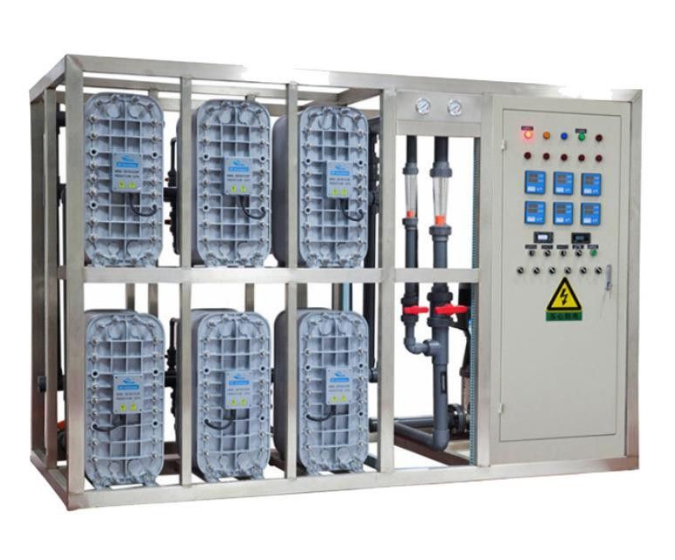
Plants use continuous electrodeionization today. It stops dangerous chemical handling. The process treats boiler feed water. It removes ions in three steps:
Targeted Ion Capture: Synthetic resins line the chamber. They trap residual bad ions.
Direct-Current Electromigration: Electric fields push charged particles. Selective membranes move them. Ions go to waste channels.
In-Situ Water Dissociation: Electric power splits water molecules. It creates hydrogen and hydroxyl. Resins stay fresh without chemicals.
Treat returning steam condensate too. This protects turbine parts. Polishers collect iron and copper. Deep beds keep water pure inside high-pressure loops:
Metric / Parameter | Target Conductivity Level |
|---|---|
Effluent Cation Conductivity | < 0.06 µS/cm |
Polished Exit Stream Conductivity | ~ 0.05 µS/cm |
Target Blended Conductivity | ~ 0.1 µS/cm |
Good polishing keeps water pure. Plant efficiency stays very high. Metal surfaces stay safe from damage.
Internal Boiler Feedwater Treatment Options

Apply internal treatments to protect hot water loops. First, run feedwater through mechanical deaerators. Heating removes bad trapped gas inside.
Mechanical Deaeration and Oxygen Scavengers
Tray-type deaerators work well during water prep:
Standard Operation: Drops dissolved oxygen under 7 ppb.
Without Oxygen Scavengers: Keeps oxygen levels under 10 ppb.
With Oxygen Scavengers: Drops oxygen down near 0 ppb.
Peak Efficiency: Pushes oxygen levels to 5 ppb.
Inject boiler feed water treatment chemicals for leftover oxygen. Pick hydrazine or carbohydrate mixes based on limits.
Parameter | Hydrazine | Carbohydrazide (Carbohydrate/Hydrazide-based) |
|---|---|---|
Reaction Speed | Reacts with oxygen at medium speed. Catalysts speed this up. | Takes time to strip oxygen away. Works at low heat. |
Thermal Stability | Turns to ammonia gas above 400 °F. | Breaks down into hydrazine above 350 °F. |
Neutralizing Amines and pH Buffering
Pump chemical agents into the water circuits. Amines move with steam to adjust pH levels.
Different amines guard parts of steam generation systems:
Cyclohexylamine: Travels far down pipes. Protects long condensate lines.
Morpholine: Stays near boilers. Protects early condensate drops.
Combined Amine Blends: Mixing both amines balances protection. Keeps whole pipe systems safe.
Proper pH control stops bad metal rust. It stops fast corrosion on inner pipes.
Treatment Method | Target pH Range | FAC Prevention Effect |
|---|---|---|
Oxygenated Treatment (OT) | 8.0 – 8.5 | Stops rust under special oxygen settings. |
All-Volatile Treatment [AVT(O)] | 9.2 – 9.6 | Gives basic protection against pipe wear. |
Low-Pressure (LP) Circuit Adjustments | Up to 9.8 | Gives extra safety against pipe wear. |
Peak Risk Level: A pH near 8.5 causes fast rust.
Mitigation Target: A pH between 9.2 and 9.6 cuts damage.
Phosphate-Polymer Programs for Sludge Control
Power plants need smart chemical plans. Choose phosphate additions or oxygen programs carefully.
Chemical Property / Parameter | Coordinated Phosphate Treatment | Oxygenated Treatment (OT) |
|---|---|---|
Primary Additives | Uses trisodium phosphate and sodium hydroxide. | Uses pure oxygen gas or liquid. |
pH Control Agents | Uses ammonia or special amines. | Uses ammonia or special amines. |
Dissolved Oxygen Strategy | Uses oxygen scavengers for safety. | Needs direct oxygen doses instead. |
Protection Mechanism | Buffers pH and catches calcium scale. | Builds strong protective layers on tubes. |
Purity & System Constraints | Works with standard boiler water. | Needs super pure water only. |
Polymers push heavy mineral dirt down. Synthetic mixes keep particles floating for clean removal.
Surface and Bottom Blowdown Control
Manage dissolved salts using smart blowdown plans. Surface blowdown cleans top liquid layers. Bottom blowdown removes dirty settled mud.
Heat recovery units catch extra hot energy:
Flash Vessel & Basic Equipment: Saves 40% of blowdown energy.
Flash Steam Energy: Saves 49% of steam heat.
Combined Heat Recovery (Flash Steam + Residual Condensate): Saves 82% of total waste heat.
Recycle hot flash steam to raise plant output. Good care keeps your machines working great.
Monitoring Plant Water Purity with SWAS

You must check fluid conditions inside your facility. SWAS systems give real-time stream data to your operators. These special panels measure key parameters. They track sodium, dissolved oxygen, pH, and conductivity.
Online Steam and Water Analysis Systems
High heat and big pressure destroy sensors. You must cool and depressurize each sample first. Special conditioning parts stabilize fluid samples. Temperature Control Units set samples to 77ºF (25ºC).
Component | Regulation Type | Function / Description |
|---|---|---|
Steam Sample Coolers | Temperature | Cools hot gas and liquid samples fast. |
Temperature Control Units | Temperature | Sets exact sample temperatures to 77ºF (25ºC). |
Thermal Shutoff Valves (Manual/Automatic) | Temperature | Stops hot samples near 120ºF (49ºC) to protect sensors. |
Sentry VREL Pressure Reducing Valve | Pressure | Cuts sample pressure above 34.5 barg (500 psig). |
Swan Back Pressure Regulator (BPR) | Pressure | Keeps flow and pressure steady for all sensors. |
Raw steam flows through primary coolers first. Back pressure regulators keep total fluid flow stable.
Real-Time pH, Conductivity, and Silica Tracking
Real-time analyzers protect plant equipment from sudden chemical damage. Continuous water checks stop bad chemical over-dosing. Fast alerts warn operators about membrane leaks. Quick notifications signal bad condenser leaks too.
Normal conductivity readings look low. Neutral salts mask hidden contaminants.
Cation conductivity removes this masking effect. It exposes bad chloride and sulfate fast.
Online silica units track gas moving in steam. Checking sodium shows bad leaks fast. Early care stops big machine failures. You keep high heat efficiency and save turbines.
Selecting Treatment Options for Power Plants
Low-Pressure Package Shell Boilers
Low pressure lets you use basic chemical plans. Simple softeners take out hard calcium ions. They clean out magnesium ions too. Next, add phosphates to shield boiler tubes. These chemicals stop hard scale layers inside. Then, pump in oxygen scavengers. They shield basic steam generation systems from pitting. Lastly, use surface blowdown regularly. This step manages total dissolved solids. Your total operating costs stay low. Your plant stays safe.
High-Pressure Utility Water-Tube Boilers
High-pressure boilers demand super clean water. This step stops bad deposit buildups. Boiler feed water needs better cleaning over 1,000 psig. First, run water through reverse osmosis filters. Next, use two-step ion exchange demineralisation. This deep cleaning strips silica and sodium away. It removes bad chlorides from fresh makeup water. Finally, add volatile neutralizing amines into loops. They protect returning condensate lines.
Pressure Rating | Primary Pretreatment Method | Conditioning Strategy | Target Conductivity |
|---|---|---|---|
< 600 psig | Ion Exchange Softening | Phosphate & Polymer | < 1,500 µS/cm |
600 – 1,000 psig | Two-Pass Reverse Osmosis | All-Volatile Treatment | < 100 µS/cm |
> 1,000 psig | RO with Demineralisation | All-Volatile Treatment | < 0.1 µS/cm |
This smart plan keeps steam clean. It keeps plant efficiency high.
Supercritical Once-Through Steam Generators
Supercritical generators push water straight through tubes. Heavy pressure turns liquid into steam fast. No steam drums separate the water inside. Floating solids cause big damage here. High heat leaves no room for minerals. These special units need very clean water. Bad water causes total tube failures fast. Always run continuous electrodeionization units first. Next, install deep-bed condensate polishers. This special boiler feed water treatment needs oxygenated chemistry. Operators add pure oxygen and ammonia. They build protective magnetite layers inside. This care protects turbine blades. Power plants keep running at high performance.
Combine top pretreatment, membrane filters, and ion exchange. Add SWAS checks too. This complete system stops bad rust. It stops heat scale. Clean feed water makes pure steam. Pure steam turns your turbine smoothly.
Follow strict ASME water rules. Follow EPRI chemistry limits too. These guidelines direct your daily water care. Meeting them stops bad tube breaks. This keeps your plant safe.
Match daily surface blowdown with chemical treatment. Chemicals stop hard mineral layers. Controlled blowdown cleans out extra dissolved solids. This smart step saves expensive heat energy. It preserves clean steam. It helps major equipment last longer.
FAQ
What is the primary purpose of boiler feedwater treatment?
Good water treatment clears out harmful minerals. It cleans bad gases out too. This work keeps scale away. Rust cannot form in pipes. Pipes pass heat very well. Machines last for a long time.
Why must you remove silica before generating steam?
Big heat turns silica into gas. Steam carries this gas into turbines. The gas cools down on blades. It forms hard glass layers. These layers ruin blade movement. Turbines shake very hard.
How does deep demineralisation protect high-pressure power systems?
Demineralisation swaps bad ions for clean water. Mixed resin tanks make pure liquid. Electricity flow drops very low. Clean water enters system loops. Scale cannot build up inside. Machines stay safe from breaks.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian