

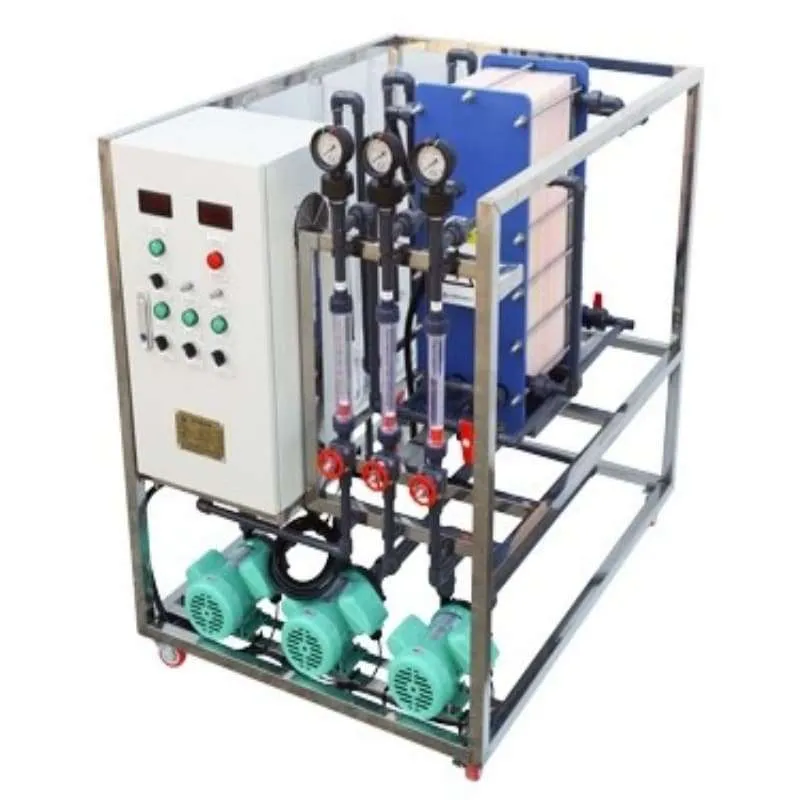
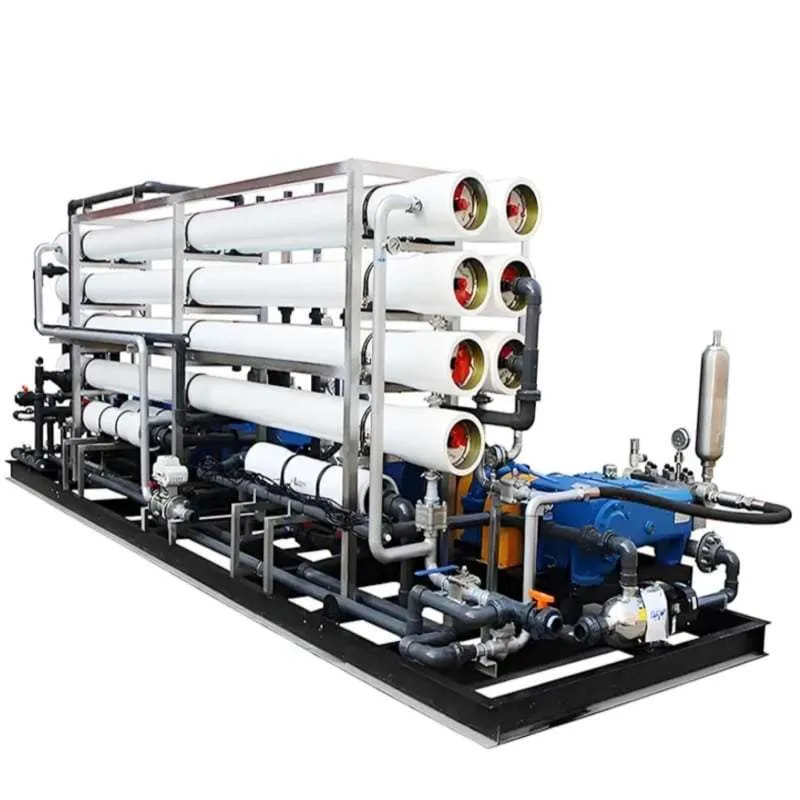
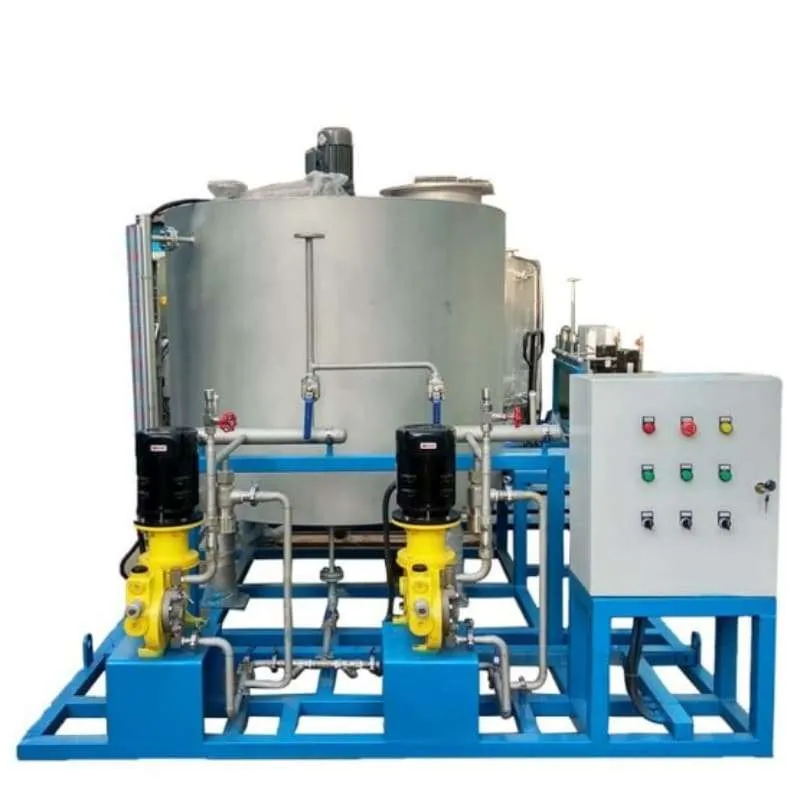
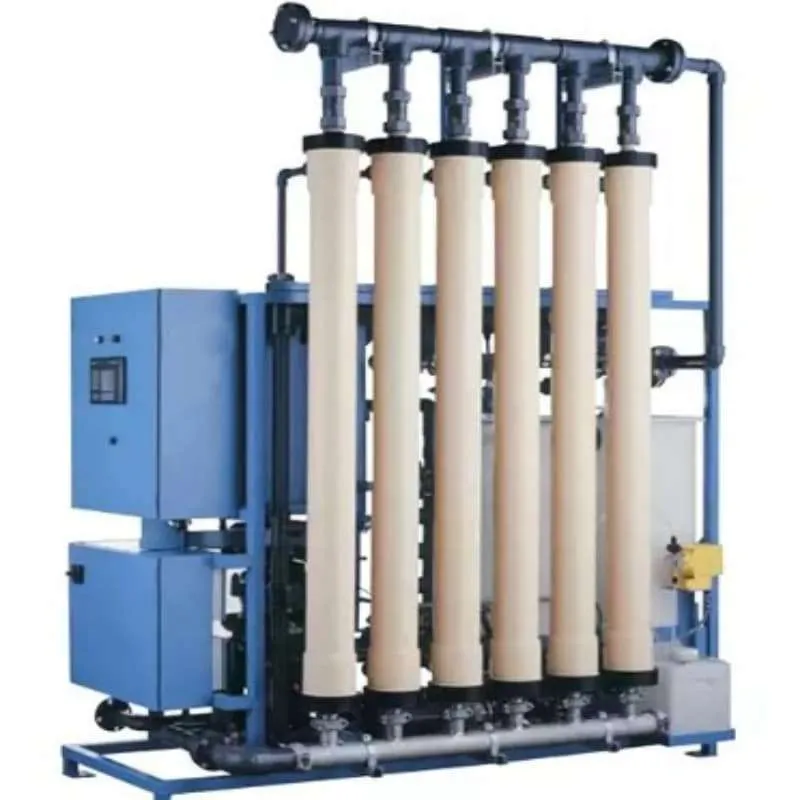
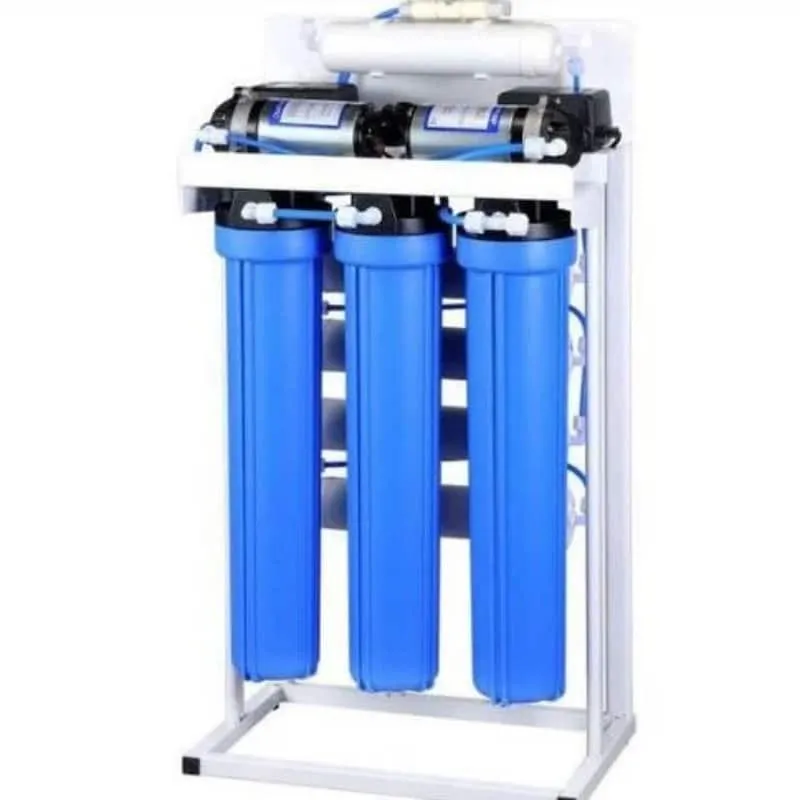



Industrial reverse osmosis plants need exact control at every step. Watching things by hand leads to mistakes, water that is not always the same, and high energy bills. Automation fixes these problems. A reverse osmosis plant runs all the time, so operators need tools they can trust. PLCs and SCADA are the main parts of this control. These technologies let workers watch and adjust reverse osmosis processes in real time. A modern ro plant relies on them. Automation in ro systems cuts human error and keeps output steady. Look at energy data from an automated ro system:
Metric | Value |
|---|---|
SEC before automation | 2.97 kWh/m³ |
SEC after automation | 2.80 kWh/m³ |
Energy reduction | 5.7% |
Better pressure control can lower energy use by 15–25%. Reverse osmosis water systems gain from this efficiency. Reverse osmosis quality stays steady. Reverse osmosis uptime gets better. Reverse osmosis costs go down. Reverse osmosis operations become safer. Reverse osmosis plants grow more easily. Reverse osmosis control improves. Reverse osmosis teams learn more. Reverse osmosis performance increases. Reverse osmosis systems keep changing.
Key Takeaways
Automation uses PLCs and SCADA to control pumps, valves, and sensors right away.
Automatic cleaning and flushing keep reverse osmosis membranes safe and help them last longer.
Automation saves energy by adjusting pressure and flow without people making mistakes.
SCADA shows operators live data on water quality and sends alarms so they can quickly fix problems.
IoT and AI tools help predict breakdowns and make plants smarter over time.
Core Automation Components in the RO Plant

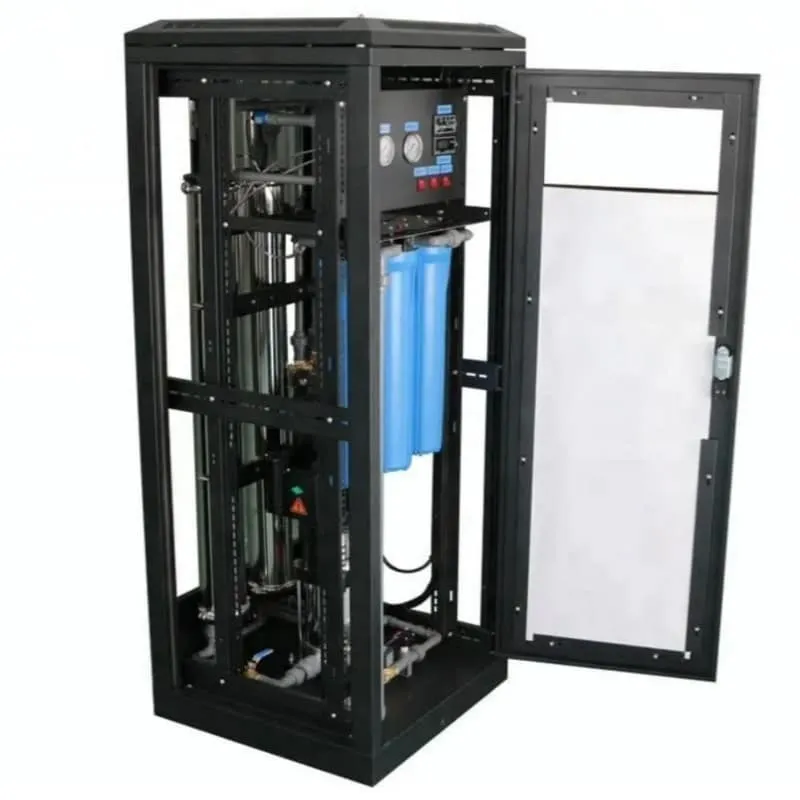
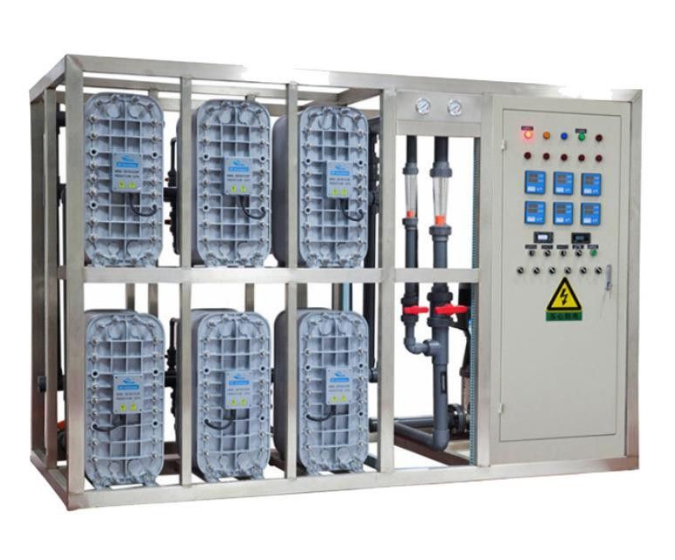
A modern industrial ro plant uses three connected layers of hardware and software. Programmable logic controllers are at the bottom. SCADA and HMI systems are at the top. Sensors and actuators connect them. Together they create an automated control system that runs the plant all day, every day.
PLC Role in Reverse Osmosis Process Control
The PLC is the main part of reverse osmosis process control. It reads signals from field devices many times each second. Then it decides what to do next. This is the heart of an automatic feedback control system.
Key PLC functions in ro plants include starting and stopping pumps, opening and closing valves, and adjusting dosing rates. The PLC also watches transmembrane pressure, flow, and conductivity. When a reading goes outside its setpoint, the PLC reacts right away. It may slow a high-pressure pump or start a flush cycle.
Think of a simple example. Feed water quality sensors see a rise in conductivity. The PLC responds by adjusting the concentrate valve. This keeps recovery steady without an operator touching a screen. That is sensor-based feedback at work.
A PLC also handles safety interlocks. It stops a pump if pressure gets too high. It locks a valve if tank level gets too low. These actions protect membranes and pumps from damage. The result is a plant that runs itself with little human help.
SCADA and HMI for Real-Time Monitoring
SCADA is software that shows, watches, and controls the whole plant. It connects to the PLC over a network. Then it shows live data on an HMI screen. Operators see the whole reverse osmosis train at once.
The HMI turns raw numbers into useful info. A color change means a problem. A trend line shows a slow drift. An alarm banner tells the operator what to fix first. This is real-time sensor feedback made visible.
The table below shows what SCADA tracks and why each parameter matters.
SCADA Real-Time Monitoring Parameter | Operational Benefit |
|---|---|
Feed Pressure | Early detection of abnormal conditions before production is affected |
Permeate Pressure | Reduced downtime through rapid operator response |
Differential Pressure (ΔP) | Improved water quality via continuous process oversight |
Flow Rates | Optimized chemical consumption |
Conductivity / TDS | Reduced energy costs |
pH (where applicable) | Scheduled preventive maintenance |
Tank Levels | Extended membrane life |
Pump Status | Increased production reliability |
Valve Position | Remote monitoring via computer, tablet, or smartphone |
Energy Consumption (kWh) | Instant notifications for pressure drops, TDS spikes, pump trips, and CIP cycles |
Alarm History | Faster maintenance team response and improved operational efficiency |
Sensors and actuators connect everything. Flow meters, pressure transmitters, and conductivity probes send data into the PLC. Actuators then follow the PLC’s commands. This loop makes sensor-controlled automation possible.
Automation in ro systems also allows remote access. An engineer can check the plant from a phone or tablet. That reduces travel time and speeds up repairs. The mix of PLC logic and SCADA visibility gives operators full control of the reverse osmosis process.
PLC–SCADA Integration Architecture

A modern reverse osmosis plant links its control layers through an organized network. The reverse osmosis process needs close watching and quick action. The PLC sits at the equipment level. The SCADA system sits above it. Together they make a full automation framework. This framework guides every stage of the reverse osmosis process.
Network Topology and Communication Protocols
The network layout follows a normal industrial setup. Field devices connect to the PLC through I/O modules. These devices include pressure transmitters, flow meters, conductivity probes, and level sensors. The PLC reads their signals and runs control logic. It then sends commands to actuators like pumps, valves, and dosing units. The plc–scada integration architecture depends on steady communication between these control layers.
The SCADA system links to the PLC over an industrial network. This network uses protocols built for dependable data sharing. Modbus is a common pick for serial communication between devices. Profibus handles faster data transfer. Ethernet/IP allows connection with modern control systems and IT networks. Best practices also suggest MQTT and OPC-UA for safe data transmission. This communication supports dependable reverse osmosis operations. Operators see pressure readings, flow trends, and alarm conditions on one screen. The network layout supports both local HMI access and remote monitoring.
This architecture gives operators real-time visibility into the reverse osmosis process. They can check the plant from a phone or tablet. The SCADA system logs every data point for audits and compliance.
Sensor and Actuator Integration Points
Sensors and actuators form the physical link between the reverse osmosis process and the control system. The table below shows the typical integration points in an ro plant.
Integration Point | Devices / Signals | Role in PLC–SCADA Architecture |
|---|---|---|
Field sensor inputs to PLC | TDS, pressure, flow, level, pH, temperature | Analog/digital signals conditioned and read by PLC for logic execution |
Actuator outputs from PLC | Pumps, valves, dosing pumps | PLC drives these based on sensor thresholds and control logic |
PLC logic layer | Sensor processing, auto start/stop, flushing, dosing, alarms | Executes control decisions based on programmed thresholds |
SCADA/HMI layer | Real-time display, mimic diagrams, logging, alarms | Visualizes sensor data and actuator states, logs trends, issues alerts |
Communication protocols | Modbus, Profibus, Ethernet/IP | Transport data between PLC, SCADA, and field devices |
Example closed-loop workflow | TDS setpoint 100 ppm → PLC monitors conductivity → auto flush → SCADA logs and alarms | Demonstrates sensor-to-actuator integration through PLC and SCADA |
These integration points support every reverse osmosis operation. The PLC works as the control brain. It gets sensor inputs such as TDS, pH, flow, pressure, temperature, and level. It runs logic to command actuators including pumps, valves, and dosing pumps. The SCADA system connects to the PLC to show these sensor readings and actuator states. It keeps process mimic diagrams, logs data for audits, and creates alarm or remote fault notifications. This complete plc & scada integration allows smooth data flow.
Best practices for sensor selection in reverse osmosis processes include using differential pressure sensors to spot filter clogging and membrane fouling. Temperature sensors keep the right conditions for water purification. These practices directly boost reverse osmosis performance and reliability. Pressure regulation helps keep stable reverse osmosis conditions. Pressure and temperature monitoring stops pump failures, pipeline ruptures, and chemical dosing imbalances. This ensures safe operation and longer equipment lifespan.
Automated dosing systems use flow-based feedback loops. They adjust chemical injection rates based on water quality measurements. VFDs and PLC-based pump controllers improve performance. They stop cavitation, cut wear, and boost energy efficiency. Advanced control algorithms automate backwashing cycles and membrane cleaning. One key parameter the system tracks is transmembrane pressure. Rising transmembrane pressure means fouling and starts a cleaning sequence.
The mix of smart sensors and SCADA systems gives precise control over reverse osmosis treatment processes. Secure protocols such as Modbus, MQTT, and OPC-UA protect operational data. Automation solutions follow EPA, NPDES, ISO 14001, and local regulations. The whole reverse osmosis system runs with very little human involvement.
Key Features of Automation in RO Systems
Modern ro plant operations rely on automated sequences that protect membranes and keep output steady. These key automation features in modern ro plants cut manual work and make equipment last longer.
Automated Membrane Cleaning and Flushing
An automated control system starts Clean-in-Place (CIP) cycles based on transmembrane pressure trends and runtime hours. A mobile CIP skid heats and holds cleaning chemicals. Operators set temperature, concentration, and flow for each cleaning cycle. Skids with multiple reservoirs prepare more than one chemical, which adds flexibility. The system can also capture cleaning chemicals for reuse and recycling.
Benefit | Supporting Detail |
|---|---|
Extends membrane life | The advanced membrane protection system automatically flushes the membrane when switched on, cutting pollution and extending membrane life. |
Reduces pollution/fouling | Automatic flushing lowers contamination buildup on the membrane surface. |
Saves time and money | Automated cleaning removes manual disassembly and tiring cleaning, cutting both time and cost. |
Enables automatic control | The system is simple to set up with automatic control, making it labor-saving and easy to run. |
Compact and low-cost | Small footprint, low investment costs, and low energy consumption. |
High pollution resistance | The separating device resists pollution well and is easy to clean. |
The case study from Caloris Engineering describes an industrial RO system that has an automatic permeate flush operation at the end of each production cycle, showing automated membrane flushing. The cleaning is manual (CIP), but the flush is automated.
Real-Time Quality Monitoring and Alarms
Real-time monitoring tracks water quality, flow rates, and pressure across every reverse osmosis stage. Continuous permeate flow rate monitoring spots small changes before they turn into failures. Alarm management warns operators when readings drift outside setpoints. This real-time oversight keeps reverse osmosis quality stable.
Advanced techniques handle disturbances and uncertainties. Model-predictive control adjusts real-time adjustable operating parameters to deal with changing feed conditions. Model predictive control also coordinates chemical dosing control across multiple injection points. Machine learning-based membrane fouling prediction and real-time fouling detection algorithms spot membrane fouling patterns early. Dynamic reverse osmosis membrane fouling control and adaptive optimal control further improve reverse osmosis performance. These methods lower membrane fouling risk and stretch out cleaning intervals.
Benefits of PLC & SCADA Integration
Efficiency, Energy Savings, and Uptime
Automation makes the whole ro plant run more smoothly. The control system keeps pumps and valves at their best settings. This reduces wasted energy and keeps output steady. A plant that adjusts pressure and flow on its own uses less power than one run by hand. The system also watches every stage at the same time, so nothing gets missed.
Uptime gets better through several connected ways. Constant monitoring and real-time adjustments let the system track feed water quality, pressure differences, and permeate flow rates all day and night. Predictive maintenance uses machine learning to study past and current data. It finds patterns that show equipment failures are coming. Operators then plan repairs before a breakdown stops production. Automated cleaning and flushing cycles run at the best times with exact chemical dosing. This approach makes cleaning work better and lowers human error. Quick fault detection catches system problems early and stops them from spreading. Remote monitoring and alarms give secure access from away, so experts can handle emergencies without driving to the site. Full data logging captures detailed data for trend analysis and supports energy efficiency improvements.
Reliability and Reduced Human Error
Doing things by hand leads to mistakes. An operator may miss a pressure spike at 3 a.m. or forget a valve setting. PLC and SCADA integration takes away those risks. The PLC follows the same logic every time. It opens valves, starts pumps, and adjusts dosing with exact repeatability. This consistency protects membranes and keeps water purity within industrial standards.
The benefits of automation in ro systems also cover safety. Interlocks stop pumps before pressure damages equipment. Alarm management warns operators when readings drift outside setpoints. Every reverse osmosis stage stays watched. The result is higher uptime, steadier water quality, and fewer costly shutdowns. Reverse osmosis teams spend less time putting out fires and more time improving the process. Reverse osmosis reliability becomes a design result, not a hope.
Industry Applications and Emerging Trends
Applications in Desalination, Pharma, and Food
Automation helps many industries that use reverse osmosis. Desalination plants use it to control high-pressure pumps and energy recovery devices. Pharmaceutical sites need very pure water, so they use reverse osmosis with automatic cleaning cycles. Food and beverage makers use reverse osmosis for water used in ingredients and for making concentrates. Power generation plants use reverse osmosis for water for boilers. Each industry gets steady quality and lower costs from the same control system.
Industry | Automation Focus | Key Benefit |
|---|---|---|
Desalination | High-pressure pump control, energy recovery | Lower energy use per cubic meter |
Pharmaceutical | Purity monitoring, sanitization cycles | Regulatory compliance |
Food and Beverage | Ingredient water, concentrate processing | Consistent product taste |
Power Generation | Boiler feedwater treatment | Reduced scaling risk |
These examples show how reverse osmosis fits different needs. The control logic changes, but the main automation ideas stay the same.
IoT, AI, and Remote Diagnostics
The Industrial Internet of Things links reverse osmosis plants to cloud services. Smart sensors measure pressure differences, flow rates, conductivity, temperature, and pH levels. An IIoT data collector gathers this data and sends it over wireless networks. The system works with older equipment through serial connections, so older plants can connect without a full rebuild. Firmware manages safe reconnection after a broker disconnects or signal loss.
AI-driven analytics bring predictive maintenance to reverse osmosis. Machine learning looks at past and current data to predict membrane fouling and plan cleaning before performance drops. These tools also support adaptive optimal control, which changes operating settings as feed conditions change.
Challenges still exist. Older PLCs may be hard to connect. Sensor calibration needs care. Cybersecurity needs planning during design. Step-by-step rollouts and close teamwork between OT, IT, and operations teams help solve these problems.
PLC and SCADA integration gives industrial reverse osmosis plants exact control. Automated cleaning, flushing, and real-time alarms protect membranes. Measurable outcomes include lower energy consumption, stable permeate quality, reduced membrane fouling, less maintenance, smooth motor starting, better remote monitoring, and extended equipment lifespan. Automation directly solves efficiency, reliability, and water quality challenges in reverse osmosis. It cuts human error and keeps output steady. Reverse osmosis teams gain safer operations and higher uptime. Reverse osmosis quality stays within industrial standards. Reverse osmosis costs drop. Smart technologies will shape the future of reverse osmosis. Remote diagnostics optimize performance. Predictive failure detection reduces downtime. AI and IoT sensors improve reverse osmosis efficiency. Reverse osmosis plants will grow smarter.
FAQ
What does a PLC do in a reverse osmosis plant?
A PLC reads sensor signals many times each second. It controls pumps, valves, and dosing rates. The PLC also watches pressure, flow, and conductivity. When a reading drifts, the PLC reacts right away. This keeps the reverse osmosis process steady without constant human input.
How does SCADA help operators run a reverse osmosis system?
SCADA connects to the PLC and shows live data on an HMI screen. Operators see pressure, flow, and water quality across every stage. Alarm banners tell them what to fix first. This real-time visibility lets teams respond fast and keep the reverse osmosis plant running smoothly.
Why does automation reduce energy use in reverse osmosis plants?
Automation keeps pumps and valves at their best settings. Better pressure control lowers energy use by 15–25%. One plant cut specific energy consumption from 2.97 to 2.80 kWh/m³ after automation. The reverse osmosis system uses less power and keeps output steady.
How does automated cleaning protect reverse osmosis membranes?
The control system starts Clean-in-Place cycles based on transmembrane pressure trends and runtime hours. Automatic flushing lowers contamination buildup on the membrane surface. This extends membrane life, saves time, and cuts cleaning costs. The reverse osmosis plant stays productive with less manual work.
Can older reverse osmosis plants connect to IoT and AI tools?
Yes. An IIoT data collector works with older equipment through serial connections. Plants can connect without a full rebuild. AI-driven analytics then predict membrane fouling and plan cleaning before performance drops. This helps the reverse osmosis system avoid unexpected downtime.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian