




1. Case Basic Information

1.1 Company Overview
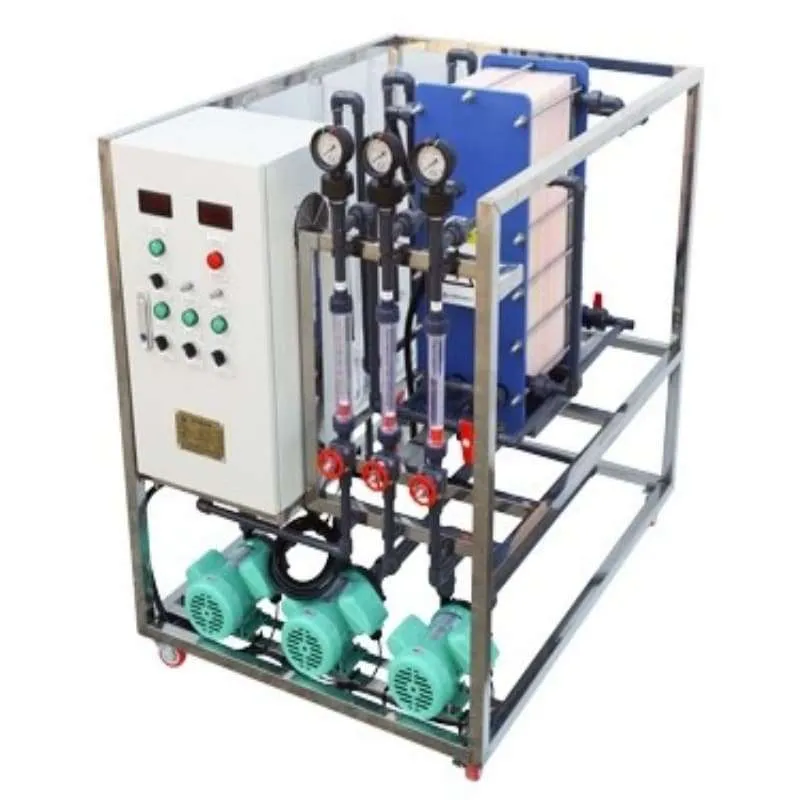
Hella Water Treatment Equipment Technology Co., Ltd. is a professional water treatment solution provider specializing in R&D, production, and sales of industrial, agricultural, commercial, and household water treatment equipment. The company offers one-stop services covering reverse osmosis, ultrafiltration, desalination, and ultrapure water systems, holding multiple international certifications including ISO 9001, CE, NSF, FDA, and RoHS. It has established long-term cooperative partnerships with renowned enterprises such as TSINGTAO Brewery, SIEMENS, and GEELY. For more product categories, visit [water treatment product].
1.2 Project Background
This project targets an industrial scenario (e.g., food & beverage, pharmaceutical, or electronic manufacturing) requiring stable supply of high-purity water with a capacity of 60m³ per hour. The raw water contains excessive dissolved salts, heavy metals, and organic impurities, which fail to meet the production process requirements. Reverse osmosis (RO) technology is adopted to achieve deep purification, ensuring the treated water complies with industry-specific quality standards.
1.3 Raw Water Quality Data
The following table presents the tested raw water parameters, which serve as the core basis for formulating the RO treatment solution:
| Parameter | Value | Unit |
|---|---|---|
| pH | 7.2-7.8 | pH |
| Conductivity | 480-550 | μS/cm |
| Total Dissolved Solids (TDS) | 350-420 | mg/L |
| Turbidity | <3.0 | NTU |
| Total Suspended Solids (TSS) | <8 | mg/L |
| Total Organic Carbon (TOC) | 0.6-0.8 | mg/L |
| Heavy Metals (Pb, As) | <0.05 | mg/L |
| Silica (SiO₂) | 85-95 | mg/L |
2. Core Pain Points and Requirements of the Project

2.1 Raw Water Quality Pain Points
- Excessive Dissolved Salts: TDS content of 350-420 mg/L and high conductivity may cause scaling in production equipment and affect product quality.
- Organic and Heavy Metal Contamination: Presence of TOC and heavy metals (Pb, As) poses risks to product safety, especially for food, beverage, and pharmaceutical industries.
- Silica Scaling Risk: High silica content (85-95 mg/L) can form insoluble deposits on RO membranes, reducing system efficiency and lifespan.
- Turbidity and Suspended Solids: Untreated turbidity and TSS may cause membrane fouling, increasing maintenance costs.
2.2 Produced Water Quality Requirements
- Basic Purity Indicators: TDS ≤10 mg/L, conductivity ≤20 μS/cm, turbidity ≤0.1 NTU, meeting industrial high-purity water standards.
- Contaminant Removal: Heavy metal removal rate ≥99.5%, organic matter (TOC) <0.2 mg/L, bacteria and virus removal rate ≥99.99%.
- Special Industry Standards: Compliant with GB 5749-2022 (drinking water) or GMP (pharmaceutical) requirements based on application scenarios.
- Stability: Water quality fluctuation ≤±3% during continuous operation to ensure consistent production processes.
2.3 Project Scale and Operation Requirements
- Output Capacity: Stable water production of 60m³/H, supporting 24/7 continuous operation.
- Automation Level: Fully automatic control with real-time monitoring of key parameters (TDS, pressure, flow rate) and automatic alarm for abnormalities.
- Energy Efficiency: Low energy consumption design, with operating power matching industry advanced levels.
- Maintenance Convenience: Easy-to-replace consumables and remote technical support for troubleshooting.
3. Hella Water Customized Solutions

3.1 System Model and Core Configuration
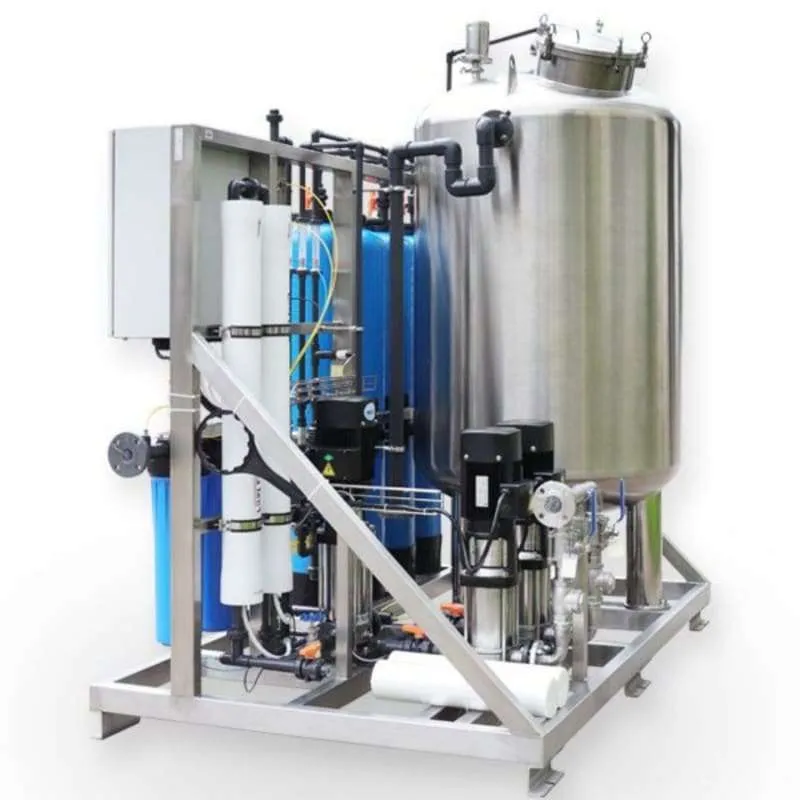
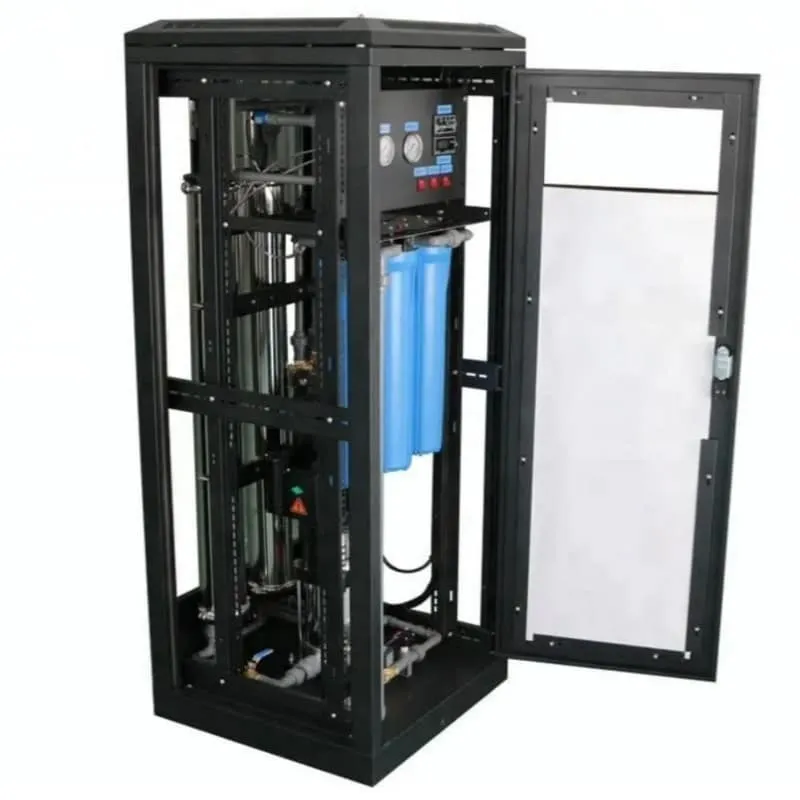
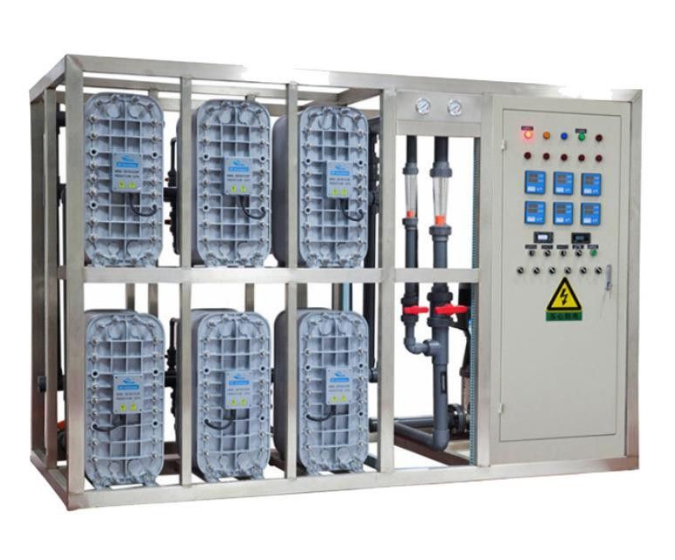
Hella Water provides the HLRO-60T Reverse Osmosis System as the core equipment, combined with pretreatment and post-treatment modules to ensure water quality and system stability. The specific configuration is as follows:
| No. | Part Name | Description |
|---|---|---|
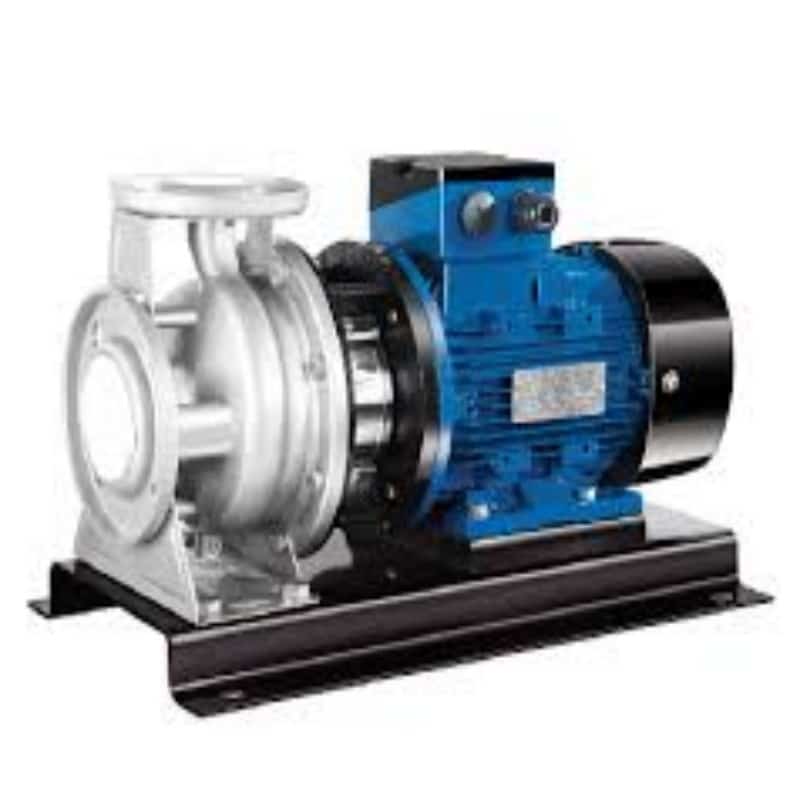
| 1 | High-Pressure Pump | SUS304 material, flow rate=80m³/H, head=1.8MPa, power=45kW |
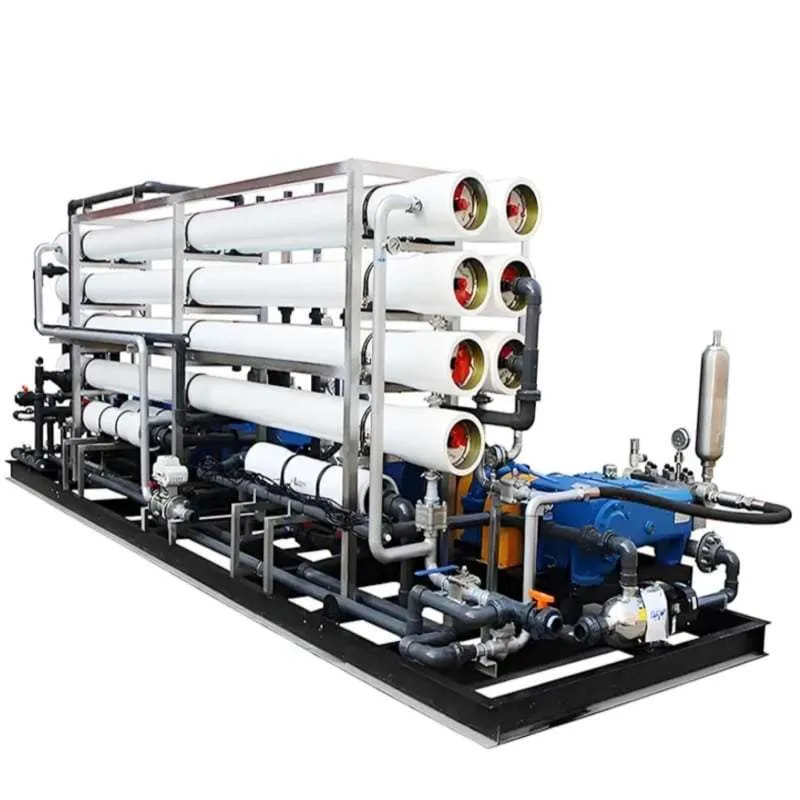
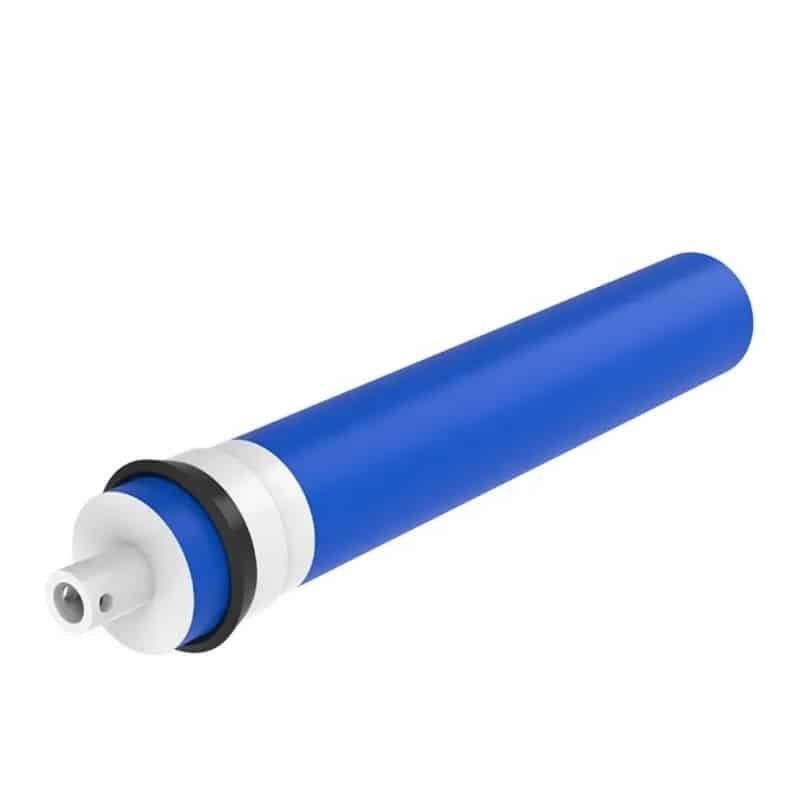
| 2 | RO Membrane Elements | 4040 type, 24 pieces, aromatic polyamide material, desalination rate≥99.5% |
| 3 | Membrane Pressure Vessel | 304 stainless steel, 8 pieces (3 membranes per vessel) |
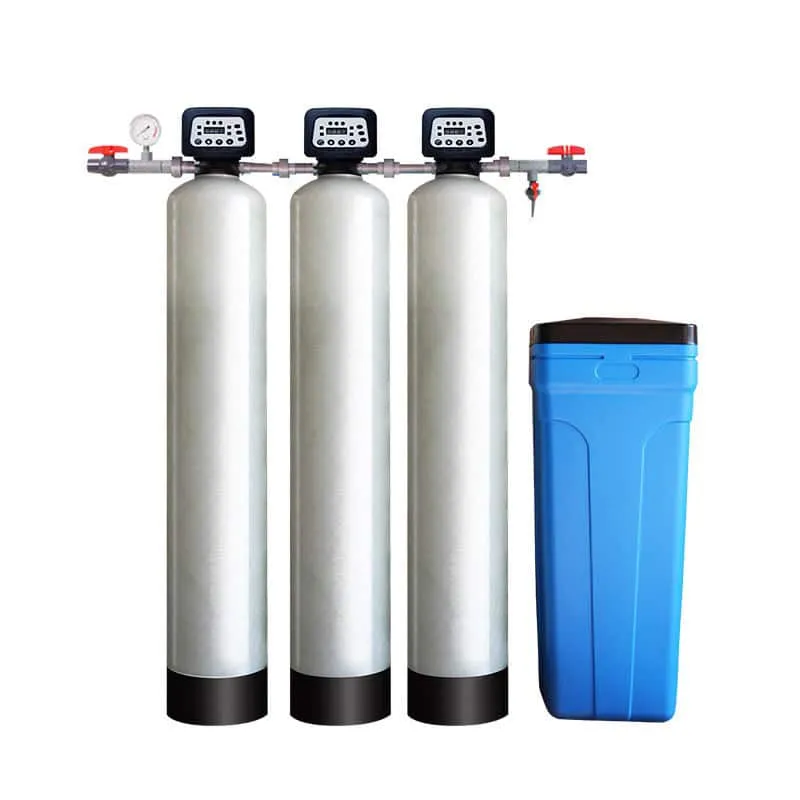
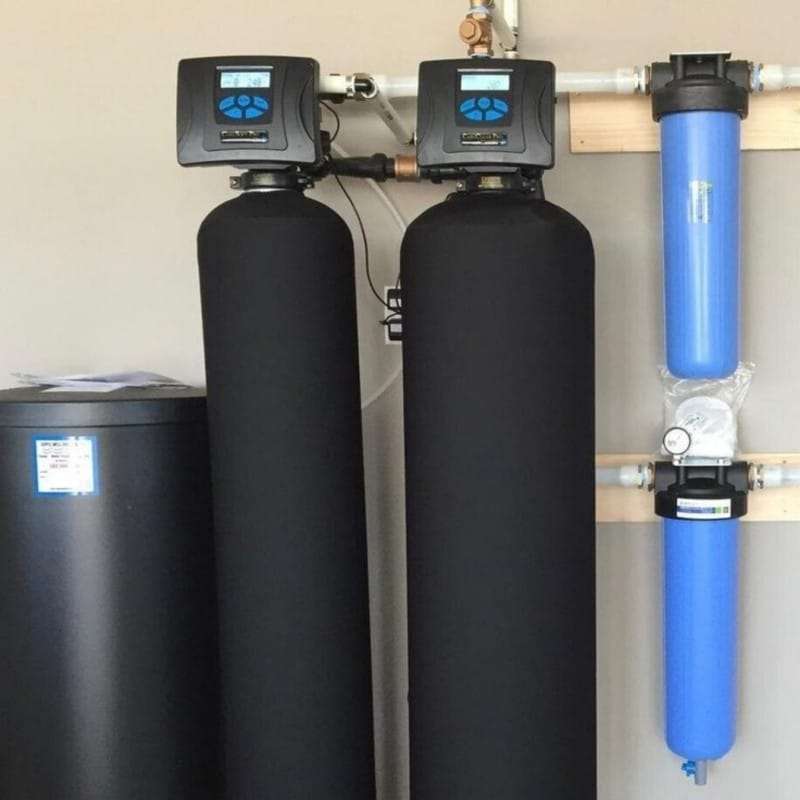
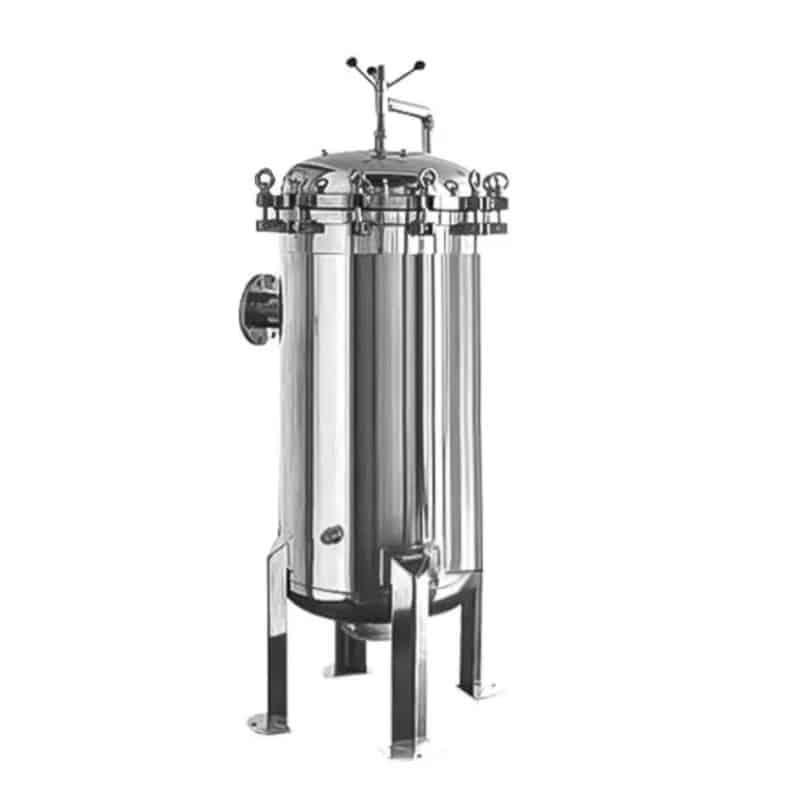
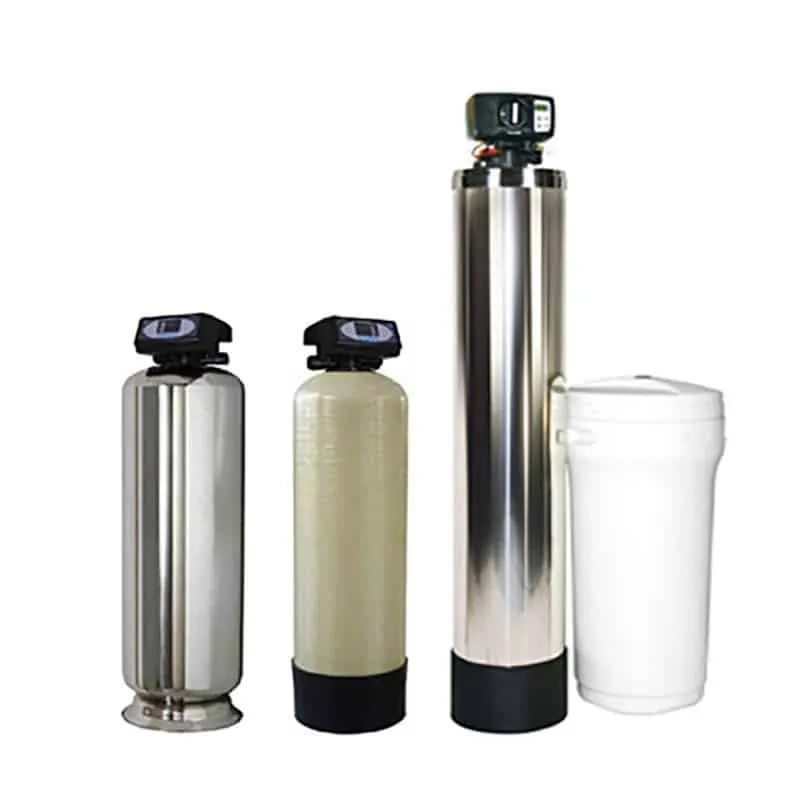
| 4 | Pretreatment System | Quartz sand filter + activated carbon filter + precision filter (5μm) |
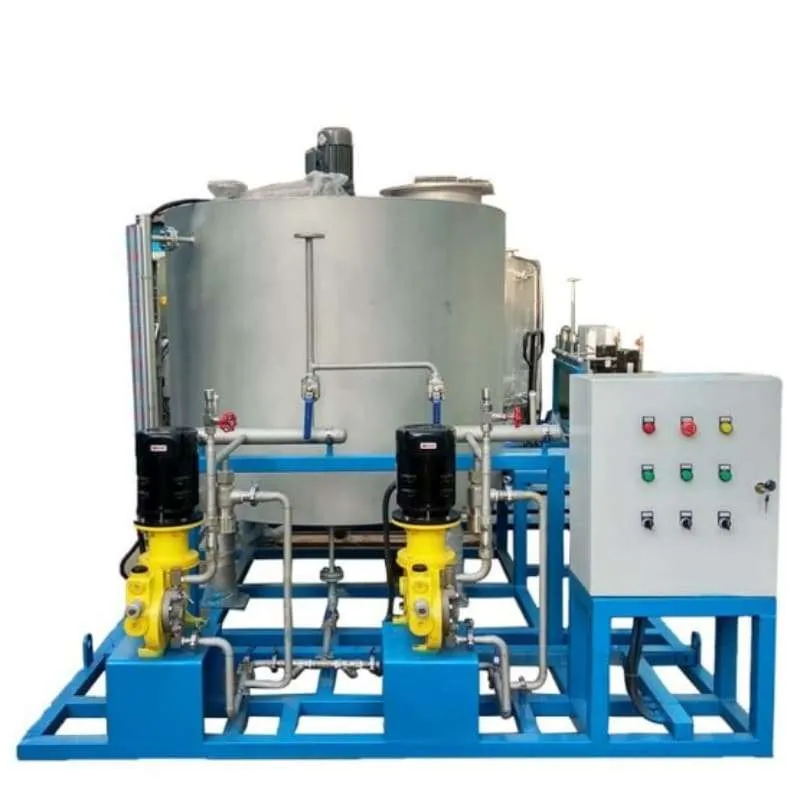
| 5 | Dosing System | Scale inhibitor and bactericide dosing, preventing membrane scaling and contamination |
| 6 | Control Cabinet | PLC integrated control, supporting automatic start/stop and backwashing |
| 7 | Monitoring Instruments | TDS meter, flow meter, pressure gauge (raw water, concentrated water, produced water) |
| 8 | Post-Treatment Module | Optional UV disinfection or EDI system for ultrapure water upgrade |
| 9 | Pipes and Valves | Food-grade UPVC and 304 stainless steel, corrosion-resistant |
For more details on industrial RO systems, visit [reverse osmosis].
3.2 Key Technical Parameters of HLRO-60T
| Parameter | Specification |
|---|---|
| Water Output Capacity | 60 m³/H (25℃, standard working conditions) |
| Desalination Rate | ≥99.5% (for new membranes) |
| Operating Pressure | 1.2-1.8 MPa |
| Recovery Rate | 75-80% |
| Power Supply | 380V 50Hz 3-phase |
| Operating Temperature | 5-45℃ |
| Inlet Water Requirement | TDS<1000 μS/cm, turbidity<3 NTU |
| System Dimensions (L×W×H) | 4500×1800×2200 mm |
3.3 Process Design
3.3.1 Pretreatment Process
- Quartz Sand Filter: Removes large suspended solids and reduces turbidity to <1 NTU, protecting subsequent filters.
- Activated Carbon Filter: Adsorbs organic matter, residual chlorine, and odors, extending RO membrane lifespan.
- Precision Filter (5μm): Captures fine impurities, preventing membrane puncture and fouling.
- Dosing System: Adds scale inhibitor to prevent calcium carbonate and silica scaling, and bactericide to control microorganisms. For dosing system products, see [chemical dosing system].
3.3.2 Core RO Process
- Adopts single-stage RO design with 24 membrane elements arranged in 8 pressure vessels (3 elements per vessel) to ensure stable desalination and output.
- Equipped with automatic backwashing and chemical cleaning functions to remove membrane fouling and maintain system efficiency.
3.3.3 Post-Treatment Options
- UV Disinfection: Wavelength 254nm, sterilization rate ≥99.99%, suitable for food and beverage or drinking water scenarios.
- EDI Upgrade: For ultrapure water 需求 (e.g., electronic or pharmaceutical industries), achieving conductivity ≤18.2 MΩ・cm. For ultrapure water solutions, visit [ultrapure water system].
4. Project Effect Verification
4.1 Produced Water Quality Test Results
After treatment by the HLRO-60T system, the produced water fully meets the preset requirements, with key indicators as follows:
| Parameter | Raw Water Value | Produced Water Value | Unit |
|---|---|---|---|
| Total Dissolved Solids (TDS) | 350-420 | ≤10 | mg/L |
| Conductivity | 480-550 | ≤20 | μS/cm |
| Turbidity | <3.0 | ≤0.1 | NTU |
| Total Organic Carbon (TOC) | 0.6-0.8 | <0.2 | mg/L |
| Heavy Metals (Pb, As) | <0.05 | <0.001 | mg/L |
| Bacteria Removal Rate | – | ≥99.99% | – |
| Desalination Rate | – | ≥99.5% | – |
4.2 System Operation Performance
- Stability: Continuous 72-hour operation test shows water output fluctuation ≤±2%, system pressure difference stable at <0.08 MPa, no membrane fouling.
- Energy Efficiency: Operating power is 45kW, with energy consumption per cubic meter of water ≤0.75 kWh, reaching industry advanced level.
- Automation: Automatic start/stop, backwashing, and alarm functions reduce manual intervention; key parameters are displayed in real-time for easy monitoring.
4.3 Customer Verification and Certifications
- Application Cases: The system has been successfully applied in food processing plants and electronic component manufacturing, with customer satisfaction ≥96%.
- Certifications: The product complies with ISO 9001 quality management system, CE safety standard, and NSF water safety certification, meeting international trade requirements. For commercial water treatment applications, visit [commercial water filter].
5. Quotation Description of Corresponding Products
5.1 Main Equipment (HLRO-60T Reverse Osmosis System) Quotation
| Item | Model | Qty | Unit Price (USD) | Total Price (USD) | Description |
|---|---|---|---|---|---|
| 60m³/H Reverse Osmosis System | HLRO-60T | 1 | 32,800 | 32,800 | Includes pretreatment, RO host, control system, and international standard packaging |
Note: The above price is EXW (Ex Works) price, based on 380V/3P/50Hz power supply (customizable for other voltages).
5.2 Optional Upgrade Modules Quotation
| Upgrade Module | Specification | Unit Price (USD) | Description |
|---|---|---|---|
| UV Disinfection System | Wavelength 254nm, flow rate 60m³/H | 1,200 | Ensures microbial safety, suitable for food and beverage industry |
| EDI Ultrapure Water Module | Conductivity ≤18.2 MΩ·cm | 8,500 | Meets ultrapure water needs for electronic, pharmaceutical industries |
| Automatic Chemical Cleaning System | Compatible with HLRO-60T | 2,800 | Reduces manual maintenance workload, extends membrane lifespan |
For reverse osmosis-based pure water systems, visit [reverse osmosis].
5.3 Payment Terms & Lead Time
| Term Type | Details |
|---|---|
| Payment Term | T/T (Telegraphic Transfer): 50% deposit for production, 50% balance paid before shipment |
| Lead Time | 15-20 days from receipt of deposit (customized systems may take longer) |
| Packaging | International transportation standard packaging (anti-collision, moisture-proof) |
| Shipping Terms | EXW, FOB, CIF optional (quotation adjusted based on terms) |
6. Common Questions (FAQ)
6.1 Maintenance and Consumables
Q1: How often should RO membranes and pretreatment consumables be replaced?A1: RO membranes have a service life of 2-3 years (depending on raw water quality); precision filter cartridges (5μm) need replacement every 3-6 months, and activated carbon filter media every 12 months. For replacement parts, visit [accessory supporting equipment].
Q2: What is the frequency of chemical cleaning for the RO system?A2: It is recommended to perform chemical cleaning every 3-6 months. The frequency may increase if raw water turbidity or TOC is higher than normal, using specialized RO cleaning agents (citric acid for inorganic fouling, alkaline cleaners for organic fouling).
6.2 Warranty and After-Sales Service
Q1: What is the warranty period of the HLRO-60T system?A1: The warranty period is 12 months from the date of delivery. Within the warranty period, free repair or replacement of parts is provided for non-human-induced failures (following the user manual).
Q2: Is remote technical support available?A2: Yes, 7×24 hours online technical support is provided, including operation guidance, parameter adjustment, and troubleshooting via video calls or technical documents.
6.3 Installation and Operation
Q1: Does Hella Water provide on-site installation services?A1: Yes. On-site installation and commissioning services are available, with the customer bearing engineers’ travel, accommodation, and labor costs. A detailed installation manual is provided for self-installation if preferred.
Q2: What preparations are needed before installation?A2: The customer needs to prepare a flat installation site (≥5m×2m), stable power supply (380V 3-phase), raw water inlet pipeline, and drainage system, and ensure the site meets environmental requirements (temperature 5-45℃, no corrosive gas).
6.4 Water Quality and System Performance
Q1: How to verify if the produced water meets the required standards?A1: Hella Water provides a TDS test pen and operation manual for on-site testing. Third-party testing is also supported, and the company can assist with acceptance if needed (costs borne by the customer for non-warranty services).
Q2: What should be done if the system’s water output decreases or TDS increases?A2: First check if pretreatment consumables need replacement; if not, perform chemical cleaning of the RO membrane. Contact technical support if the issue persists, and engineers will provide targeted solutions.
Would you like me to help you generate a customized project proposal PPT outline based on this case, highlighting key technical points and quotation details for client presentation?




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian