




1. Case Basic Information

1.1 Project Subject
- Provider: HELLA WATER, a trusted supplier of high-performance water treatment product, specializes in customized industrial wastewater treatment solutions for food processing industries.
- Project Name: Tunisia 600 Tons/Day Cheese Production Wastewater Treatment Project
- Core Objective: Treat high-concentration organic wastewater from cheese production to meet local discharge standards (DB 37/599-2006), realize energy recovery (biogas utilization), and minimize environmental impact.
1.2 Treatment Scale & Water Quality Parameters
Inlet Water Quality (Comprehensive Production Wastewater)
| Parameter | Value |
|---|---|
| CODcr | 21800 mg/L |
| BOD₅ | 9600 mg/L |
| Suspended Solids (SS) | 1600 mg/L |
| Kjeldahl Nitrogen | 298 mg/L |
| Total Phosphorus | 164 mg/L |
| Oil | 250 mg/L |
| Detergent | 4.1 mg/L |
| pH | 3.2 (acidic) |
Effluent Discharge Standard (Local Requirements)
| Parameter | Value |
|---|---|
| CODcr | ≤200 mg/L |
| BOD₅ | ≤50 mg/L |
| SS | ≤50 mg/L |
| Kjeldahl Nitrogen | ≤5 mg/L |
| Total Phosphorus | ≤2 mg/L |
| Oil | ≤10 mg/L |
| Detergent | ≤1 mg/L |
| pH | 6.5-9.0 |
1.3 Core Equipment & Process Configuration
| Process Unit | Key Equipment | Specifications | Quantity |
|---|---|---|---|
| Pretreatment | Mechanical Grille + Dissolved Air Flotation Machine | Hydraulic curved screen; PAM/PAC dosing device | 1 set (grille), 1 set (flotation machine) |
| Regulation & Neutralization | pH Adjustment Pool + Equalization Tank | Semi-underground steel-concrete structure; Effective volume: 200 m³ | 1 set each |
| Anaerobic Treatment | UASB Anaerobic Reactor | Volume: 180 m³; Volume load: 5-10 kgCOD/m³·d | 1 unit |
| Aerobic Treatment | Multi-stage A/O Reaction Tank | Level I A/O: 1200 m³; Level II A/O: 500 m³; Tubular microporous aerator | 1 set |
| Solid-Liquid Separation | Secondary Sedimentation Tank | Surface load: 8 m³/m²·h; Total volume: 800 m³ | 1 unit |
| Sludge Treatment | Spiral Dewatering Machine + Sludge Thickener | DYLT-301 type; PAM dosing device (JY-500) | 1 set each |
| Energy Recovery | Biogas Collection & Purification System | Desulfurization tower + gas storage tank + flame arrester | 1 set |
| Automatic Control | PLC Control System + Online Monitors | DO, pH, level, flow rate monitors; Central control cabinet | 1 set |
1.4 Design Standards & Compliance
The project adheres to industry core standards and regulations, including:
- DB 37/599-2006: Local Wastewater Discharge Standard
- GBJ 14-87 (1997 edition): Code for Design of Outdoor Drainage
- GBJ 13-86: Outdoor Water Supply Design Code
- GB 141-90: Code for Structural Design of Water Supply and Drainage Engineering
- JB2932-1999: Technical Specifications for Water Treatment Equipment
- ISO9001: Quality Management System Certification
1.5 Application Scenarios
- High-concentration organic wastewater treatment in dairy/cheese factories
- Food processing industry wastewater purification (containing proteins, fats, sugars)
- Industrial wastewater treatment projects requiring energy recovery (biogas)
- Acidic wastewater treatment with corrosion protection requirements
- Compliance-oriented wastewater treatment in regions with strict discharge standards
2. Project Core Pain Points & Requirements

2.1 Industry Common Pain Points
- High Pollution Load: Cheese wastewater is high-concentration organic wastewater (COD up to 21800 mg/L) with high nitrogen and phosphorus, leading to severe eutrophication if discharged directly.
- Acidic Corrosion: pH=3.2 acidic wastewater corrodes equipment and pipelines, requiring special anti-corrosion treatment.
- Ammonia Nitrogen Surge: Anaerobic treatment of protein-rich wastewater increases ammonia nitrogen concentration (200-600 mg/L), making denitrification difficult.
- Large Sludge Production: Traditional processes generate massive sludge, increasing disposal costs and secondary pollution risks.
- High Operating Costs: Aerobic treatment of high-concentration wastewater consumes excessive energy; lack of resource recovery leads to waste.
2.2 Customer Core Requirements
- 达标排放: Efficiently remove COD, BOD, ammonia nitrogen, and phosphorus to meet local discharge standards.
- Corrosion Resistance: Ensure equipment and structures withstand acidic wastewater and long-term stable operation.
- Energy Recovery: Utilize biogas generated from anaerobic treatment to reduce energy consumption and operating costs.
- Sludge Reduction: Minimize sludge production and simplify sludge disposal to lower environmental and economic burdens.
- Intelligent Operation: Realize automatic control of pH, flow rate, and aeration to reduce manual intervention.
3. Hella Water Customized Solutions

3.1 Process Design: Anaerobic-Aerobic Integration + Energy Recovery
The solution adopts a “Pretreatment → Regulation & Neutralization → UASB Anaerobic → Multi-stage A/O → Solid-Liquid Separation → Disinfection” integrated process, combined with biogas energy recovery:
- Pretreatment Stage:
- Mechanical Grille: Removes large suspended solids (e.g., cheese residues, fibers) to protect subsequent equipment.
- Dissolved Air Flotation Machine: Cooperates with chemical dosing system (PAM/PAC) to remove 85% of oil and 90% of SS, reducing the burden on biological treatment.
- Regulation & Neutralization Stage:
- Equalization Tank: Balances water quality and quantity (retention time: 5h) to mitigate impact loads; adjusts pH by recycling effluent (no additional neutralizer needed during stable operation).
- pH Adjustment Pool: Temporarily adjusts acidic wastewater during commissioning to ensure suitable conditions for anaerobic/aerobic microorganisms.
- Anaerobic Treatment Stage (Energy Recovery):
- UASB Anaerobic Reactor: Degrades 60-70% of COD through hydrolysis, acidification, and methanogenesis; generates biogas (methane content ≥65%).
- Biogas Utilization: Biogas is purified (desulfurization + dehydration) and used for boiler combustion, power generation, or factory canteen use, reducing energy costs by 30%.
- Aerobic Treatment Stage (Deep Purification):
- Multi-stage A/O Reaction Tank:
- Level I A/O: Denitrification with organic carbon sources in wastewater; reduces nitrate nitrogen to N₂.
- Level II A/O: Nitrification (DO=2-3 mg/L) converts ammonia nitrogen to nitrate nitrogen; realizes deep denitrification and phosphorus removal.
- Tubular microporous aerators ensure high oxygen transfer efficiency, reducing aeration energy consumption.
- Multi-stage A/O Reaction Tank:
- Solid-Liquid Separation & Sludge Treatment:
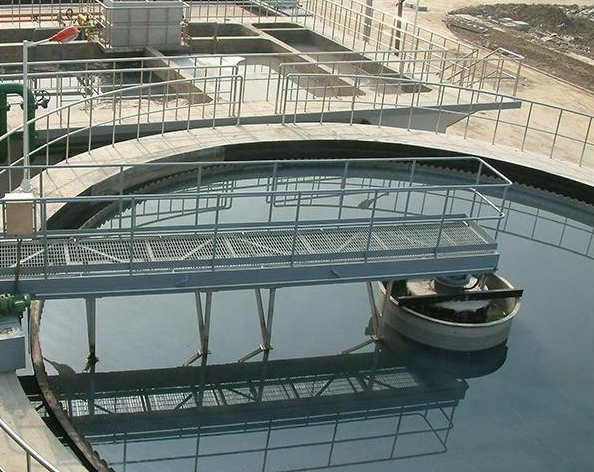
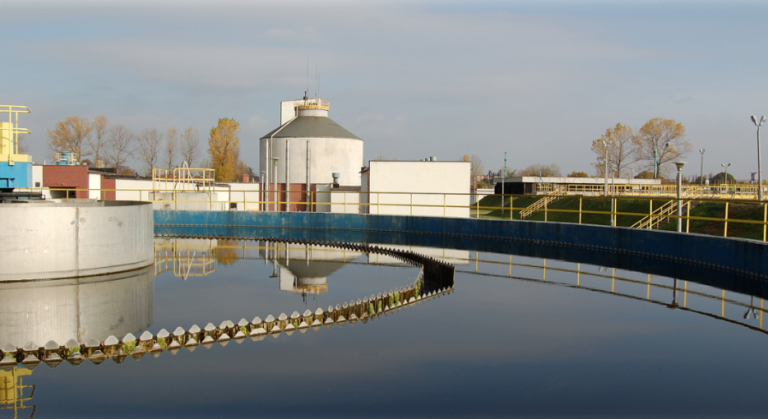
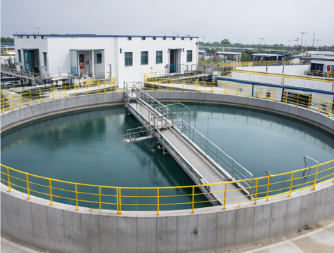
- Secondary Sedimentation Tank: Separates activated sludge from treated water; sludge reflux to A/O tank maintains microbial concentration.
- Spiral Dewatering Machine: Dewaters excess sludge (moisture content ≤60%); granular sludge from UASB is sold as commercial inoculant, realizing resource utilization.
3.2 Core Technical Advantages
| Technical Highlight | Description |
|---|---|
| High-Efficiency Anaerobic-Aerobic Synergy | UASB removes most COD (energy-saving) + multi-stage A/O achieves deep denitrification; total COD removal rate ≥99%, ammonia nitrogen removal rate ≥98%. |
| Corrosion Protection Design | Steel-concrete structures with fiberglass lining; acid-resistant pumps/pipelines; adapts to pH=3.2 acidic wastewater. |
| Energy Recovery | Biogas generation (≈0.5 m³ biogas/kgCOD degraded) reduces energy consumption by 30-40% compared to traditional processes. |
| Sludge Reduction | Anaerobic sludge production (0.05 kg/kgCOD) is 1/10 of aerobic processes; granular sludge recycling reduces disposal costs. |
| Intelligent Control | PLC automatic control of pH, flow rate, and aeration; online monitors (DO, pH, level) trigger alarms and adjust parameters in real time. |
3.3 Key Supporting Systems
- Pre treatment filtration system: Grille + flotation machine ensures inlet water quality for UASB and A/O systems.
- Anti-corrosion System: Fiberglass lining for tanks, acid-resistant pipelines/pumps, and stainless steel components to extend service life.
- Emergency Protection: Overflow pipes and accident tanks prevent untreated wastewater discharge during equipment failure.
4. Project Effectiveness Verification
4.1 Pollutant Removal Efficiency
| Pollutant | Inlet Concentration | Effluent Concentration | Removal Rate |
|---|---|---|---|
| CODcr | 21800 mg/L | ≤200 mg/L | ≥99.1% |
| BOD₅ | 9600 mg/L | ≤50 mg/L | ≥99.5% |
| SS | 1600 mg/L | ≤50 mg/L | ≥96.9% |
| Kjeldahl Nitrogen | 298 mg/L | ≤5 mg/L | ≥98.3% |
| Total Phosphorus | 164 mg/L | ≤2 mg/L | ≥98.8% |
| Oil | 250 mg/L | ≤10 mg/L | ≥96.0% |
4.2 Operational Performance
- Stability: Continuous operation for 8000 hours with stable effluent quality; adapts to ±30% flow fluctuations and ±25% COD concentration changes.
- Energy Efficiency: Biogas generation ≈10,900 m³/d (based on 21800 mg/L COD); annual energy saving ≈360,000 kW·h, reducing operating costs by USD 36,000 (0.1 USD/kW·h).
- Sludge Reduction: Annual sludge production ≤150 tons (moisture content 60%), 70% less than traditional aerobic processes.
- Corrosion Resistance: No equipment corrosion reported after 2 years of operation; anti-corrosion components maintain good performance.
4.3 Economic & Environmental Benefits
- Economic Benefits: Annual energy savings USD 36,000; sludge disposal cost reduction USD 20,000; granular sludge sales income USD 15,000; total annual economic benefit ≈USD 71,000.
- Environmental Benefits: Annual reduction of COD emission by ≈7,900 tons; ammonia nitrogen emission by ≈107 tons; phosphorus emission by ≈60 tons; biogas utilization reduces greenhouse gas (methane) emission.
5. Case Corresponding Product Quotation Description
5.1 Quotation Overview
| Item | Description | Total Amount (USD) |
|---|---|---|
| Core Equipment | UASB reactor, multi-stage A/O tank, flotation machine, sludge dewatering system | Included in total |
| Auxiliary Systems | Biogas purification system, automatic control system, online monitors | Included in total |
| Engineering Design & Installation | Civil construction design, equipment installation, pipeline connection | Included in total |
| Total Project Quotation | – | 2,171,450 |
5.2 Quotation Terms
| Term Type | Details |
|---|---|
| Validity Period | 45 working days from the date of quotation |
| Payment Terms | Negotiable (reference: 30% advance payment, 40% during construction, 30% after acceptance) |
| Project Cycle | 7 months (1 month design + 3 months civil construction + 2 months equipment installation + 1 month commissioning) |
| Warranty Period | 12 months from the date of acceptance (free repair/replacement for non-human damage) |
| Incoterms | DAP (Delivered at Place, Tunisia) |
| Additional Services | Free operator training (2-3 personnel); 24/7 online technical support |
5.3 Additional Notes
- The quotation includes equipment, design, installation, and commissioning; civil construction materials (steel, concrete) are excluded.
- Spare parts (aerators, pumps, filters) are provided at 15% of the equipment price for long-term supply.
- Biogas utilization system can be customized (power generation/boiler combustion) based on factory needs.
6. Frequently Asked Questions (FAQ)
6.1 Installation & Commissioning
Q: What are the on-site installation requirements for the UASB reactor?
A: The UASB reactor requires a flat foundation with load-bearing ≥5 tons/m²; installation space ≥10m×6m×8m (length×width×height). It needs to be connected to biogas storage and purification facilities; we provide detailed installation drawings and dispatch 2-3 engineers for on-site guidance. Commissioning takes 1 month, including granular sludge inoculation and system stabilization.
6.2 Maintenance & Upkeep
Q: How often does the UASB reactor and A/O tank require maintenance?
A: Routine maintenance includes: 1) UASB reactor: Check three-phase separator and water distributor every 3 months; desulfurize biogas system every 6 months. 2) A/O tank: Clean aerators every 6 months; replace worn aerator membranes every 2 years. 3) Sludge dewatering machine: Clean screw shaft every week; replace filter screen every 1 year.
Q: What is the service life of core equipment?
A: UASB reactor (15-20 years), multi-stage A/O tank (15 years), biogas purification system (10 years), sludge dewatering machine (8-10 years). We provide lifelong technical support and preferential spare parts supply.
6.3 Warranty & After-Sales
Q: What is covered under the 1-year warranty period?
A: Within the warranty period, we provide free repair or replacement for faults caused by design, manufacturing, or material defects, including core equipment (UASB reactor, A/O tank, control system), pumps, aerators, and monitors. Damage from improper operation, corrosion due to non-compliant water quality, or natural disasters is not covered.
Q: How to get after-sales technical support for overseas projects?
A: We provide 24/7 online support via email and video calls; for urgent on-site issues, technicians can be dispatched to Tunisia within 72 hours (additional fees apply for international travel). We also conduct semi-annual return visits to monitor system operation.
6.4 Operational Cost
Q: What is the estimated monthly operating cost of the system?
A: The main operating costs include electricity (aeration, pumps), chemicals (PAM/PAC), and labor. For a 600m³/d system, the monthly electricity cost is about USD 4,500 (excluding biogas energy savings), chemical cost about USD 1,200, and labor cost about USD 2,000. With biogas energy savings (≈USD 3,000/month), the net monthly operating cost is ≈USD 4,700.
6.5 Safety & Compliance
Q: Is biogas utilization safe, and how to prevent explosion risks?
A: Yes. The biogas system is equipped with desulfurization towers (removes H₂S), flame arresters, and pressure relief valves. The gas storage tank is installed in an open area ≥10m away from buildings; online biogas flow monitors trigger alarms for abnormal pressure. We provide safety training for operators to ensure compliant use.
Q: How to handle sudden increases in ammonia nitrogen concentration?
A: The multi-stage A/O system has strong shock resistance; the PLC control system automatically increases the nitrification liquid reflux ratio (up to 300%) and adjusts aeration intensity to enhance denitrification. If ammonia nitrogen exceeds 500 mg/L, the system activates emergency dosing of external carbon sources (e.g., methanol) to ensure effluent compliance.




 English
 Chinese
 German
 Russian
 Japanese
 French
 Dutch
 Italian